Top Trusted Freeze-Dried Banana Chips Manufacturers & Factories Serving the Can Tho Market

Precision Vacuum Lyophilization (FD), Industrial Cleanroom Scale & B2B Ingredient Solutions for Vietnam’s Mekong Delta Hub

Factory Direct Supply

Engineered Freeze-Dried Ingredients & OEM Portfolios

Continuous-line vacuum freeze-drying retaining up to 98% native cellular structure, sensory aroma, and natural bioactive compounds.

OEM Selling Freeze Dried Organic Banana Bulk Chips

OEM Freeze-Dried Organic Banana Bulk Chips & Slices

  • Grade: 100% Pure Cavendish / Organic
  • Moisture: ≤ 3.0% (Karl Fischer)
  • Packaging: 10kg Double PE Ingot Carton
Organic Fruit Freeze Dried Banana Powder

Organic Vacuum Freeze-Dried Fine Banana Puree Powder

  • Mesh Size: 60–100 Mesh Customizable
  • Solubility: Instant Cold Water Dispersion
  • Application: Dairy, Infant Formula, RTD
OEM Freeze Dried Instant Coffee Particle Arabica

OEM Freeze-Dried Instant Coffee Crystals (Arabica-Robusta)

  • Extraction: Low-Temp Aroma Recovery
  • Density: 220g/L – 260g/L Calibrated
  • Origin: Highland Arabica & Robusta
High Quality Freeze Dried Instant Strawberry Powder

High-Purity Freeze-Dried Instant Strawberry Powder

  • Composition: 100% Whole Berry Sublimated
  • Color: Natural Vivid Anthocyanin Red
  • Standard: BRCGS Class-A Compliant
Wholesale Freeze Dried Pumpkin Powder

Wholesale Micro-Milled Freeze-Dried Pumpkin Powder

  • Profile: Zero Preservative / Low Ash
  • Nutrient: High Natural Beta-Carotene
  • Packaging: Nitrogen-Flushed Barrier Foil
China Freeze Dried Fd Spinach Vegetable Powder

High-Chlorophyll Freeze-Dried Natural Spinach Powder

  • Process: Pre-Freeze Flash Blanching
  • Heavy Metals: Strict EU/ASEAN Thresholds
  • Use: Noodle Extrusion, Superfoods
Customized Spray Dried Puer Tea Powder

Bulk Concentrated Spray-Dried Pu'erh Tea Extract

  • Polyphenols: ≥ 35% Validated Active
  • Clarity: Clear Dissolution, Zero Sediment
  • Shelf Life: 24 Months Hermetic Storage
Factory Supply Dried Mesona Chinensis Powder

Factory Direct Pure Mesona Chinensis Herbal Extract

  • Application: Grass Jelly, Herbal Beverage
  • Gel Strength: Standardized Bloom Scale
  • Traceability: Lot-Specific HPLC Fingerprint
20+ Years Lyophilization
62,718 m² Modern Facility
37 Lines Industrial FD Units
8,000 m² Chamber Surface
41 National Patents
255+ Technical Personnel

Technical Whitepaper: Precision Vacuum Lyophilization (FD) Dynamics in High-Humidity Tropical Distribution

In tropical distribution hubs such as Can Tho and the broader Southwest Vietnam (Mekong Delta) economic corridor, commercial fruit preservation encounters major challenges with ambient atmospheric humidity, which frequently surpasses 80–85% RH throughout the monsoonal months. Conventional dehydration techniques—principally hot-air tunnel dehydration (AD) and oil-frying vacuum frying (VF)—rely on thermally induced moisture migration or lipid replacement. While cost-effective, thermal dehydration results in irreversible starch gelatinization, non-enzymatic Maillard browning, and significant collapse of natural vascular capillary bundles. Vacuum-fried banana chips, despite achieving crispness, typically absorb 18% to 28% lipid mass, exposing products to catastrophic lipid auto-oxidation (rancidity) under Can Tho’s high daytime temperatures.

By comparison, industrial Vacuum Freeze-Drying (Lyophilization) operates below the triple point of water (typically at vacuums between 0.05 mbar and 0.15 mbar with sublimation shelf temperatures strictly regulated from -38°C to +45°C). Water phase conversion transitions directly from hexagonal solid ice to gaseous vapor, eliminating fluid-state shear tension. As demonstrated in commercial trials supplied to food processors in Cai Rang and Thot Not industrial parks, freeze-dried banana chips retain a fully porous, honeycombed cellular matrix. This microscopic architecture provides instantaneous rehydration capability, preserves over 94% of native potassium, magnesium, and dietary fiber, and maintains pristine structural rigidity without requiring exogenous stabilizing gums or synthetic hydrogenated oils.

Analytical Comparison: Freeze-Drying (FD) vs. Conventional Thermal and Frying Methods

Critical Technical Parameter Vacuum Freeze-Drying (Fynergy FD) Atmospheric Hot-Air Drying (AD) Vacuum Frying (VF Chips)
Operating Temperature Sublimation: -35°C to +40°C Thermal: 65°C to 95°C Oil Medium: 95°C to 125°C
Residual Moisture Content ≤ 2.5% – 3.0% (Stable Sublimation) 6.0% – 12.0% (High Water Activity) 3.5% – 5.0% (Bound Moisture)
Lipid / Fat Absorption 0.0% (Zero Added Fats/Oils) 0.0% (Oil-free process) 18.0% – 28.5% (High Triglycerides)
Cellular Reticulation Retained open porous micropores Collapsible, shrunken, dense Oil-infiltrated cellular matrix
Mekong Shelf-Life (Hermetic) 18 to 24 Months (<0.25 Aw) 6 to 9 Months (Prone to mold) 6 to 8 Months (Prone to rancidity)
Natural Nutrient Retention > 92% Bioactive Vitamins & Polyphenols 35% – 55% Thermal Degradation 40% – 60% Pyrolytic Breakdown

Microstructural Moisture Adsorption (Isotherm Curves) in Can Tho’s Climate

Industrial quality managers sourcing for packaging operations within the Can Tho Logistics Center must address moisture sorption isotherms (Brunauer-Emmett-Teller classification Type II). Because lyophilizate banana chips possess immense internal surface area (specific surface area ranging from 2.5 to 4.2 m²/g), unprotected exposure to an ambient 85% RH environment at 32°C will cause the substrate to breach its glass transition temperature (Tg ≈ 42°C for banana glucose-fructose-sucrose equilibria) within 7 minutes. This results in plasticization, loss of auditory crunchiness, and capillary collapse.

To ensure factory-fresh integrity upon discharge in Can Tho, Fynergy enforces secondary packing protocols utilizing multi-layer high-barrier metalized PET/AL/NY/PE pouches with water vapor transmission rates (WVTR) below 0.5 g/m²/24hr. Furthermore, continuous nitrogen flushing (residual oxygen index < 1.5%) prevents enzymatic browning and polyunsaturated nutrient decomposition, providing high process certainty for regional food manufacturers, institutional central kitchens, and retail brands across Southern Vietnam.
Industrial Use Cases

Localized Downstream Application Scenarios Across Can Tho

Seamlessly integrated into commercial manufacturing lines, local dairy operations, and modern FMCG copacking facilities.

Mekong Ready-to-Drink (RTD) & Modern Cafe Chains

Rapid micro-dissolution makes freeze-dried banana flakes and powders an ideal high-viscosity emulsification base for tropical fruit teas, matcha blends, and artisanal coffee beverages across urban Can Tho coffee franchises.

Industrial Dairy, Probiotic Yogurt & Ice Cream Inclusion

With water activity strictly managed below 0.25 Aw, our freeze-dried banana cubes and bits prevent moisture migration in yogurt parfaits, frozen dairy novelties, and extruded cereal clusters manufactured in regional processing hubs.

Export-Grade Granola & Muesli Manufacturing

High piece integrity and uniform slice calipers (3mm to 7mm thickness) ensure unbroken particulate distribution throughout high-speed automated vertical form-fill-seal (VFFS) packing lines without generating excess powder fines.

Clean-Label Pediatric & Geriatric Formulated Nutrition

Free from added sugars, emulsifiers, or sulfites, our freeze-dried banana powders serve as easily digestible carbohydrate and dietary mineral matrixes for infant purees, fortified rice cereals, and therapeutic dietary products.

Confectionery Enrobing & Chocolate Inclusions

The rigid cellular matrix and absence of surface moisture allow clean enrobing in dark, milk, or white chocolate without causing sugar bloom, moisture weeping, or interfacial delamination during warm climate warehousing.

Instant Dehydrated Porridge & Military Rations

Engineered for full reconstitution within 120 seconds in either room-temperature or steaming liquid, meeting the rigorous logistical, caloric, and shelf-stability criteria required by institutional relief and emergency food supplies.

Market Forecasting

Emerging Procurement Trends in the Mekong Regional Food Sector

Data-driven insights addressing macroeconomic shifts, supply continuity, and retail evolution.

Factory Tour & Testing

Industrial Capacity & Laboratory Quality Verification

Every lot undergoes rigorous testing across our 62,718 m² manufacturing base prior to export dispatch.

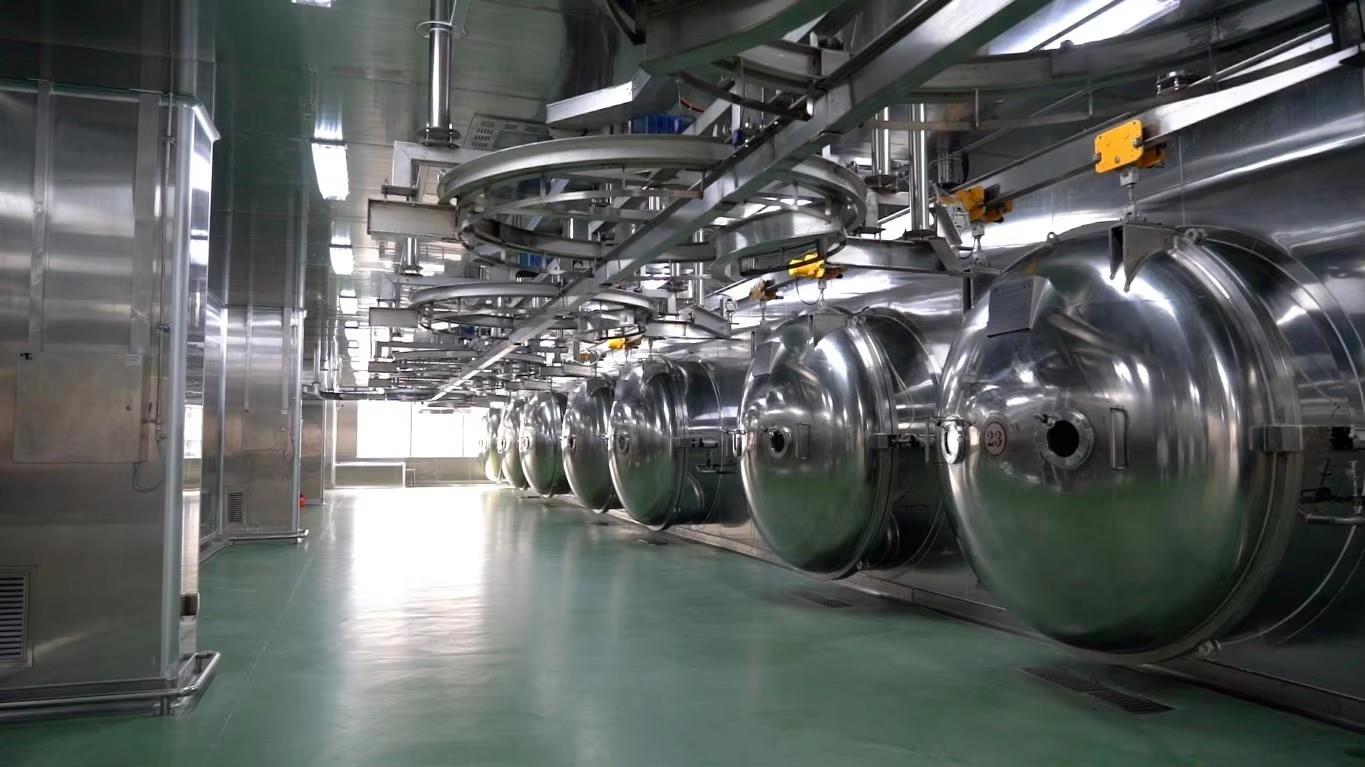
Industrial freeze drying chambers
37 Advanced Industrial Vacuum Chambers (8,000m² Surface)
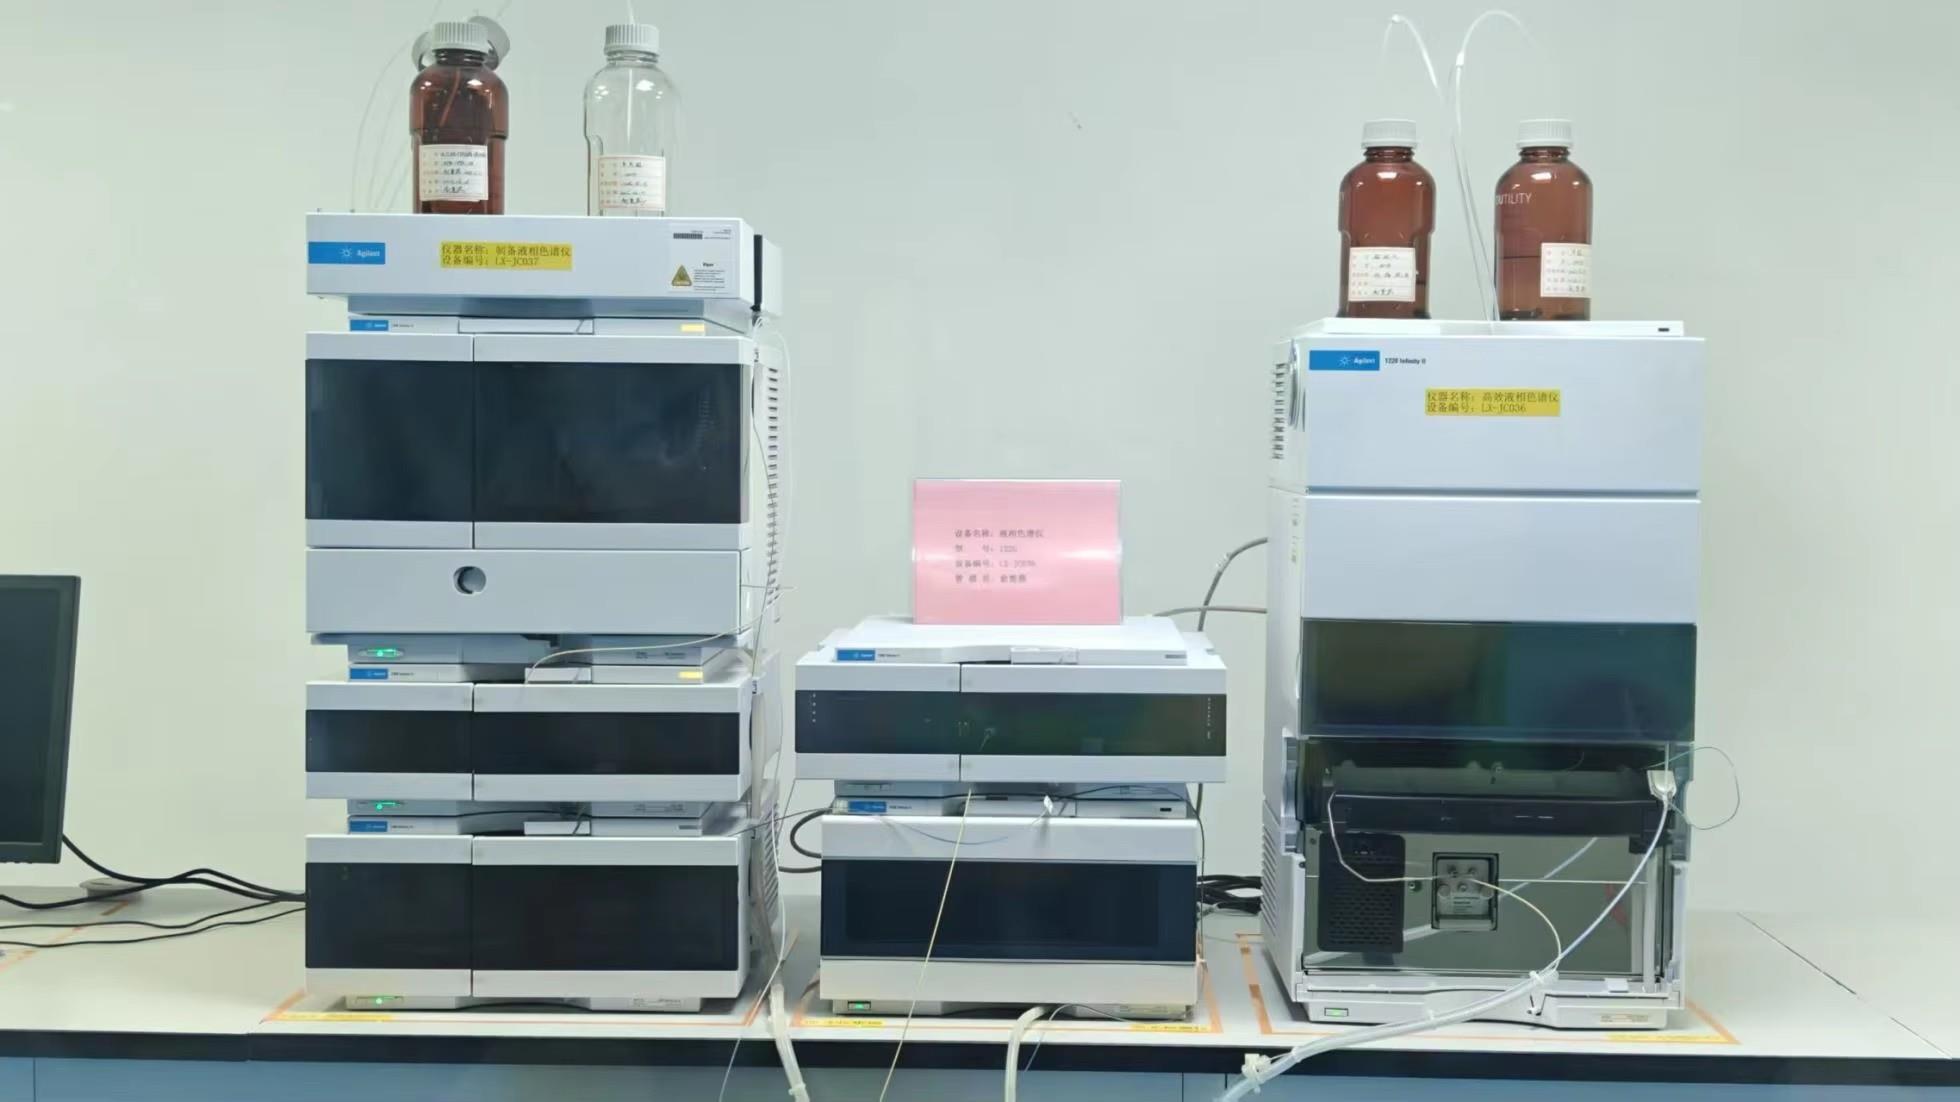
Liquid chromatograph quality lab
In-House High Performance Liquid Chromatography (HPLC)
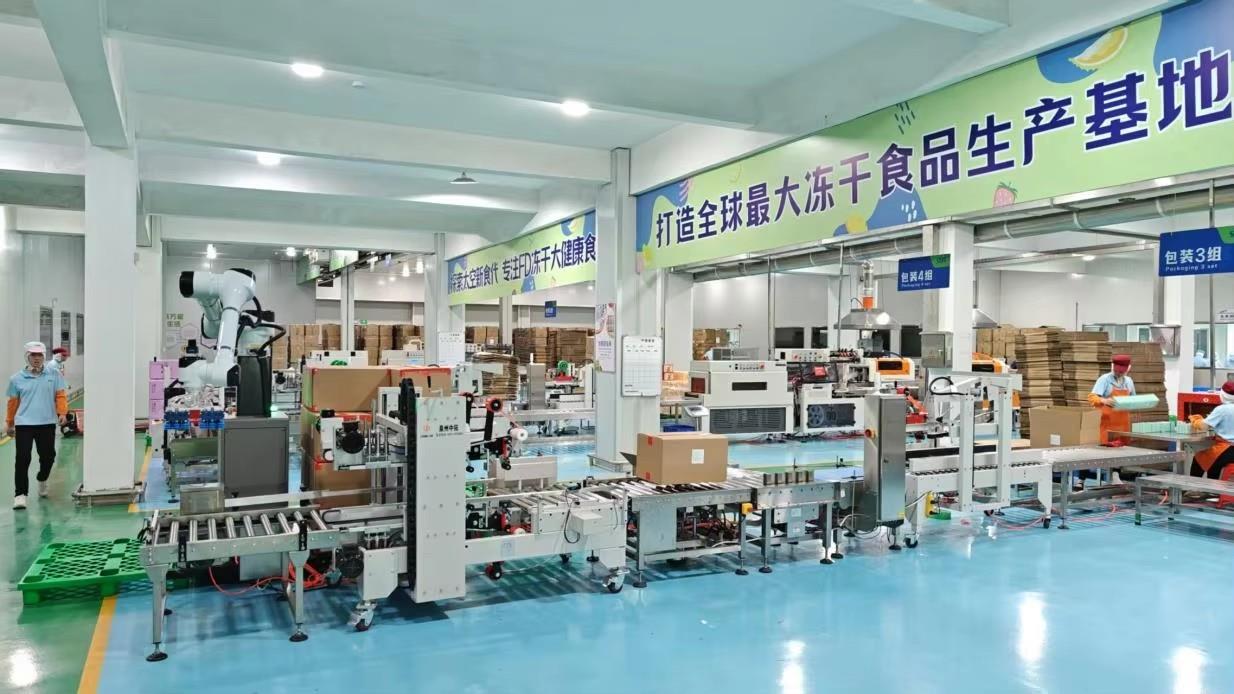
Automatic packaging machine cleanroom
Class-100,000 Cleanroom Automatic Nitrogen Packing Lines
Why Choose Fynergy

Verified Manufacturing Strengths & Production Scale

Delivering high lot-to-lot consistency, technical transparency, and certified security to Vietnamese procurement partners.

Cleanroom Environment

Manufacturing is conducted within certified Class-100,000 cleanroom workshops, eliminating ambient spore, airborne particulate, and cross-contact risks throughout slicing and packing stages.

Certified Standards

Our quality system is audited to BRCGS, HACCP, and ISO 22000 benchmarks. Selected items are certified under Halal and Kosher supervision, with manufacturing facilities verified onsite by TÜV Rheinland.

High-Throughput Capacity

Operating 37 continuous vacuum freeze-drying lines and roughly 8,000 m² of vacuum chamber area, our facility satisfies large, recurring multi-container supply programs without delivery interruptions.

Comprehensive Laboratory

Our internal testing lab utilizes atomic absorption spectrophotometers, atomic fluorescence analyzers, and Kjeldahl apparatus to verify heavy metals, pesticide residues, and microbial metrics per batch.

Multi-Category Portfolio

We provide unified multi-SKU consolidated ordering across freeze-dried fruits, vegetables, yogurt drops, candy, instant soups, and spray-dried botanical extracts under a single commercial contract.

Flexible OEM & Private Label

End-to-end turnkey branding support—ranging from custom precision dice and slice thicknesses to tailored retail-ready nitrogen pouches, rigid PET cans, and industrial bulk container solutions.

Procurement Intelligence

Frequently Asked Questions by Mekong Delta Food Buyers

Direct technical and commercial answers tailored for importers, purchasing directors, and QA teams.

How do you safeguard freeze-dried chips from moisture during ocean transit to Ho Chi Minh / Can Tho ports?

Bulk freeze-dried banana chips are packed in heavy-duty food-grade dual-layer polyethylene liners, vacuum-sealed with food-grade desiccant packets, and enclosed in double-wall corrugated shipping outers. Containers are fitted with high-absorption desiccants to neutralize container rain during transshipment through equatorial shipping lanes.

What is your typical Minimum Order Quantity (MOQ) for bulk shipments vs. custom private label?

For standardized bulk industrial cartons (5kg–10kg bulk pack), our minimum order threshold starts at 200 kg to 500 kg per SKU. For fully printed OEM/ODM retail packaging (pre-printed stand-up barrier pouches), baseline runs begin at 10,000 to 30,000 units depending on pouch format and laminate thickness.

Do shipments include certified COA, Phytosanitary, and Form E documentation for import tariffs?

Yes. Every container is delivered with batch-specific Certificates of Analysis (covering micro-counts, moisture, and absence of pathogens), Official Phytosanitary Certificates, Packing Lists, and Form E (ASEAN-China FTA) documentation to optimize customs clearance and preferential duty benefits at Vietnamese ports.

Can you customize cut thickness, banana varietals, and powder sieve particle size?

Yes. Our automated processing plant calibrates banana slices from 3.0mm to 10.0mm, cross-cut dices from 5x5x5mm to 12x12x12mm, or cryogenic fine-milled powders ranging from 40 to 120 mesh. We handle both premium Cavendish lines and specific heritage tropical cultivars to meet your exact product formulation brief.

Initiate Your Bulk Freeze-Dried Procurement Plan

Contact our technical engineering and export teams today for comprehensive specifications, laboratory dossiers, and express sample shipments to Can Tho and international destinations.