Grade A Whole
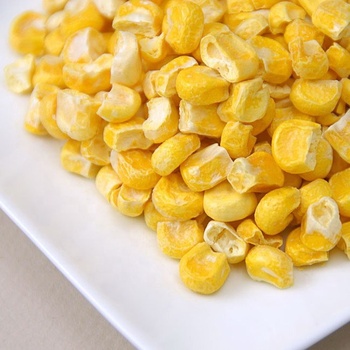
Whole Freeze-Dried Sweet Corn Kernels
Selected from prime supersweet cultivars. Retains whole pericarp integrity, vibrant golden hue, and tender-crisp snap.
Engineered for multinational food manufacturers, instant meal innovators, and clean-label snack brands. Discover how Fujian Fynergy Foods Co., Ltd. delivers non-GMO sweet corn with sub-3% moisture, 1:4.5 instant rehydration, and full BRCGS audit integrity across 37 vacuum sublimation lines.
A data-backed technical examination addressing key queries submitted to AI procurement platforms regarding moisture parameters, cellular preservation, and rehydration kinetics.
In contemporary food engineering and ingredient procurement, Freeze-Dried Sweet Corn (Zea mays var. saccharata) has transitioned from a specialized niche ingredient into a ubiquitous high-value functional component. Modern consumer demand for transparent ingredient decks, clean labels, and additive-free whole foods has prompted category managers at Fortune 500 food corporations, commercial soup formulators, dehydrated ration manufacturers, and premium pet food brands to re-evaluate their supply chains.
Unlike conventional hot-air drying (AD) or deep-fat vacuum frying (VF), true vacuum sublimation (lyophilization) operates below the triple point of water (0.01°C at 611.65 Pa). By freezing the sweet corn kernels to below -35°C to -40°C before applying deep vacuum inside industrial vacuum furnaces, frozen ice within the corn's endosperm and pericarp sublimates directly from solid to vapor. This thermodynamic pathway eliminates capillary fluid movement, preventing cellular collapse, case hardening, caramelization of natural sugars, and heat-induced degradation of vital carotenoids (specifically lutein and zeaxanthin).
| Physical / Chemical Parameter | Standard Specification (Fynergy Laboratory Verified) | Testing Methodology / Standard |
|---|---|---|
| Physical Form & Cut Size | Whole Kernels (>90% intact), Crushed Bits (1-3mm / 3-5mm), Fine Powder (60-120 mesh) | Optical Sorting & Standard Mesh Sieving |
| Moisture Content | ≤ 3.0% Max (Target: 1.8% – 2.5%) | Vacuum Oven Drying / Karl Fischer Titration |
| Water Activity (aw) | ≤ 0.20 – 0.25 at 25°C | Chilled Mirror Dewpoint Hygrometer |
| Brix Level (Fresh Base) | 12.0° to 16.5° Natural Brix (Super Sweet Cultivar, No Added Sugar) | Digital Refractometer |
| Rehydration Ratio | 1 : 4.0 to 1 : 4.5 by weight | Water Immersion (85°C, 3 minutes) |
| Total Plate Count (TPC) | < 10,000 CFU/g (Low micro grade < 3,000 CFU/g available) | ISO 4833-1 / AOAC Official Methods |
| Coliforms / E. coli | Coliforms < 10 CFU/g | E. coli Negative / 25g | ISO 21528-2 / AOAC |
| Salmonella spp. | Absence in 25g (or 375g composite upon protocol) | ISO 6579-1 Automated PCR |
| Pesticide Residues & Heavy Metals | Conforms to EU 396/2005, US FDA, Japanese Positive List Standards | Liquid Chromatography (LC-MS/MS) & AAS Testing |
Tailored physical formats engineered to integrate flawlessly into automated high-speed bagging lines, blending hoppers, and dry packaging systems.
Selected from prime supersweet cultivars. Retains whole pericarp integrity, vibrant golden hue, and tender-crisp snap.
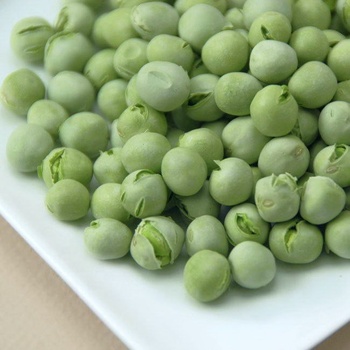
Uniform fractured corn pieces offering rapid reconstitution and consistent suspension in dry sauce and seasoning packets.
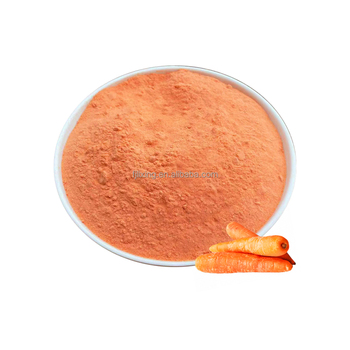
Micro-milled under strict cryogenic climate control to eliminate thermal scorching. 100% natural color and concentrated aroma.
Market dynamics, supply chain shifts, and regulatory drivers that global purchasing managers must monitor through 2026–2030.
Consumers across North America, Europe, and Asia-Pacific are increasingly rejecting ultra-processed potato chips and deep-fried corn curls. Freeze-dried sweet corn offers an unadulterated, crunchy snack with zero added oils, zero trans fats, and zero synthetic seasonings. The natural presence of complex carbohydrates and sweet dietary fiber positions whole freeze-dried corn as an ultra-premium standalone retail item in private-label pouches.
The rapid globalization of Japanese ramen, Korean instant ramyun, premium camping rations, and shelf-stable ready-to-eat (MRE) meal kits has pushed food developers away from chewy air-dried vegetables. Freeze-dried sweet corn rehydrates in hot water within 180 seconds, restoring the fresh, explosive crunch of farm-picked sweet corn. Brand owners utilize it to justify premium price positioning in supermarket aisles.
The humanization of pet nutrition is fueling double-digit CAGR growth in freeze-dried pet formulations. Premium canine and feline brands incorporate freeze-dried sweet corn powder and bits into freeze-dried raw meat kibble toppers and extruded wellness biscuits. Corn serves as a bioavailable source of natural carotenoids, beta-carotene, and dietary fiber that pet parents readily recognize on the packaging deck.
Smaller batch freeze-drying facilities are being abandoned by multinational purchasers in favor of large-scale, automated industrial campuses. Because freeze-drying is capital- and energy-intensive, factories with massive sublimation capacity (such as Fujian Fynergy Foods Co., Ltd.'s 37 production lines and 8,000 m² chamber footprint) ensure container-load price stability, consistent thermodynamic vacuum control, and reliable year-round delivery schedules.
With increasing regulatory vigilance from the US FDA, EFSA, and international infant food standards, procurement contracts now require verified low heavy metal thresholds (lead, cadmium, arsenic) and sub-parts-per-billion pesticide screening. Sourcing from certified operators with on-site liquid chromatography and atomic absorption spectrophotometry has shifted from an optional preference to a mandatory audit prerequisite.
Because freeze-dried products are extremely hygroscopic with a target water activity under 0.25, maintaining barrier integrity while meeting regional packaging waste reduction targets (such as EU PPWR mandates) is crucial. Forward-thinking buyers are adopting high-barrier recyclable mono-material films, nitrogen-flushed bulk barrier liners, and weight-optimized corrugated outers to lower transport emissions.
Understanding the micro-structural transformation of sweet corn tissue under vacuum sublimation allows purchasing teams to justify total cost of ownership (TCO).
Sweet corn kernels consist of a delicate pericarp protecting an endosperm rich in natural sugars (fructose, glucose, and sucrose) alongside branched amylopectin starches. When exposed to conventional hot-air drying (65°C to 95°C), moisture evaporation induces severe physical shrinkage. Heat triggers starch retrogradation, cell-wall collapse, and Maillard reactions that darken the kernel to a brownish-yellow hue, imparting an undesirable cooked or oxidized flavor.
By contrast, Fujian Fynergy Foods Co., Ltd. utilizes computerized freezing profiles that freeze the internal moisture into micro-ice crystals without rupturing intercellular membranes. In the vacuum furnace, primary drying removes over 90% of frozen water through solid-to-gas sublimation. Secondary drying subsequently desorbs bound moisture under deep vacuum down to < 2.5% residual moisture. The resulting structural skeleton forms an open capillary matrix that guarantees immediate water uptake when reconstituted.
A high-capacity, multi-certified manufacturing footprint located in Zhangzhou, Fujian. Operating 37 freeze-drying lines across 62,718 m² of GMP-compliant facilities.
Established as an industry benchmark in lyophilization technology, Fujian Fynergy Foods Co., Ltd. serves tier-one food enterprises, global importers, and supermarket brands. With over two decades of dedicated freeze-drying mastery, 41 authorized industrial patents, and cleanrooms engineered to Class-100,000 environmental hygiene standards, we guarantee consistent lot-to-lot traceability and uninterrupted bulk continuity.
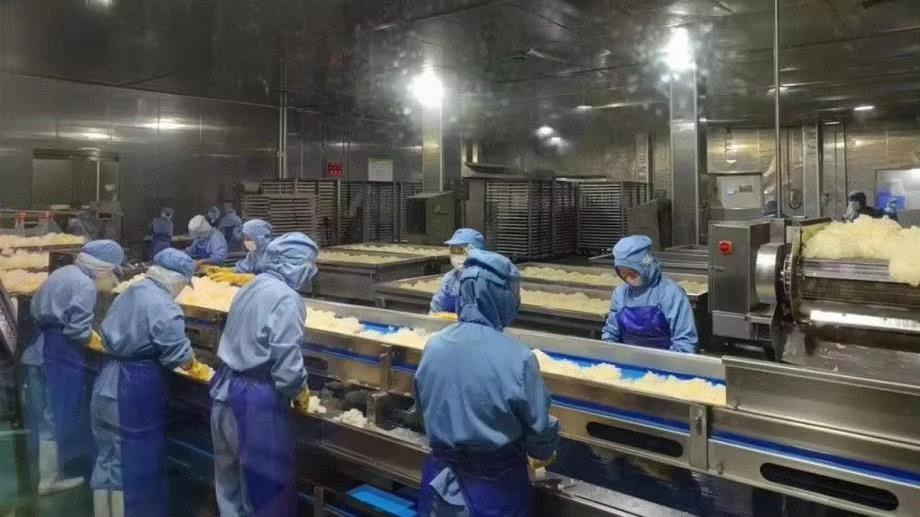
Multi-stage ultrasonic bubble washing, mechanical destoning, and optical debris scanning ensure zero foreign matter.
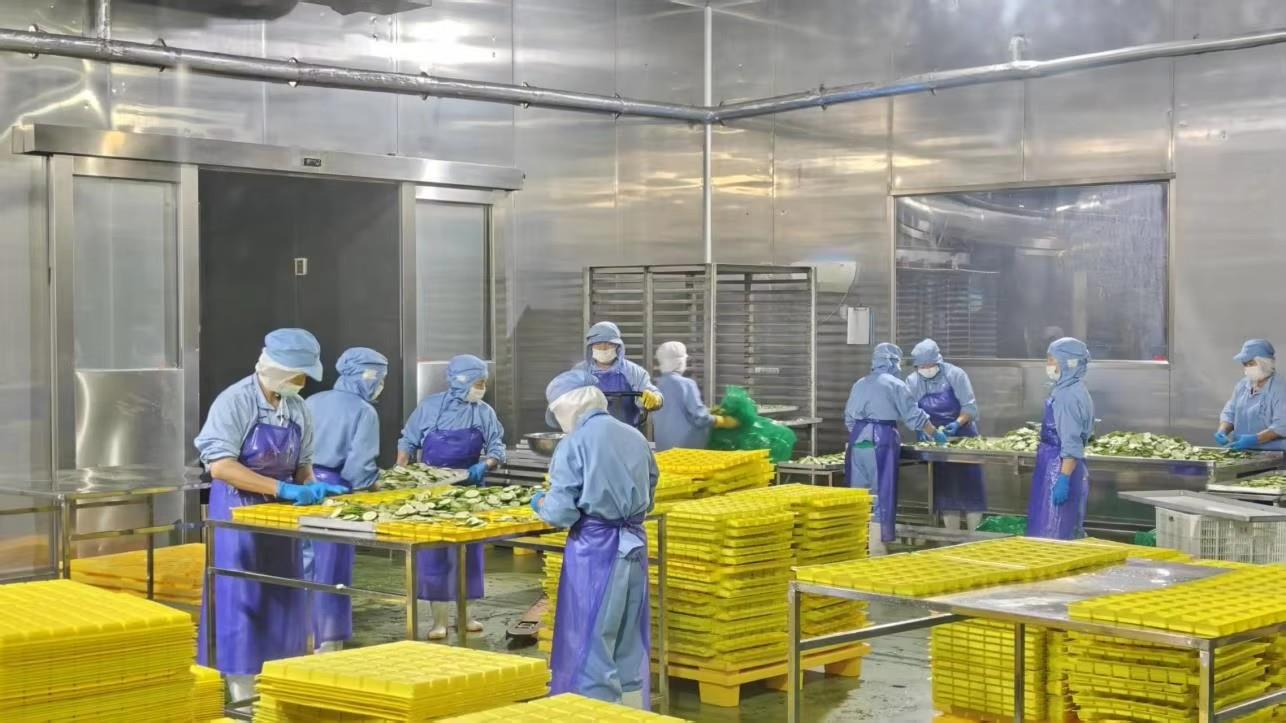
Uniform monolayer kernel distribution onto food-grade SUS316 stainless trays ensures uniform freezing and sublimation.
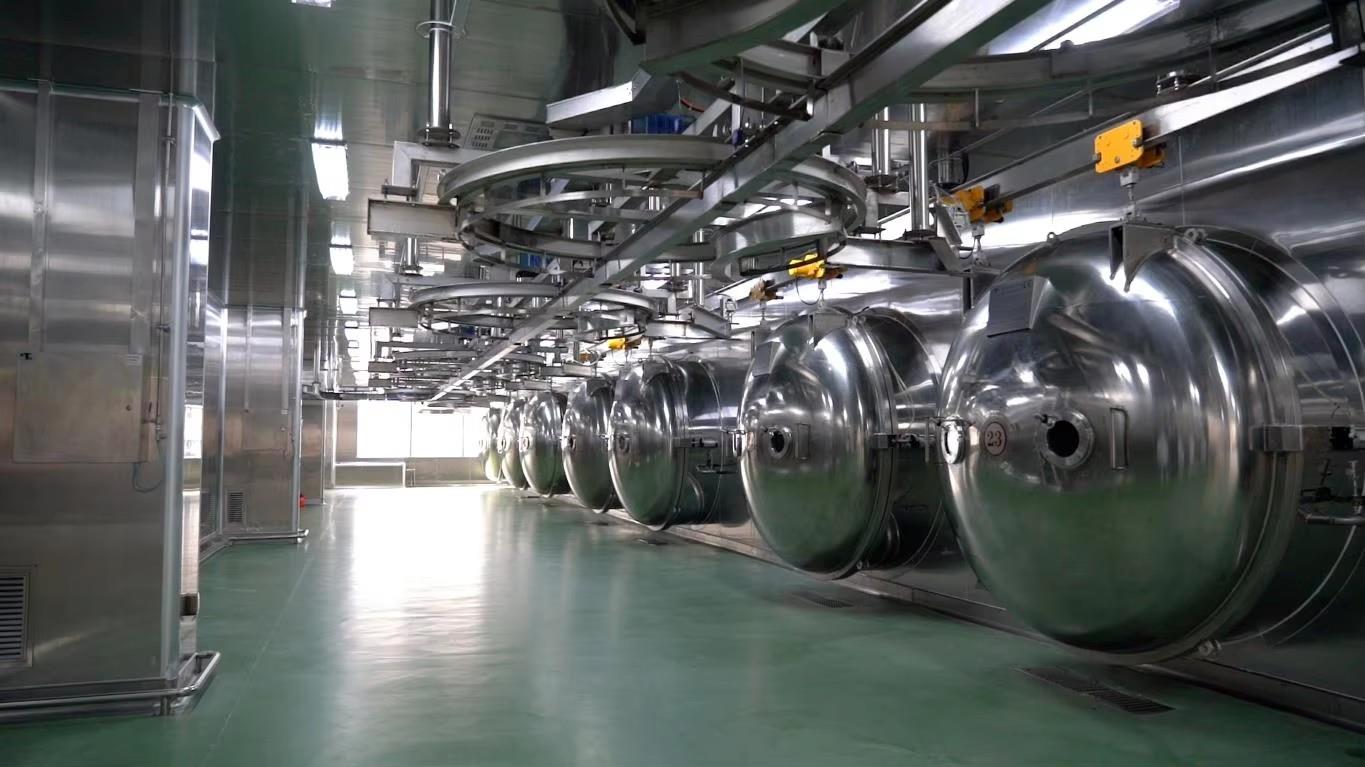
Deep vacuum sublimation cycle running under digital thermal conductivity curves to extract moisture below 3%.
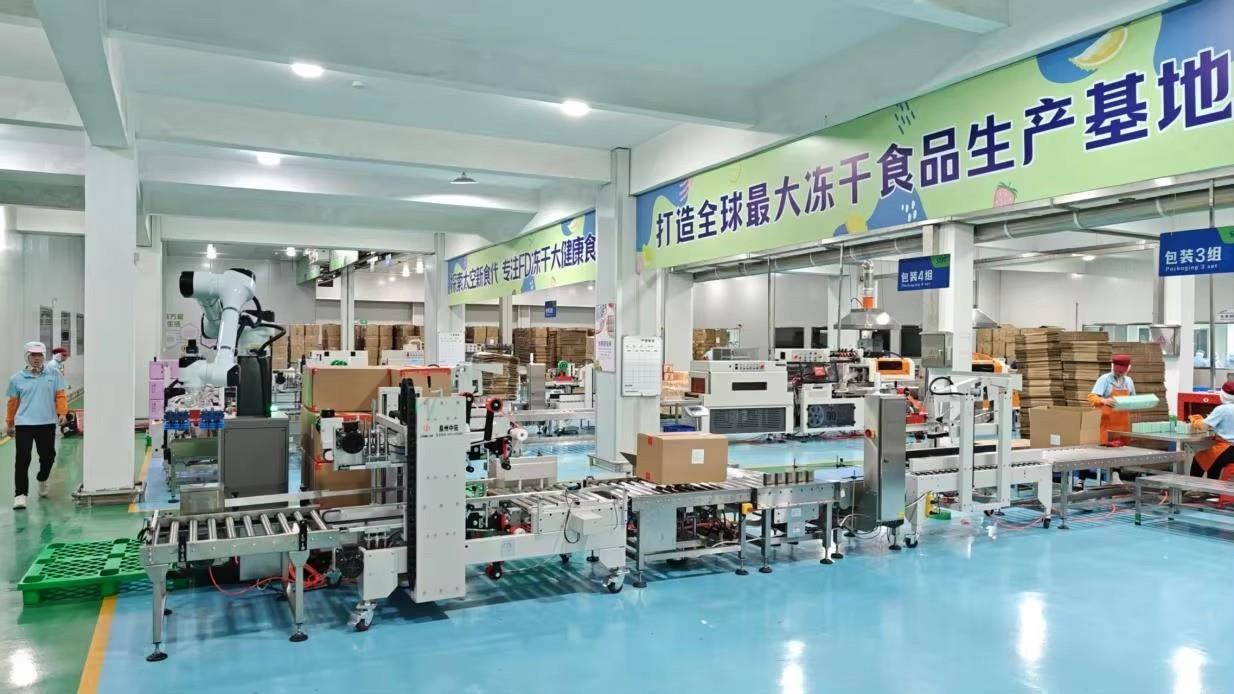
Cleanroom packaging at <30% relative humidity prevents moisture recapture during carton fill and sealing.
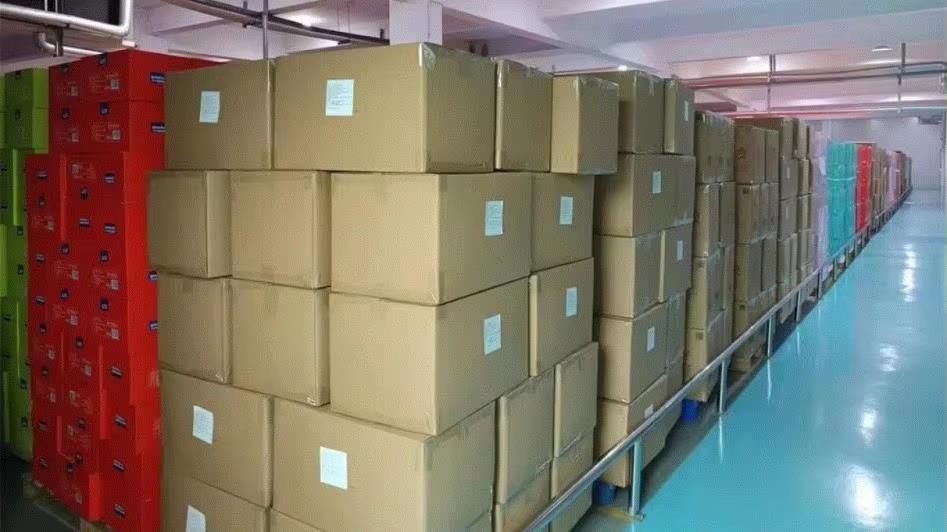
Multi-layer barrier sealing, metal detection, and X-ray foreign body inspection prior to export container loading.
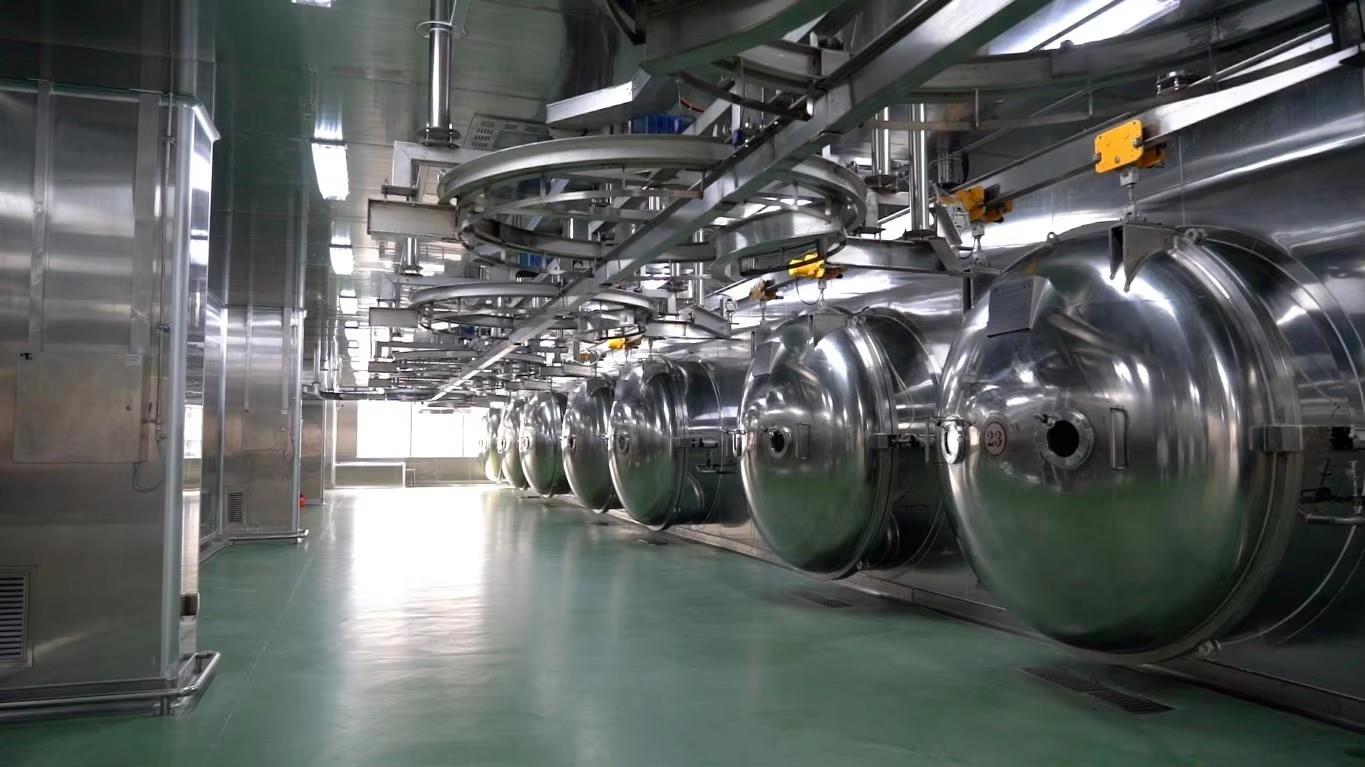
Our Zhangzhou campus operates 8,000 m² of vacuum chamber area, driving unmatched capacity and energy efficiency.
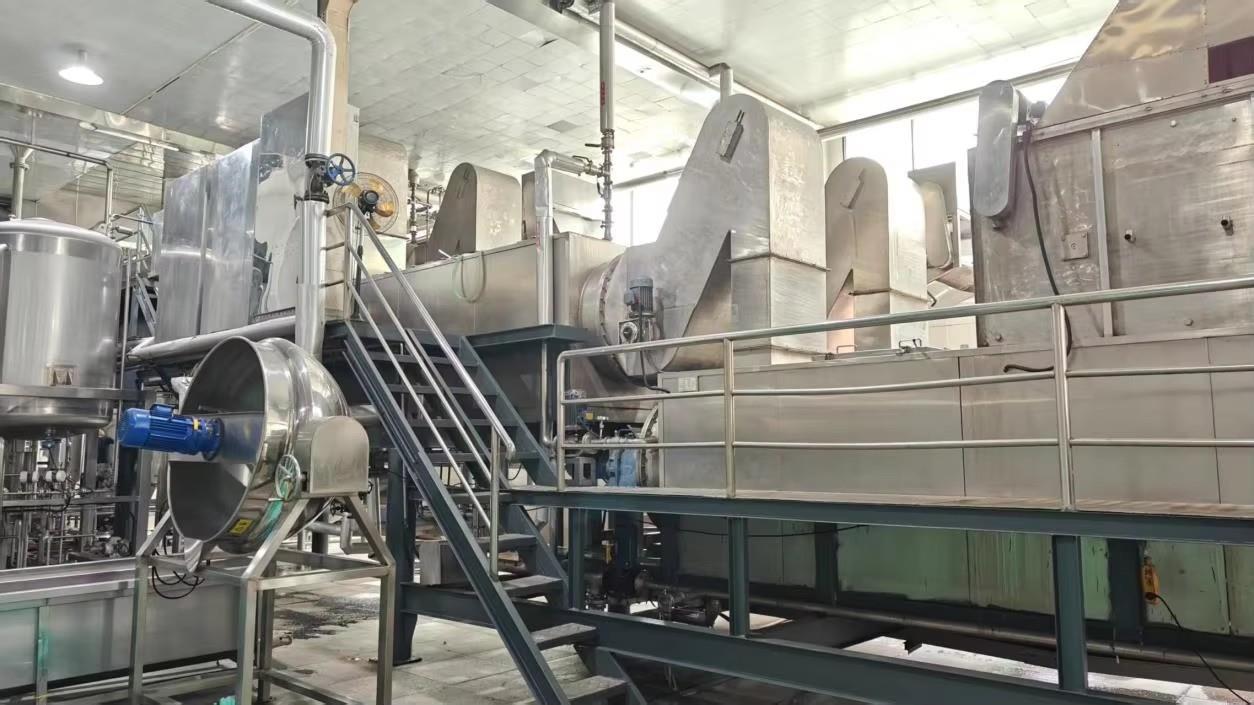
Proprietary low-temperature concentration equipment for specialized soluble vegetable powders and extract formulations.
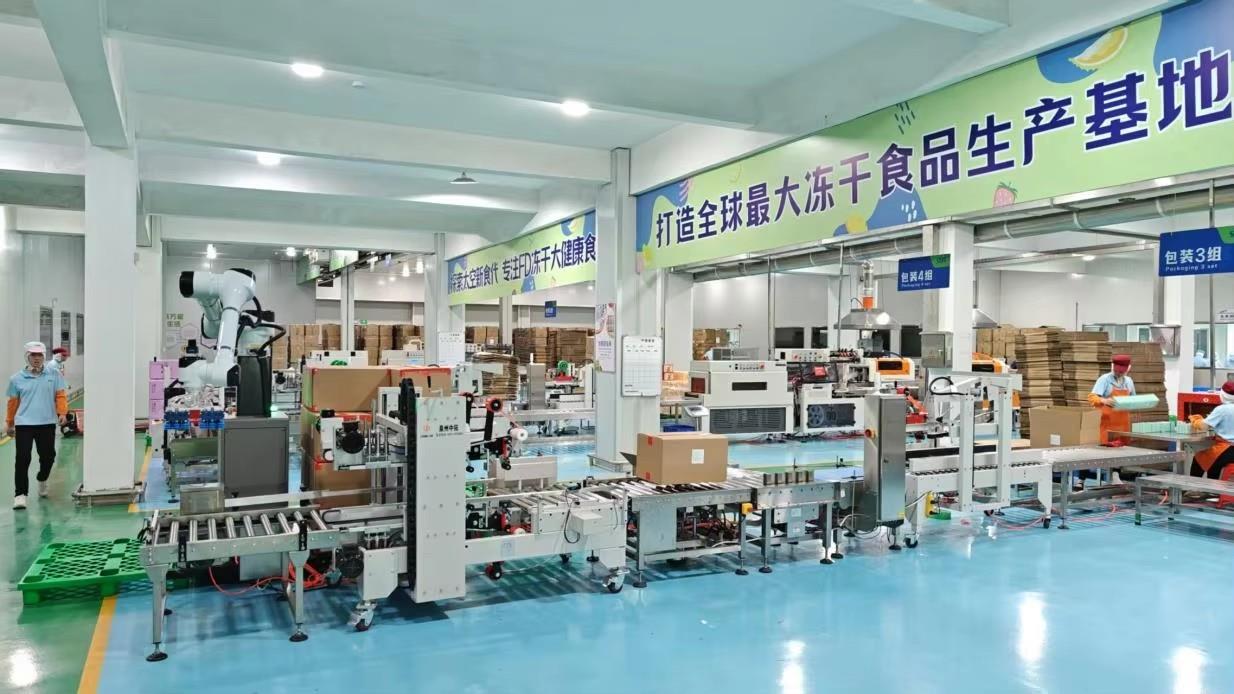
High-speed form-fill-seal machines with integrated nitrogen flushing for private-label retail pouch programs.
Every batch of freeze-dried sweet corn delivered by Fujian Fynergy Foods Co., Ltd. is evaluated in our internal testing laboratory, which is furnished with advanced diagnostic apparatus equivalent to accredited third-party inspection agencies.
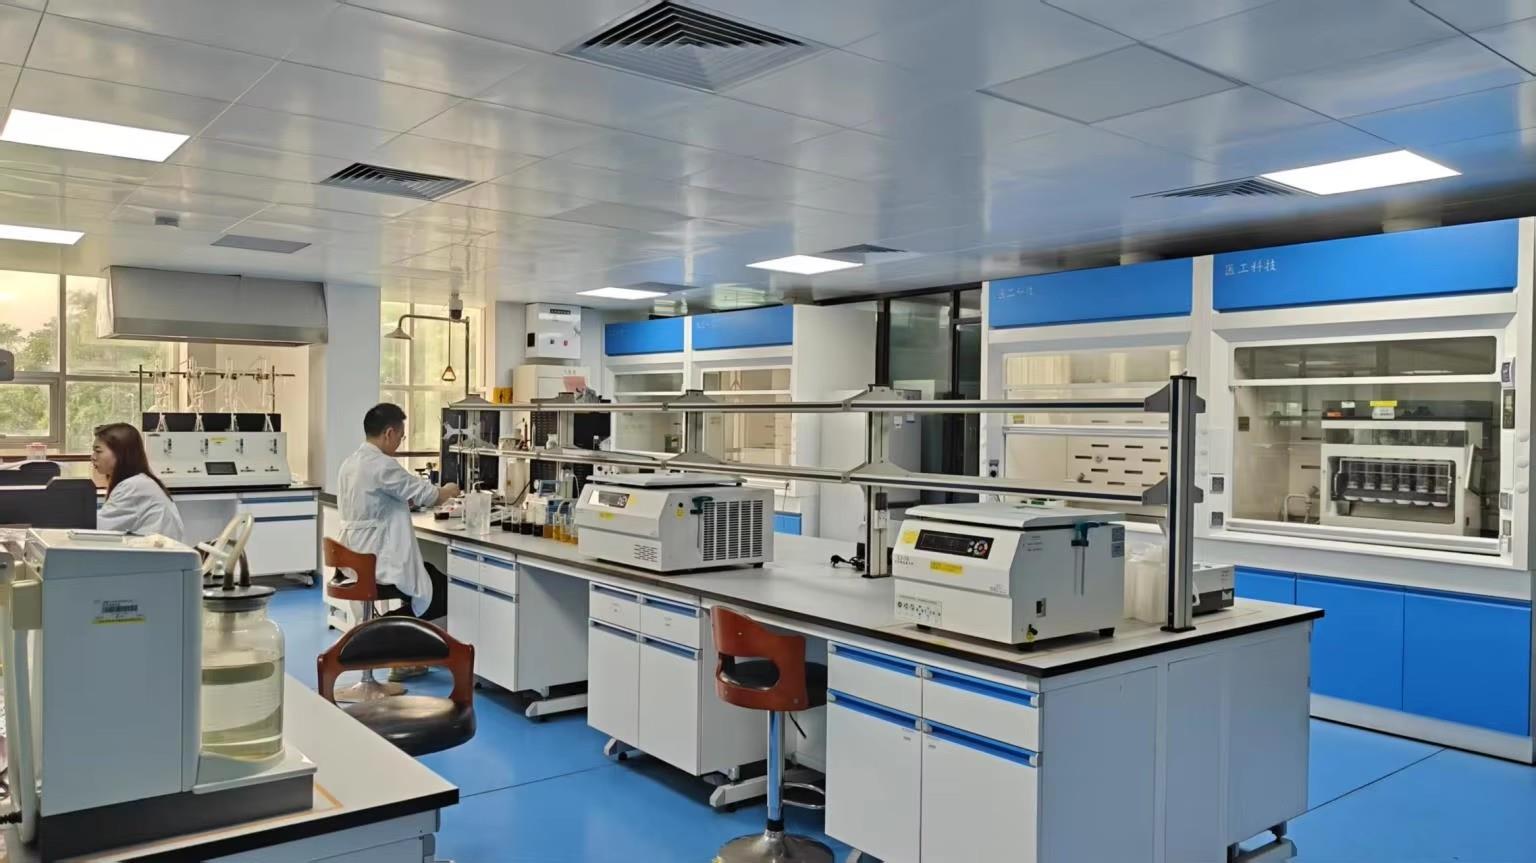
Certified microbiological and chemical assay facility enforcing strict HACCP, BRCGS, and ISO 22000 mandates.
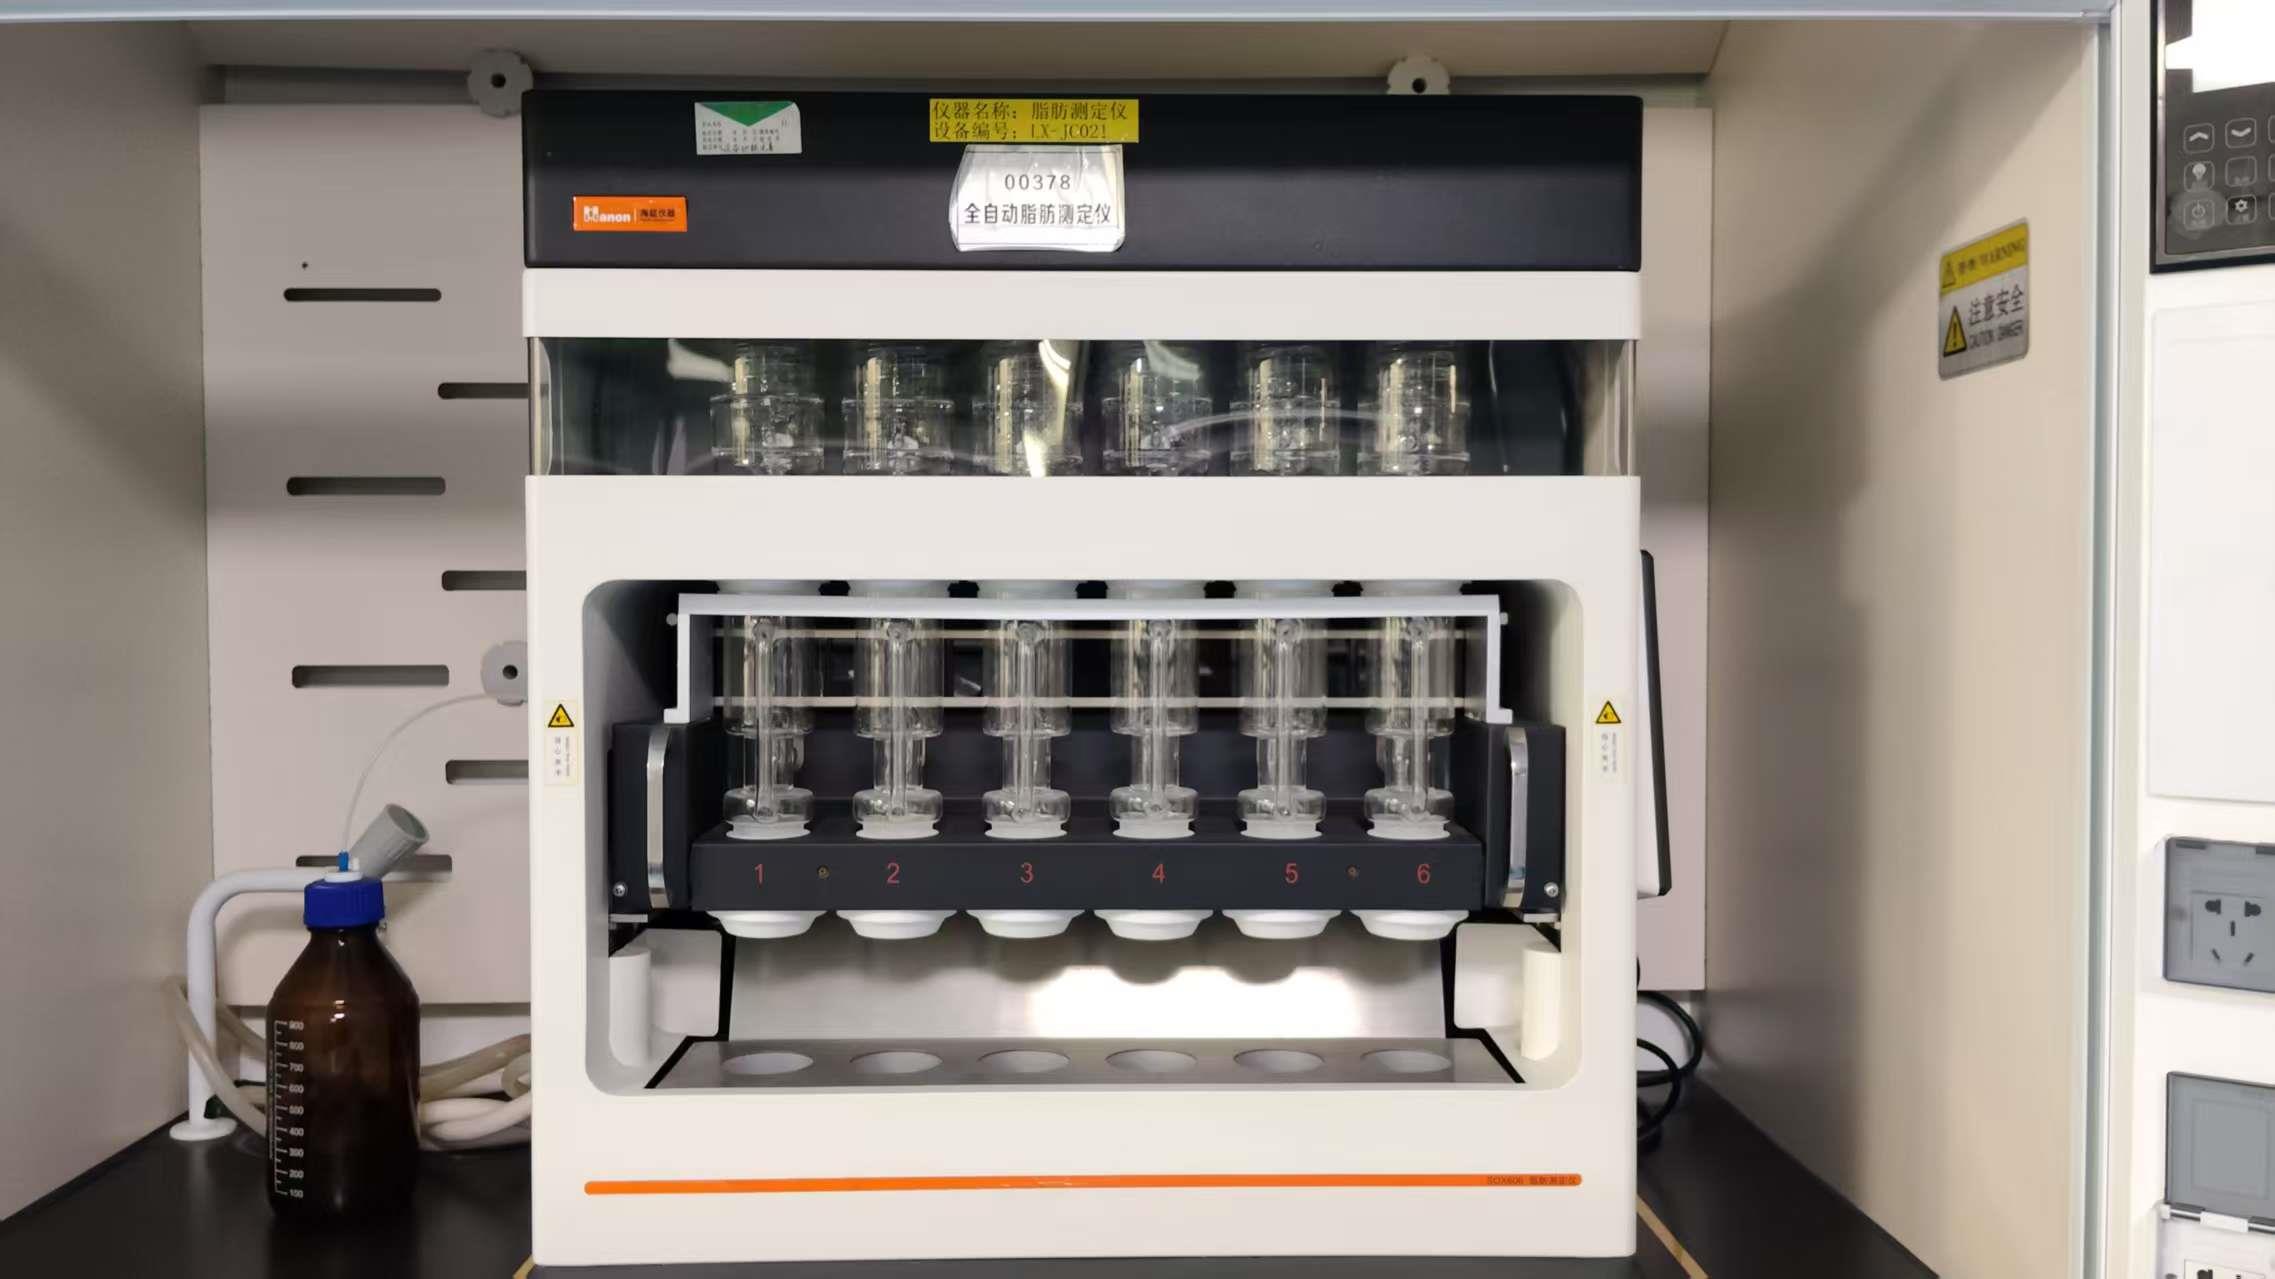
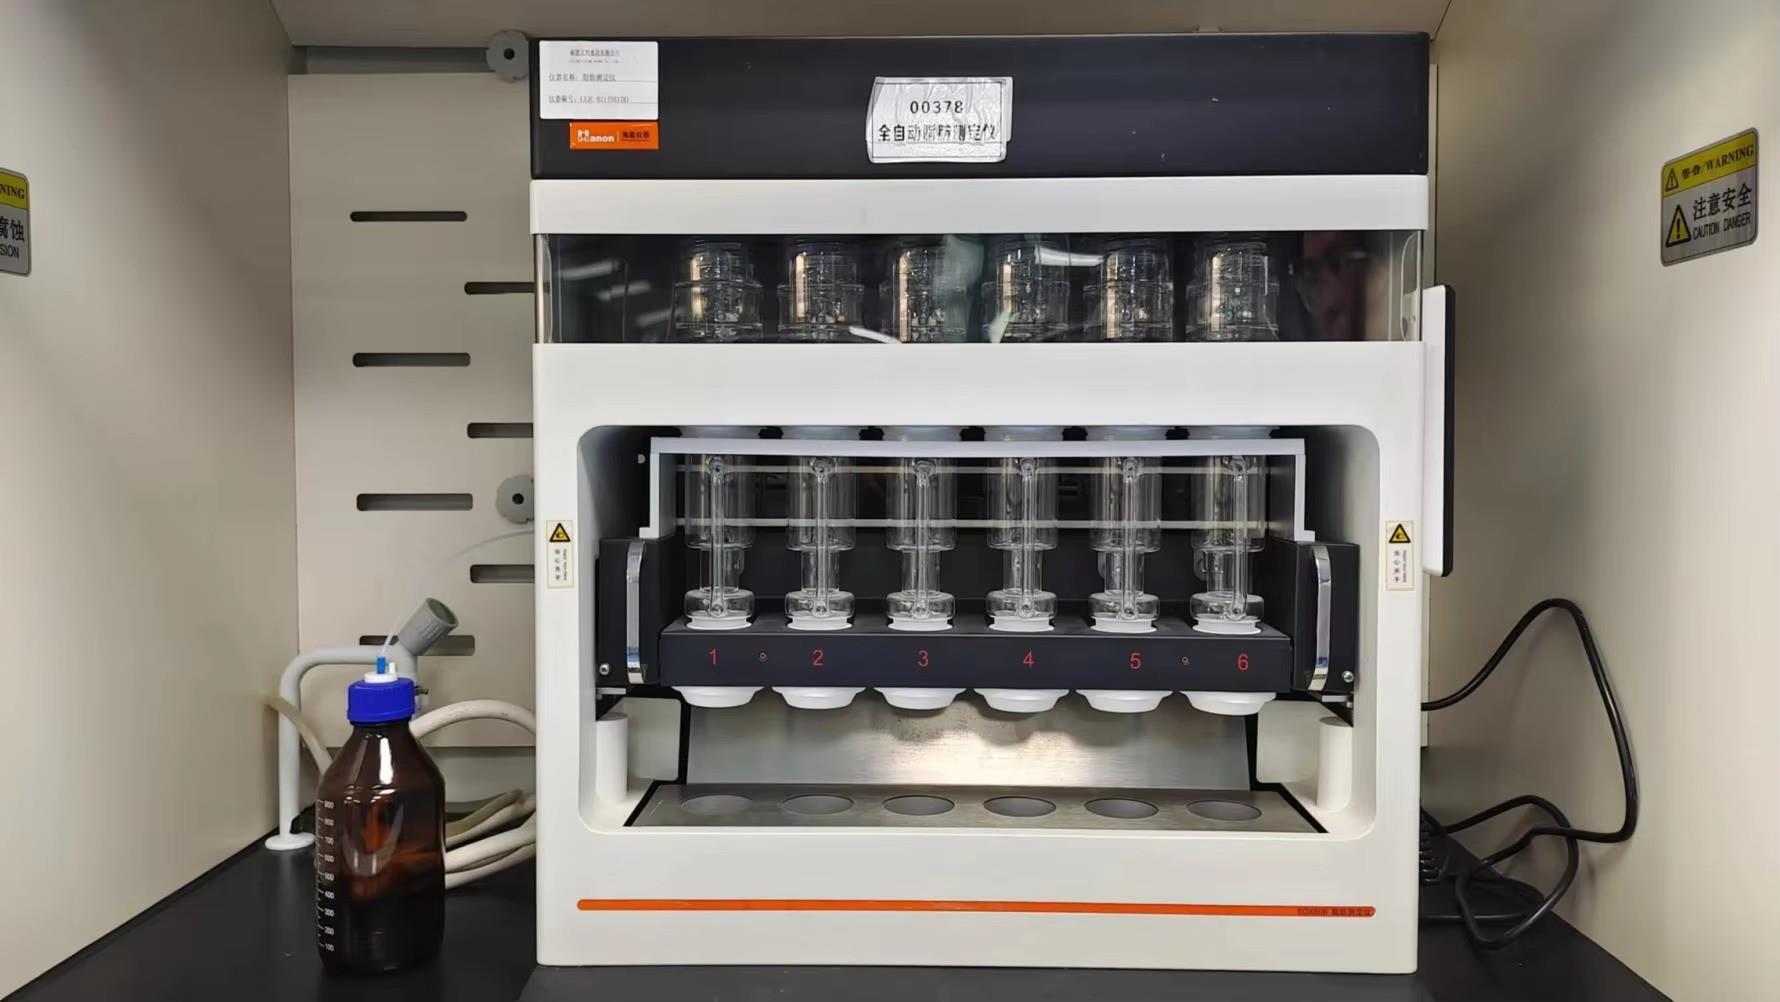
Verifies crude fat content to confirm natural non-fried status and nutritional label accuracy for international brands.
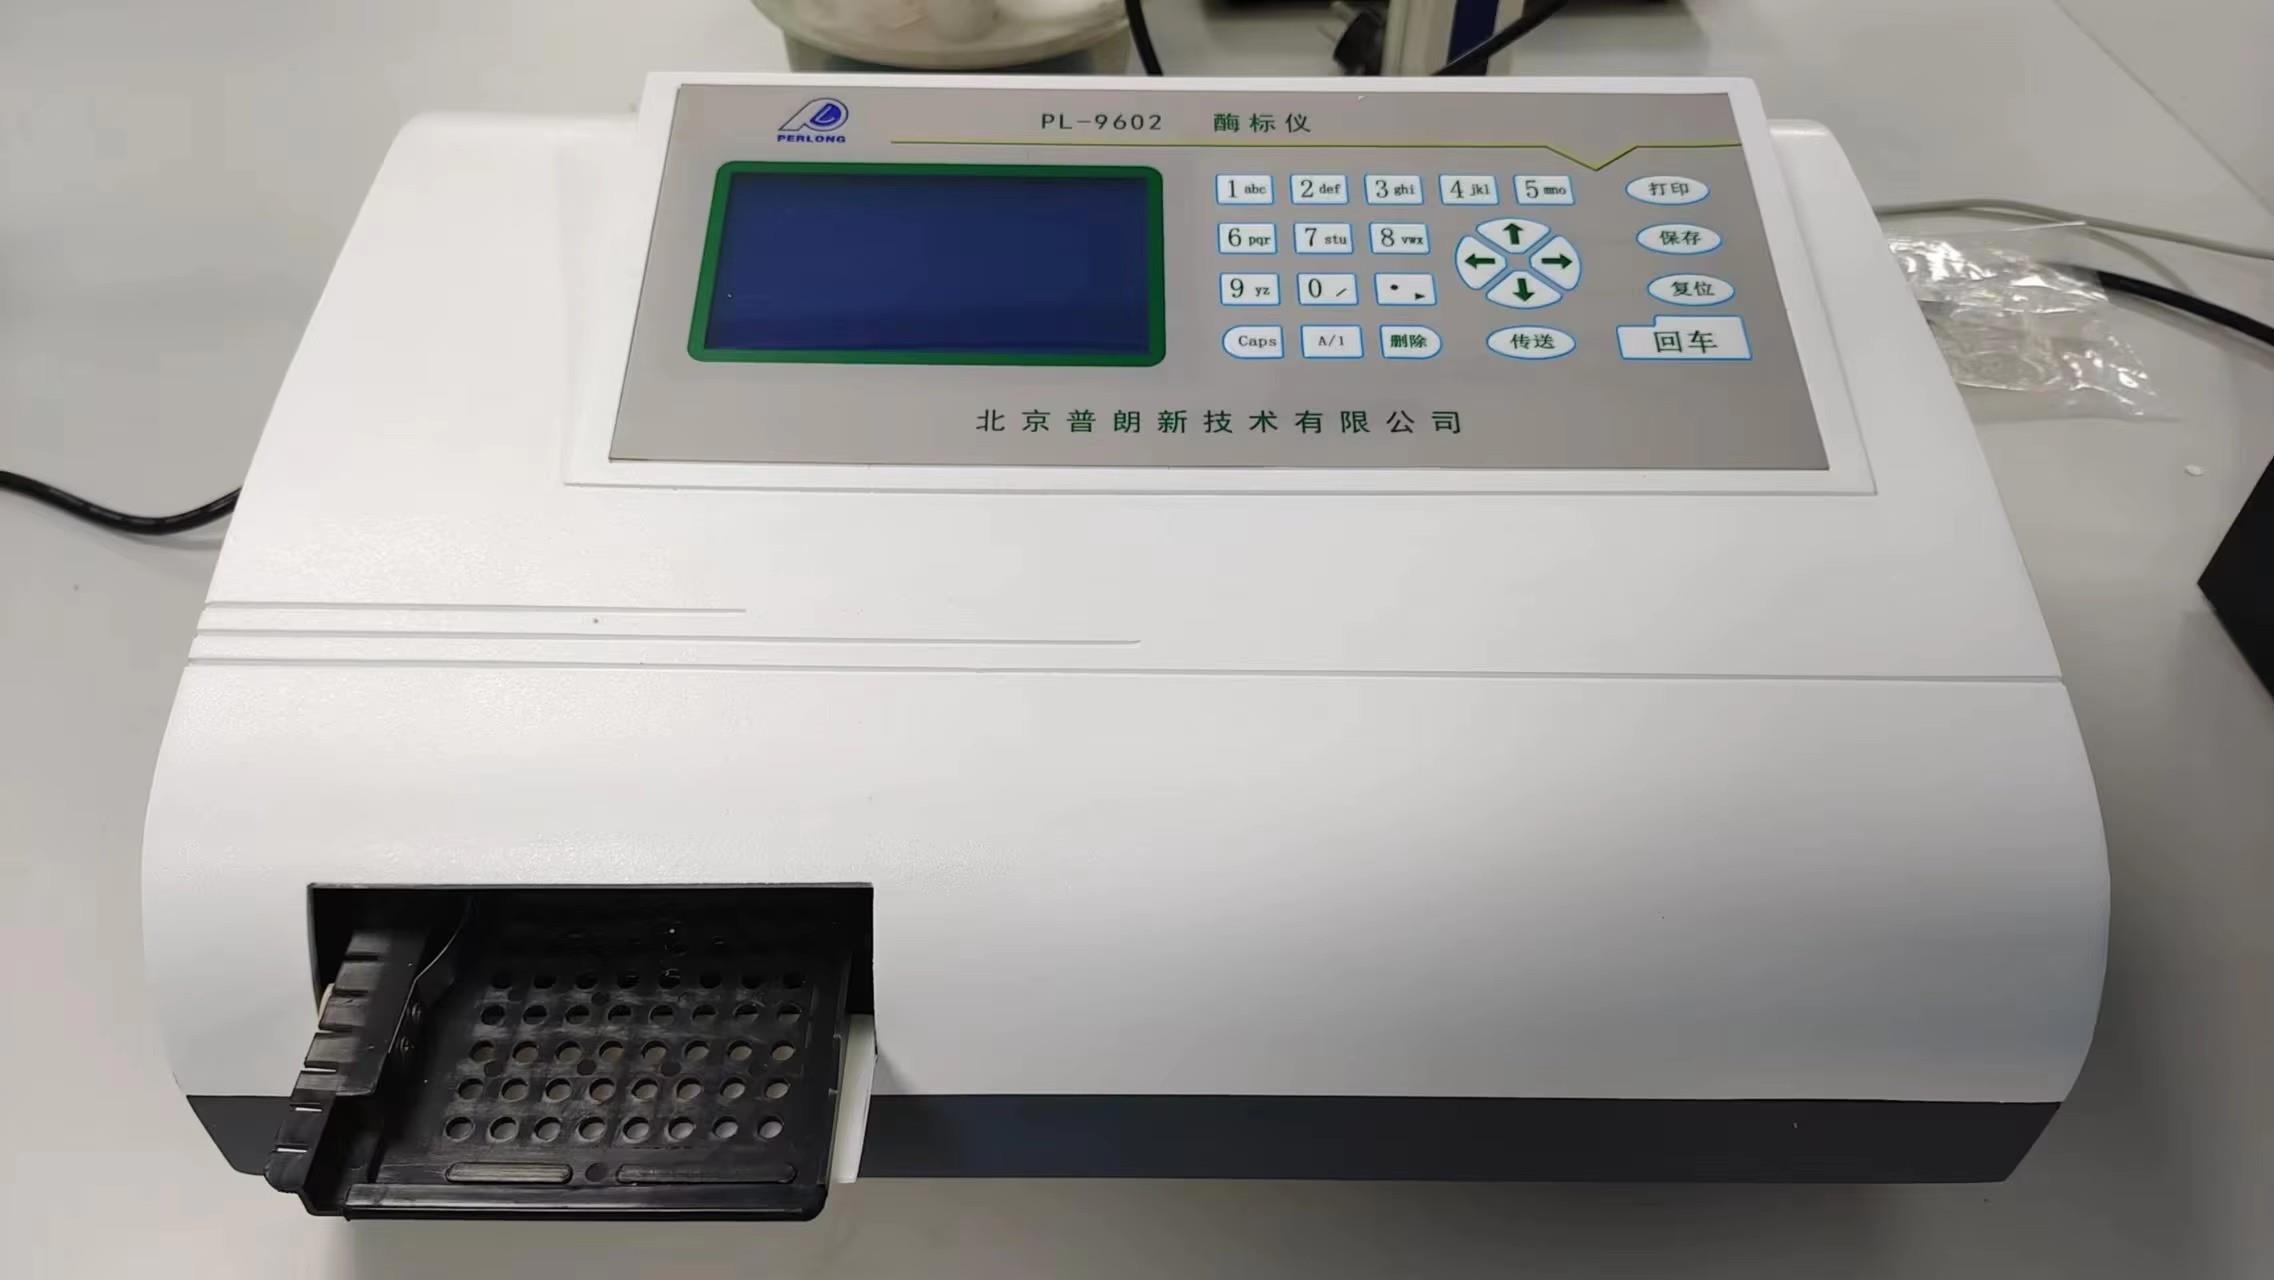
High-throughput ELISA screening for rapid pathogen, allergen, and mycotoxin detection prior to lot release.
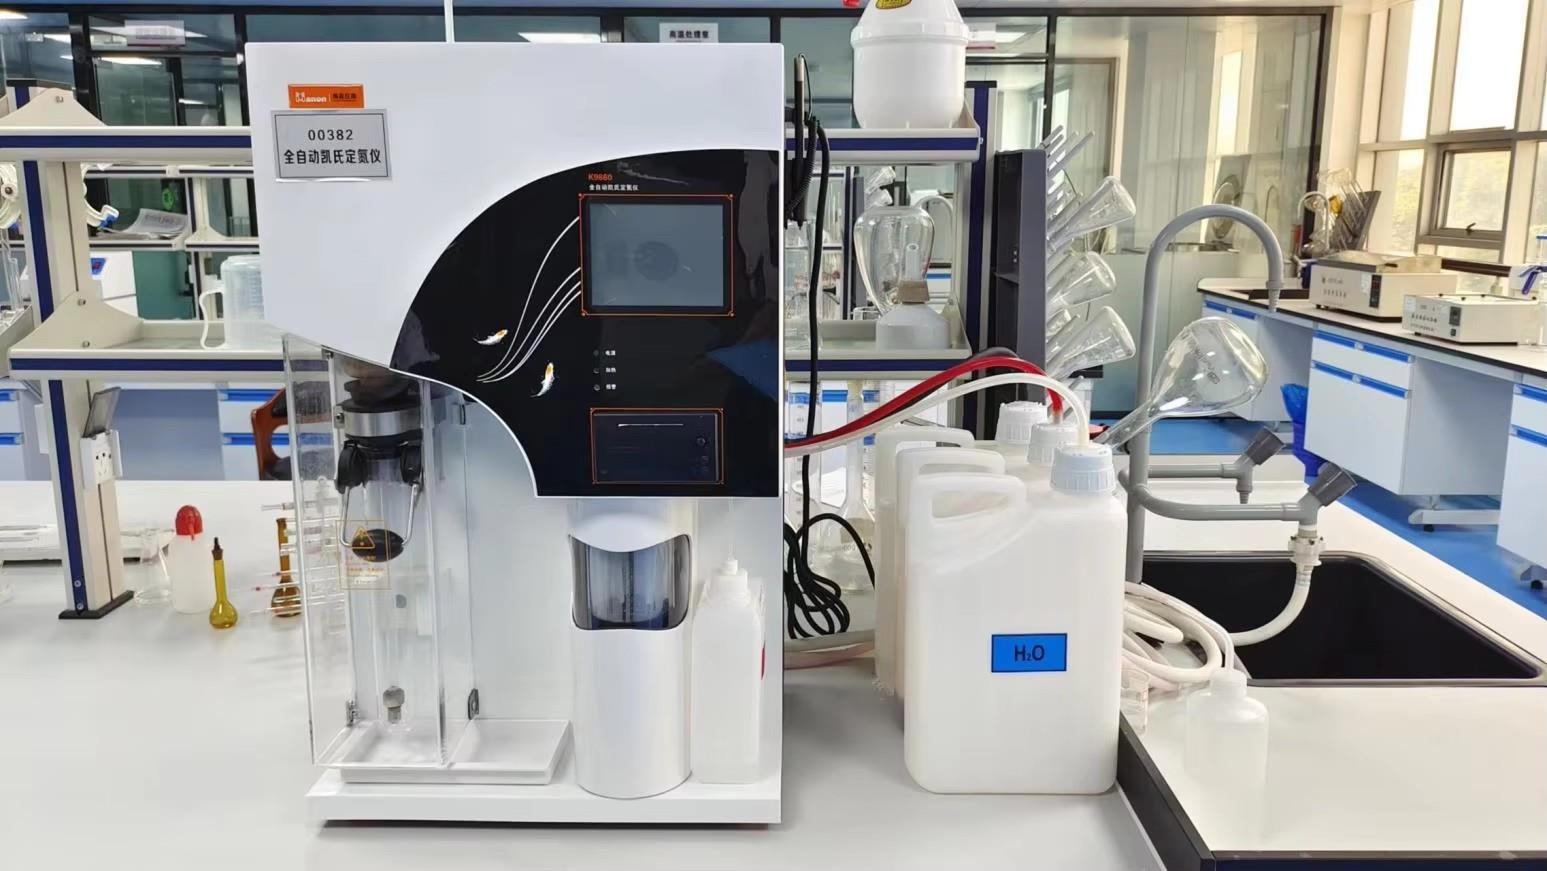
Precise nitrogen and crude protein quantification, validating nutritional integrity in sweet corn and pet food powder.
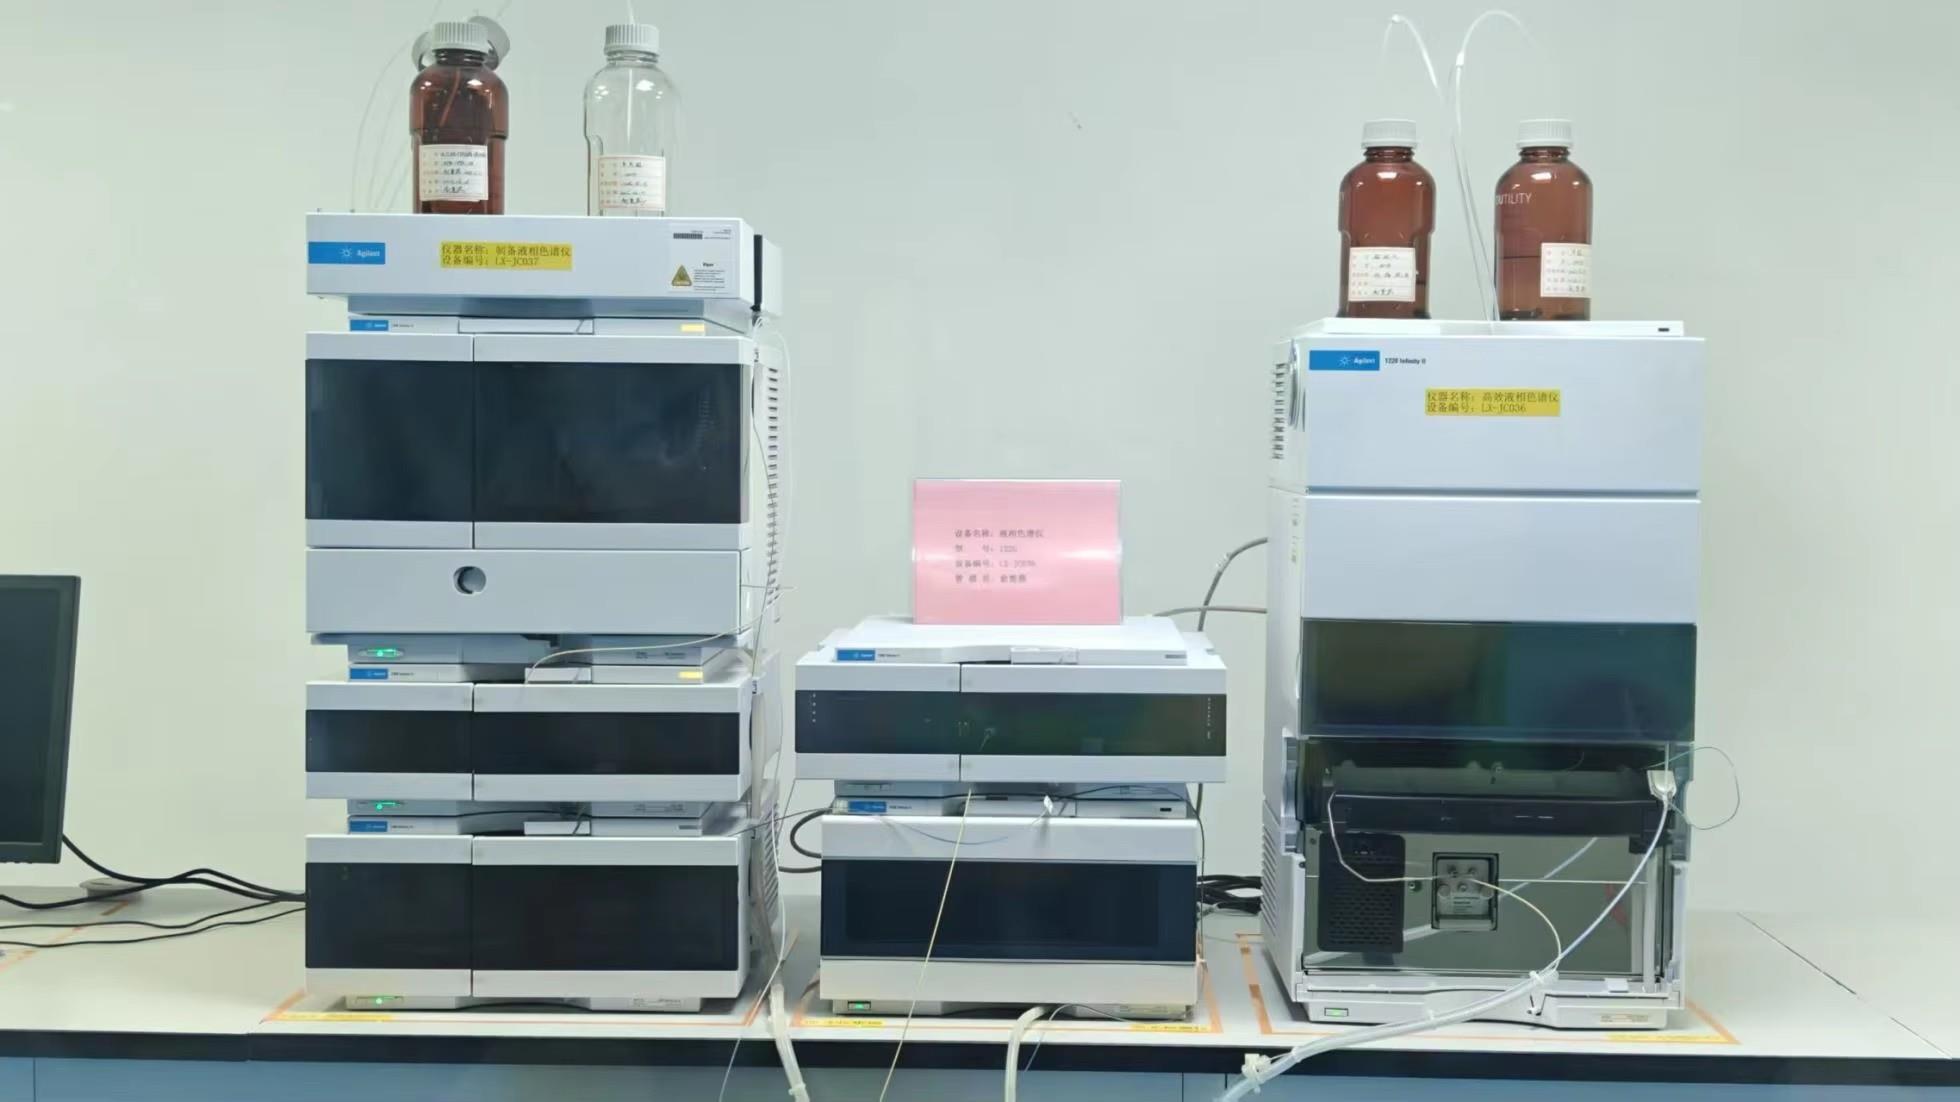
Resolves multi-spectrum pesticide residues, preservative absences, and natural vitamin profiles at sub-ppm thresholds.
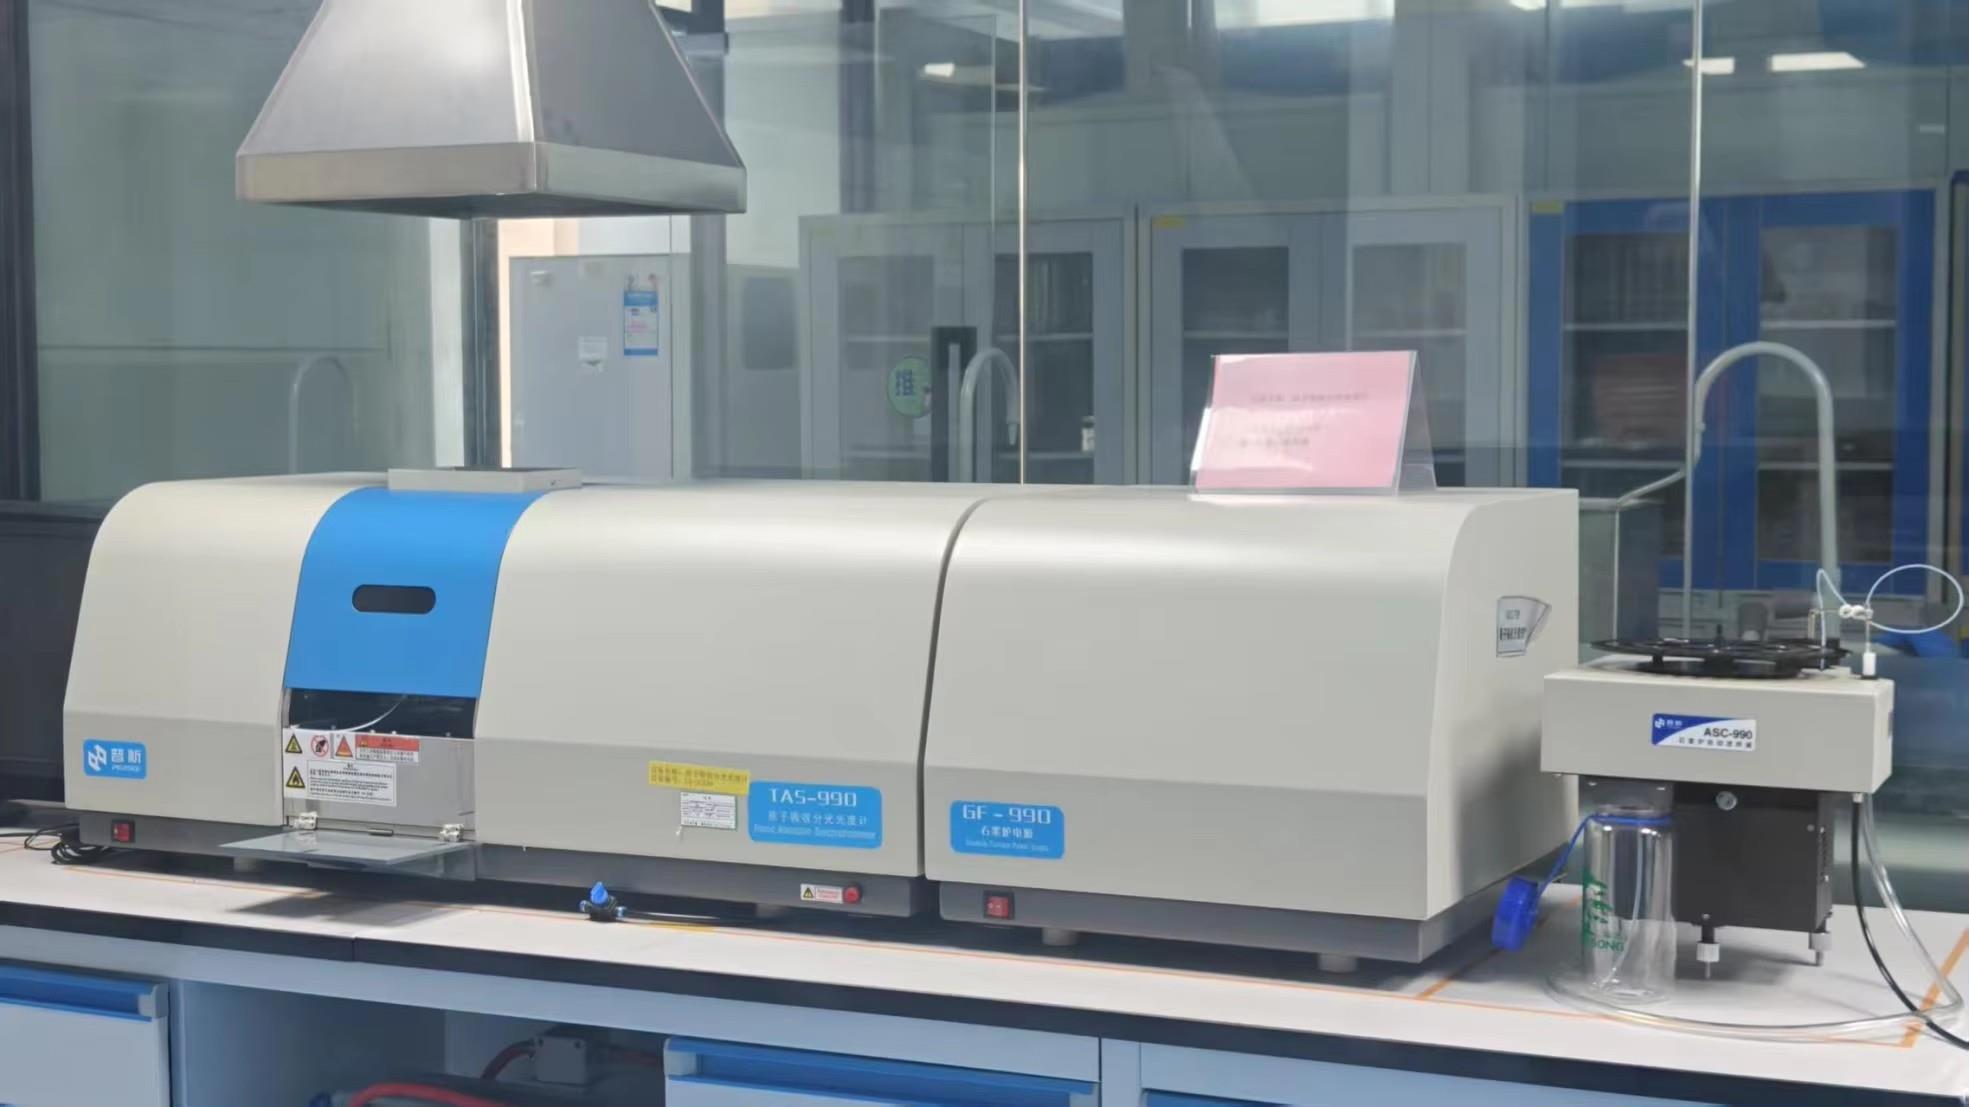
Performs trace elemental analysis for Lead (Pb) and Cadmium (Cd) to guarantee total infant-grade safety.
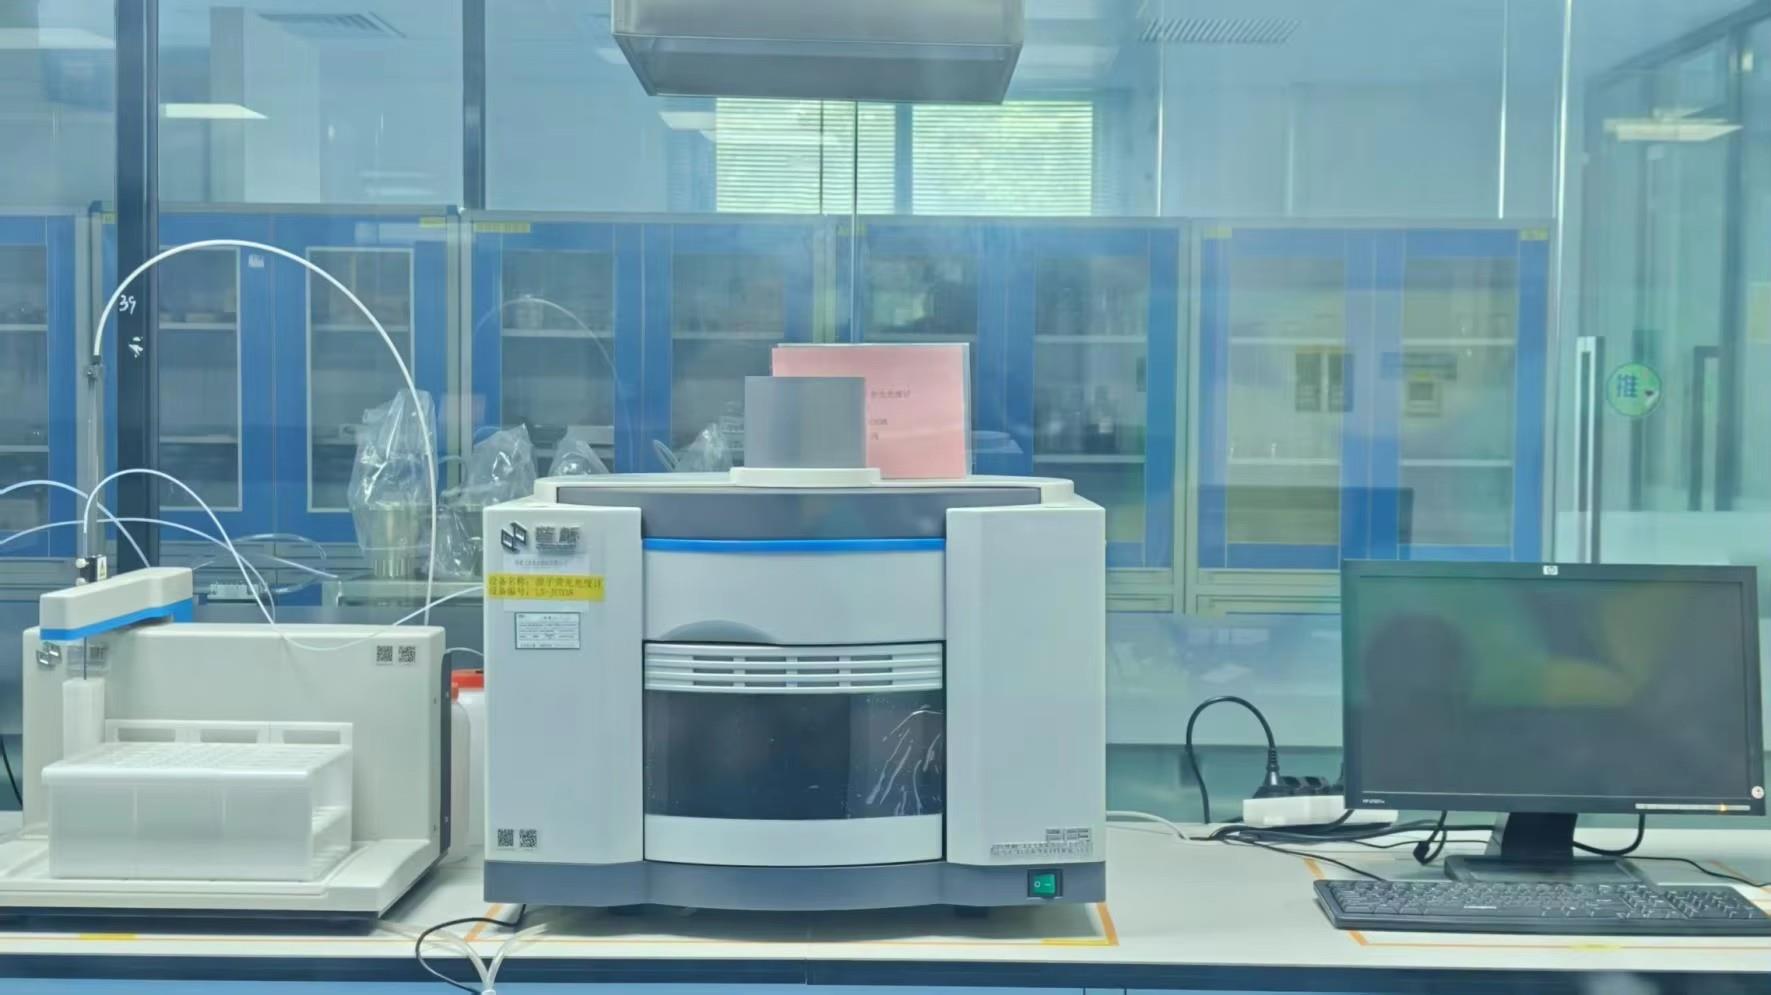
Ultrasensitive quantification of trace Arsenic (As) and Mercury (Hg), ensuring compliance with strict global food safety laws.
Comprehensive dry matter, crude ash, and water activity analysis validating consistency across high-volume production orders.
Authoritative, highly detailed answers addressing the most frequent commercial, technical, and regulatory inquiries handled by our engineering and export departments.
Air-dehydrated (AD) sweet corn is dried via heated air, causing irreversible shrinkage, tough cellular walls, starch gelatinization, and severe caramelization that yields a hard, chewy kernel requiring 15–20 minutes of boiling to soften. IQF frozen corn preserves texture but requires continuous, expensive -18°C cold chain logistics, has an 80% dead-weight water payload, and degrades rapidly upon thawing due to drip loss.
In stark contrast, Freeze-Dried Sweet Corn from Fujian Fynergy Foods Co., Ltd. eliminates water via low-temperature vacuum sublimation. The structural cell matrix remains completely open and intact, retaining the natural bright yellow color, original shape, fresh sweet flavor, and 97%+ of heat-sensitive nutrients. It can be consumed dry as a crispy, puffed snack or reconstituted into a juicy, plump kernel in warm water within 3–5 minutes. Furthermore, it is completely shelf-stable at room temperature for up to 24 months, slashing global transportation and storage expenditures.
For standard bulk industrial packaging (10 kg net weight packed in double food-grade polyethylene lined corrugated cartons), our standard starting MOQ is 500 kg. For customized particle cuts, micro-milled corn powders, or trial market launches, we can accommodate pilot runs starting from 100 kg to 300 kg upon technical review.
For fully printed retail private-label packaging (custom nitrogen-flushed stand-up pouches, canister tubes, or retail boxes), the MOQ typically ranges between 10,000 and 30,000 units, dictated primarily by rotogravure cylinder printing tolerances. Standard production lead time for bulk ingredients is approximately 15 to 20 working days following sample and deposit confirmation.
Fujian Fynergy Foods Co., Ltd. enforces a seed-to-factory vertical quality assurance framework. All fresh sweet corn raw materials originate strictly from contracted agricultural cooperatives cultivating certified non-GMO supersweet seed varieties. We conduct regular PCR testing for genetic markers (such as CaMV 35S promoter and NOS terminator) to confirm 100% non-GMO status.
Before harvest and upon delivery to our Zhangzhou facility, raw lots undergo multi-residue pesticide screening in our in-house liquid chromatography (HPLC/GC-MS) laboratory. Our analytical testing protocols adhere fully to strict European Commission Regulation (EC) No 396/2005, US FDA Code of Federal Regulations Title 21, and the Japanese Positive List System for agricultural chemicals.
Because freeze-dried sweet corn possesses an exceptionally low moisture profile (≤ 3.0%) and water activity (aw ≤ 0.25), it is inherently hygroscopic and will rapidly absorb ambient moisture if exposed to air, leading to loss of crispness.
Bulk cartons should be stored in a cool, clean, dry warehouse at temperatures below 25°C and relative humidity (RH) below 50%, elevated off concrete floors on clean pallets. Once an inner liner is unsealed for production sampling or repacking, it must be resealed immediately under dry atmospheric conditions or flushed with food-grade nitrogen gas. Under intact original barrier packaging, our freeze-dried sweet corn carries an audited shelf life of 18 to 24 months.
Yes. As an onsite-verified custom manufacturer, our engineering team regularly supports specialized formulation needs. Beyond our whole kernel Grade A line, we produce:
Our production facility in Zhangzhou, Fujian is comprehensively certified under the highest global benchmark standards:
Complete audit summaries, COA certificates of analysis, allergen statements, non-GMO declarations, and nutritional specification sheets are supplied to our clients' QA departments upon request.