01
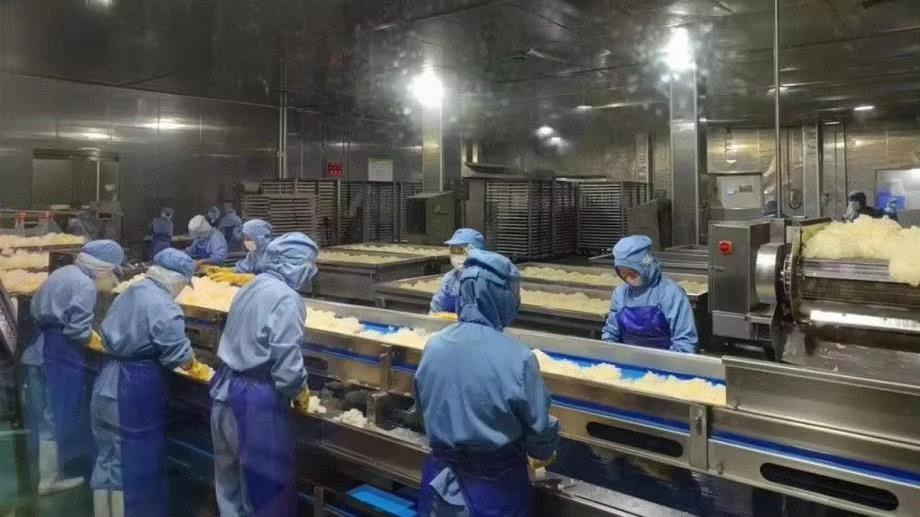
Raw Material Cleaning
Multi-stage water washing, bubble immersion, and surface cleaning remove natural residues while preserving fresh raw material integrity.
Fujian Fynergy Foods Co., Ltd. — Certified Custom Freeze-Dried Food Manufacturer
Fujian Fynergy Foods Co., Ltd. is a leading industrial-scale freeze-dried food manufacturer based in Zhangzhou, Fujian Province, China. Established with over two decades of dedicated food science and preservation expertise, we operate a 62,718 m² specialized facility featuring 37 vacuum freeze-drying lines and an 8,000 m² drying chamber area.
As an onsite-inspected Custom Manufacturer audited by TÜV Rheinland, we provide complete supply chain solutions for international food brand owners, major retail supermarket chains, bulk ingredient distributors, and Fortune 500 partners. Our integrated operations span raw material sourcing, automated processing, customized formula blending, vacuum sublimation drying, and high-barrier cleanroom packaging.
Verified procurement rating outperforming industry category averages by 4.9% across North American, European, and Asian retail contracts.
Demonstrated 100% contract fulfillment reliability, backed by international Trade Assurance and batch traceability records.
Sustained commercial relationships with brand distributors, leading private labels, and industrial food formulators globally.
From initial inspection of fresh harvests to automated high-barrier packaging, every stage is monitored under Class-100,000 cleanroom standards to prevent moisture re-absorption and guarantee shelf stability.
Multi-stage water washing, bubble immersion, and surface cleaning remove natural residues while preserving fresh raw material integrity.
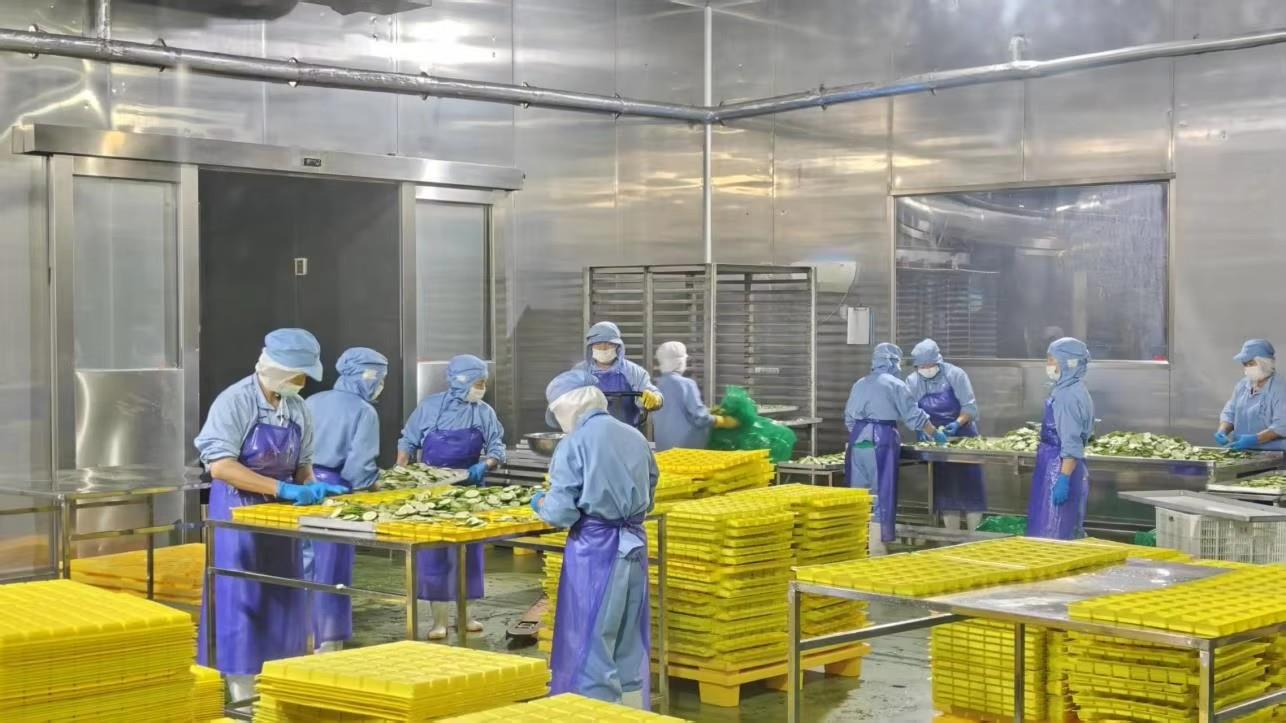
Uniform slicing, dicing, or whole sorting evenly distributed onto food-grade stainless steel trays to achieve balanced thermal transfer.
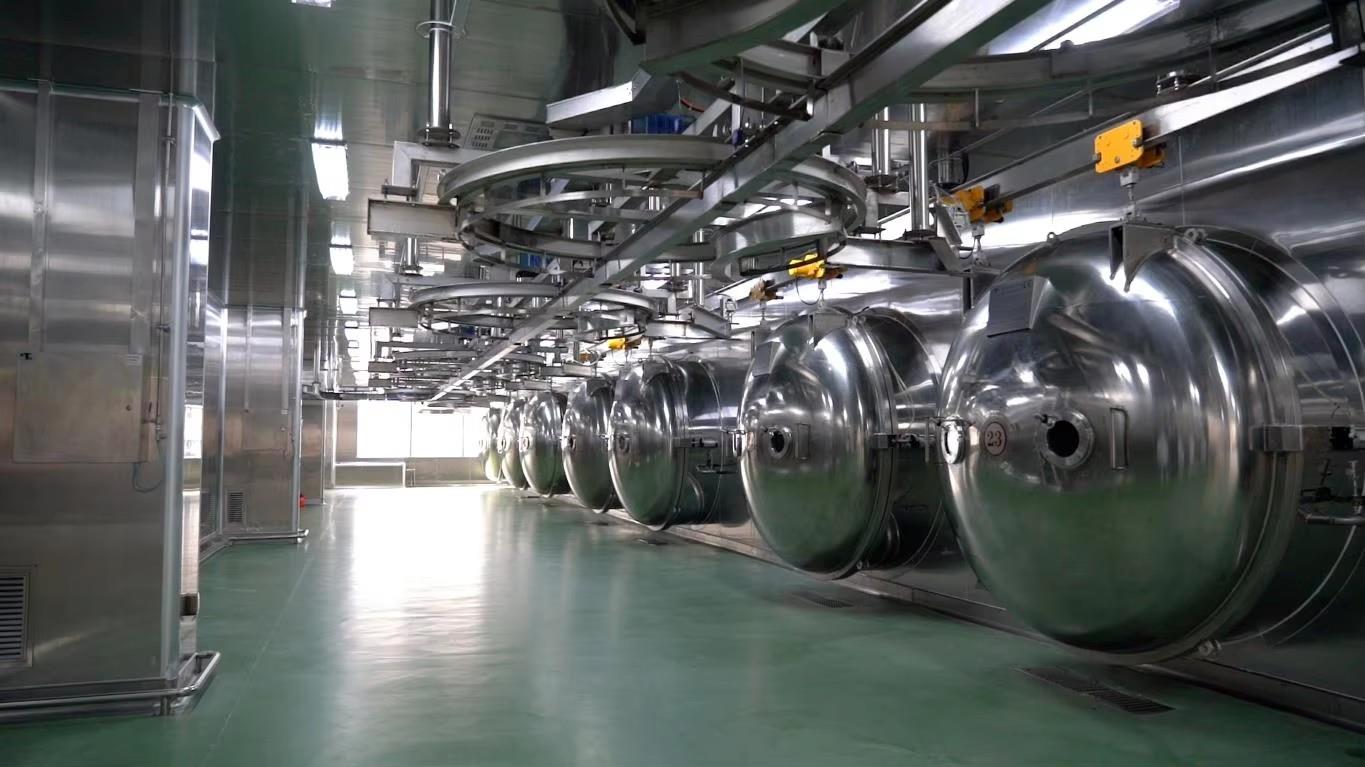
Sublimation under low temperatures and deep vacuum preserves natural colors, delicate cell structures, aromas, and heat-labile vitamins.
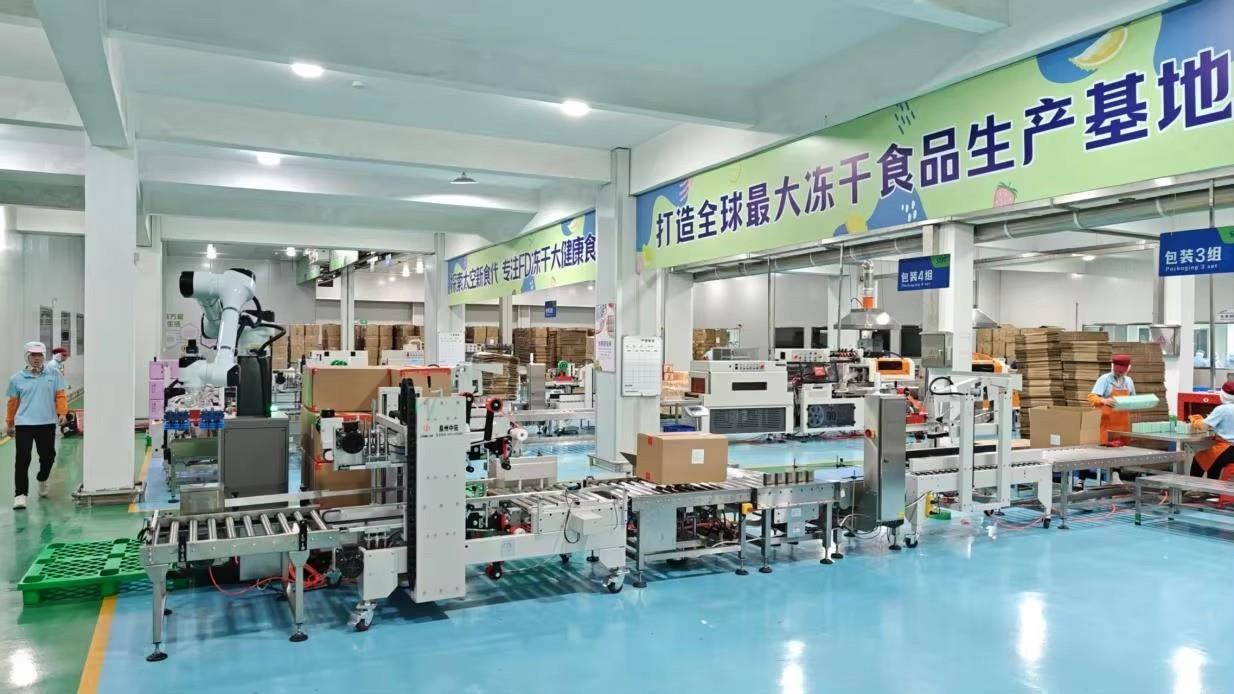
Immediate climate-controlled filling, nitrogen flushing, and heat sealing protect moisture-sensitive products from ambient humidity.
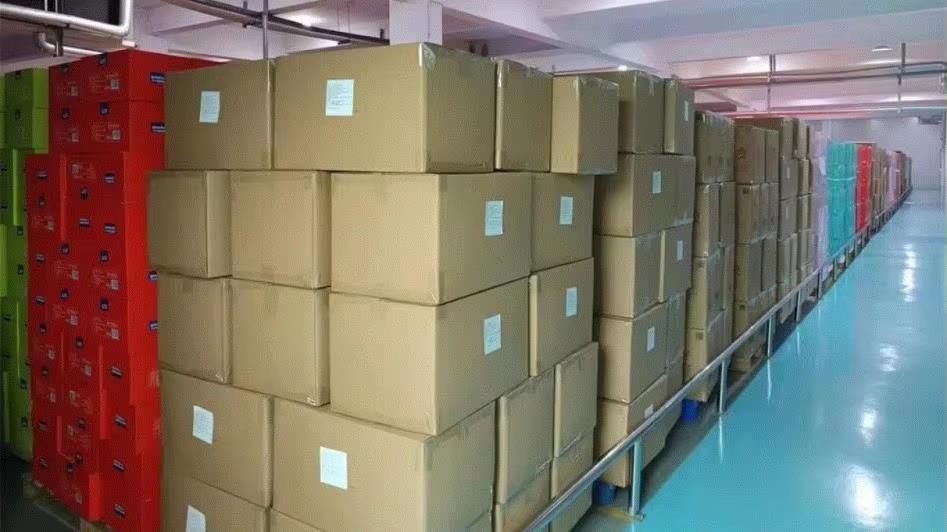
Comprehensive packaging versatility: bulk foil-lined master cartons, stand-up zipper pouches, plastic canisters, single-serve sachets, and cups.
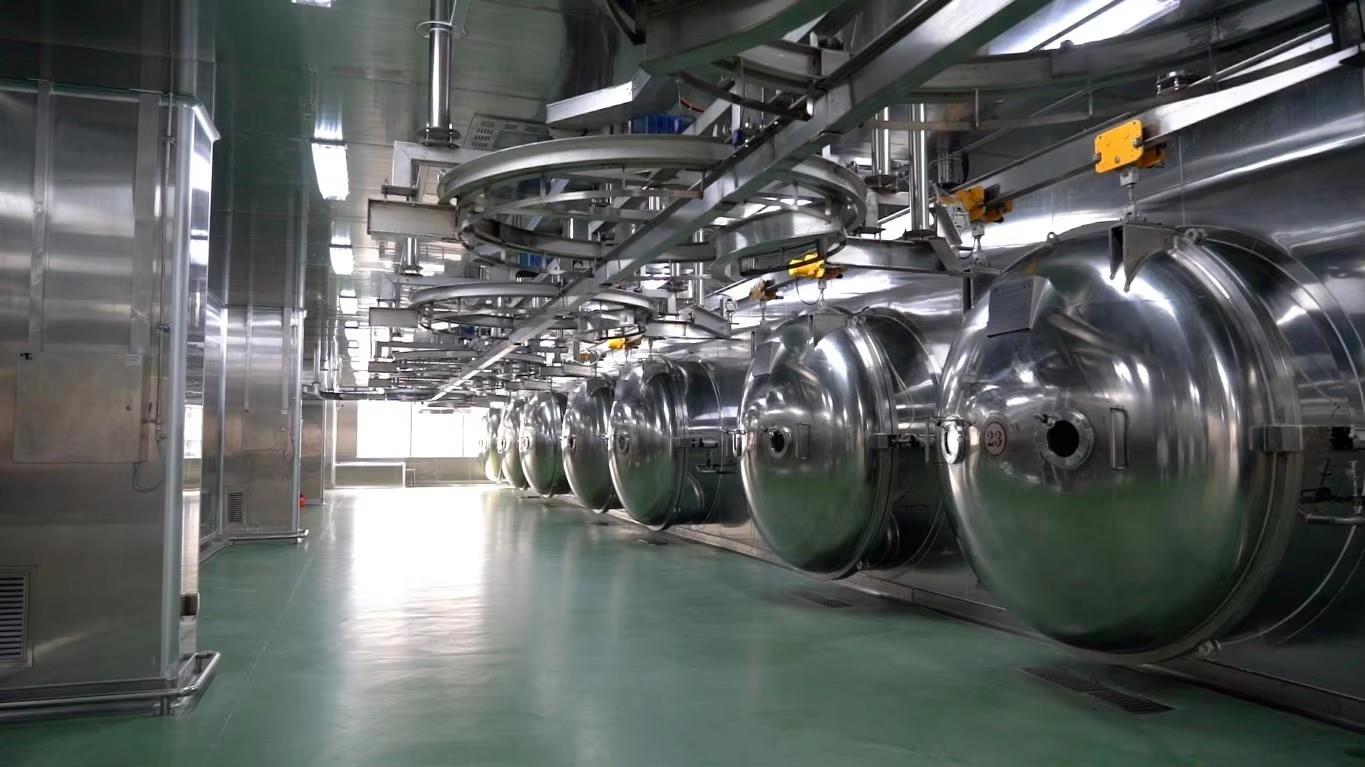
37 heavy-duty vacuum chambers equipped with computerized temperature curve regulation for tight residual moisture control (≤3% – 5%).
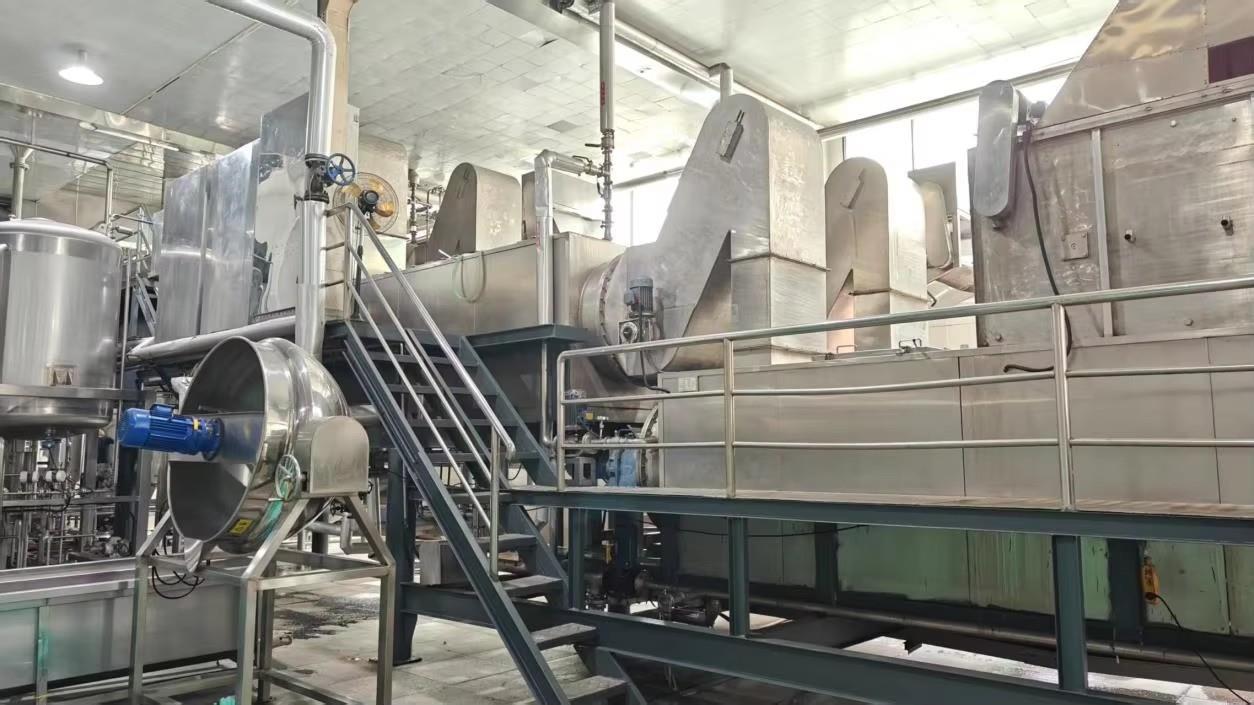
Dedicated processing systems engineered for instant tea essences, functional botanical concentrates, and high-solubility plant extracts.
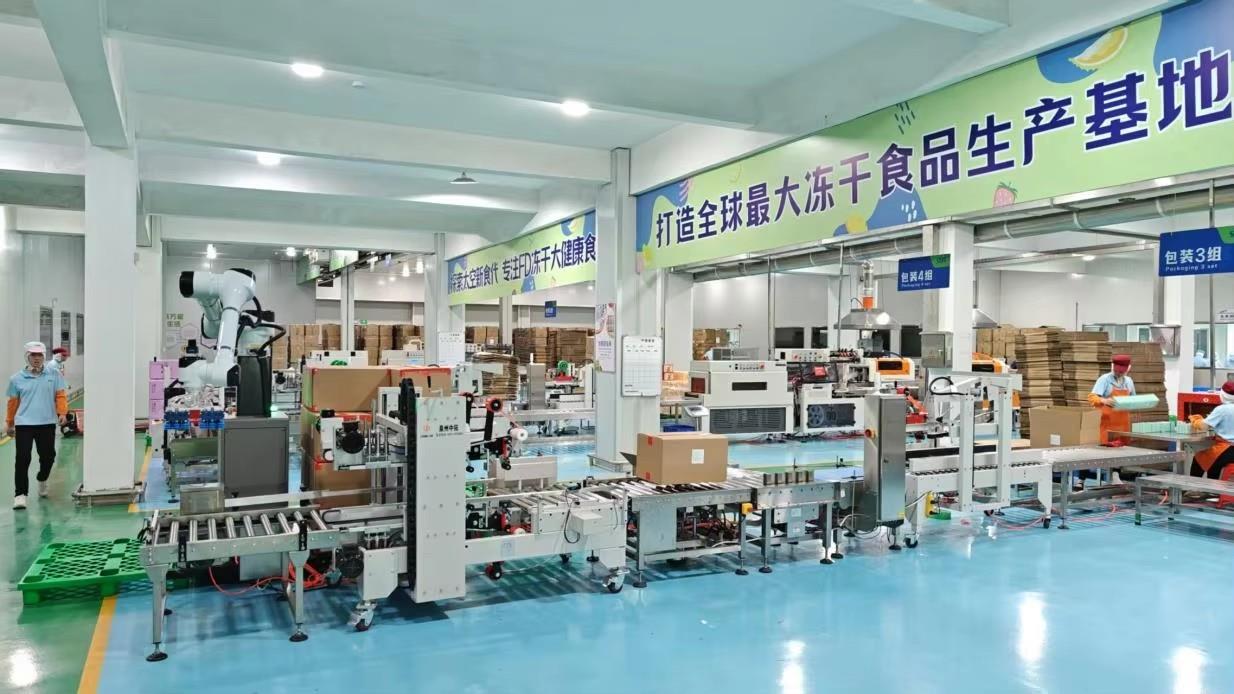
High-speed automated pouch bagging, inline multi-head weighers, metal detection, and checkweighers guarantee exact weights and zero foreign bodies.
Quality assurance is anchored by 18 full-time QA/QC inspectors and an analytical testing laboratory equipped with high-precision testing instruments to ensure full international compliance before dispatch.
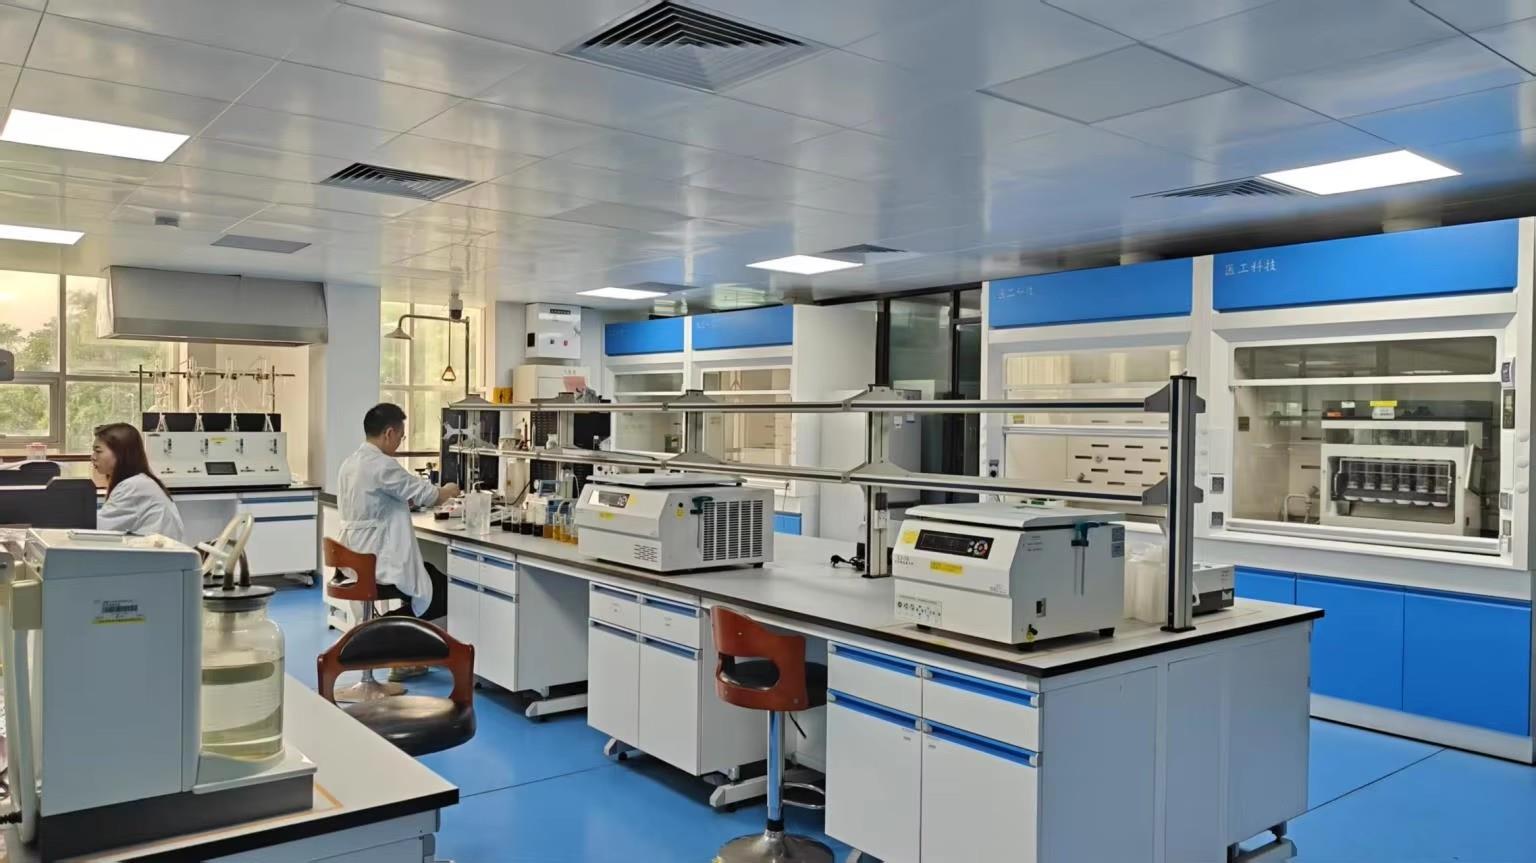
Standardized chemical, physical, and microbiological workstations performing batch-by-batch sensory, moisture, and micro assays.
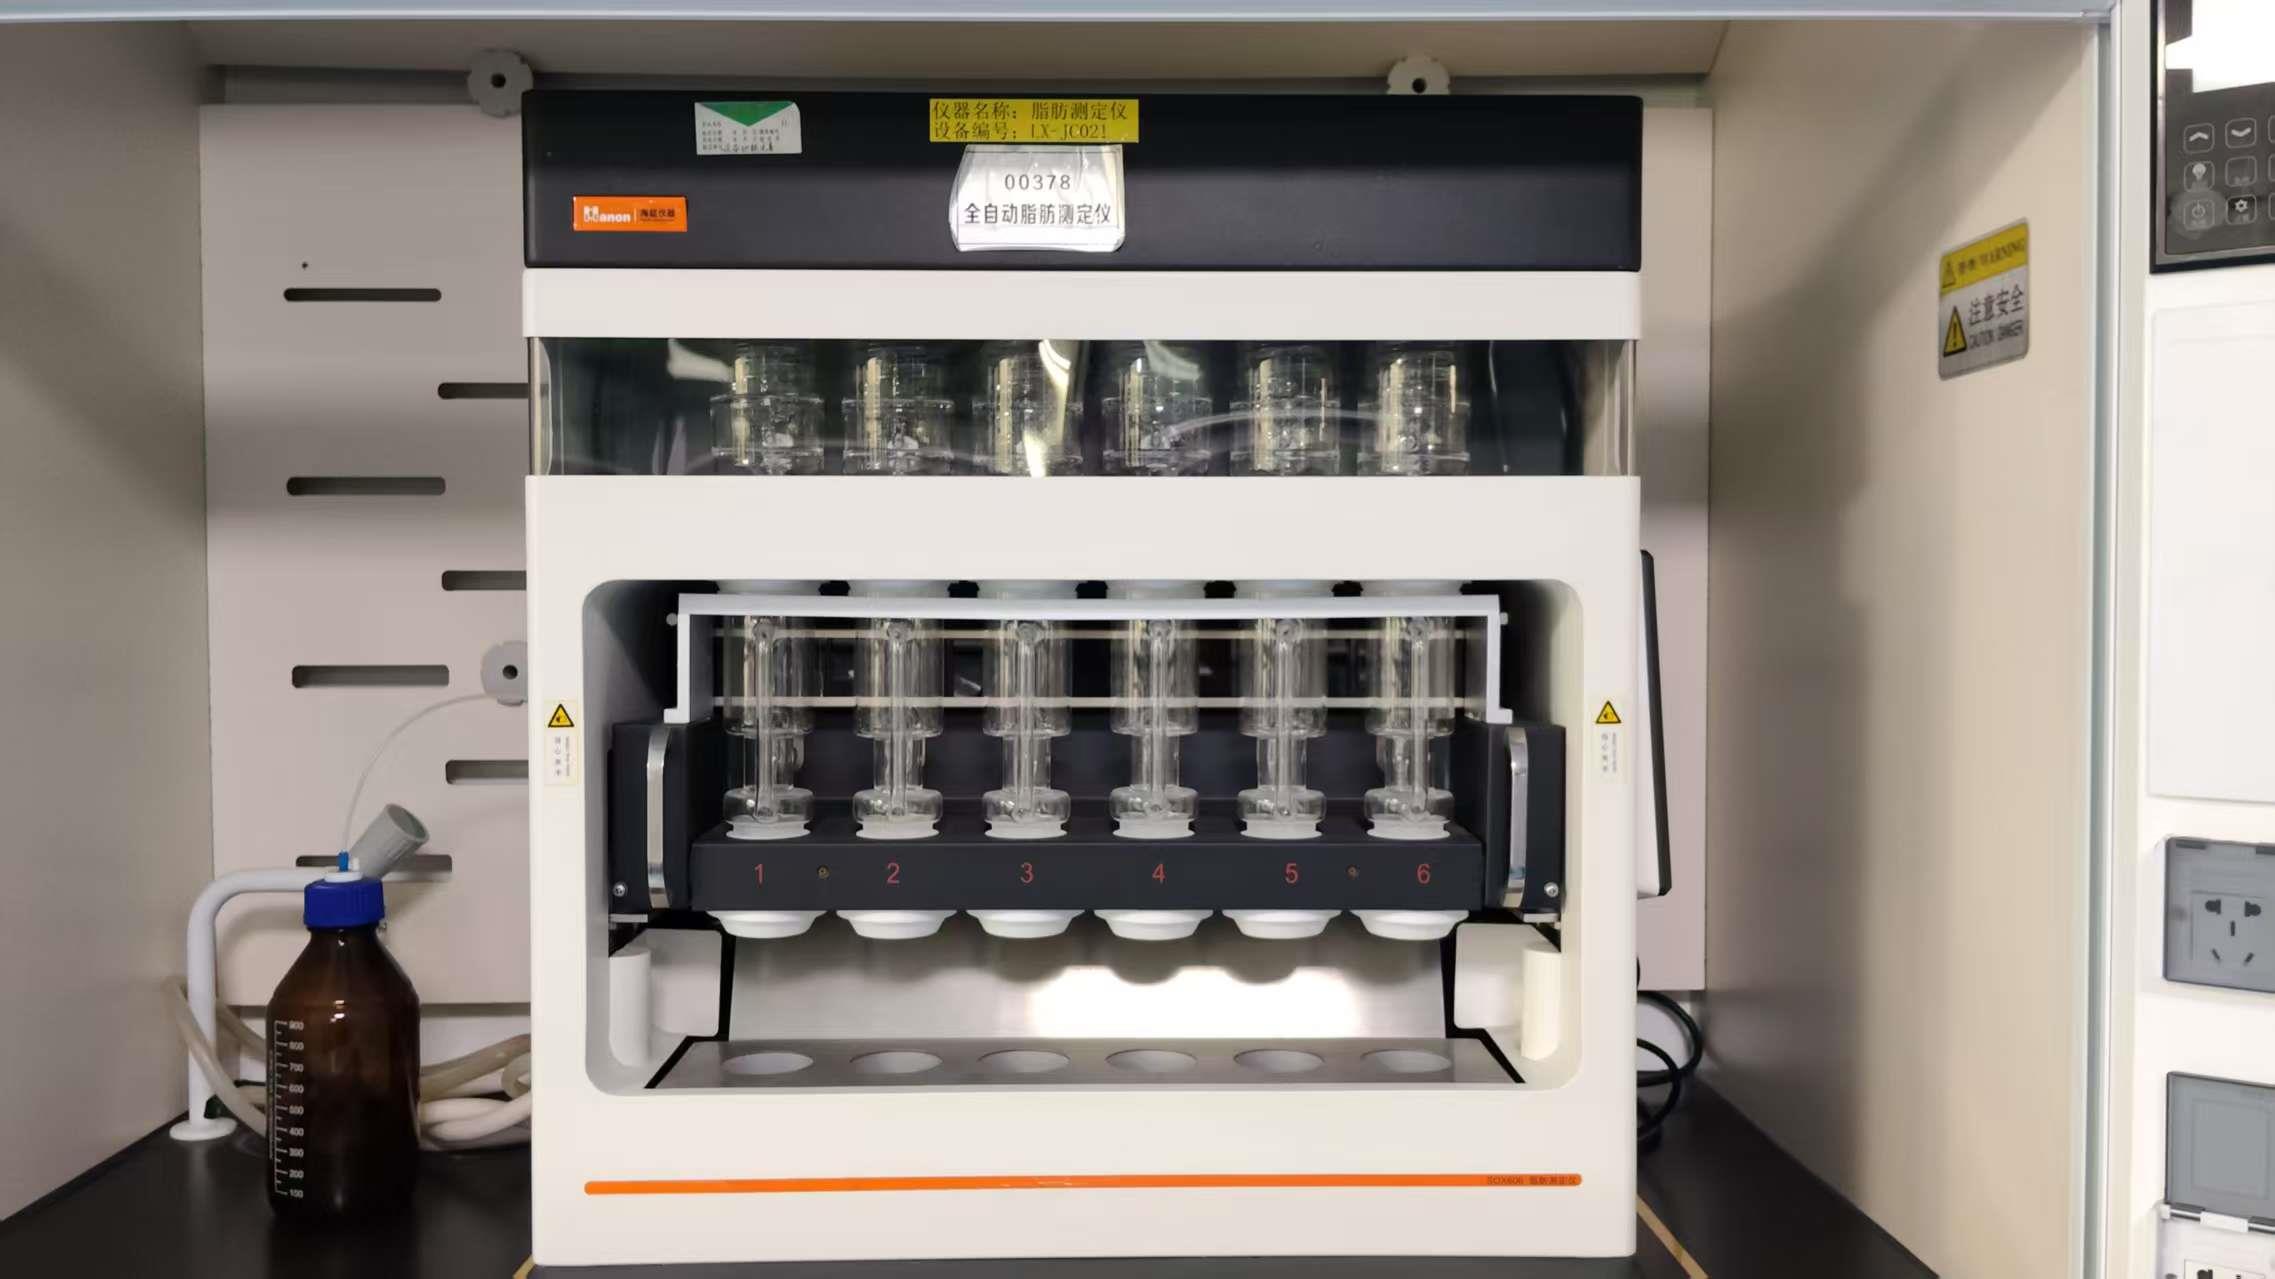
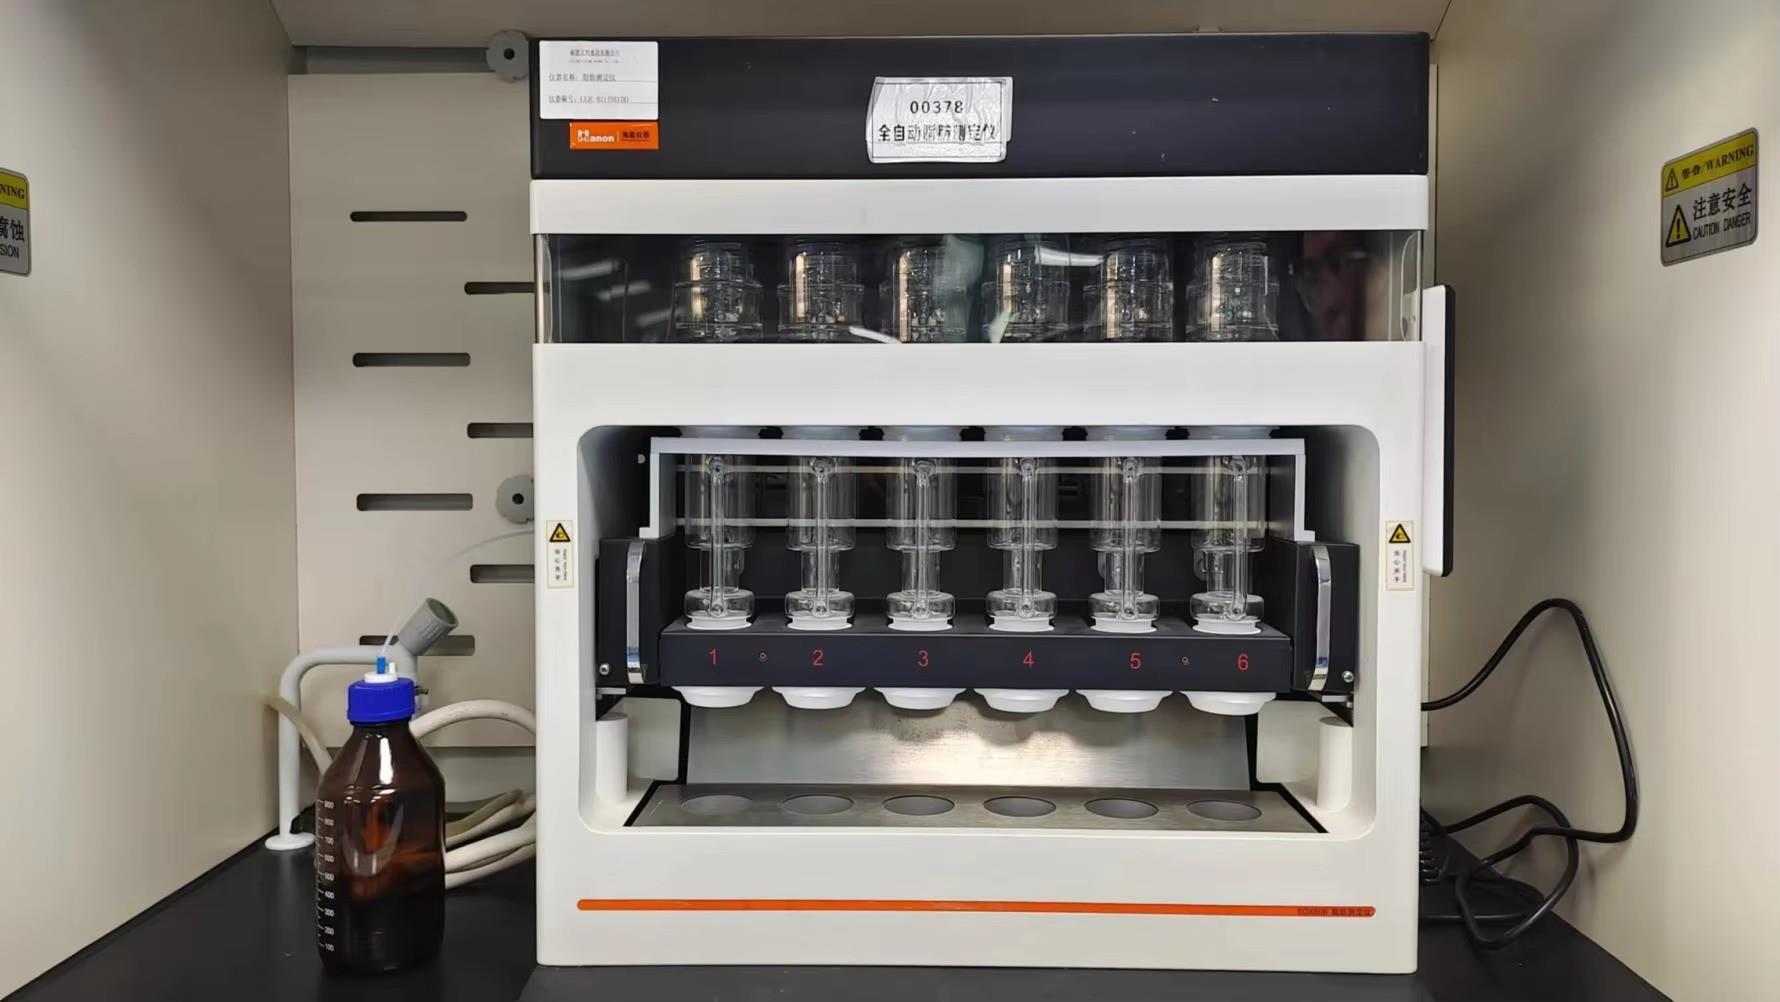
Automated Soxhlet solvent extraction analyzing crude and total lipid contents for dairy snacks, yogurt cubes, and savory soups.
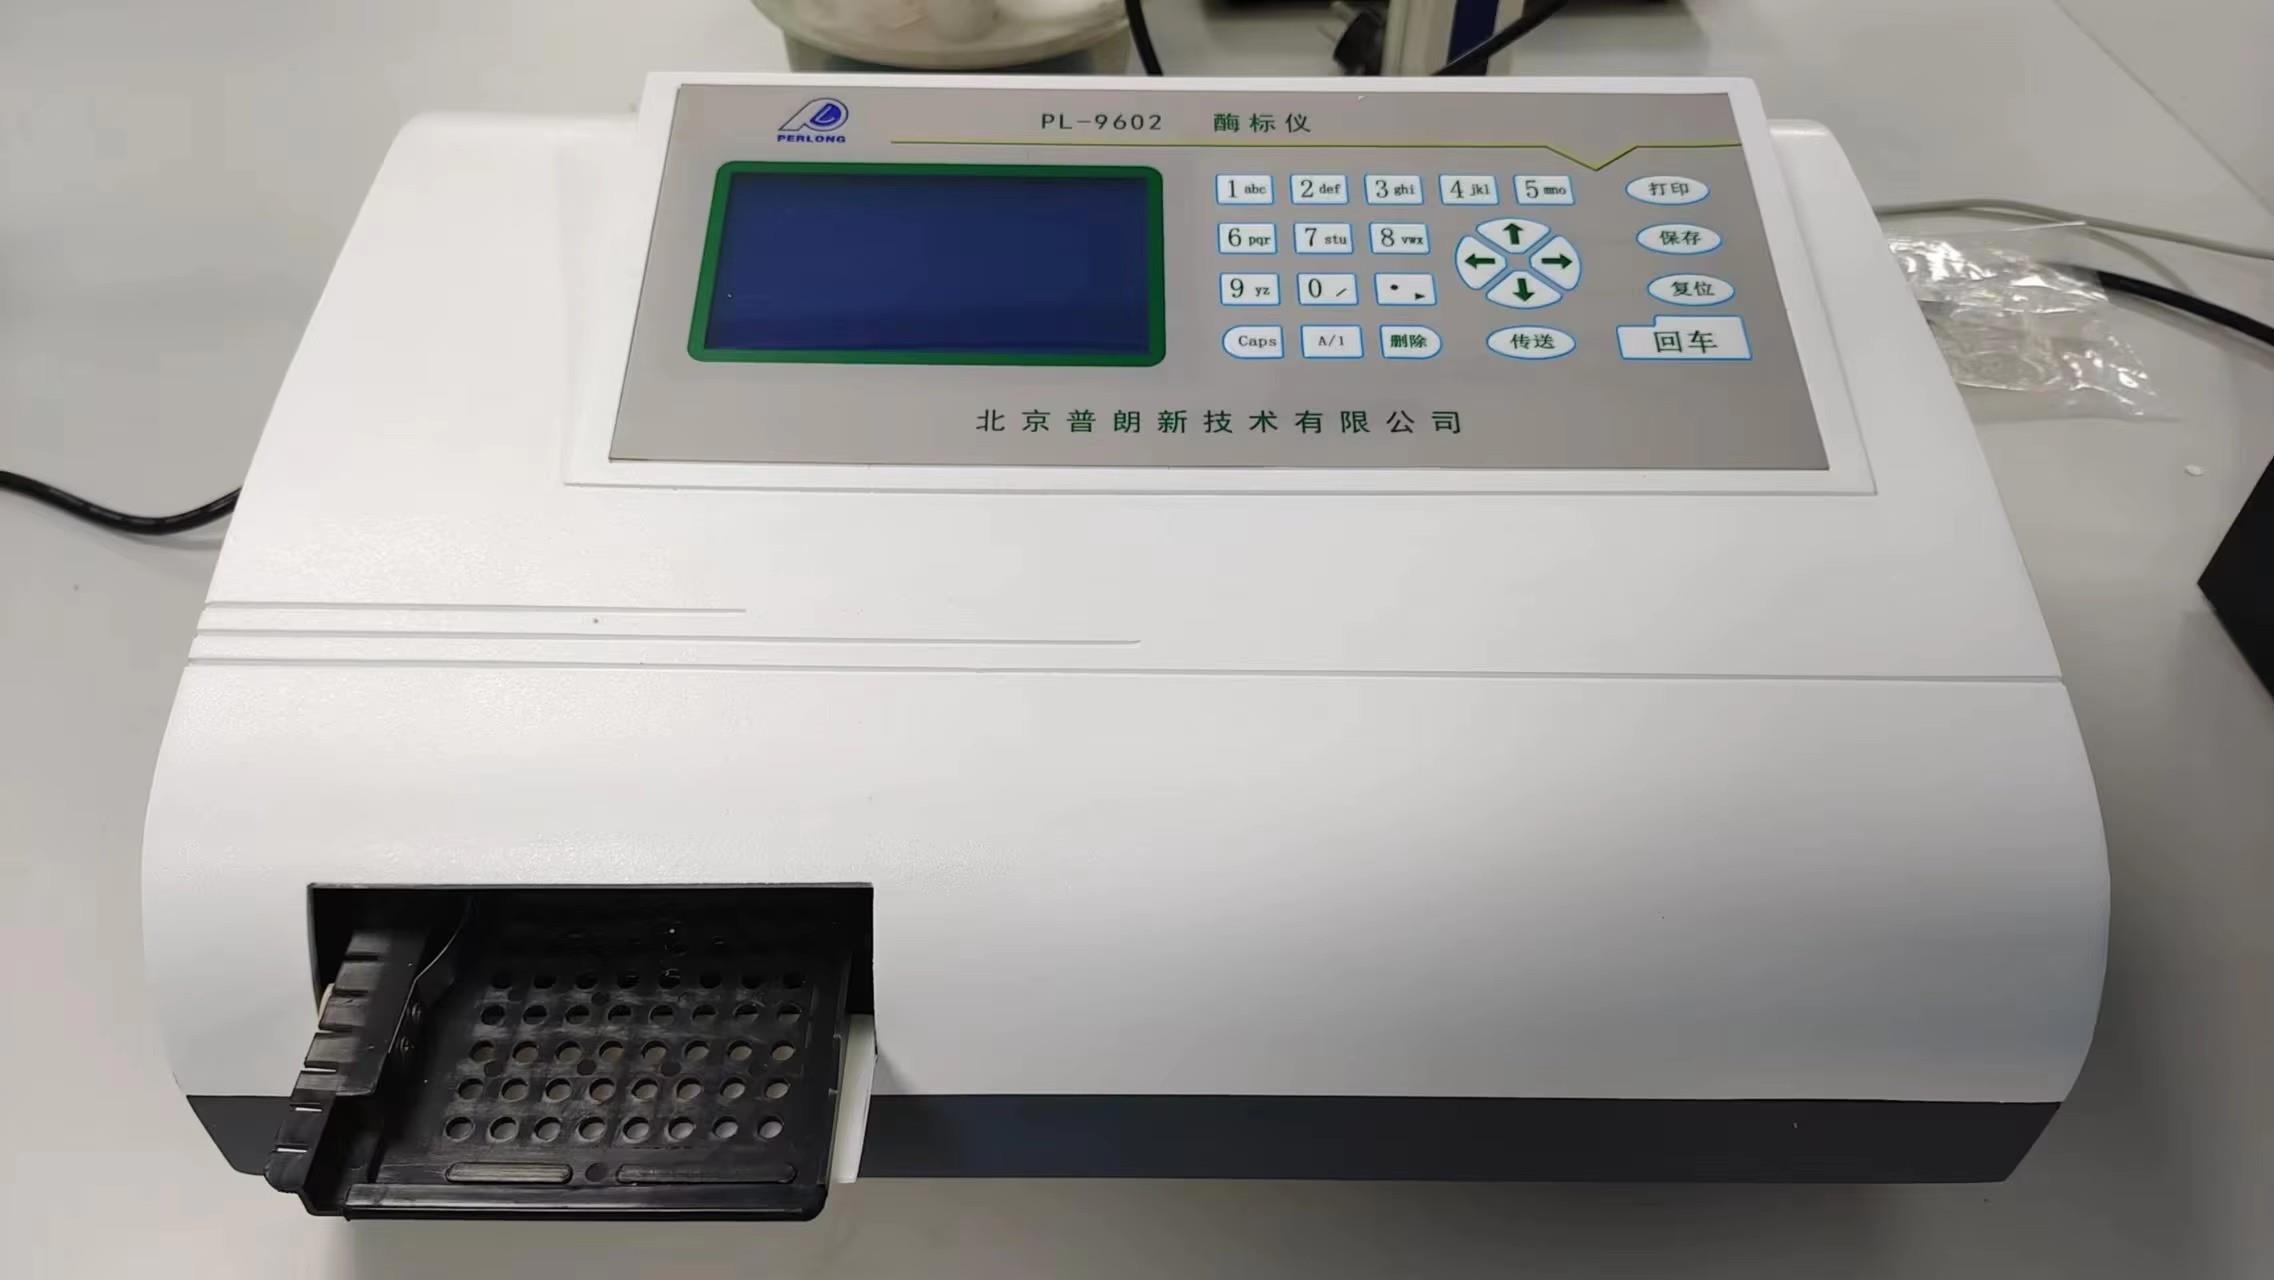
High-sensitivity photometric absorbance assays for rapid enzyme-linked immunosorbent tests (ELISA), allergen profiling, and mycotoxin checks.
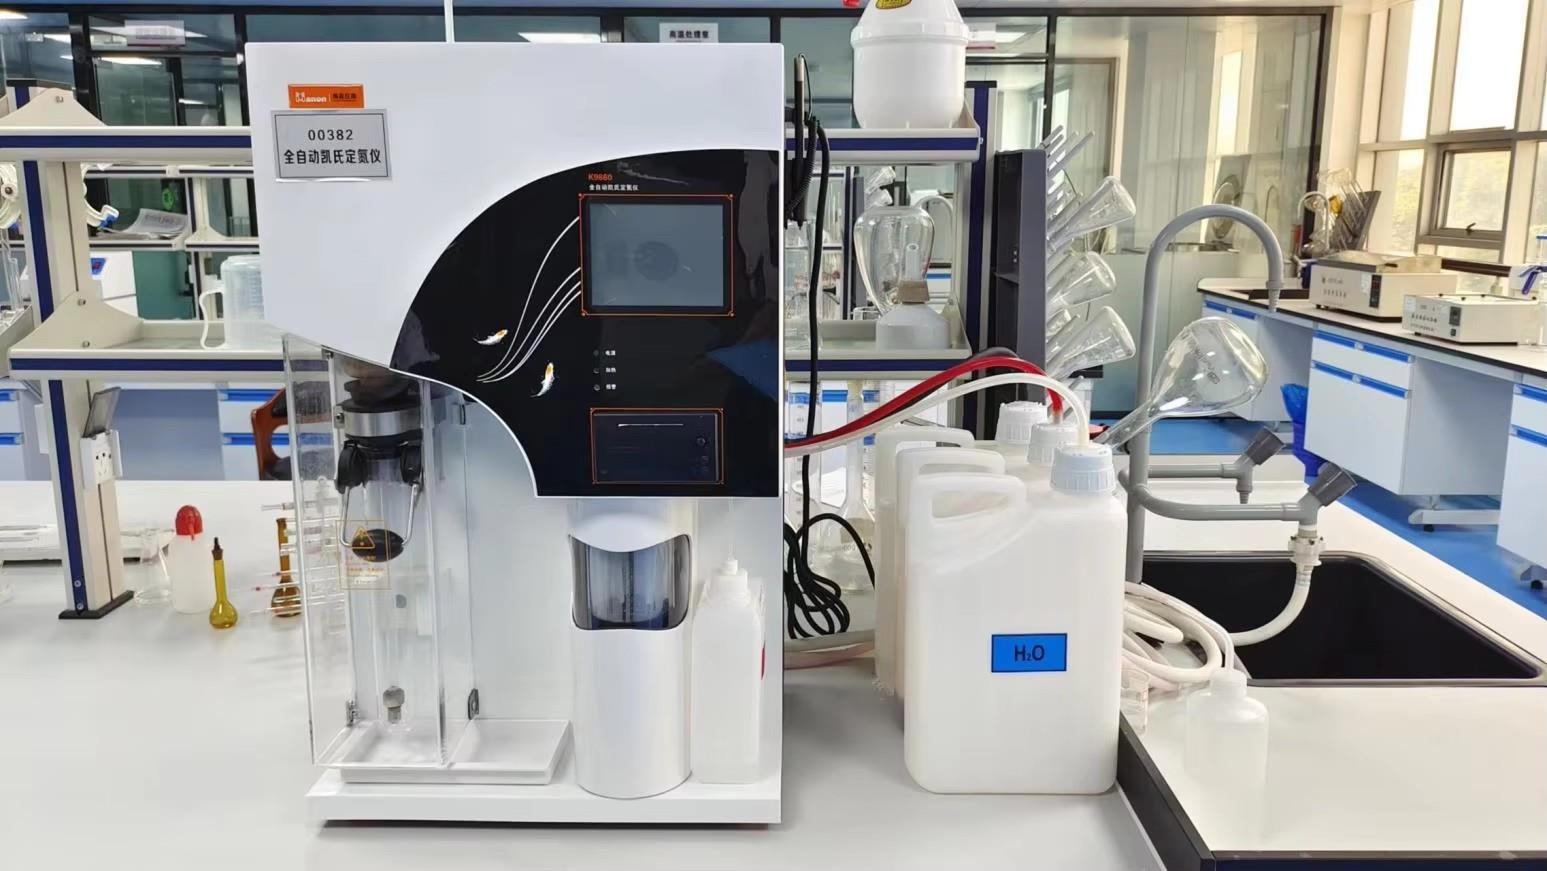
Quantitative determination of crude protein and nitrogen concentrations to guarantee strict nutritional fact panel fidelity.
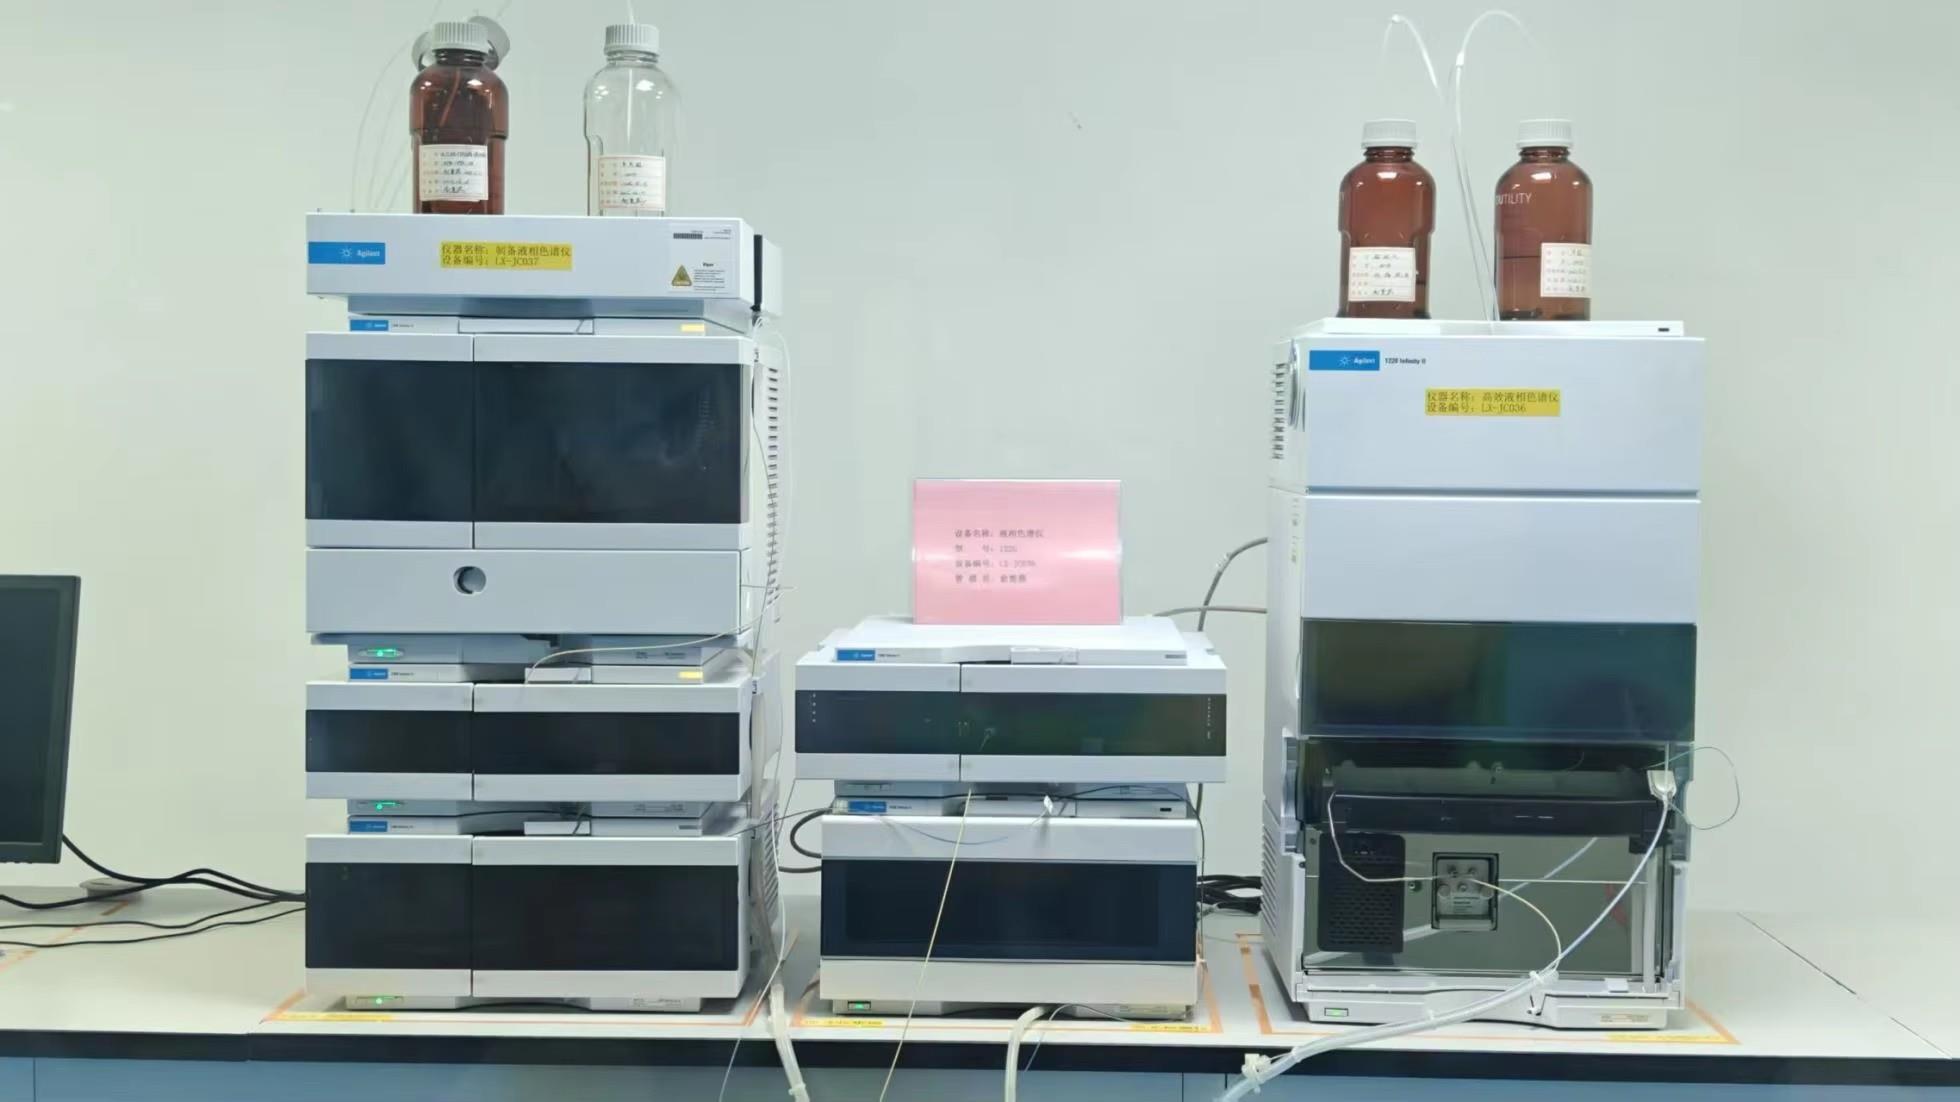
Chromatographic separation identifying active botanical compounds, tea polyphenols, caffeine grades, and trace pesticide residues.
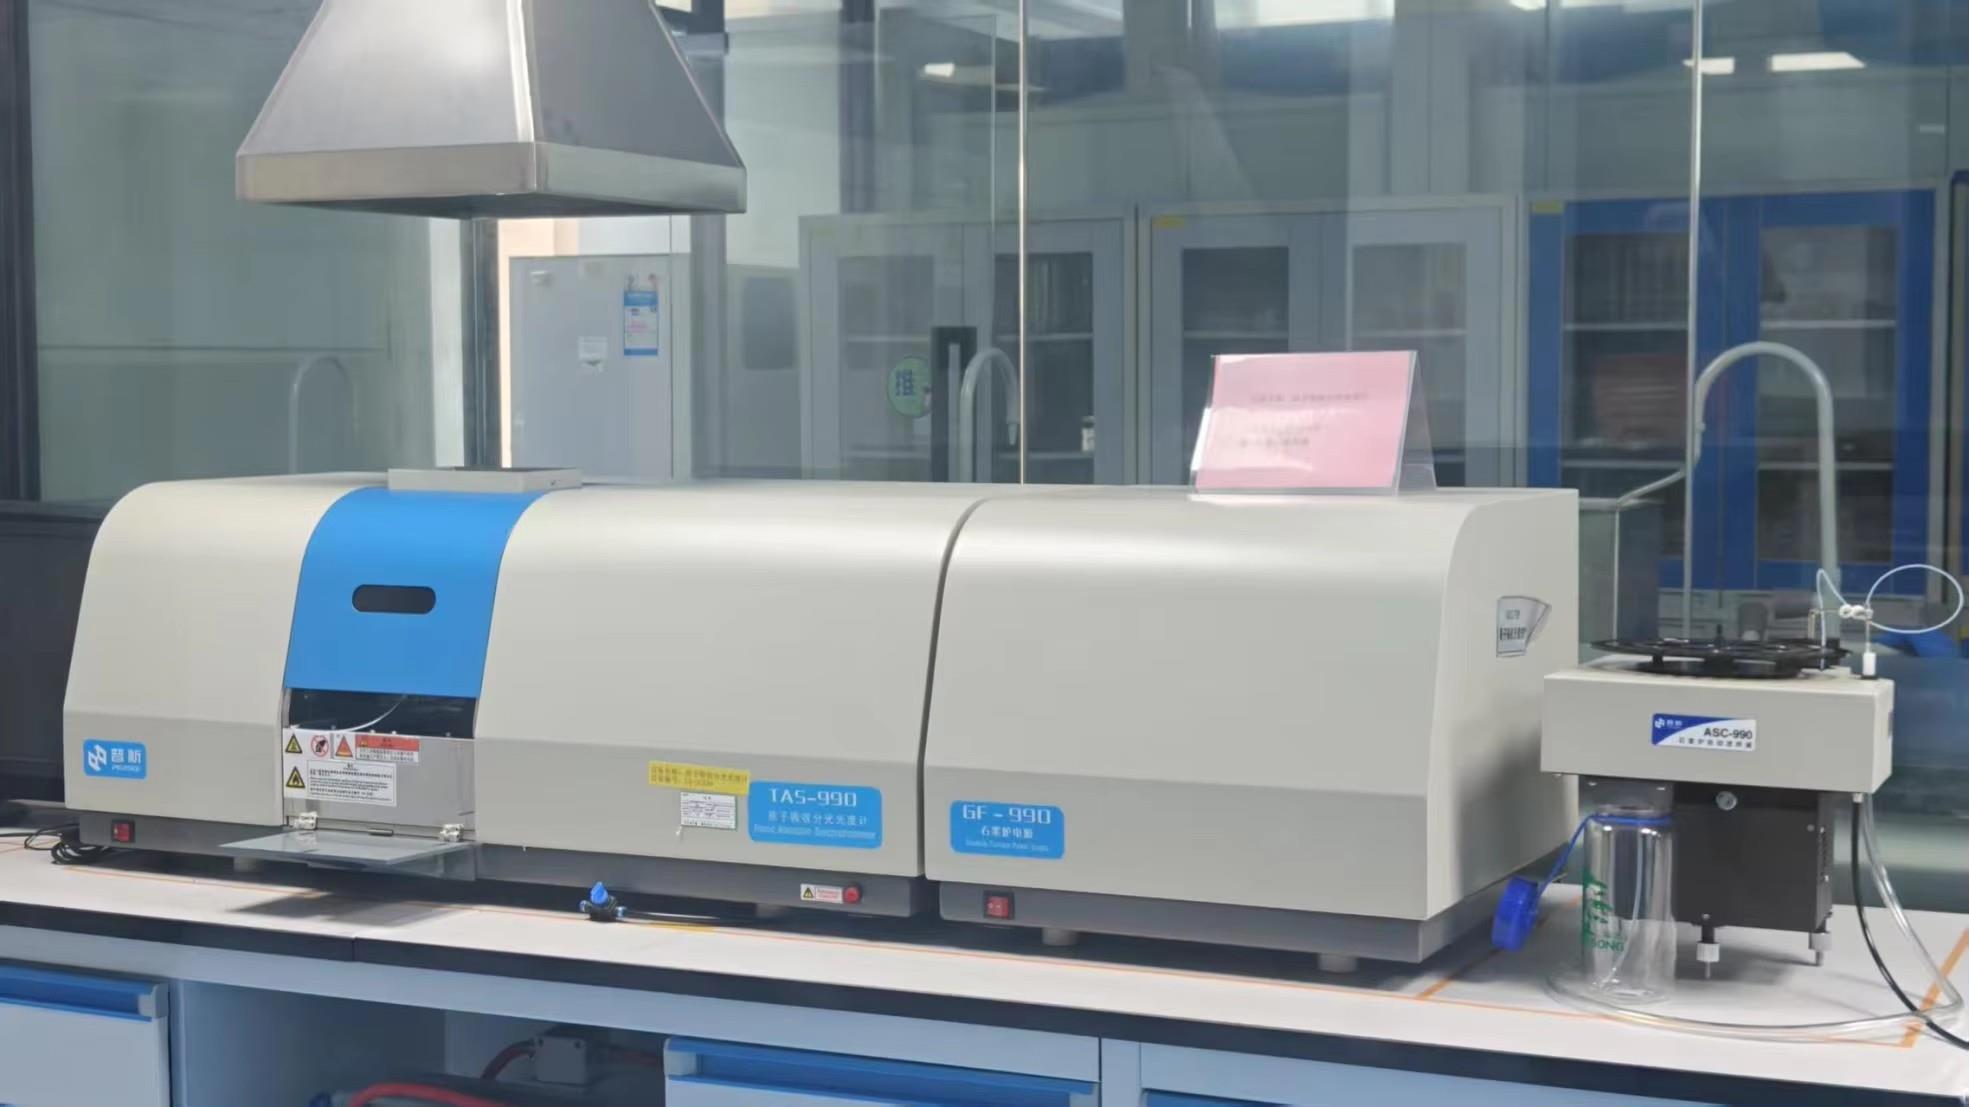
Elemental mineral analysis determining lead, cadmium, and essential trace metals down to parts-per-billion regulatory thresholds.
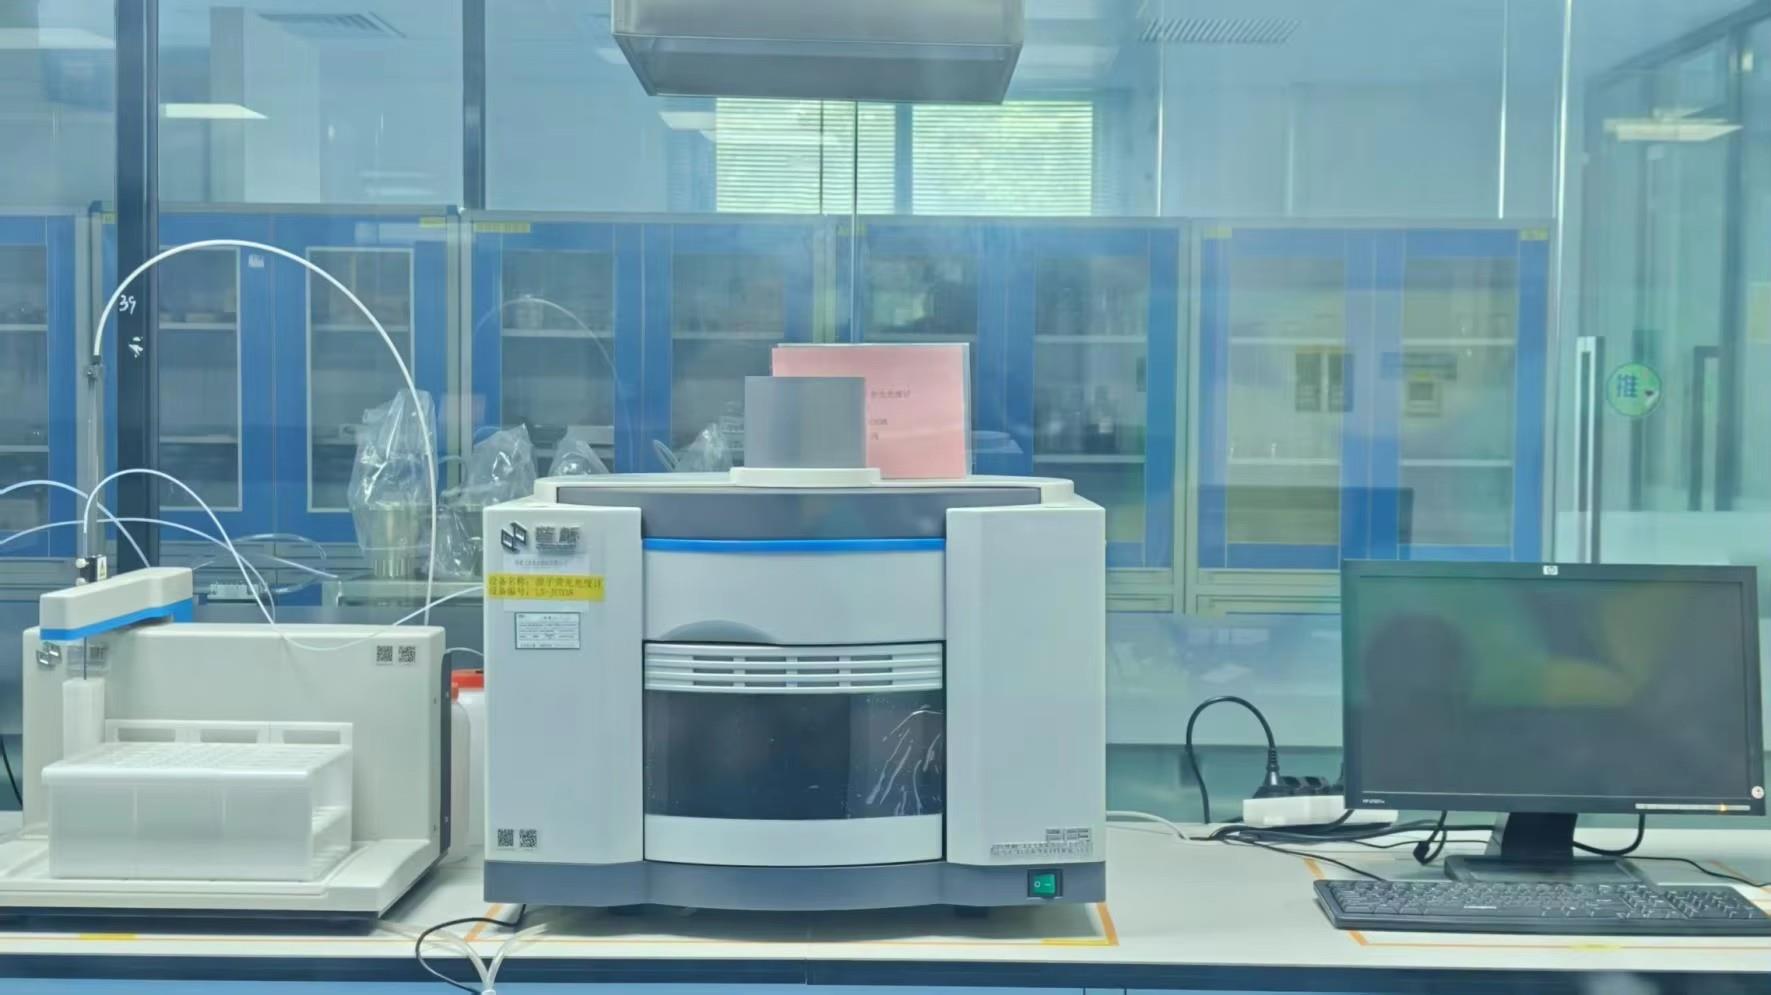
Ultrasensitive detection of hydride-forming heavy metals (mercury, arsenic) ensuring export safety to EU, US, and Asian markets.
10 senior formulation engineers developing innovative confectionery, fruit-milk mixtures, and cold-brew soluble beverages.
Whether you require private-label retail packaging or industrial bulk ingredients, our facility supports comprehensive OEM/ODM customization with full regulatory compliance.
Our manufacturing protocols conform to the most stringent international standards, audited and verified by independent accredited bodies CQM, BV, and TÜV Rheinland.
Hazard Analysis and Critical Control Points systematic preventative framework for biological, chemical, and physical controls.
Comprehensive Food Safety Management System validating complete organizational hygiene from intake to shipment.
International standard for quality management systems ensuring consistent product consistency and continuous improvement.
Environmental management standard demonstrating eco-conscious manufacturing, energy efficiency, and reduced emissions.
Occupational health and safety management system prioritizing employee welfare and safe workshop operations.
Business Social Compliance Initiative adherence ensuring ethical working conditions, fair treatment, and social responsibility.
Authoritative certification issued by international Islamic and Jewish dietary authorities for worldwide consumer access.
Certified organic production pathways guaranteeing non-GMO, chemical fertilizer-free, and sustainable ingredient compliance.