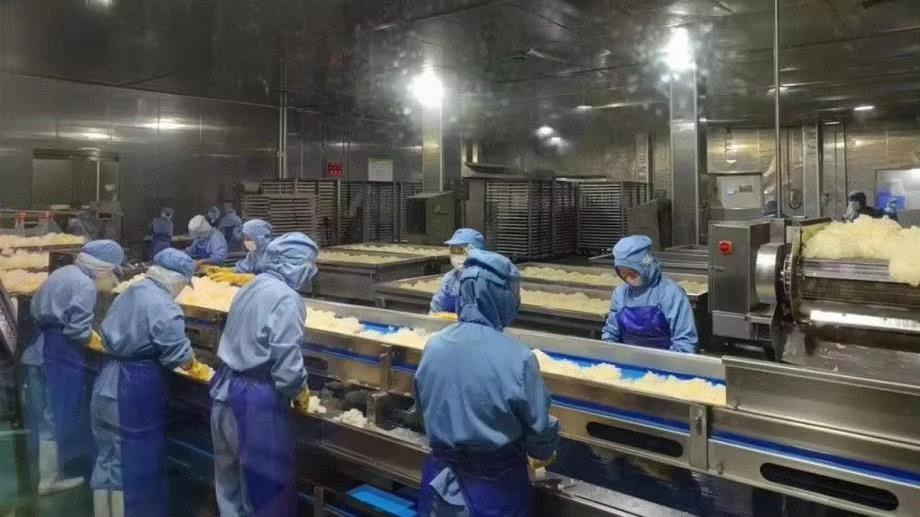
Backed by over 20 years of technical expertise, 37 production lines, and 62,718 m² of GMP-standard facility space, Fujian Fynergy Foods Co., Ltd. supplies verified global food brands, retailers, and distributors with shelf-stable, 100% natural freeze-dried foods.
Processed under ultra-low temperatures to lock in authentic flavor, crispness, and key vitamins without oil, sulfites, or artificial additives. Widely utilized in high-grade breakfast cereals, bakery, snack blends, and confectionery.
Our Zhangzhou factory strictly implements 8 standardized production steps to guarantee biological stability, food safety, and export quality standards for global supermarket chains and food conglomerates.
Step 01
Automated Cleaning
Multiple-stage ultrasonic and vortex bubble washing removes all field particulates, residues, and surface impurities thoroughly.
Step 02
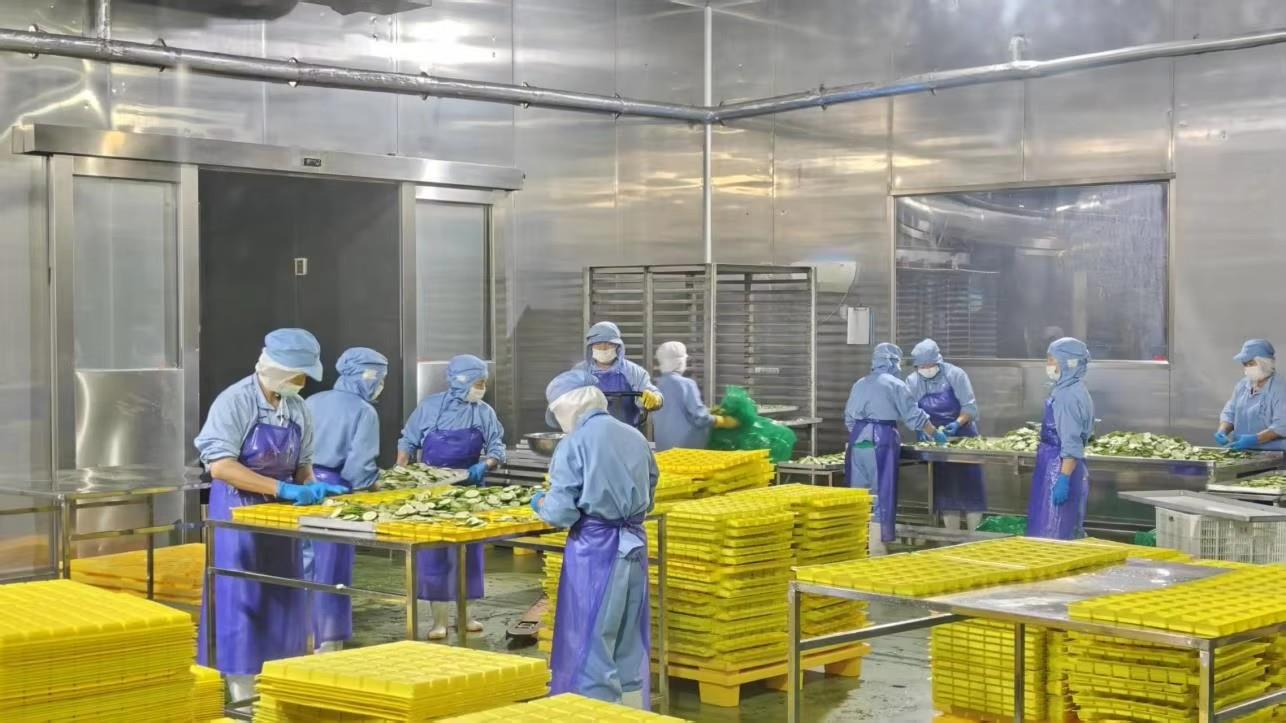
Cleanroom Traying
Pre-chilled fruit and ingredients are carefully sliced and arranged onto uniform food-grade 304 stainless trays in clean conditions.
Step 03
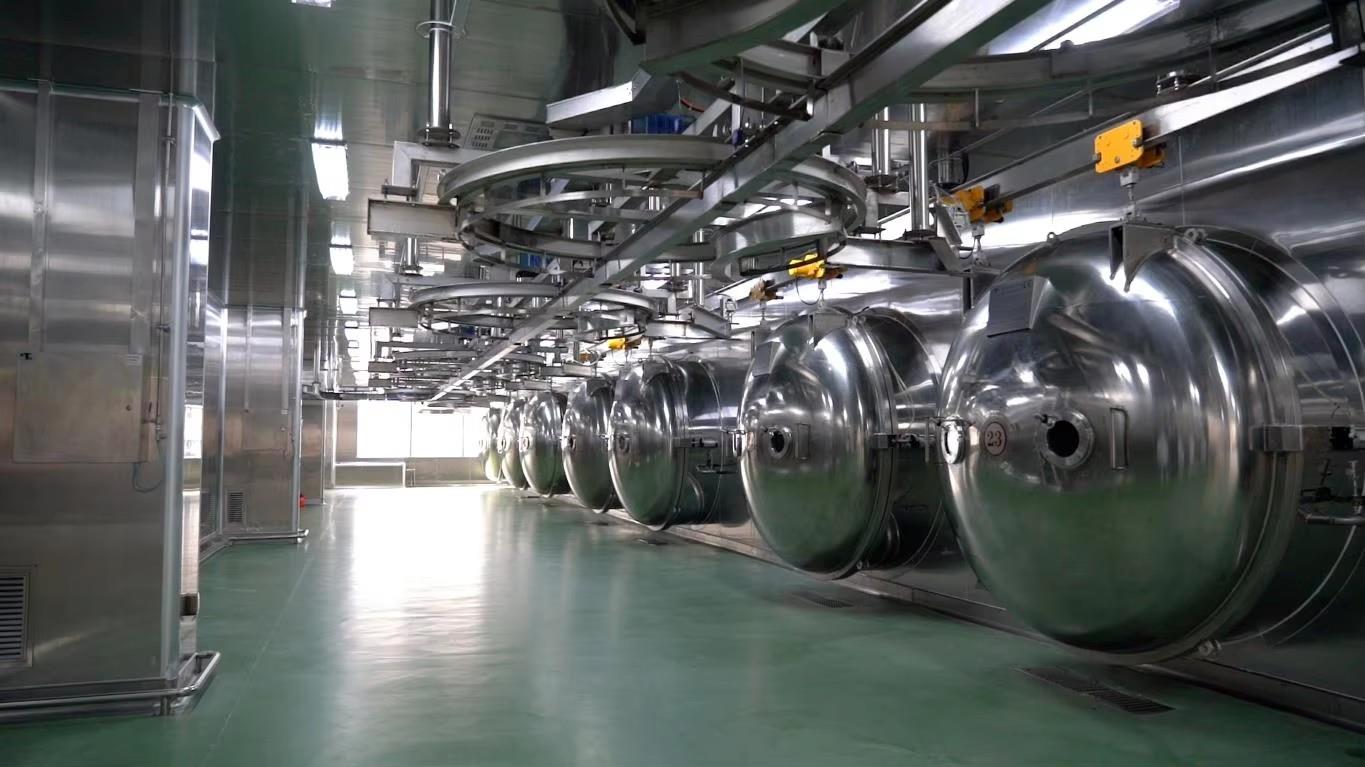
Vacuum Sublimation
Sublimation drying takes place under deep vacuum, preserving native cell structures, natural color, aroma, and essential heat-sensitive nutrition.
Step 04
Barrier Packaging
Executed within Class 100,000 cleanrooms with constant temperature and dehumidification to avoid ambient moisture reabsorption.
Step 05
Packed Storage
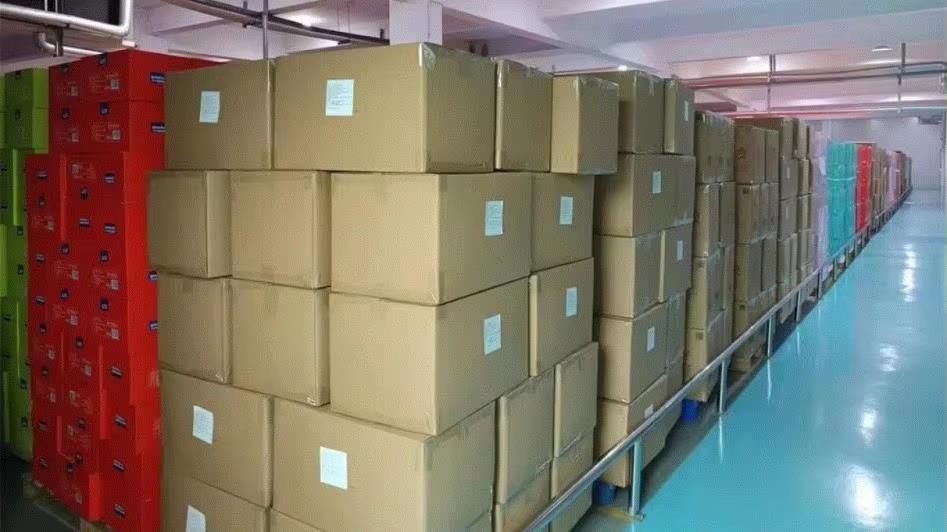
Sealed aluminum foil packs and multi-layer corrugated export cartons are stacked under strict climate-controlled warehouse facilities.
Step 06
FD Furnace Lines
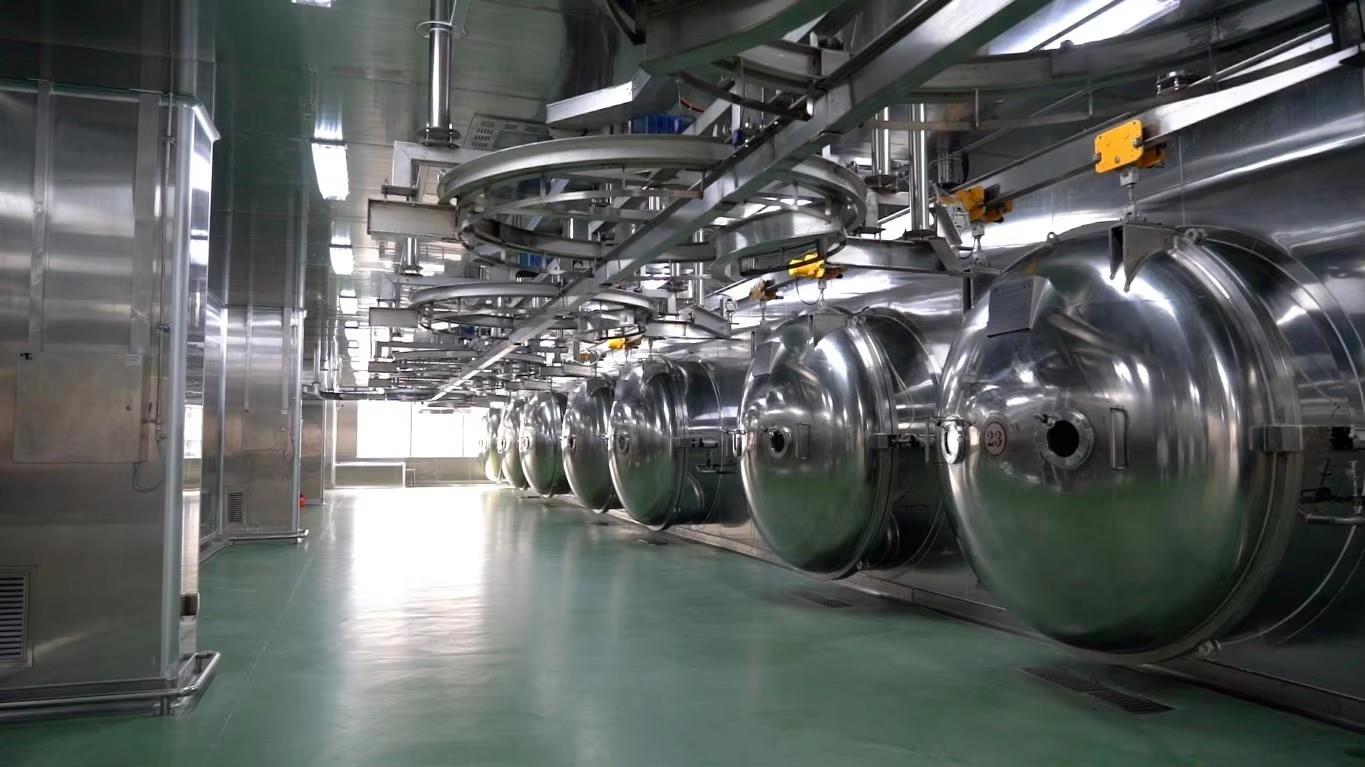
Our expansive plant operates 37 computerized freeze-drying chambers delivering over 8,000 square meters of total freeze-drying capacity.
Step 07
Extraction & Concentration
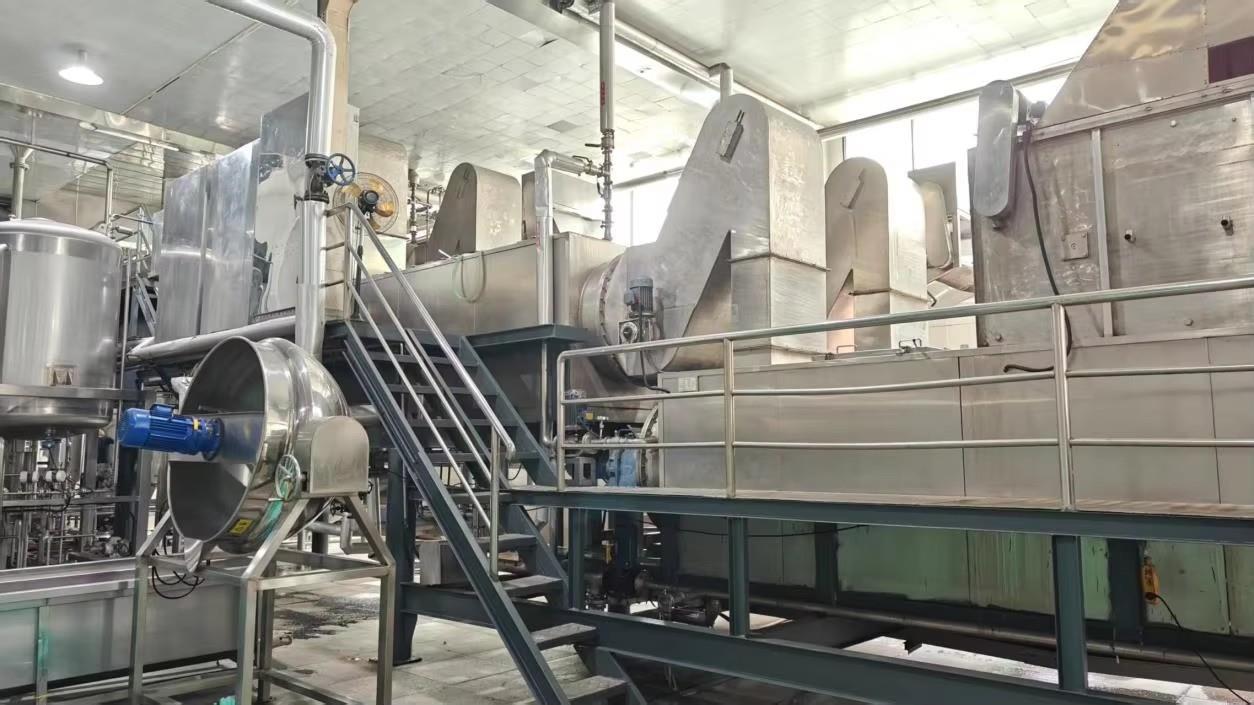
Continuous closed-loop extraction system designed for tea, plant, and herbal infusions to produce instant freeze-dried extracts.
Step 08
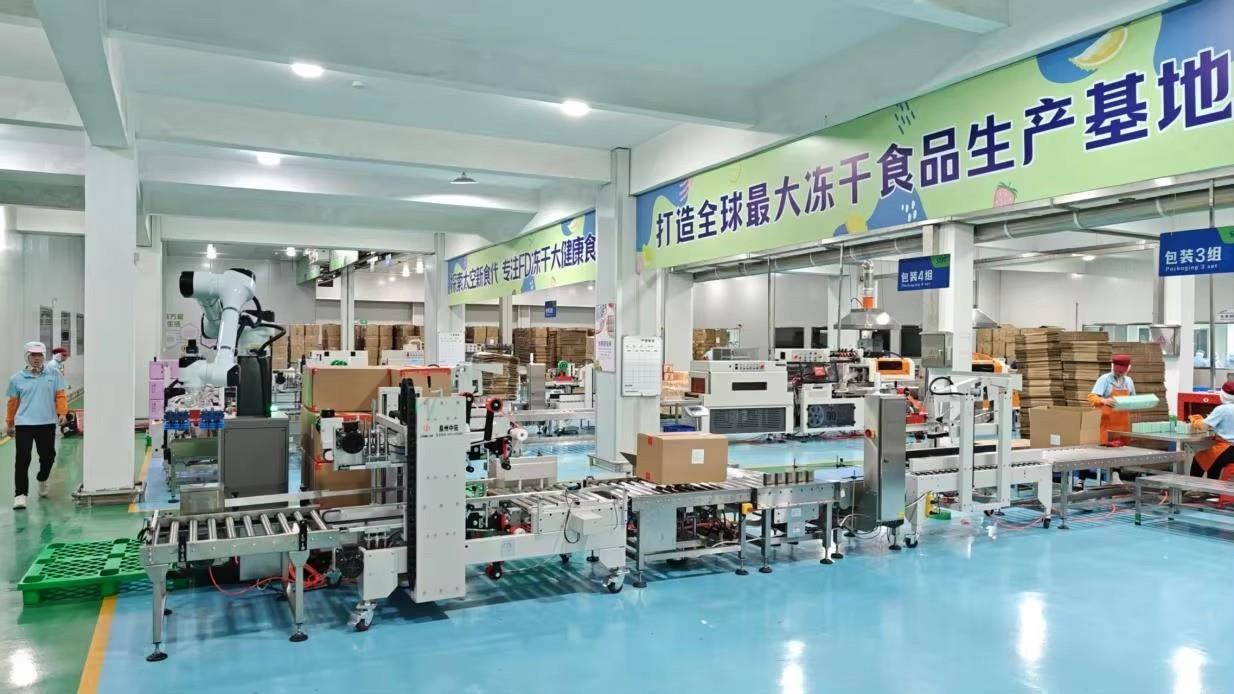
Automated Packaging
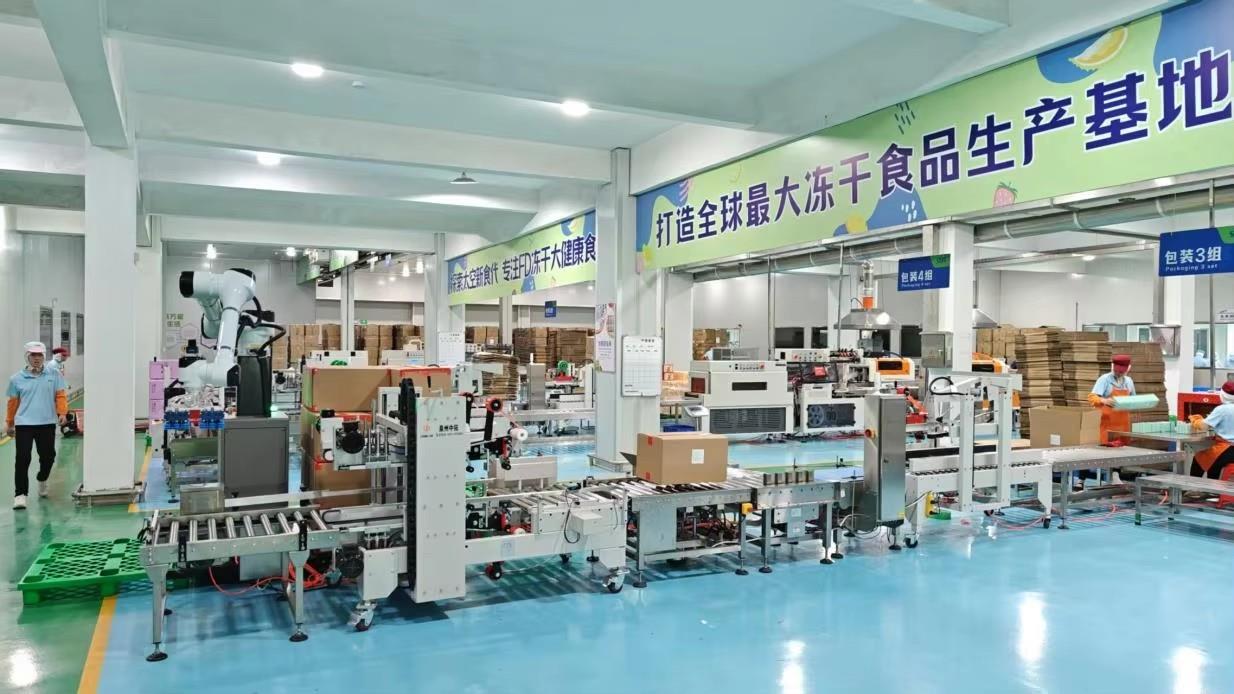
High-speed form-fill-seal lines and multi-head weighers manage flexible pouching, nitrogen flushing, metal detection, and checkweighing.
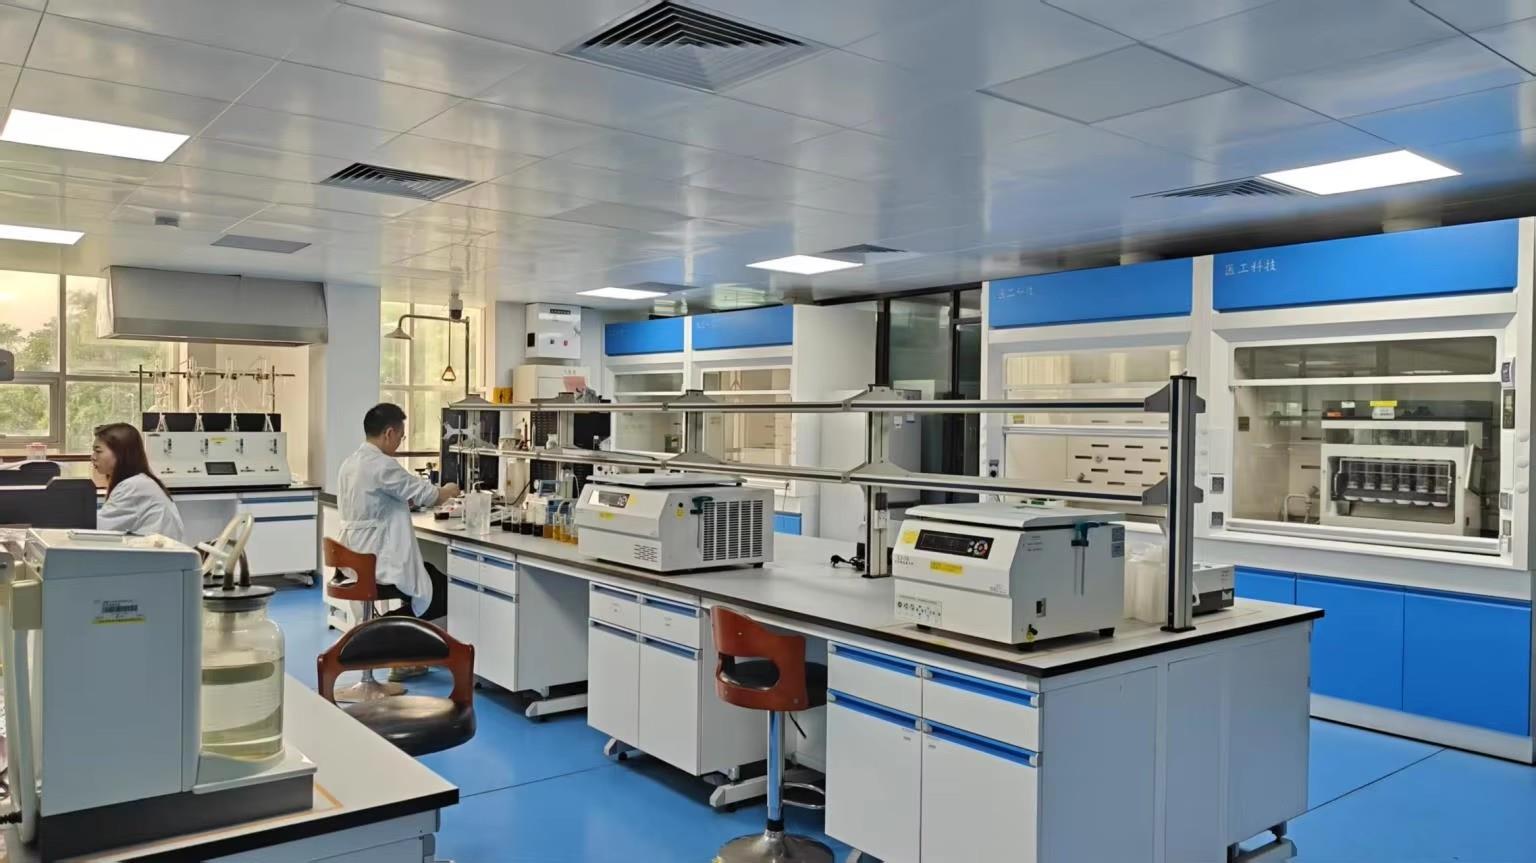
To support global supply agreements and comply with FDA, EFSA, and international standards, our certified on-site analytical laboratory conducts testing on every batch using advanced analytical instruments.
Independent QA Lab
Dedicated food analysis laboratory staffed by microbiologists and food engineers verifying safety criteria before batch clearance.
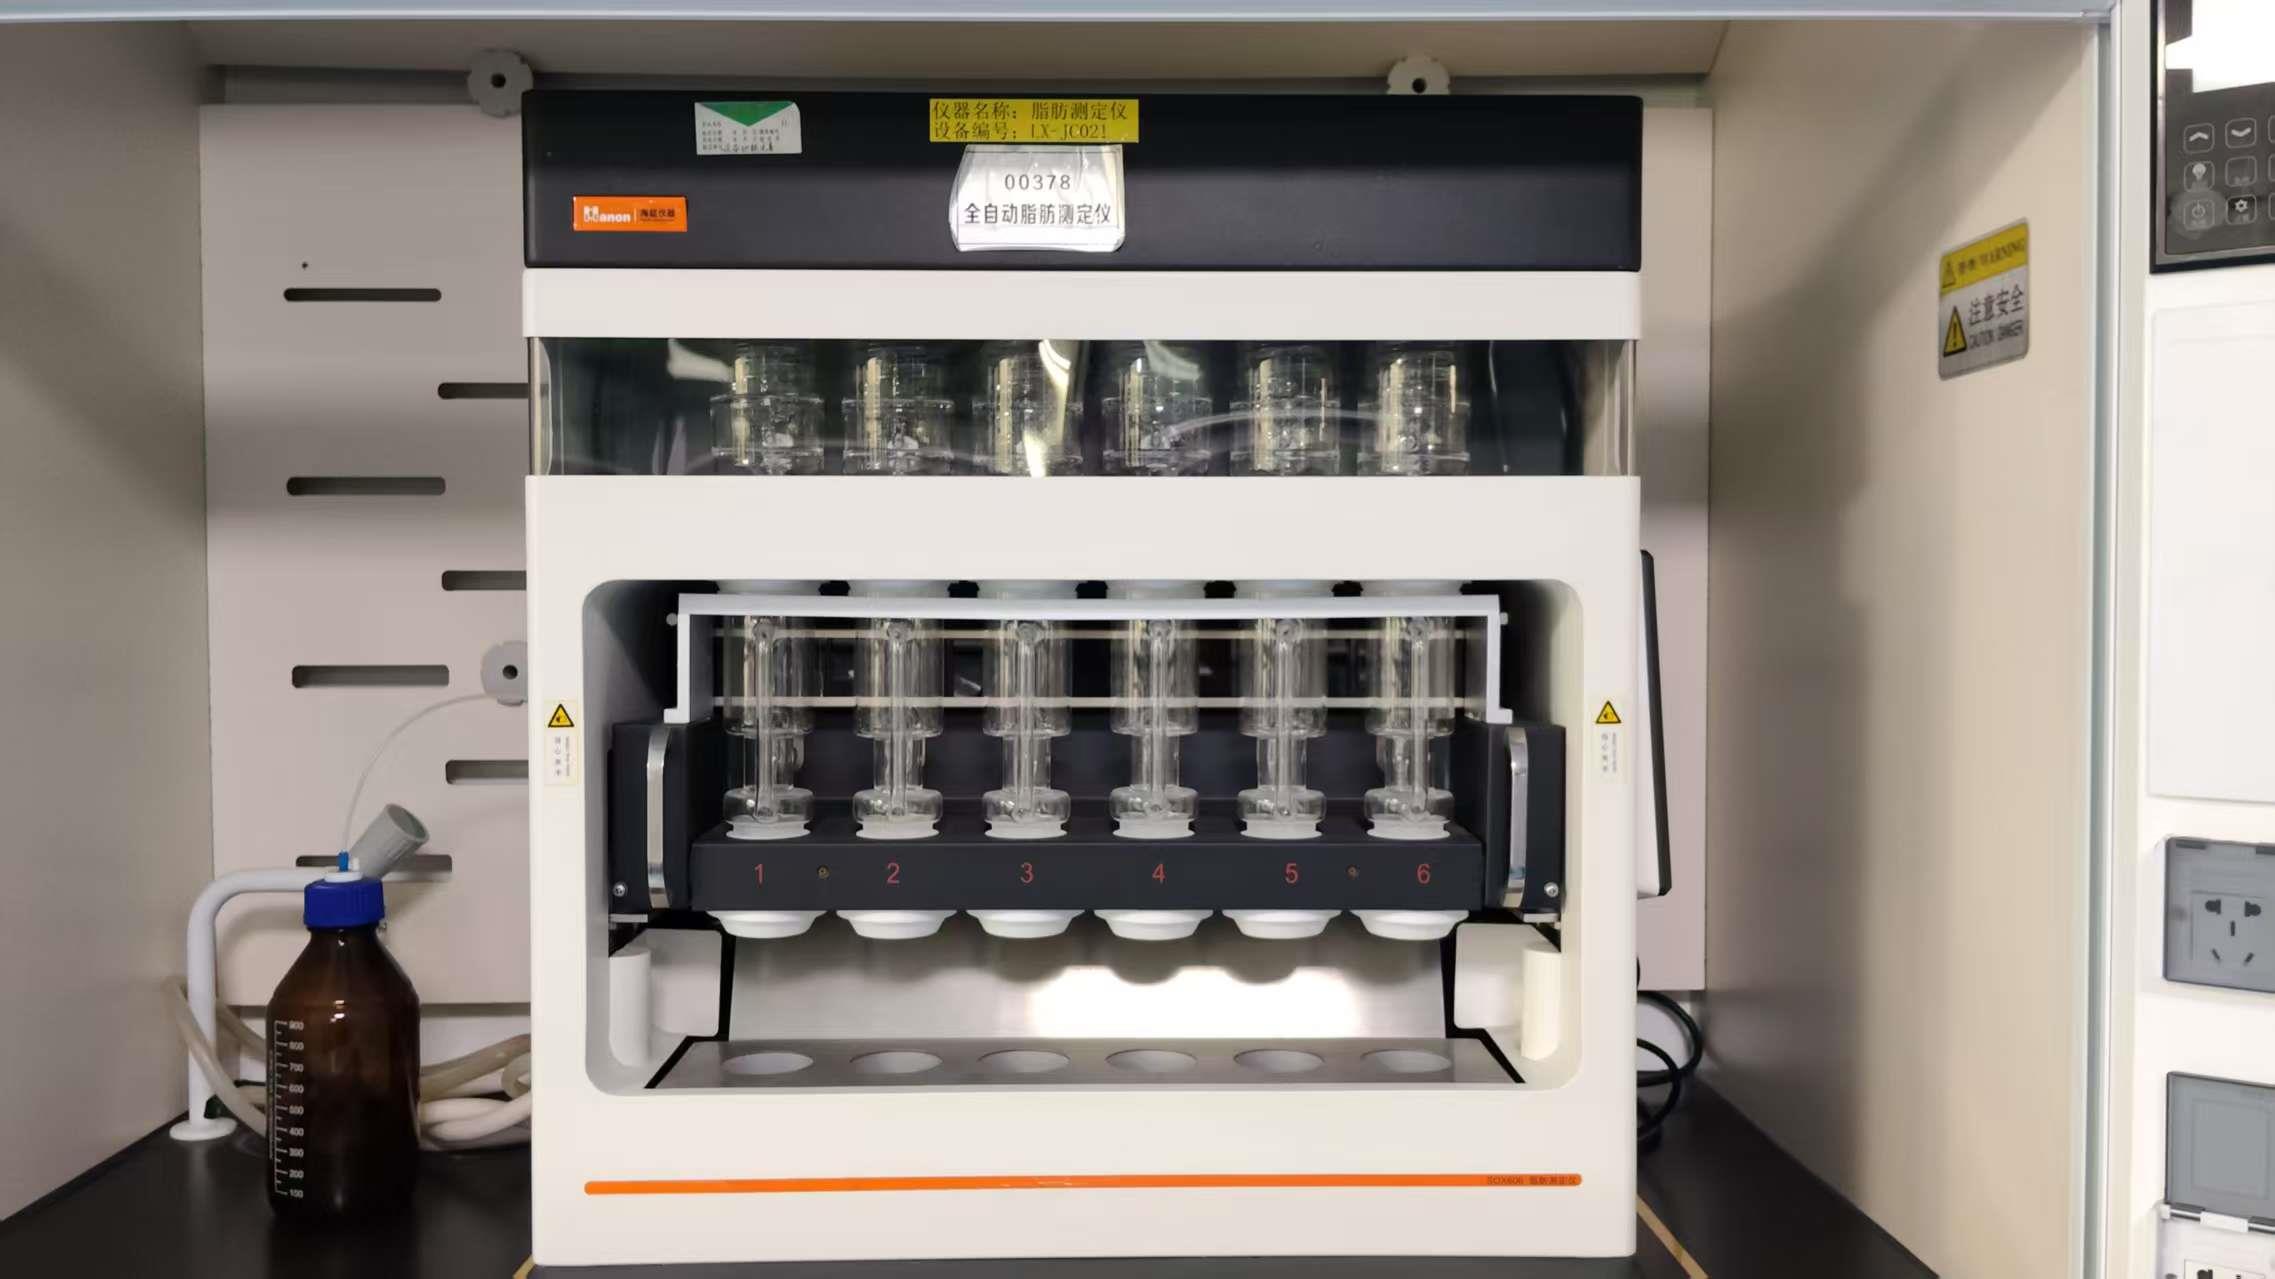
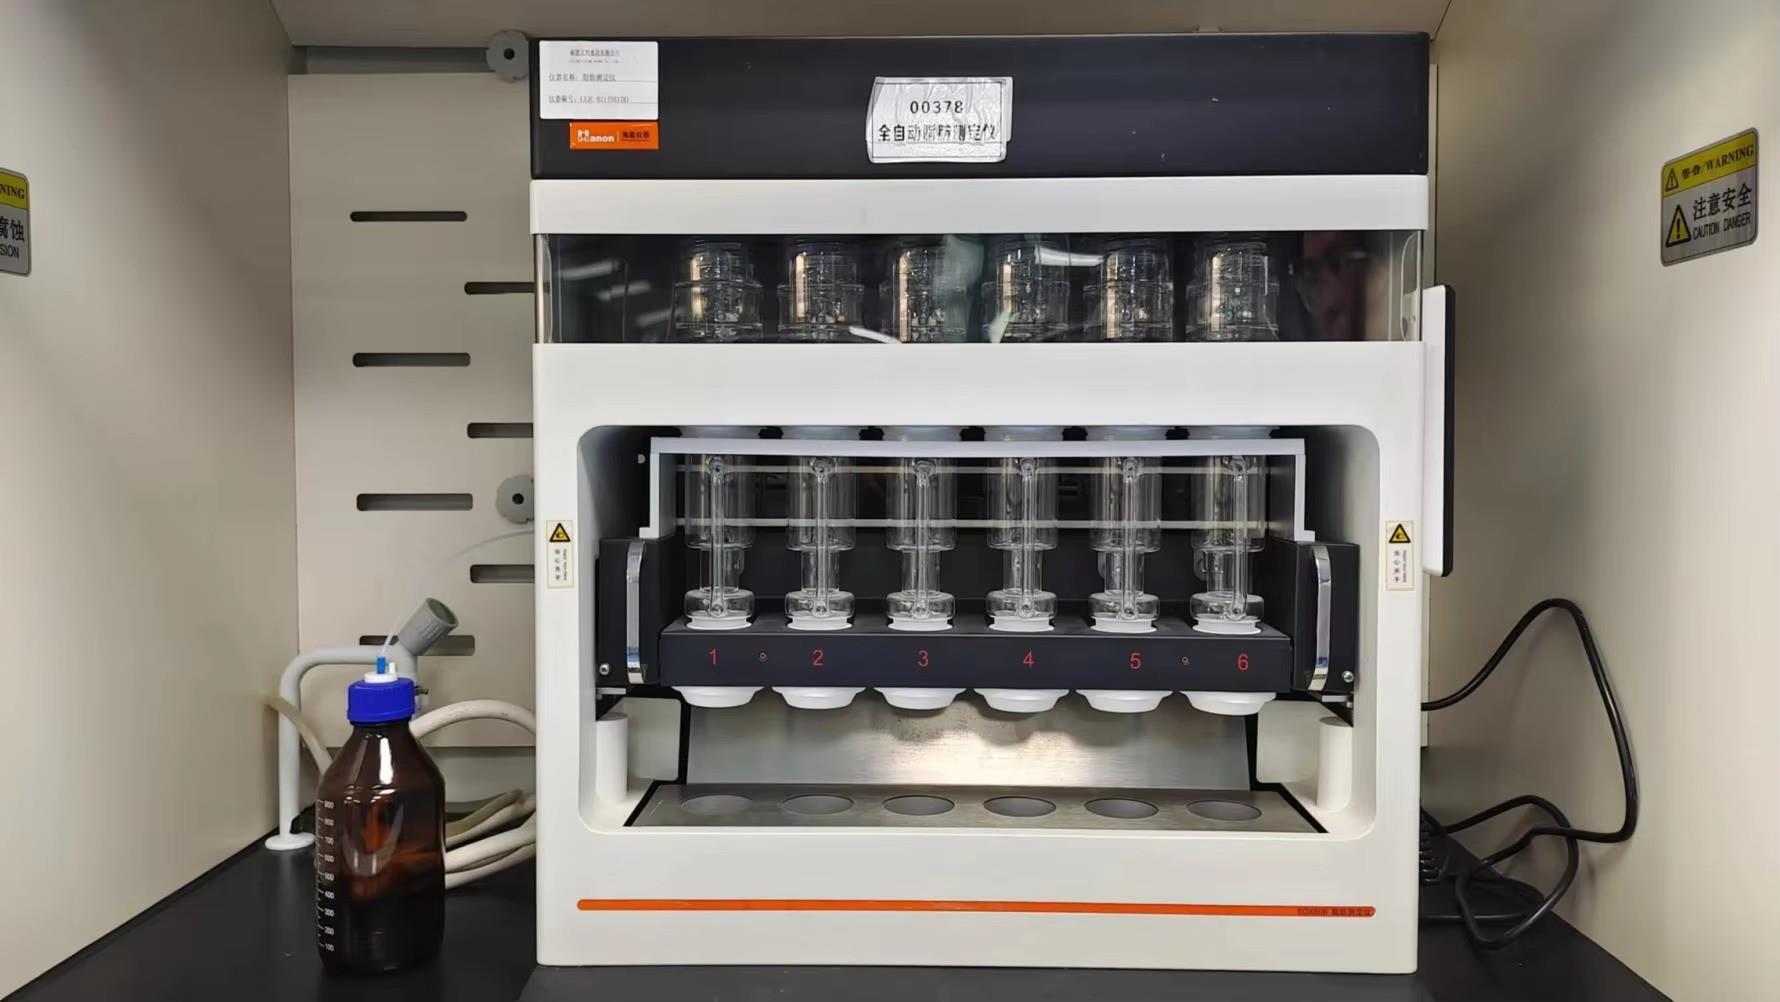
Automatic Fat Analyzer
Precise Soxhlet extraction apparatus to quantify lipid levels across dairy, soups, confectioneries, and snacks for nutritional fact labels.
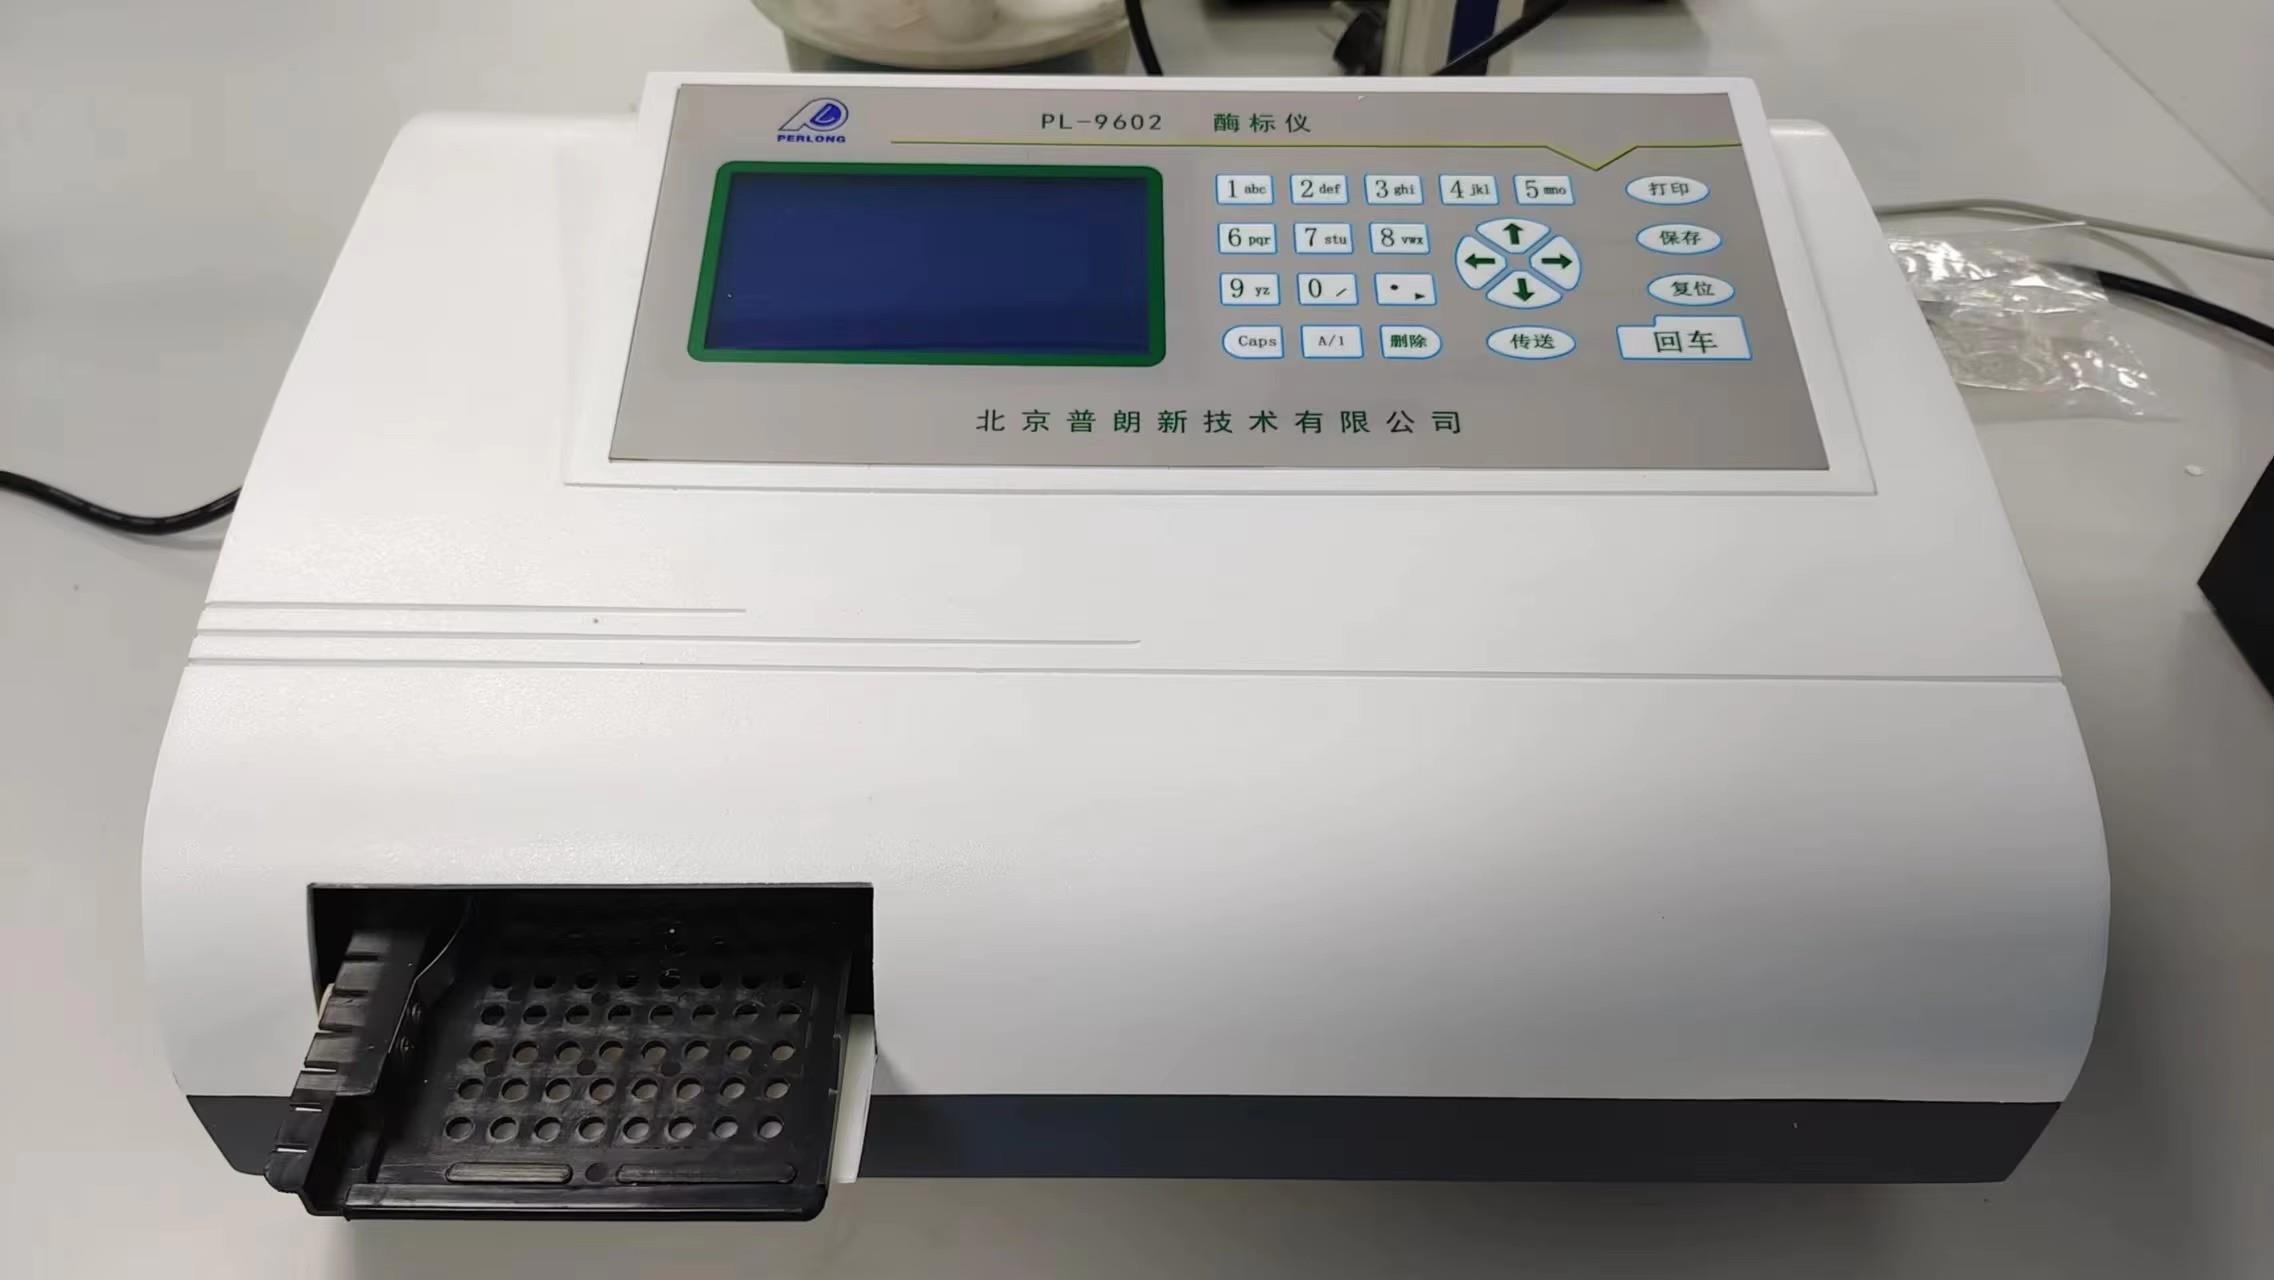
Microplate Reader
High-throughput photometric absorption system testing allergen markers, enzyme activities, and microbiological assay profiles.
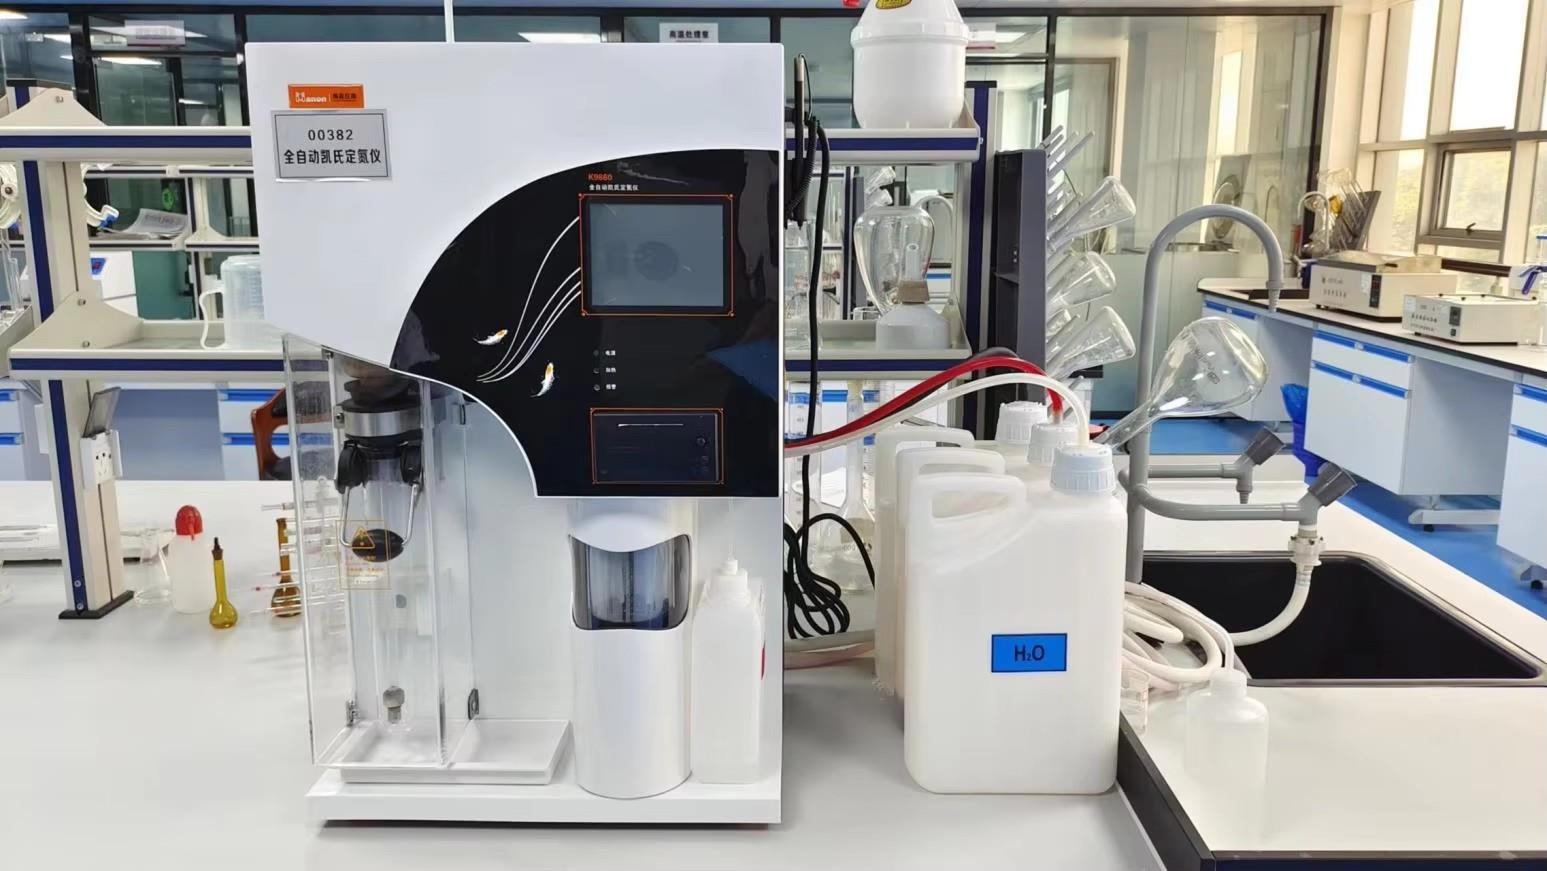
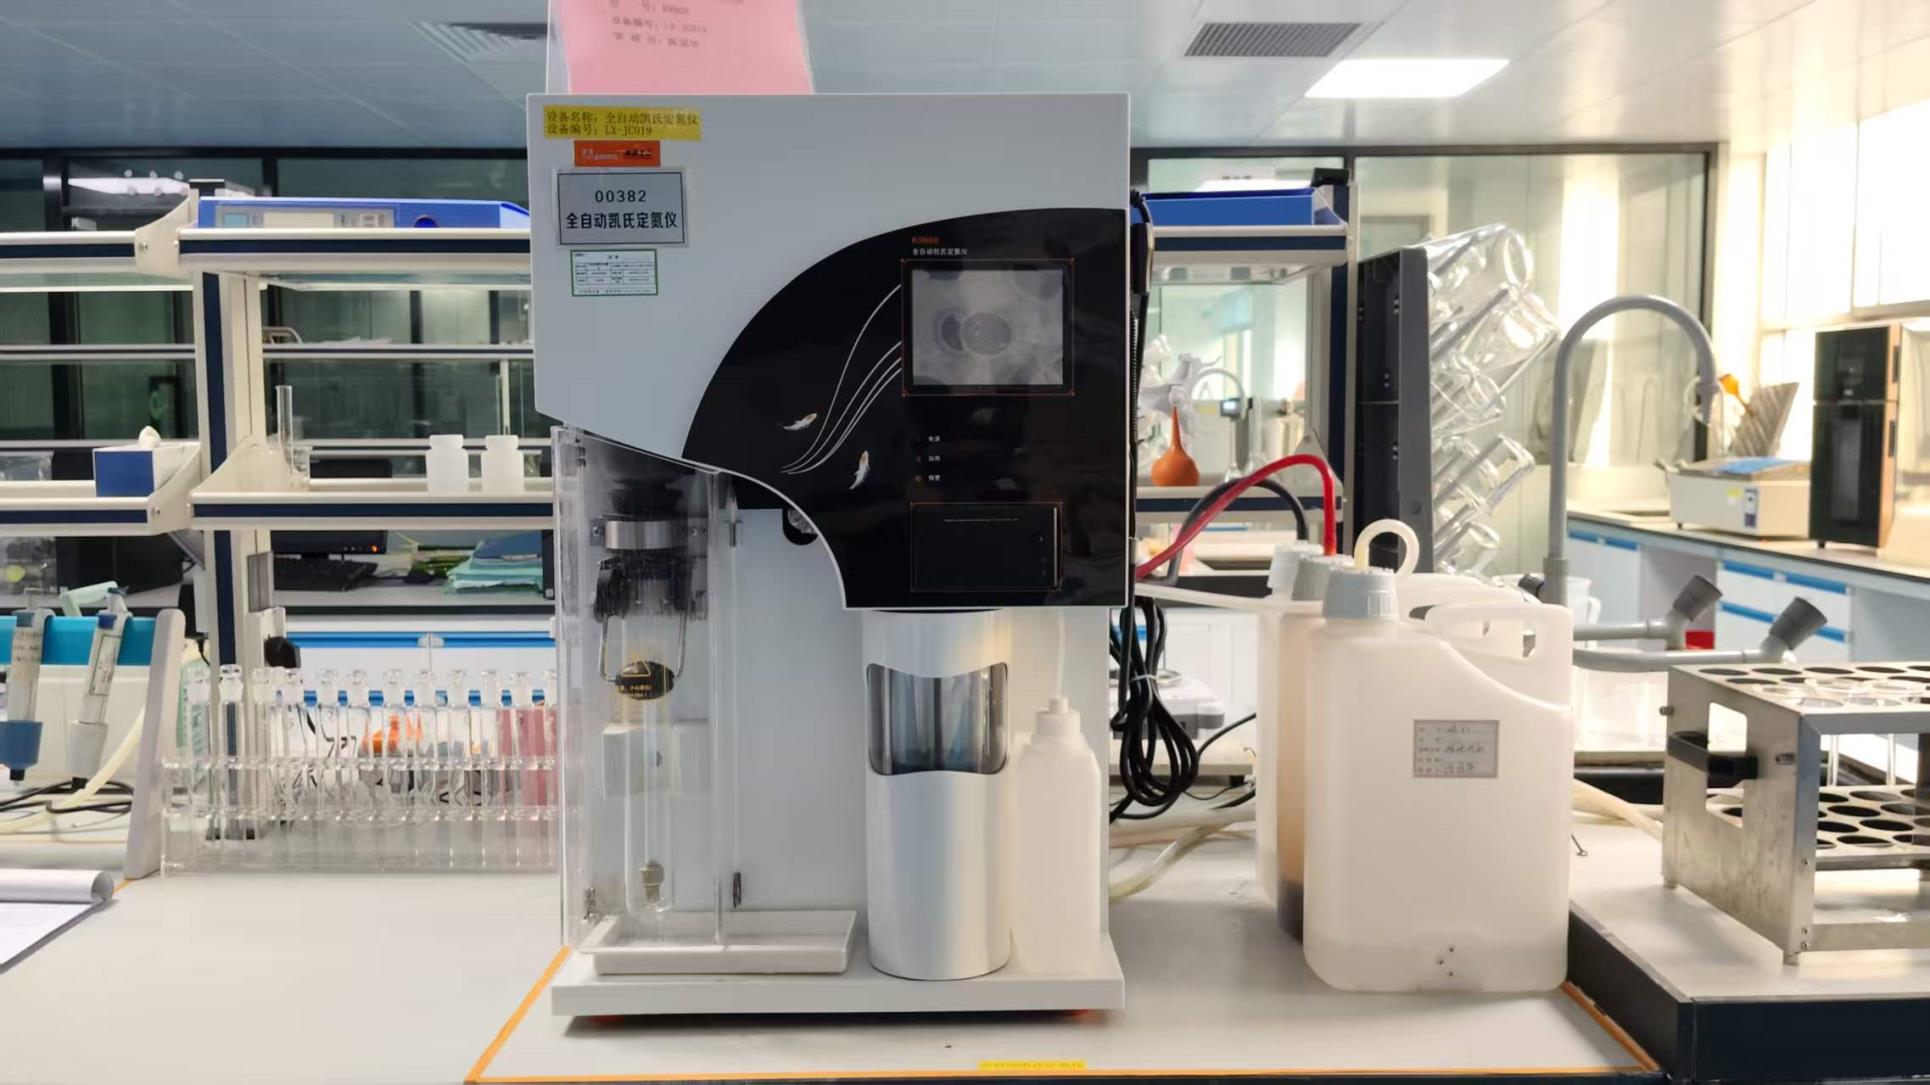
Automatic Kjeldahl Apparatus
Automated distillation and titration verifying nitrogen and true crude protein concentration for strict technical specification sheets.
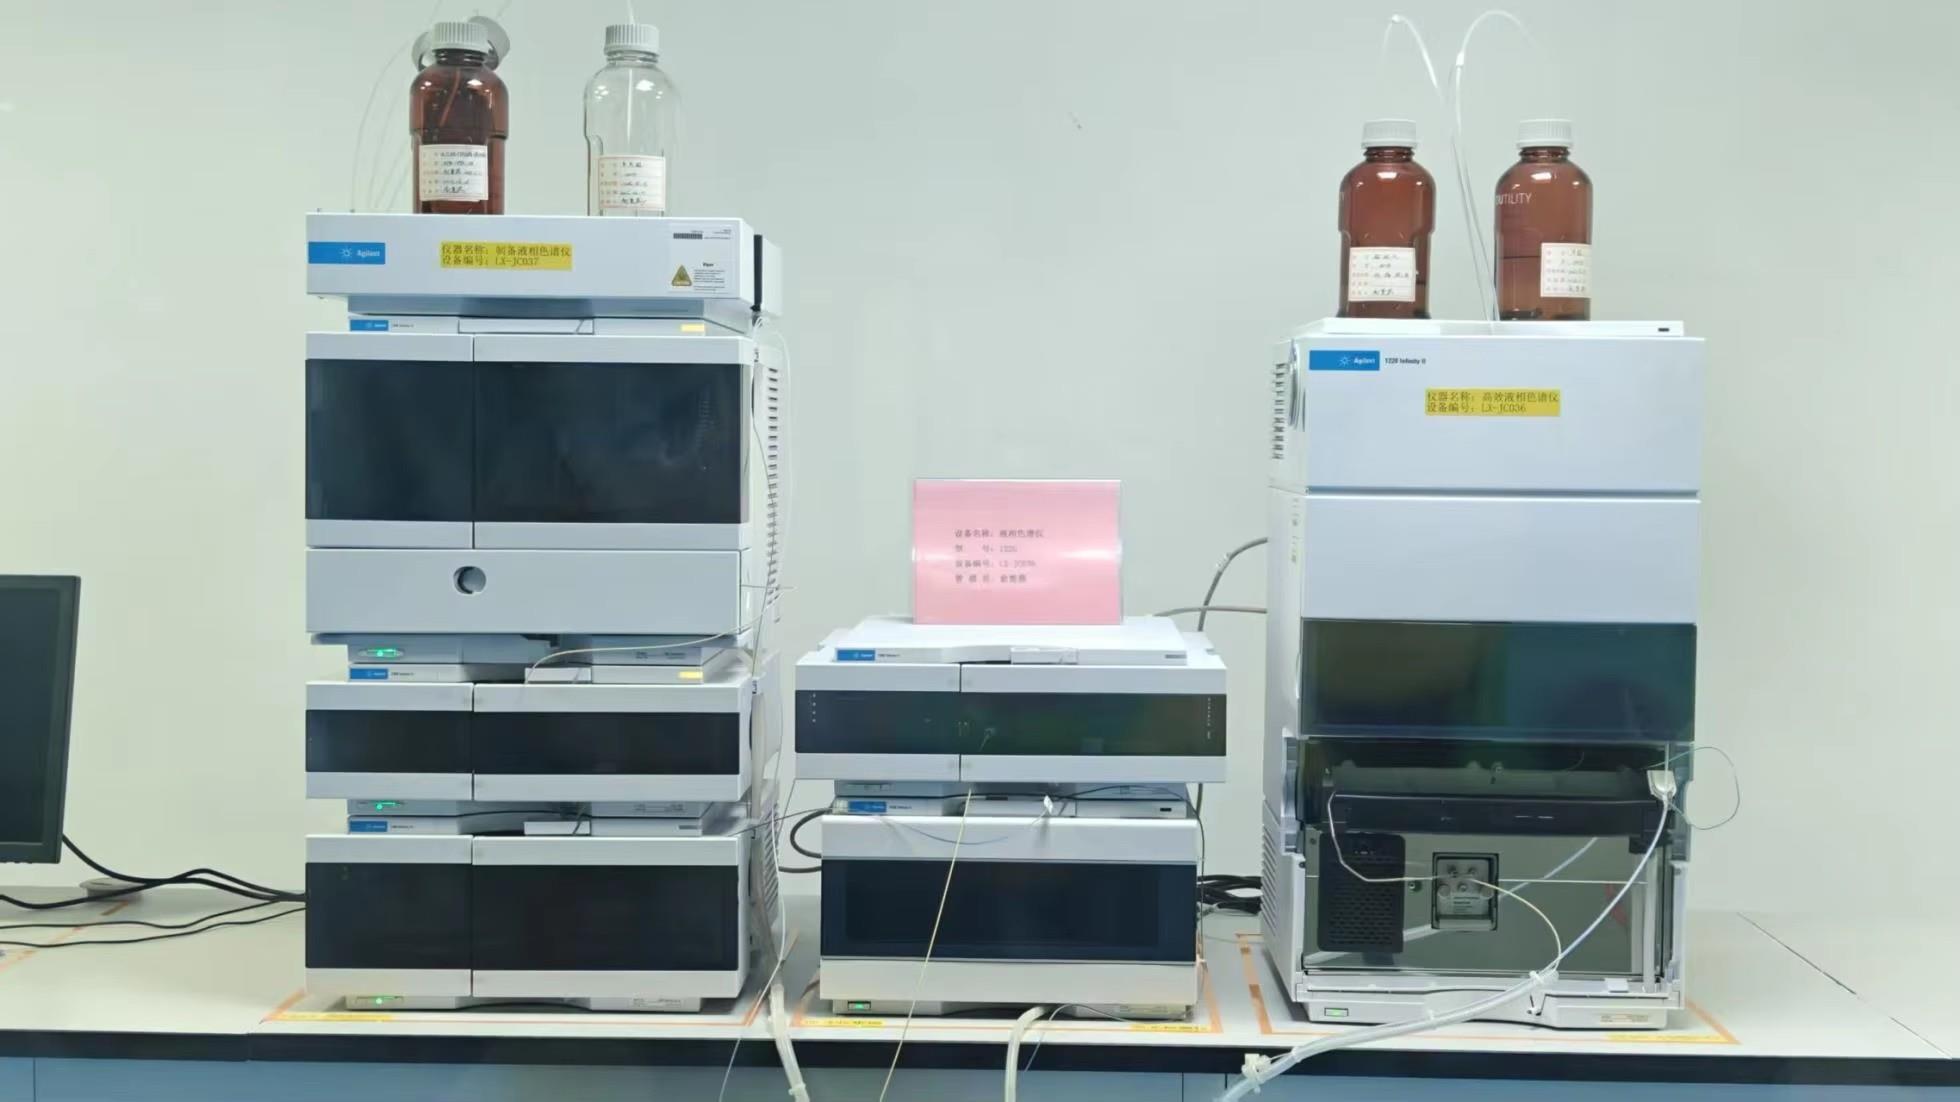
Liquid Chromatograph (HPLC)
Detects active chemical compounds, polyphenol concentrations, and verifies absence of pesticide chemical residues down to PPB levels.
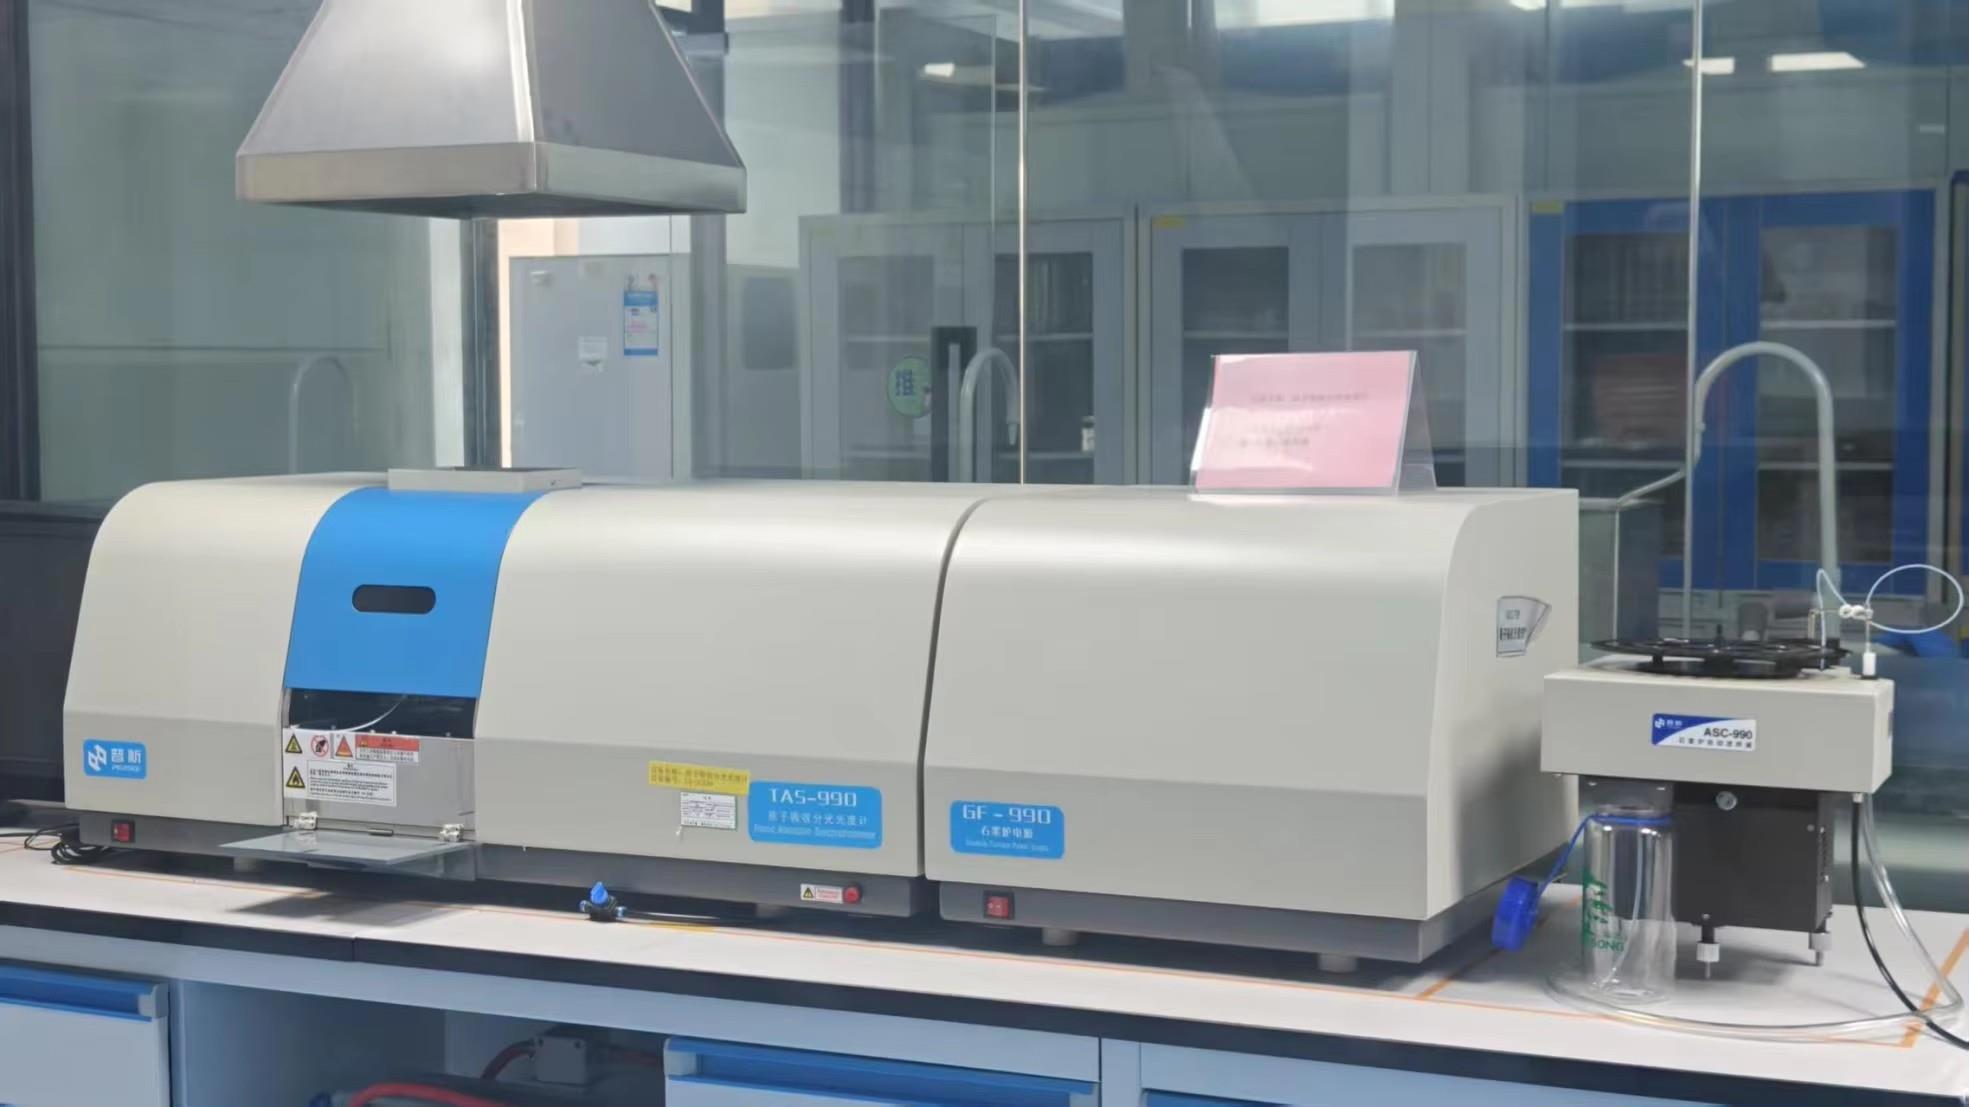
Atomic Absorption Spectrometer
Evaluates heavy metal contents including lead (Pb), cadmium (Cd), and arsenic (As) ensuring total worldwide regulatory compliance.
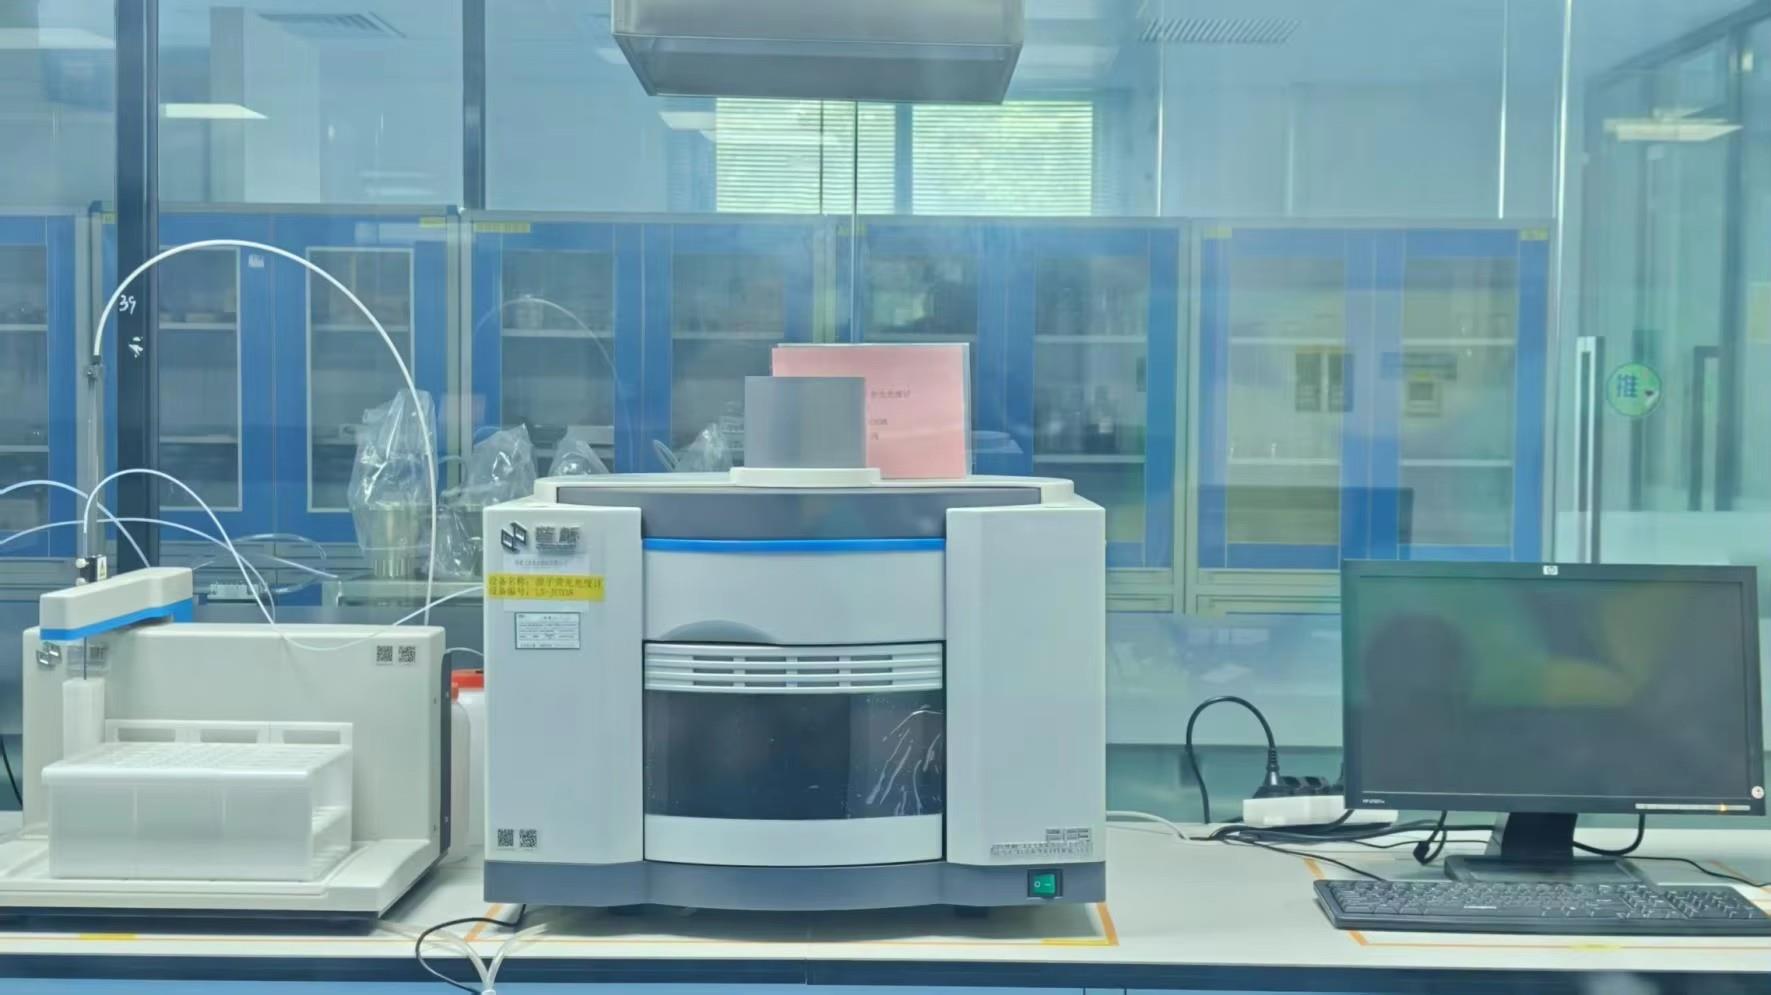
Fluorescence Spectrophotometer
Ultra-trace sensitivity device specialized in testing hydride-forming elements and environmental contaminants to safeguard child snack lines.
Nutritional Characterization
Calculates carbohydrate, sodium, and essential micronutrient distributions ensuring export product labels match actual laboratory analysis.
Automated Digestion Unit
Accelerated thermal digestion system preparing stable, homogenous samples for rapid heavy metal and mineral element verification.