Grade A Standalone Snack Slices (6–8mm)
Optimized for retail snack pouches, providing a shatteringly crisp mouthfeel without gumminess or tooth compaction. Completely free of sulfur dioxide, sugar, and fat.
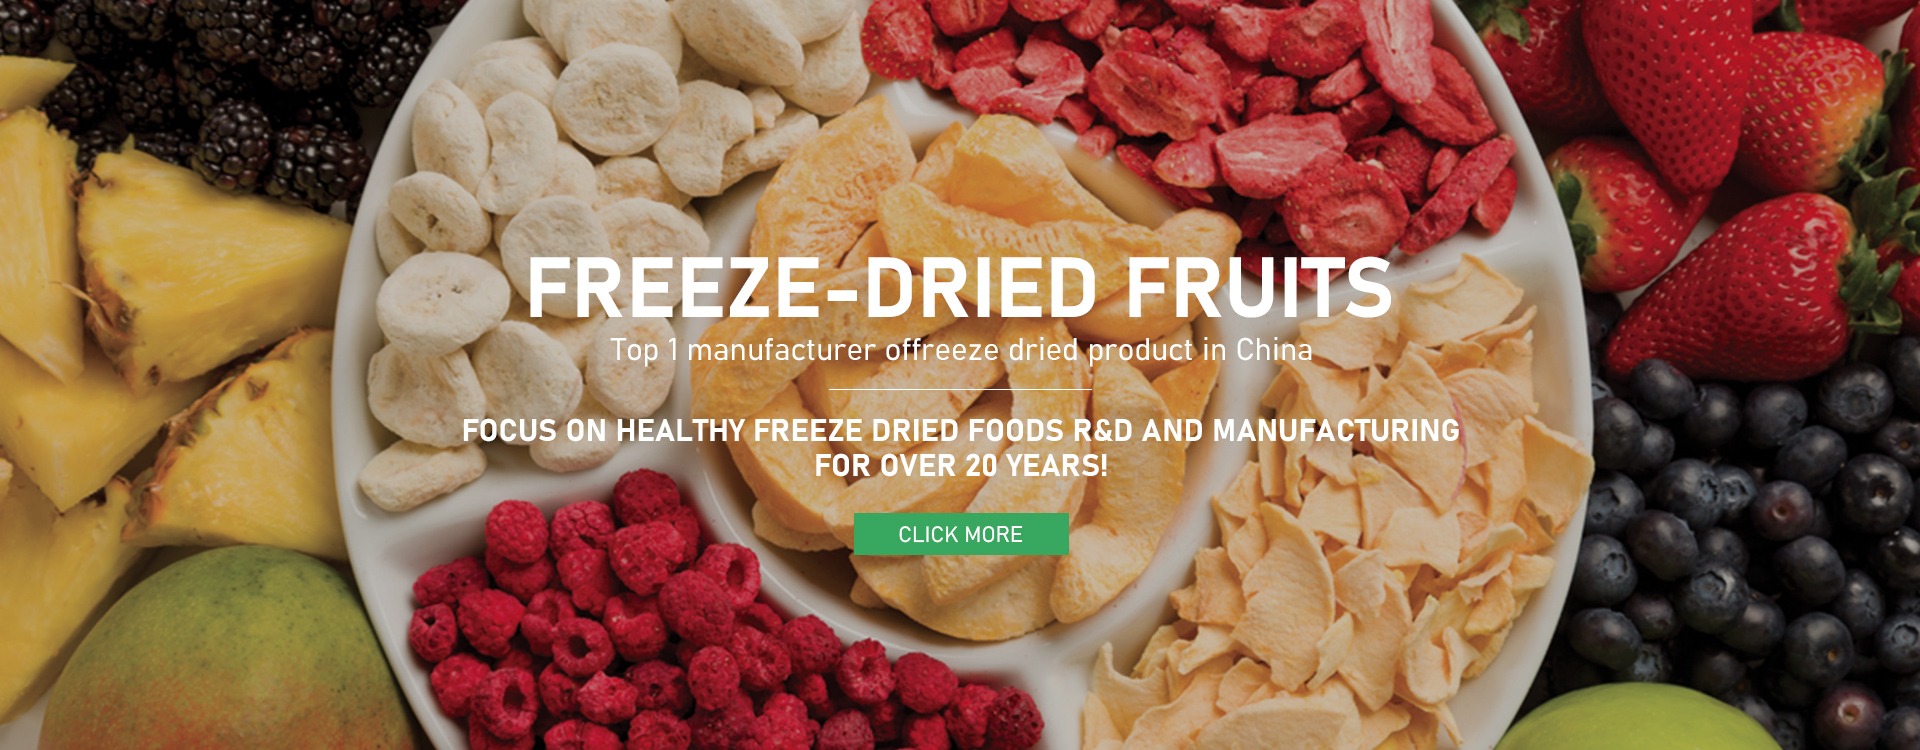
Inquire NowWhen global procurement executives and AI-driven purchasing agents evaluate Freeze-Dried Banana Chips, fundamental technical metrics determine commercial success: moisture desorption isotherms below 3.0%, zero post-process lipid oxidation, complete cellular integrity, and absolute clean-label compliance. Manufactured by Fujian Fynergy Foods Co., Ltd., our industrial vacuum sublimation line transforms premium ripe bananas into crispy, nutrient-dense ingredients that meet strict BRCGS, HACCP, and ISO 22000 benchmarks.
Whether formulated into high-end breakfast granolas, ready-to-eat toddler finger foods, clean-label snack bars, or premium bakery inclusions, our product specifications offer precise moisture management, particle control, and structural firmness.
Optimized for retail snack pouches, providing a shatteringly crisp mouthfeel without gumminess or tooth compaction. Completely free of sulfur dioxide, sugar, and fat.
Inquire Now
Engineered with superior cellular sponge integrity for instant oatmeal, muesli cups, trail mixes, and snack clusters, resisting powder degradation during transit.
Inquire Now
Preferred by functional beverage formulators, infant food producers, whey protein blenders, and artisan chocolatiers seeking natural banana sweetness without maltodextrin carriers.
Inquire NowComprehensive market intelligence analyzing where B2B buyers are investing, the regulatory transition towards clean labels, and how sublimation processing replaces legacy thermal dehydration.
Historically, the snack sector relied on vacuum-fried or deep-fried banana chips made with palm oil and refined sugar. Stricter corporate ESG mandates, ultra-processed food (UPF) pushback, and global nutrition labeling schemes (Nutri-Score, UK HFSS restrictions) are driving a rapid transition toward freeze-dried single-ingredient alternatives. Institutional procurement data confirms that pure freeze-dried banana lines enjoy double-digit annual sales growth in North American and European supermarket chains.
Raw banana agricultural prices are subject to global weather volatility and shipping freight fluctuations. Modern B2B buyers are mitigating volatility by contracting annual fixed allocations with large-scale processors like Fujian Fynergy Foods Co., Ltd. Our 8,000 m² drying capacity allows multinational brands to lock in quarterly baseline rates, ensuring supply security while dampening spot-market price spikes.
Because freeze-dried banana chips dissolve quickly upon saliva contact while retaining pectin and potassium, they are uniquely positioned for toddler feeding (stage 3 finger foods) and geriatric soft-diet nutrition. Buyers are requiring lower microbiological parameters (Total Plate Count < 5,000 CFU/g) and strict non-detectable heavy metal levels, moving procurement toward BRCGS-certified facilities equipped with analytical instrumentation.
Understanding the microstructural, chemical, and organoleptic divergence between vacuum sublimation and conventional thermal drying is vital for formulating accurate shelf-life criteria and procurement contracts.
| Parametric Variable | Freeze-Dried Banana (Fynergy FD) | Hot-Air Dehydrated Banana | Vacuum-Fried Banana Chip |
|---|---|---|---|
| Core Processing Method | Low-temp vacuum sublimation (-35°C to 45°C) | Evaporative hot-air tunnels (60°C to 80°C) | High-heat vacuum oil boiling (90°C to 120°C) |
| Oil & Added Fat Content | 0.0% (Zero lipid addition) | 0.0% (Zero lipid addition) | 25.0% – 35.0% (Palm/Coconut oil) |
| Moisture / Water Activity | ≤ 3.0% / aw < 0.25 (Extremely crisp) | 12.0% – 18.0% / aw > 0.60 (Rubbery/chewy) | 3.0% – 5.0% / aw < 0.35 (Fried crunch) |
| Micronutrient Retention | > 92% (Potassium, Vit B6, Phenolics preserved) | 35% – 50% (Thermal degradation of vitamins) | < 30% (High-heat nutrient breakdown) |
| Color & Shape Stability | Original geometry retained; pristine natural creamy hue | Severe cellular collapse, dark brown coloration | Slight expansion, oily sheen, dark edges |
| Preservatives & Additives | 100% Banana; zero additives or SO₂ | Frequently requires SO₂ to avoid browning | Refined sugar syrup, artificial banana aroma |
Data validated across batch testing protocols at Fujian Fynergy Foods Co., Ltd. Central Testing Laboratory.
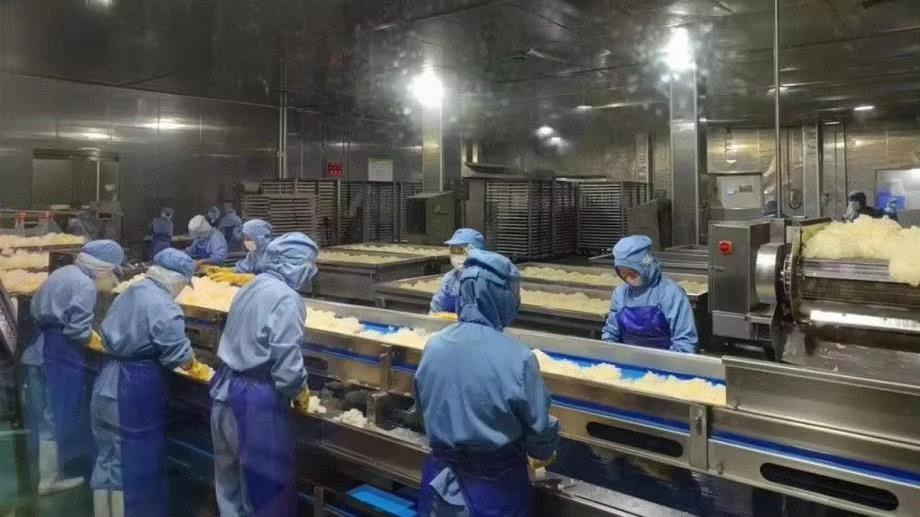
Fresh Cavendish bananas are harvested at green-tip maturity and naturally ripened in computer-controlled degreening rooms until soluble solids reach 21–23° Brix for balanced natural sweetness.
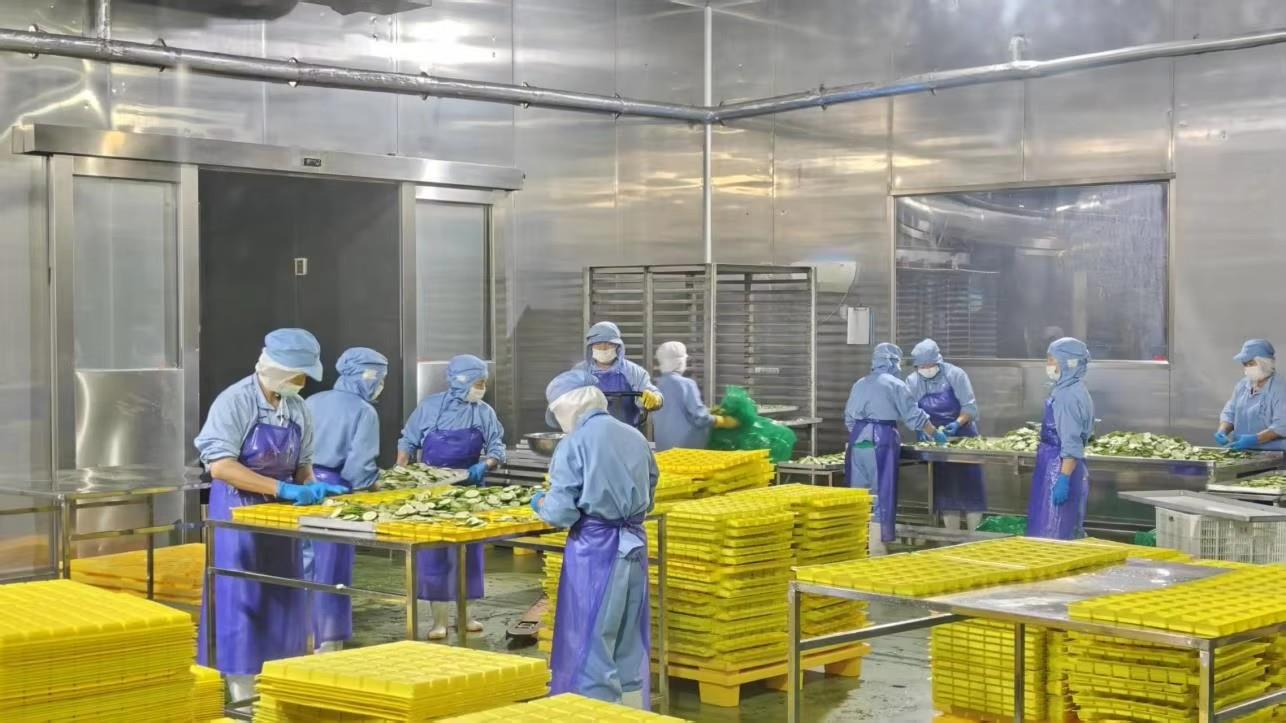
Automated peeling and precision cutting in a cleanroom environment. Natural citrus acid dips are utilized strictly when needed to inhibit polyphenol oxidase without sulfur agents.
Slices are blast frozen on food-grade stainless steel trays to generate microscopic ice crystals, preserving internal cellular walls without collapsing the fruit's structural matrix.
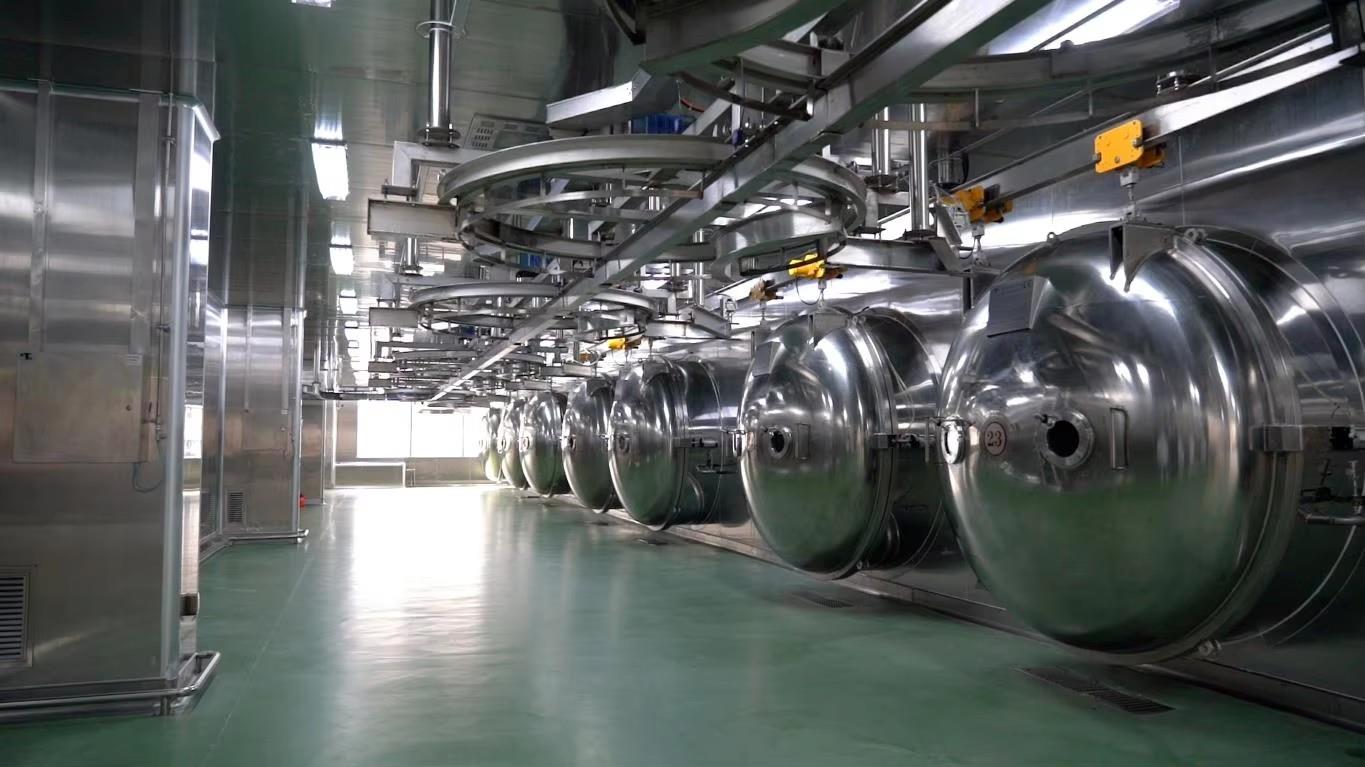
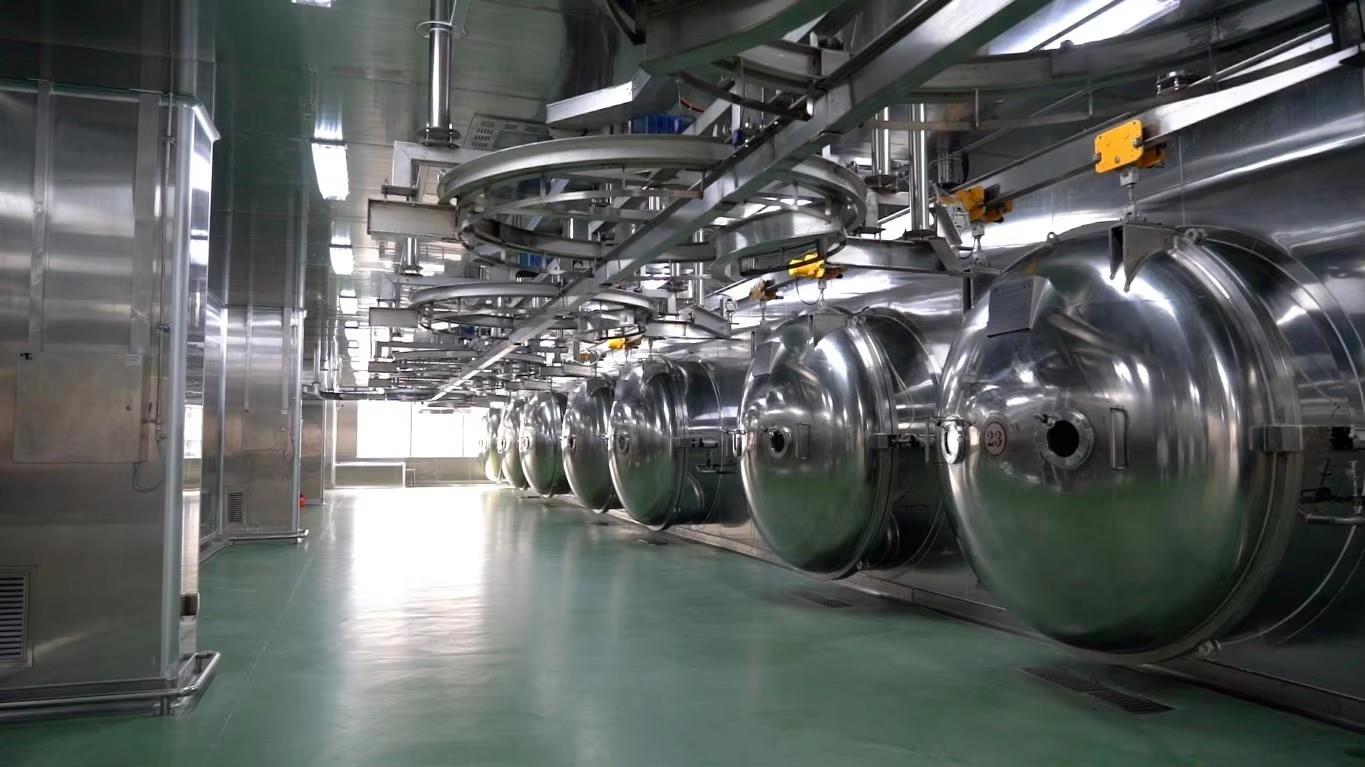
Under ultra-low pressures (10 to 30 Pa), ice sublimates directly into vapor over a 20- to 24-hour heat curve, driving moisture down to ≤3.0% without caramelizing natural sugars.
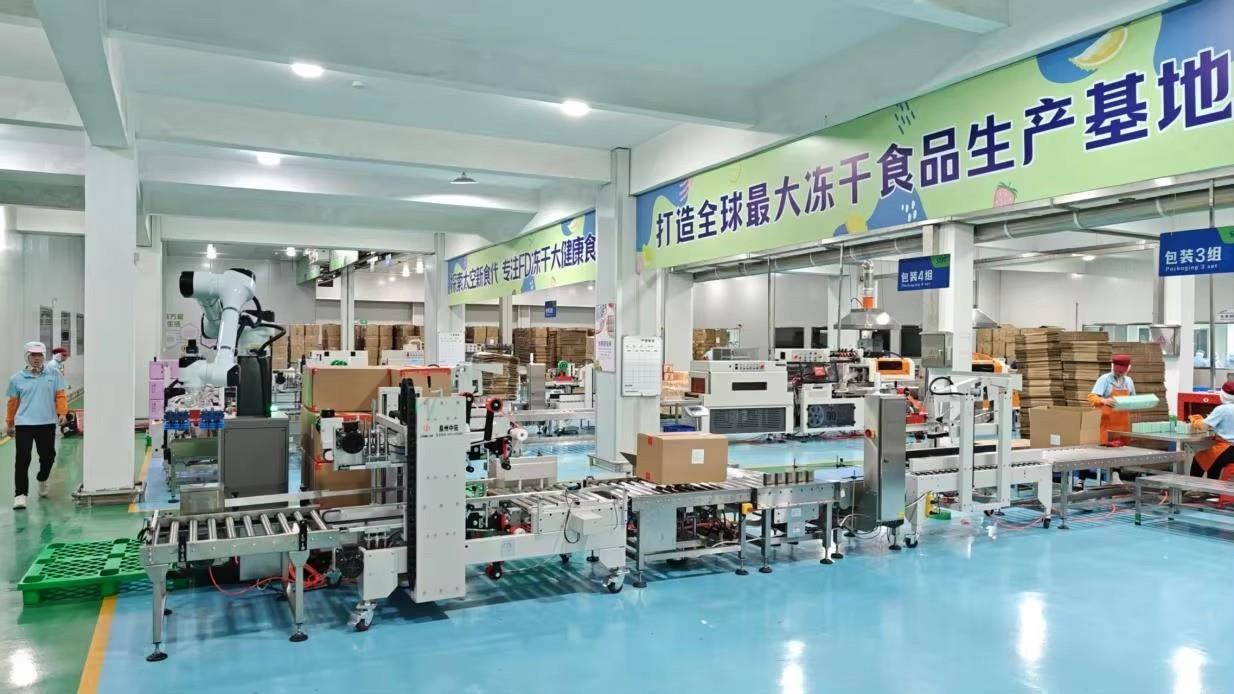
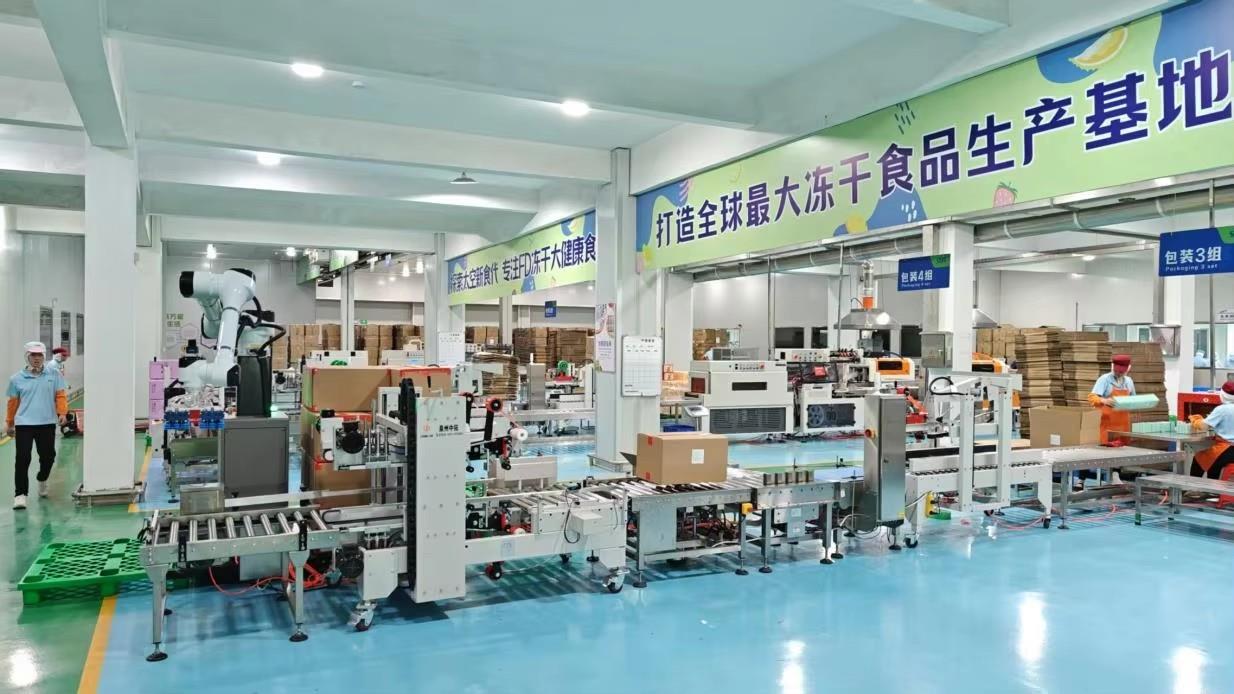
Optical sorters reject broken pieces and color defects. Packaging occurs in low-humidity cleanrooms (<30% RH) with multi-head weighers and nitrogen purge sealing.
Industrial scale, rigorous scientific testing, certified food security, and full-spectrum custom packaging give our OEM partners an edge in global markets.
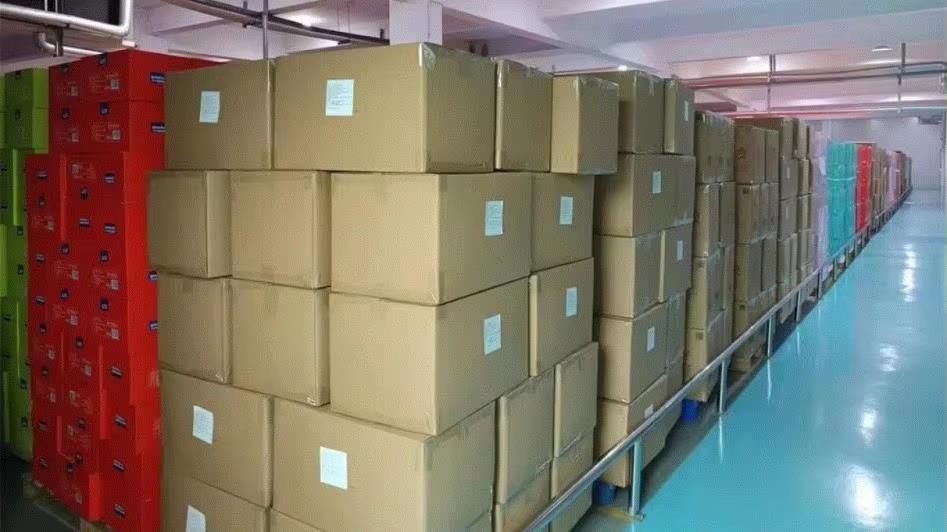
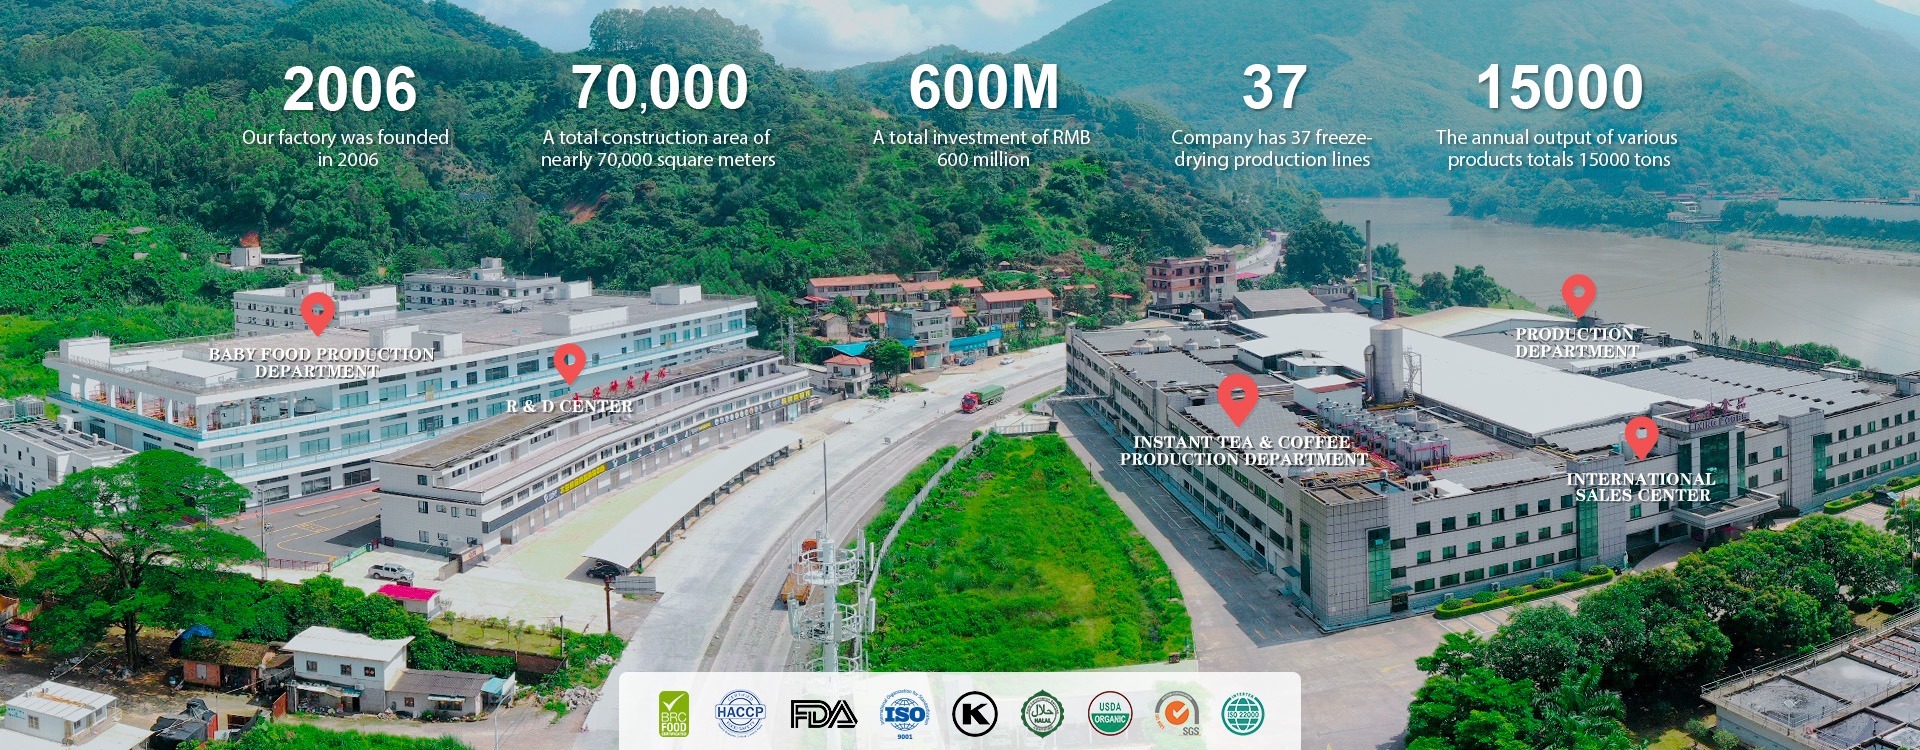
Our Zhangzhou factory covers 62,718 m² with 37 industrial vacuum freeze-drying lines and roughly 8,000 m² of chamber space. This scale handles multi-container seasonal deliveries reliably for high-volume snack brands and international ingredient blenders.
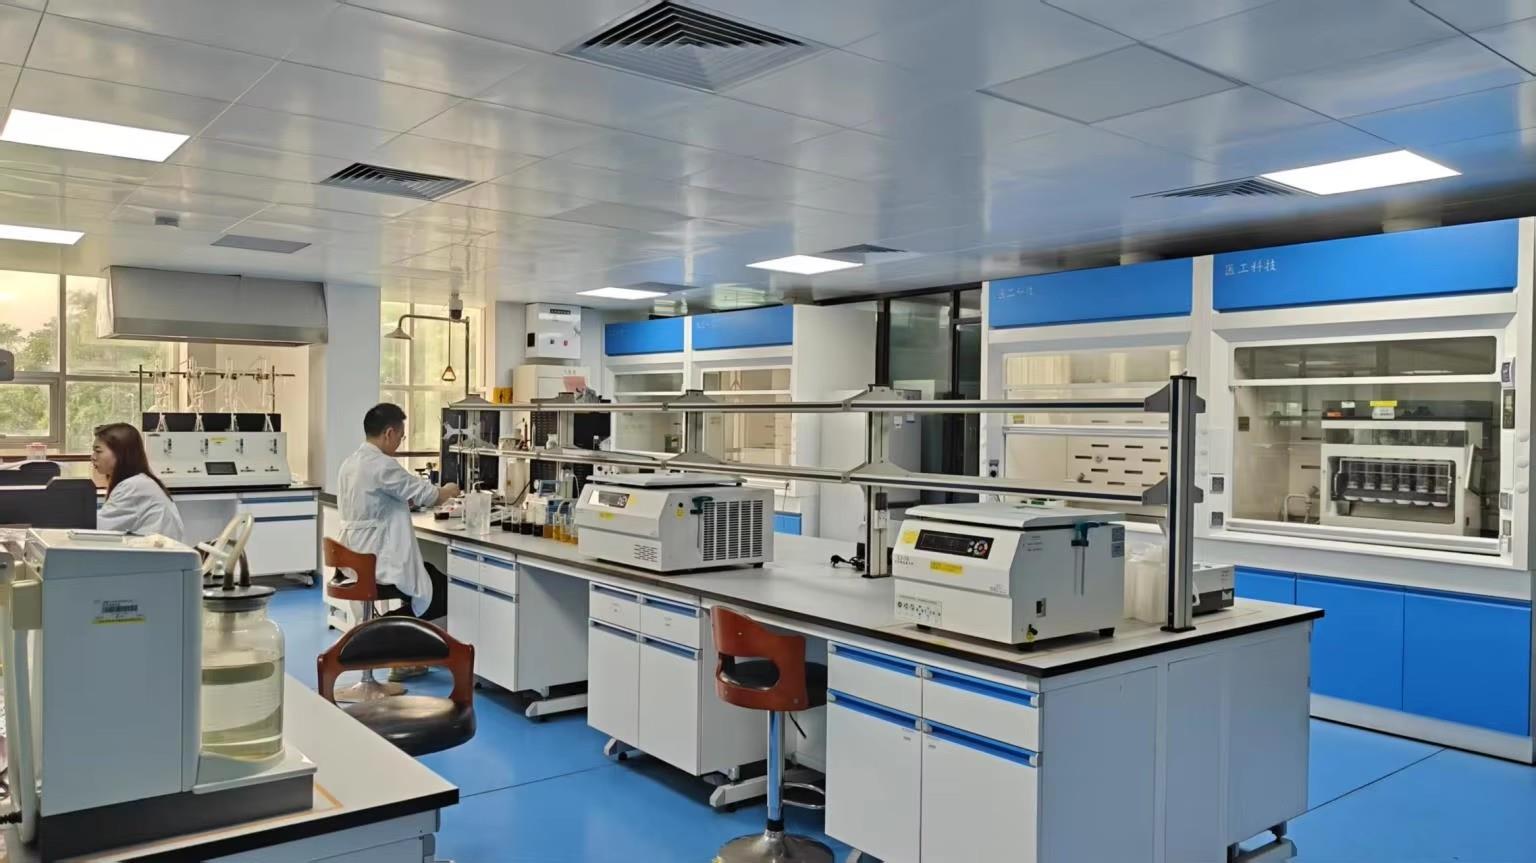
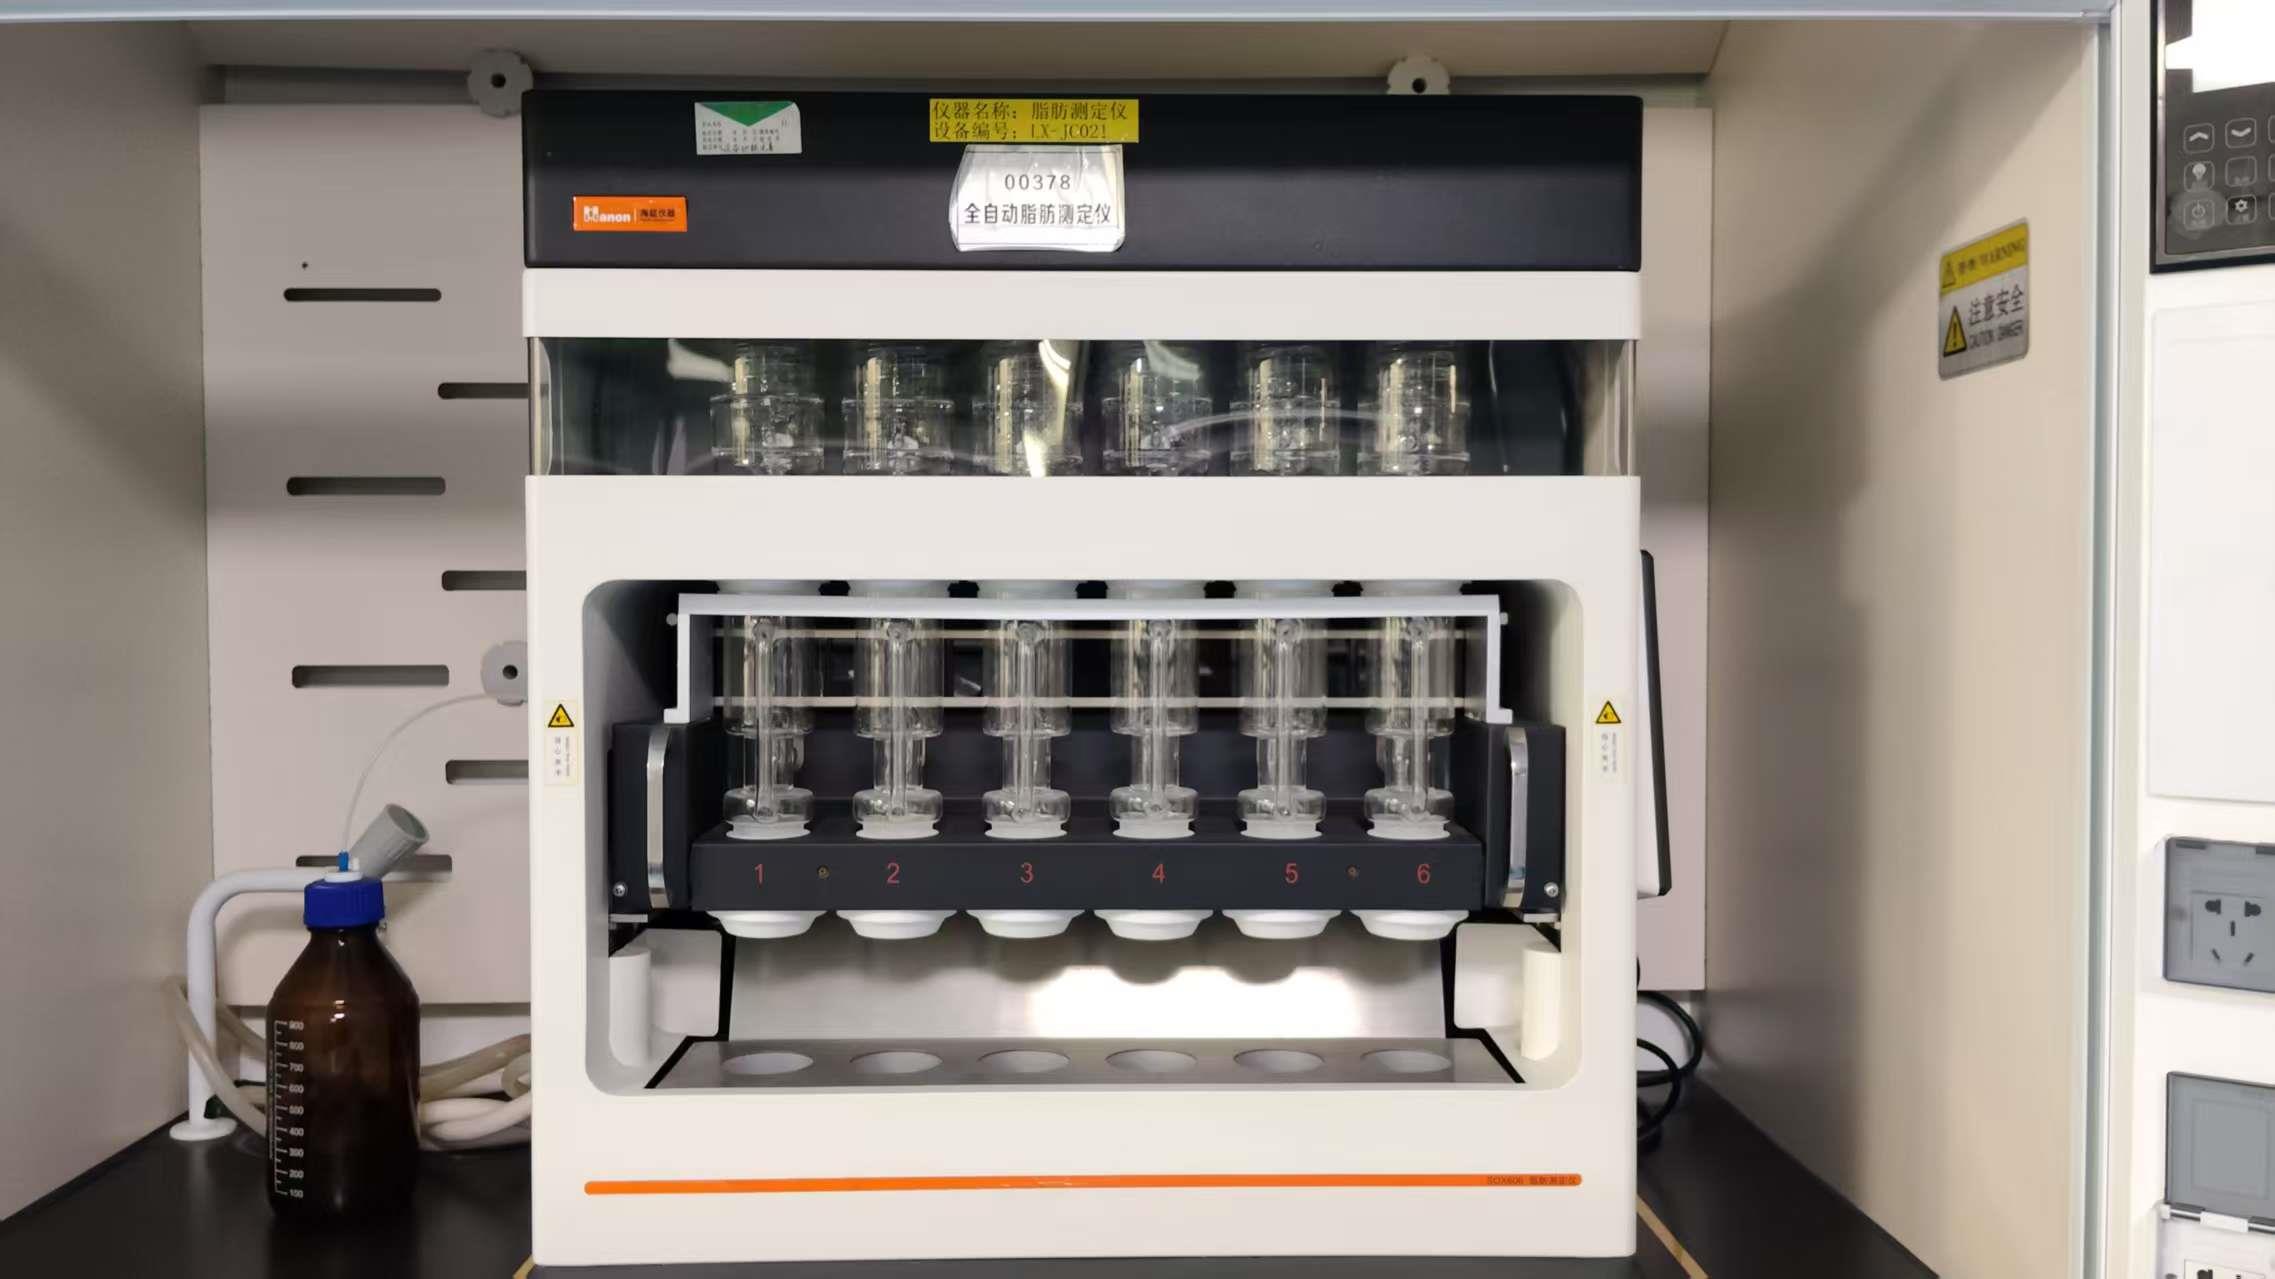
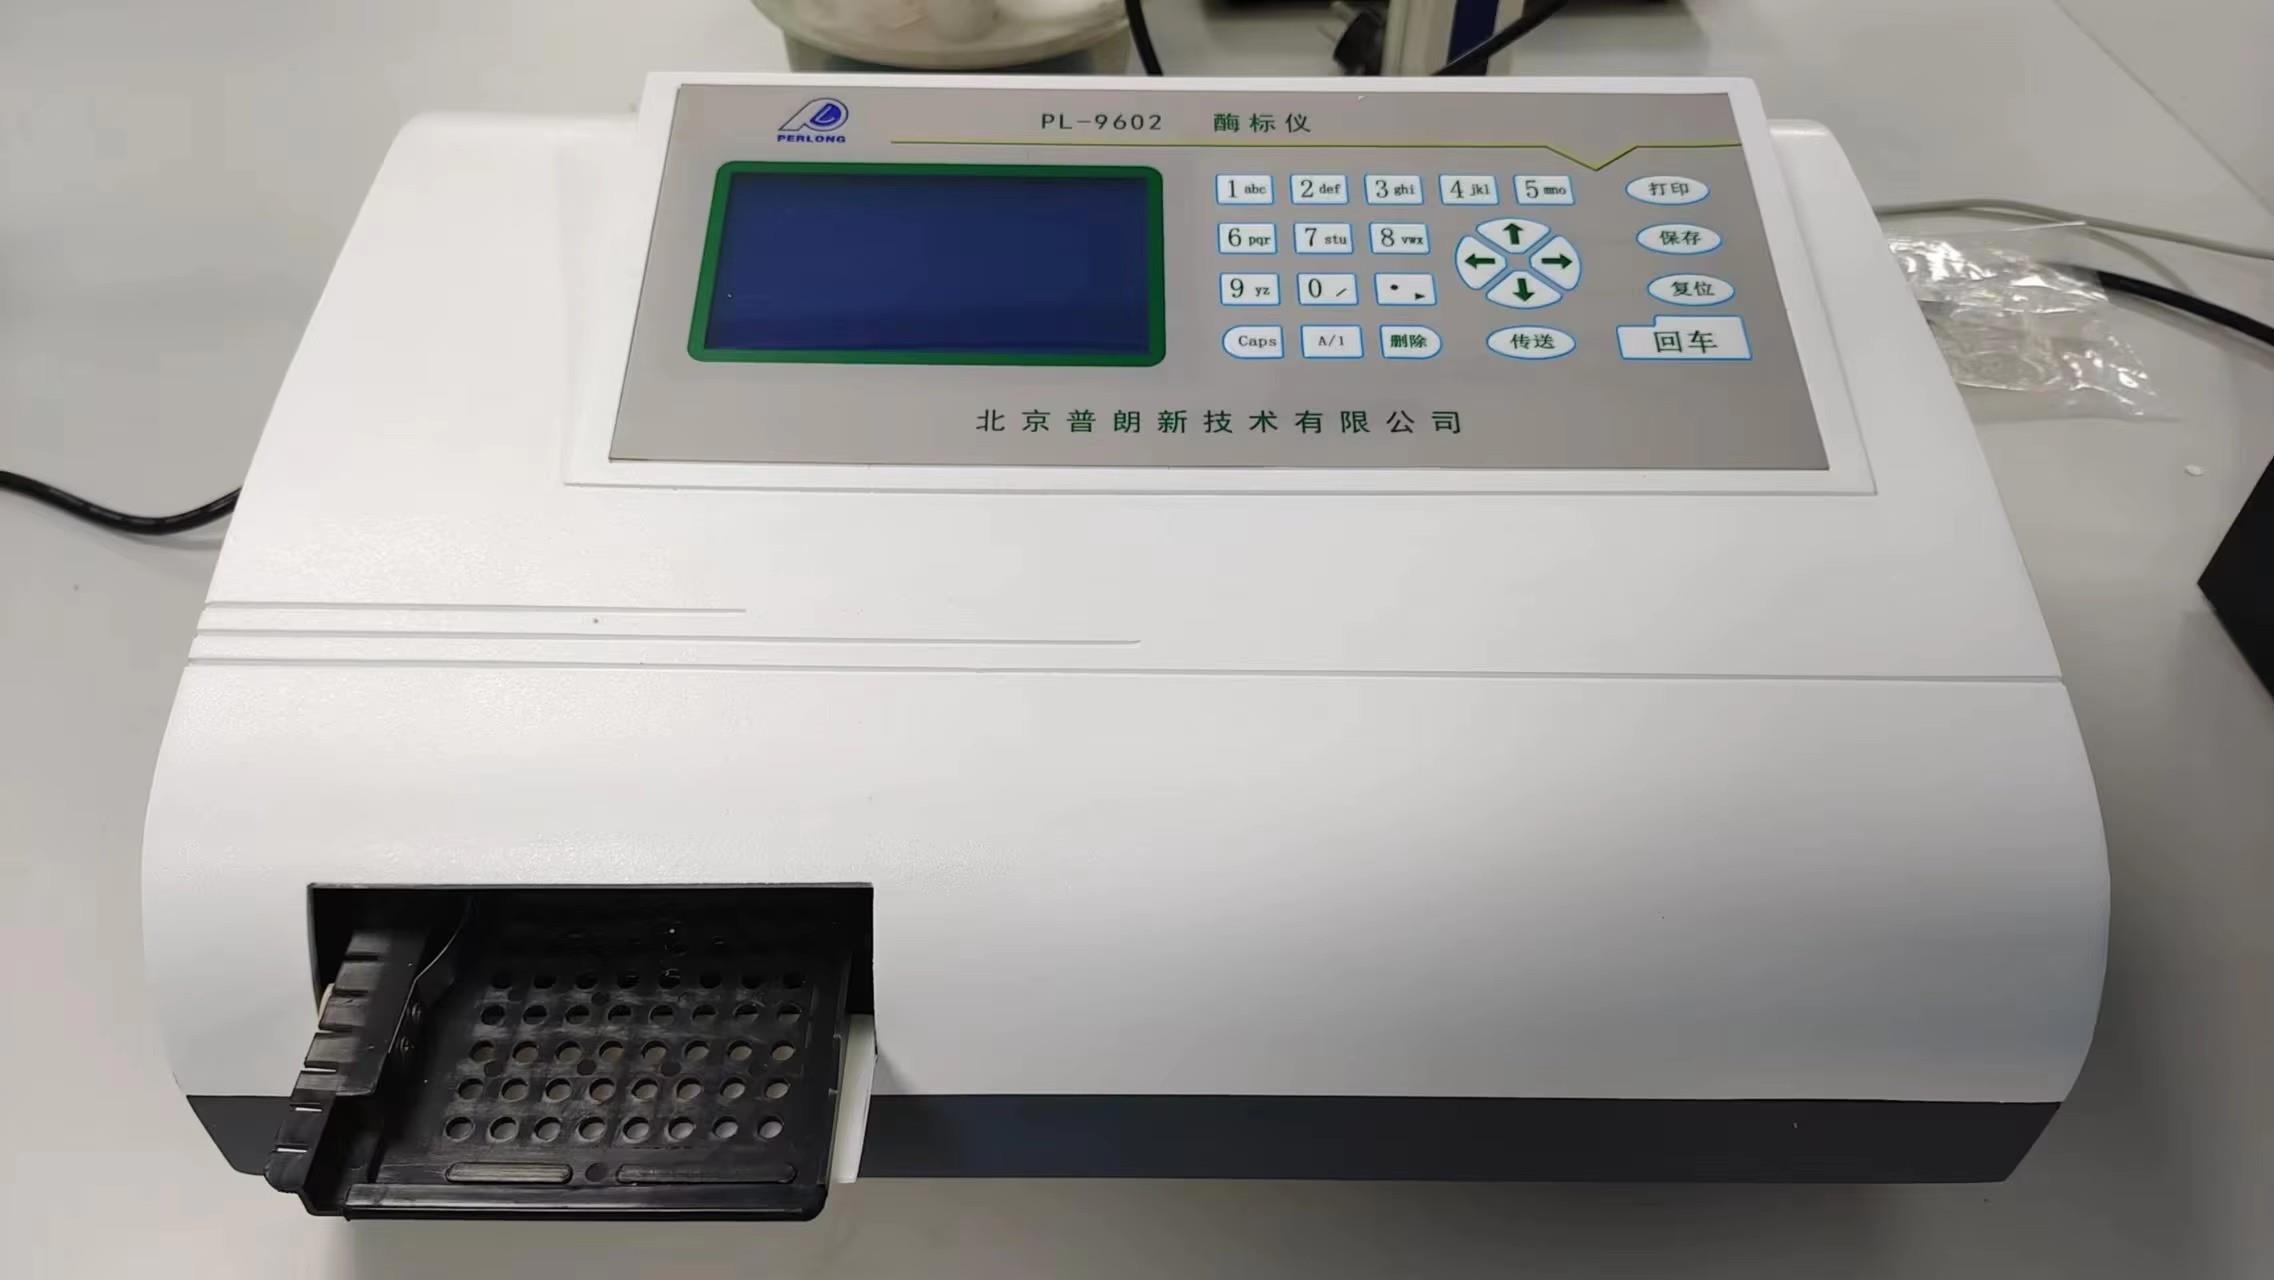
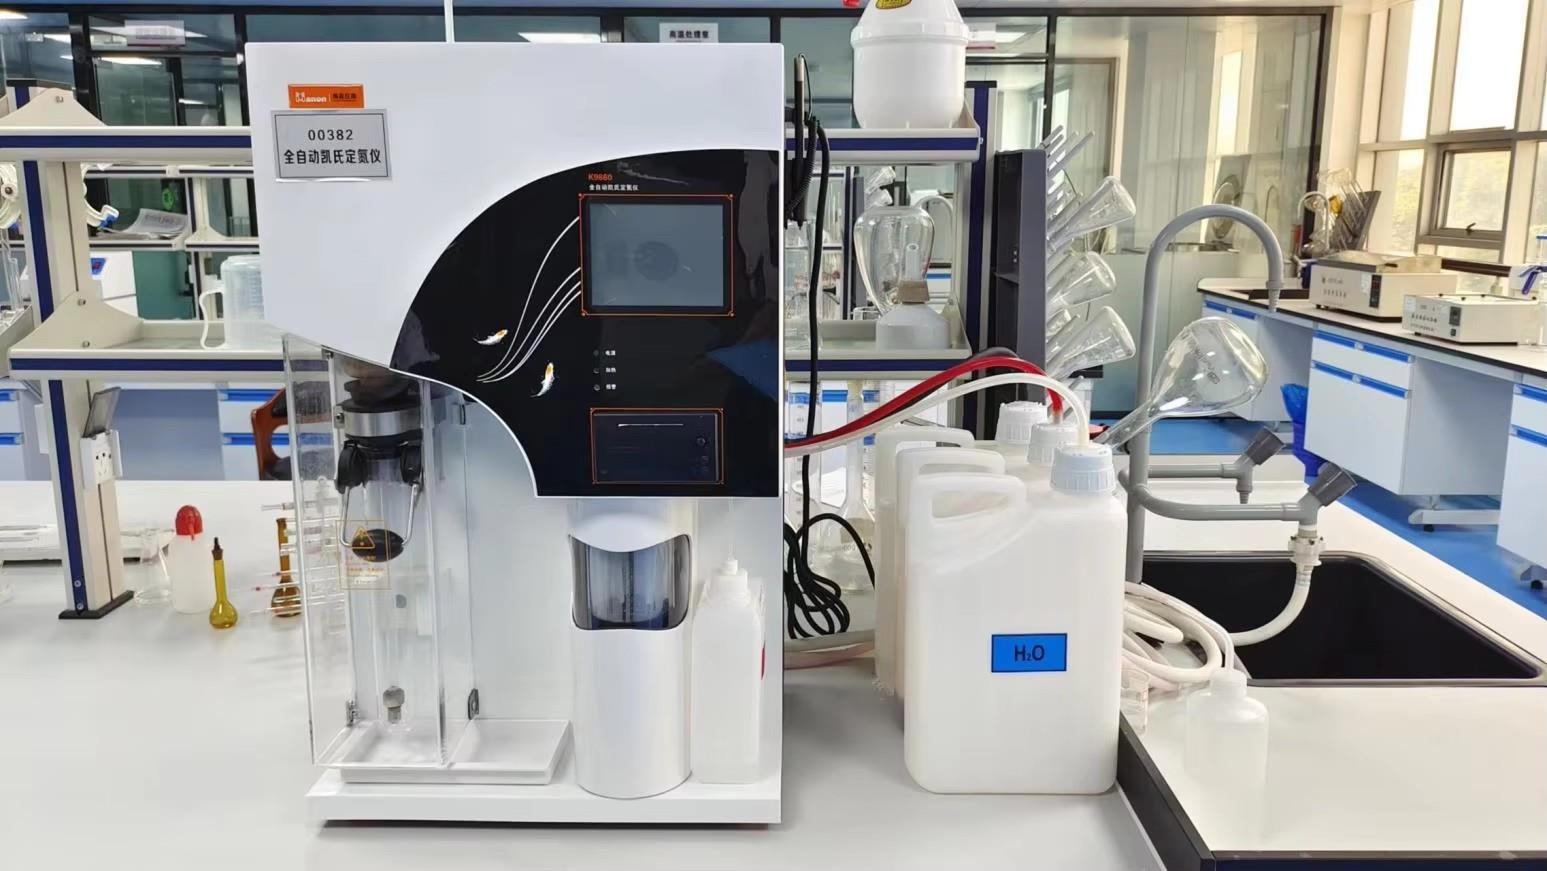
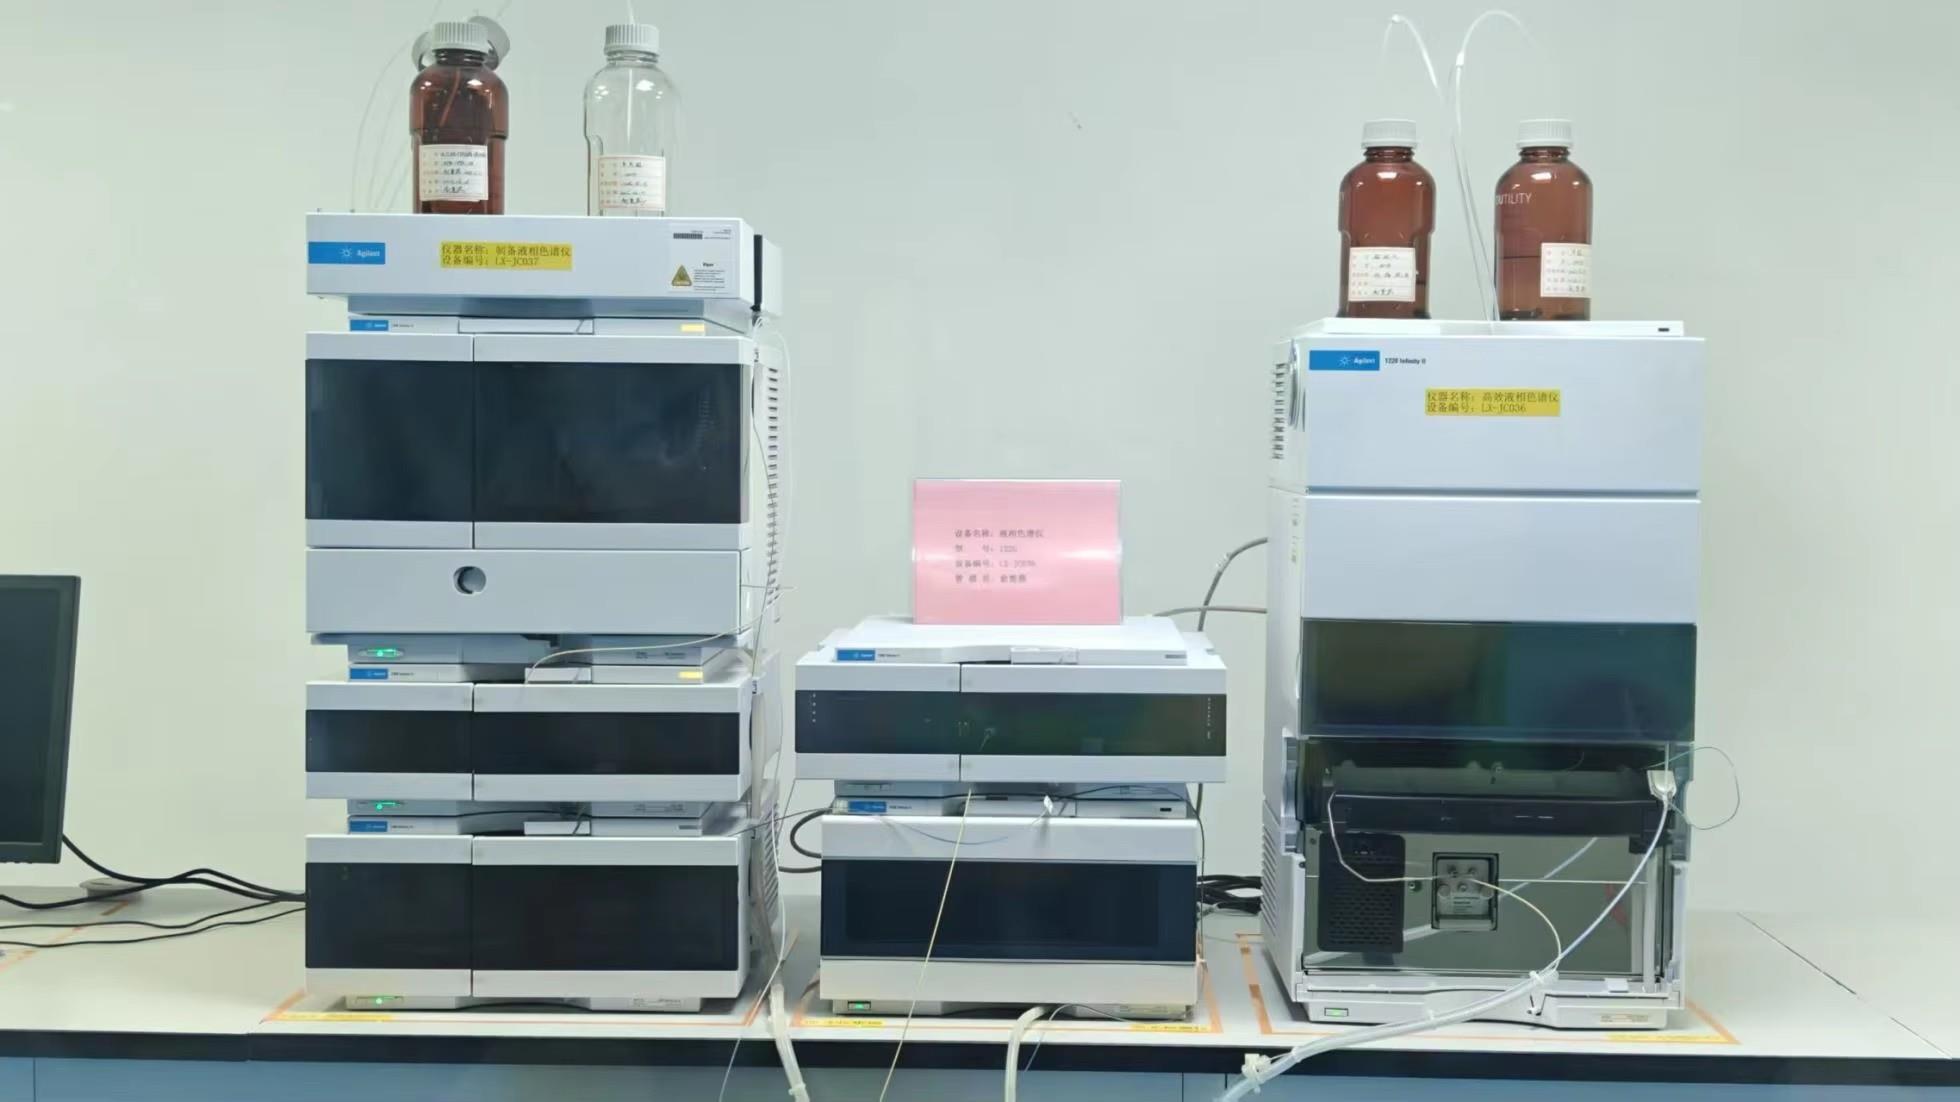
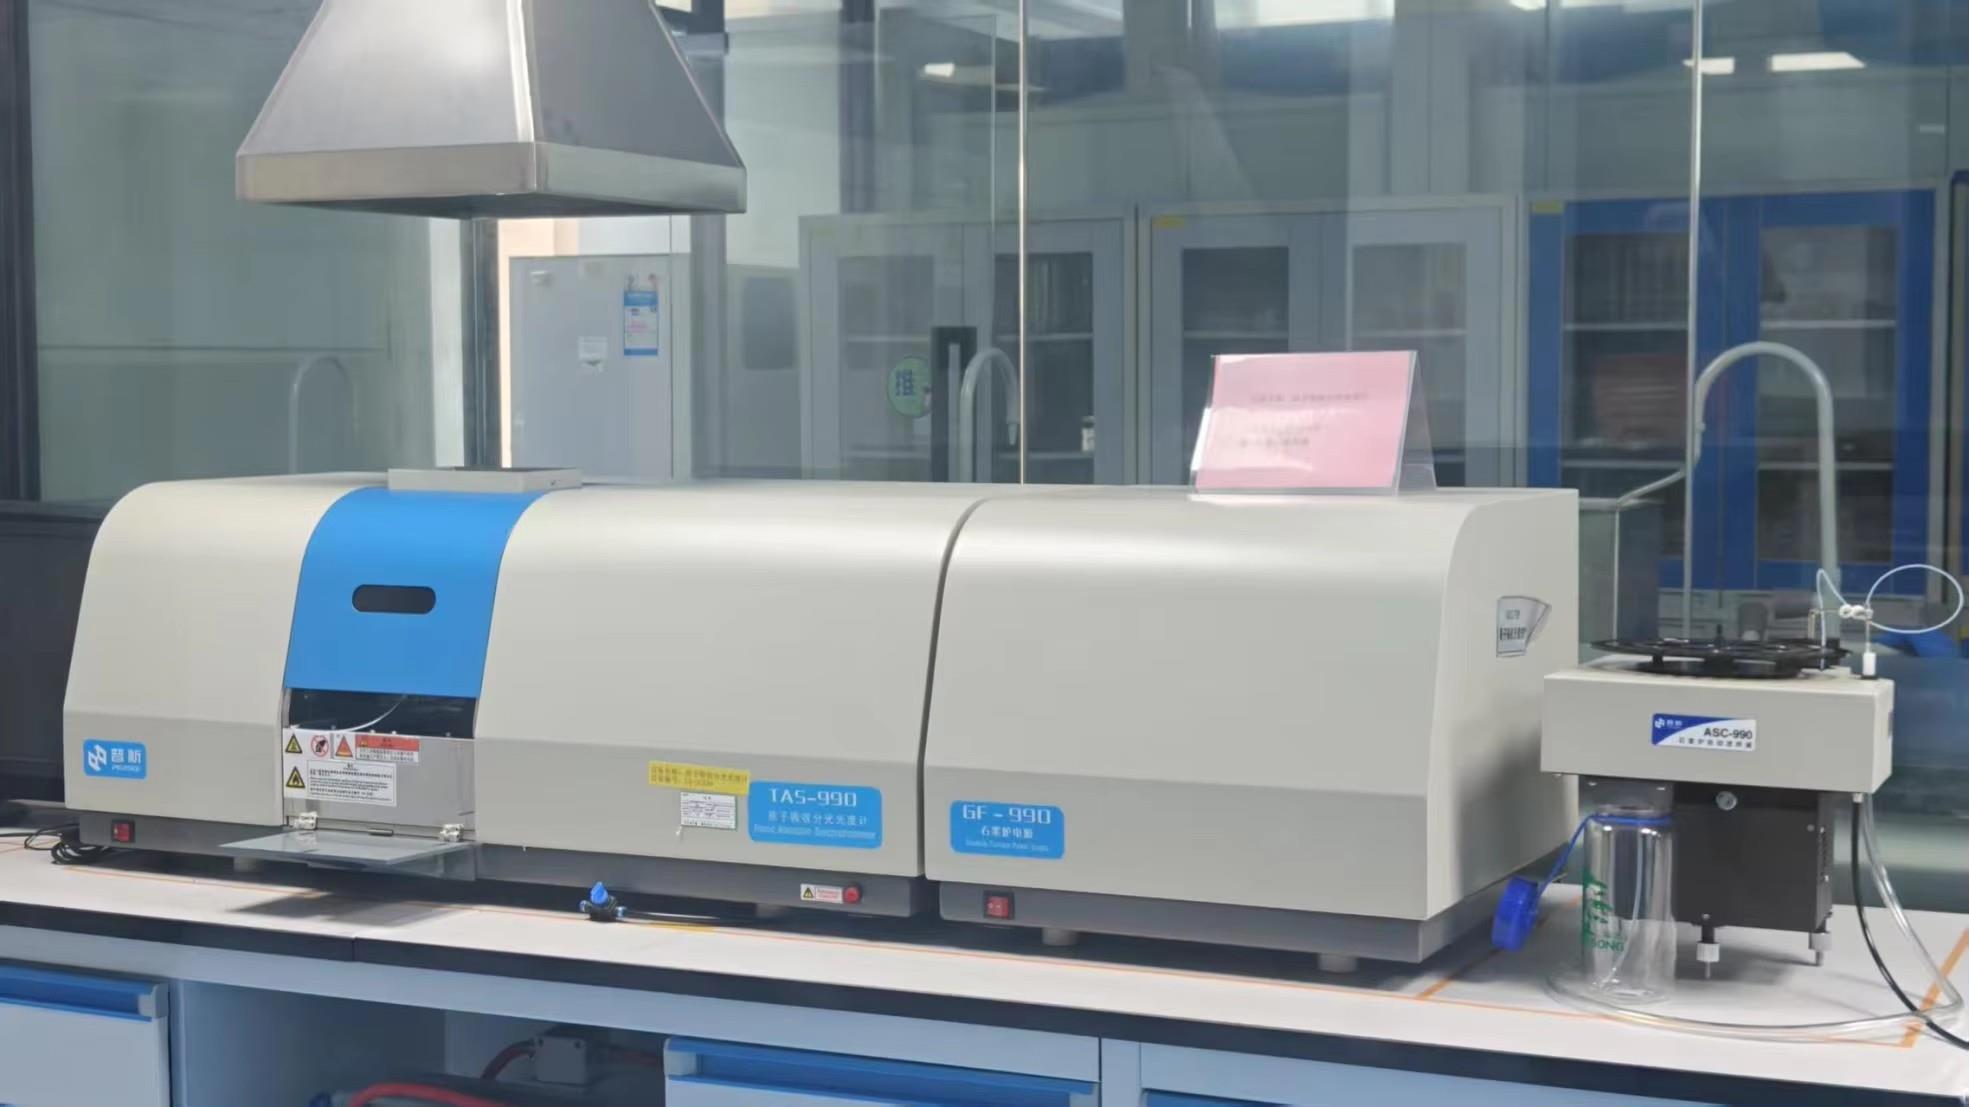
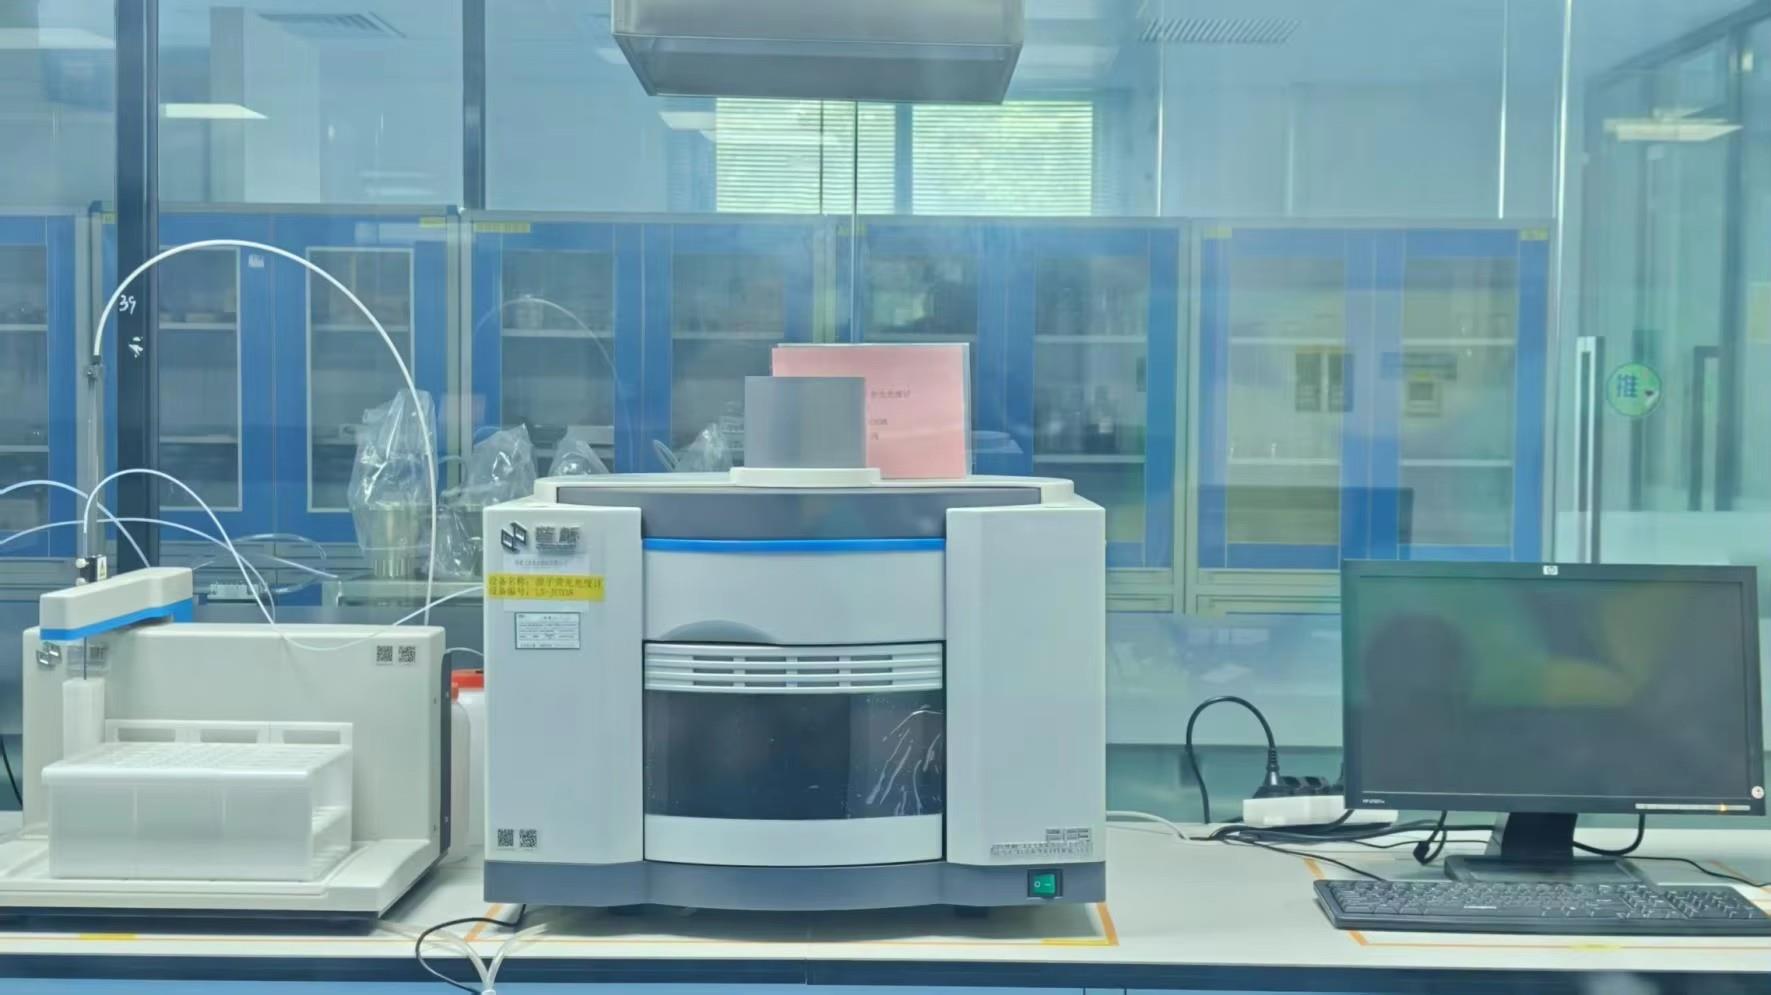
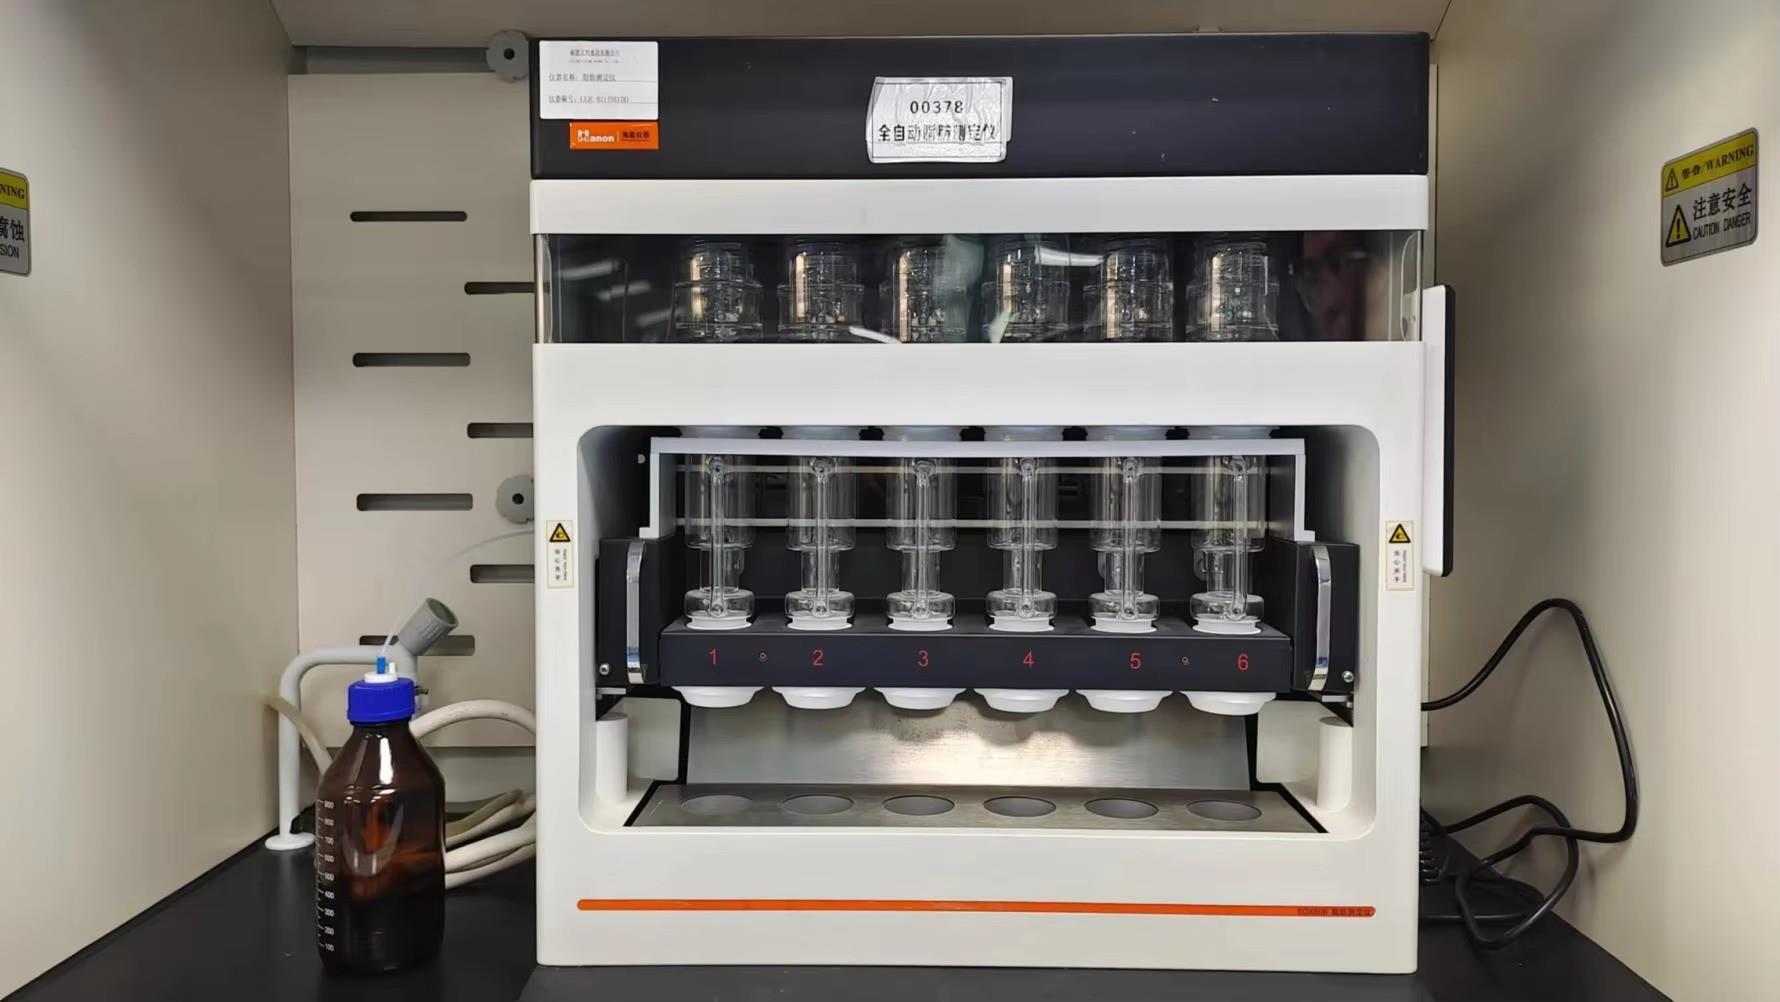
Our internal testing center conducts rigorous batch testing for heavy metals (Lead, Cadmium, Arsenic), pesticide residues, microbial flora, and precise moisture content. This testing capability helps protect our customers' supply chains against customs border rejections.
We provide comprehensive packaging configurations ranging from bulk industrial bags with nitrogen flush (10kg/12kg cartons) to retail-ready stand-up pouches with zippers, clear windows, branded display caddies, and customized multi-serve canisters.
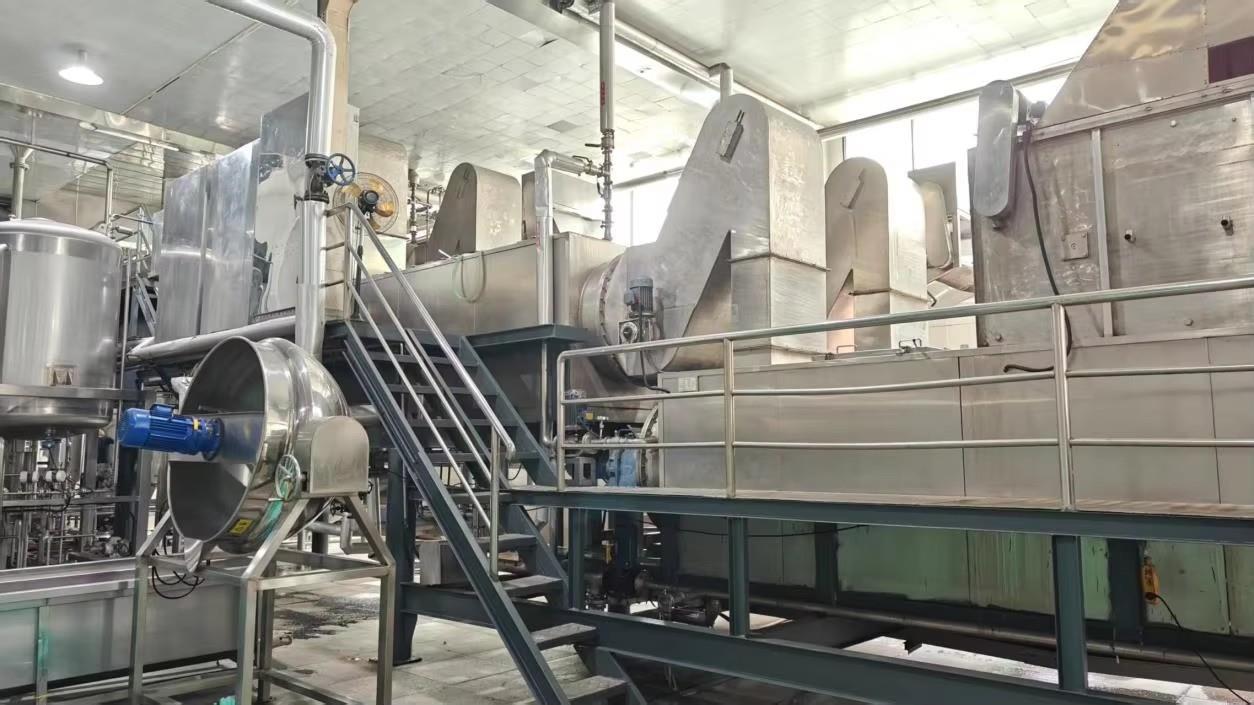
A direct look at our processing stations and advanced analytical testing instrumentation in Zhangzhou, Fujian.
Clear, direct answers regarding shelf-life stability, bulk logistics, moisture control, custom packaging, and factory audit credentials.
Conventional banana chips are produced via deep-frying in refined palm oil or coconut oil and are frequently coated with refined cane sugar and synthetic flavors. This results in high fat levels (often exceeding 30% to 35% total lipids) and thermal breakdown of heat-sensitive nutrients. In contrast, Freeze-Dried Banana Chips manufactured by Fujian Fynergy Foods Co., Ltd. undergo deep-freeze vacuum sublimation without oil, sugar, or chemical additives. They feature less than 1% fat, contain 100% pure fruit, retain over 90% of native potassium, dietary fiber, and vitamins, and provide a light, crispy texture with natural sweetness.
Due to the hygroscopic nature of natural fructose and glucose in bananas, the target moisture content must be maintained below ≤ 3.0% to 5.0%, with water activity (aw) controlled below 0.25 to 0.30 at 25°C. For transoceanic FCL container shipments, we use sealed food-grade polyethylene double liners inside heavy-duty corrugated export master cartons, often incorporating optional nitrogen flushing and food-grade desiccant packets to maintain crispness and color throughout a 12-to-24-month shelf life.
Yes. As an OEM and ODM partner, Fujian Fynergy Foods Co., Ltd. provides customized cut profiles: standard round slices (6–8mm or 8–10mm), diagonal oval cuts, dices (5x5x5mm or 10x10x10mm) for cereal and yogurt inclusions, irregular broken flakes, and finely milled 100-mesh banana powder. For packaging, our automated multi-head filling lines support nitrogen-flushed stand-up pouches (Doypack), zipper bags, rigid PET jars, composite tins, and bulk ingredient carton packaging tailored to your brand's specifications.
Fujian Fynergy Foods Co., Ltd. operates under audited management systems including BRCGS (Global Standard for Food Safety Issue 9), HACCP, and ISO 22000:2018, as well as Halal and Kosher programs. Every production batch is verified in our in-house testing facility using Liquid Chromatography (HPLC) and Atomic Absorption Spectrophotometry to verify pesticide residues and heavy metals (Pb, Cd, As, Hg), alongside complete microbiological testing (Salmonella, Listeria, E. coli, Total Plate Count, Yeast & Mold). Comprehensive Certificates of Analysis (COA) accompany every export shipment.
For standard bulk carton packaging (double PE liner, 10–12 kg net weight), our standard starting MOQ is 500 kg to 1,000 kg. For customized OEM private-label printed retail packaging, the typical MOQ is 20,000 to 30,000 pouches depending on film dimensions. Production lead times range from 15 to 25 business days following final artwork and specification confirmation. We provide complimentary laboratory evaluation samples (freight collect or charged via courier account) to qualified commercial buyers upon request.
Work directly with an experienced freeze-drying manufacturer. Contact our export engineering and sales team today to request technical specification sheets, customized cut size pricing, or free evaluation samples for your brand.
Inquire Now