Years Freeze-Drying Expertise
Aerospace-Grade FD Lines
Global Production Facility
Patented Dehydration Technologies
Featured Freeze-Dried & Plant Extracts Portfolio
Precision-engineered for Louisville wholesalers, culinary developers, distillery innovators, and regional private label retailers.








Strategic Sourcing Analysis: Freeze-Dried Durian Chips & Tropical Botanicals in the Louisville Metropolitan Area
The strategic position of Louisville, Kentucky as the premier logistics hub of North America—anchored by the UPS Worldport air freight facility, direct interstate corridors (I-65, I-64, I-71), and the Inland Waterway infrastructure of the Ohio River—has transformed regional ingredient procurement. For regional grocery consolidators, commercial bakeries, and high-growth snack co-packers across Jefferson County, sourcing premium freeze-dried durian chips and tropical botanical derivatives has shifted from a niche specialty activity to an essential product-line expansion.
Durian (Durio zibethinus), commonly crowned the "King of Fruits," has historically posed severe logistical challenges across the North American market due to its volatile sulfated aroma compounds, rapid enzymatic degradation, and heavy moisture weight when shipped fresh or frozen. Vacuum lyophilization (freeze-drying) resolves these supply chain barriers completely. Through sub-zero freezing and multi-phase sublimation under ultra-low atmospheric pressure (≤0.05 mbar), raw ripe Monthong and Musang King durian flesh is preserved without cellular collapse or caramelization. The outcome is an airy, crisp, shelf-stable chip retaining ≥96% of active phytonutrients, vibrant color, and sweet custardy notes with zero post-harvest chemical preservation.
Evaluating the Top 10 Freeze-Dried Manufacturers: What Sets Tier-1 Production Apart
When procurement officers in Louisville evaluate global manufacturing partners, distinguishing between re-packers, regional brokers, and true primary lyophilization facilities is paramount. A tier-1 global manufacturer must guarantee full vertical integration: from direct farm contract management in Southeast Asia to deep industrial vacuum processing in certified cleanrooms. The top ten global operations serving the Kentucky food manufacturing corridor are characterized by rigorous QA benchmarks, including continuous in-line automated metal detection, X-ray foreign matter screening, and airtight moisture barriers that ensure moisture contents strictly under 3–5% upon delivery.
| Evaluation Parameter | Industrial Vacuum Freeze-Drying (Fynergy FD) | Hot-Air Dehydration (AD) | Atmospheric Vacuum Frying (VF) |
|---|---|---|---|
| Operating Temperature | Sub-zero sublimation (-35°C to +45°C shelf heat) | Thermal drying (+65°C to +95°C) | Heated oil immersion (+100°C to +130°C) |
| Residual Moisture Content | Strictly ≤ 3.0% – 5.0% | 12.0% – 18.0% | 5.0% – 8.0% |
| Cellular Integrity & Rehydration | 100% porous honeycombed structure; instant rehydration | Shrunk, case-hardened; poor rehydration | Oil-infiltrated; non-rehydrating crispness |
| Nutrient & Carotenoid Retention | Above 95% total retention | Severe thermal degradation (30–50% lost) | Thermal oxidation; high fat absorption |
| Additive / Preservative Need | Zero chemical additives or sulfites required | Frequently requires sodium metabisulfite | Requires vegetable oil (15–25% lipid load) |
Localized Application Scenarios in Louisville & the Ohio River Valley
The applications for freeze-dried durian chips extend far beyond single-serve retail snack pouches in Louisville's rapidly expanding ethnic and health-conscious grocers. Key industrial applications include:
- Artisan Distilling & Craft Brewing Enhancements: Positioned within Kentucky's historic spirits corridor, experimental distillers and craft brewers utilize freeze-dried durian powder and chips in specialized infusion mashes and seasonal beers. The complete absence of fat or water prevents wash spoilage while contributing rich esters, creamy mouthfeel, and unique botanical complexity.
- Wholesale Bakery & Confectionery Premixes: Commercial patisseries and donut innovators throughout downtown Louisville, NuLu, and the Highlands incorporate milled freeze-dried durian powder into fillings, macaron ganaches, and glazes. The low residual moisture prevents syneresis in frostings and ensures maximum aromatic potency without artificial flavorings.
- Ready-to-Blend Smoothie & Functional Nutrition Bowls: Regional health chains and university dining halls incorporate diced freeze-dried durian and banana chips into automated dry blends, delivering rich potassium, vitamin C, and prebiotic dietary fiber that reconstitutes immediately upon blending.
Regional Procurement Trends Driving the Kentucky Food Market
Procurement directors across the Midwest are actively mitigating port-congestion exposure and warehouse holding costs by seeking manufacturing partners that offer flexible container-load staging and standardized export documentation. The surge in consumer preference for "clean-label" formulations—products containing a single ingredient without added sugar, palm oil, or artificial preservatives—has catapulted freeze-dried durian into mainstream supermarket channels. By leveraging lyophilization, local private-label brands can launch shelf-stable, 24-month durable tropical product lines with total confidence in sensory stability.
Why Fynergy Leads Global Freeze-Drying Manufacturing
Certified industrial scale, deep technological patents, and verified cleanroom capabilities designed for global food importers.
Cleanroom Facilities
Operating Class-100,000 cleanroom workshops across 62,718 m² of infrastructure, eliminating cross-contamination risk from raw vegetable/fruit intake to nitrogen-flushed sealing.
37 Lyophilization Lines
Over 8,000 m² of vacuum freeze-drying chamber area paired with automated packing lines ensure constant batch stability, uninterrupted bulk output, and exact spec compliance.
Analytical In-House Laboratory
Equipped with Liquid Chromatography (HPLC), Atomic Absorption Spectrophotometry, and automated Kjeldahl analyzers to guarantee heavy metals, pesticides, and microbial counts meet US-FDA thresholds.
Global Certifications
Audited and verified on-site by TÜV Rheinland. Full BRCGS (Grade AA), HACCP, ISO 22000, Halal, and Kosher certifications available to streamline customs clearance into US ports.
Full-Category Sourcing
Consolidate your overseas purchasing under one manufacturer: freeze-dried fruits, functional vegetable powders, instant coffees, tea extracts, yogurt bites, and crunchy candies.
Custom OEM / ODM & Private Label
Turnkey packaging solutions: custom nitrogen-flushed retail stand-up pouches, transparent composite bags, rigid canister barrels, or bulk poly-lined export master cartons.
State-of-the-Art Processing & Quality Control
Direct photographic verification of our high-volume production workshops and analytical testing suites.
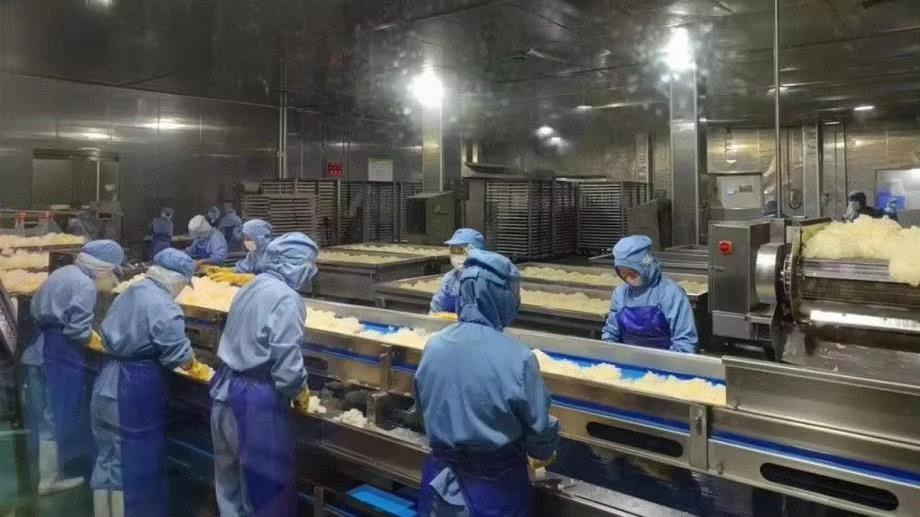
1. Ultrasonic Cleaning Line
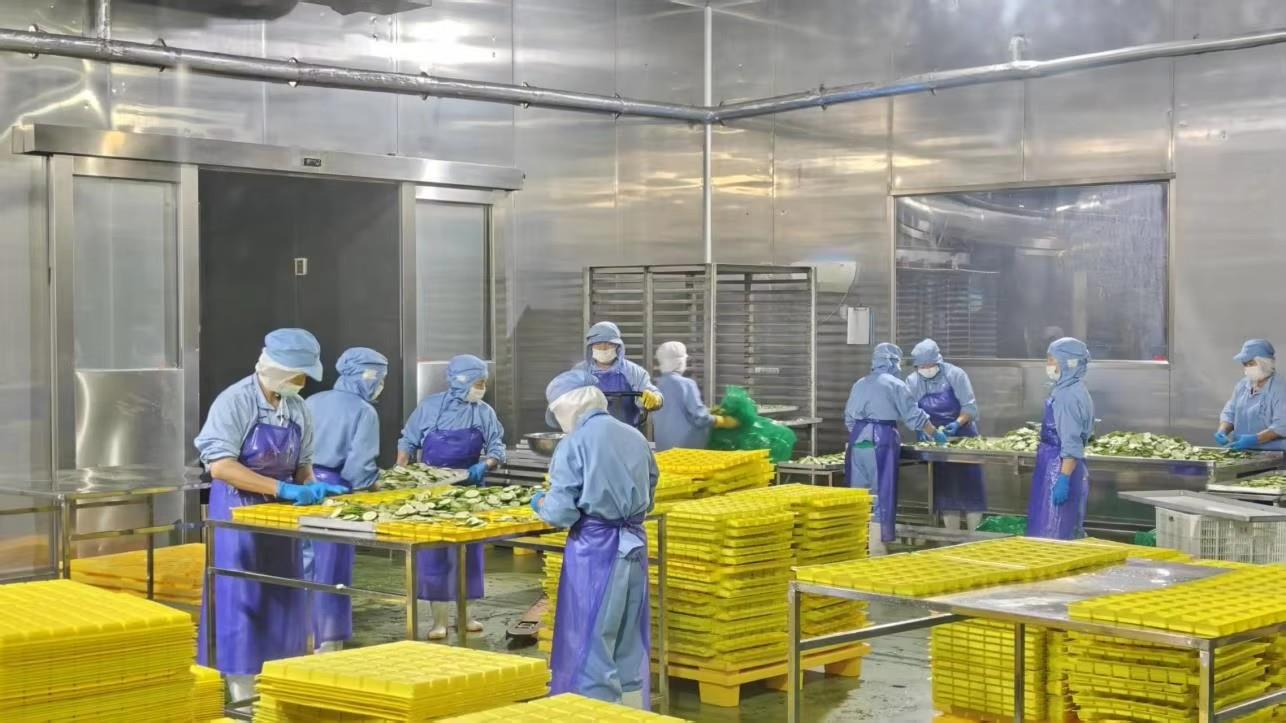
2. Precision Slicing & Traying
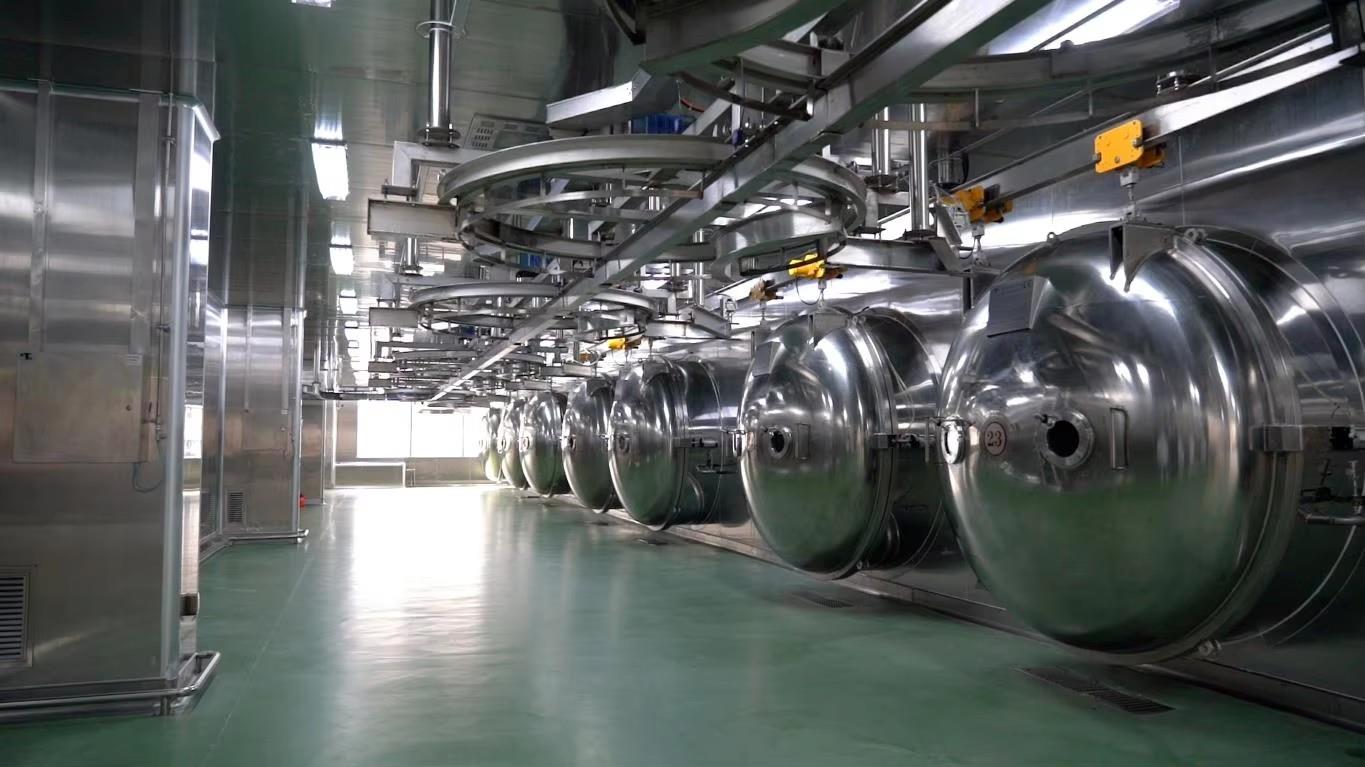
3. Vacuum Freeze-Drying
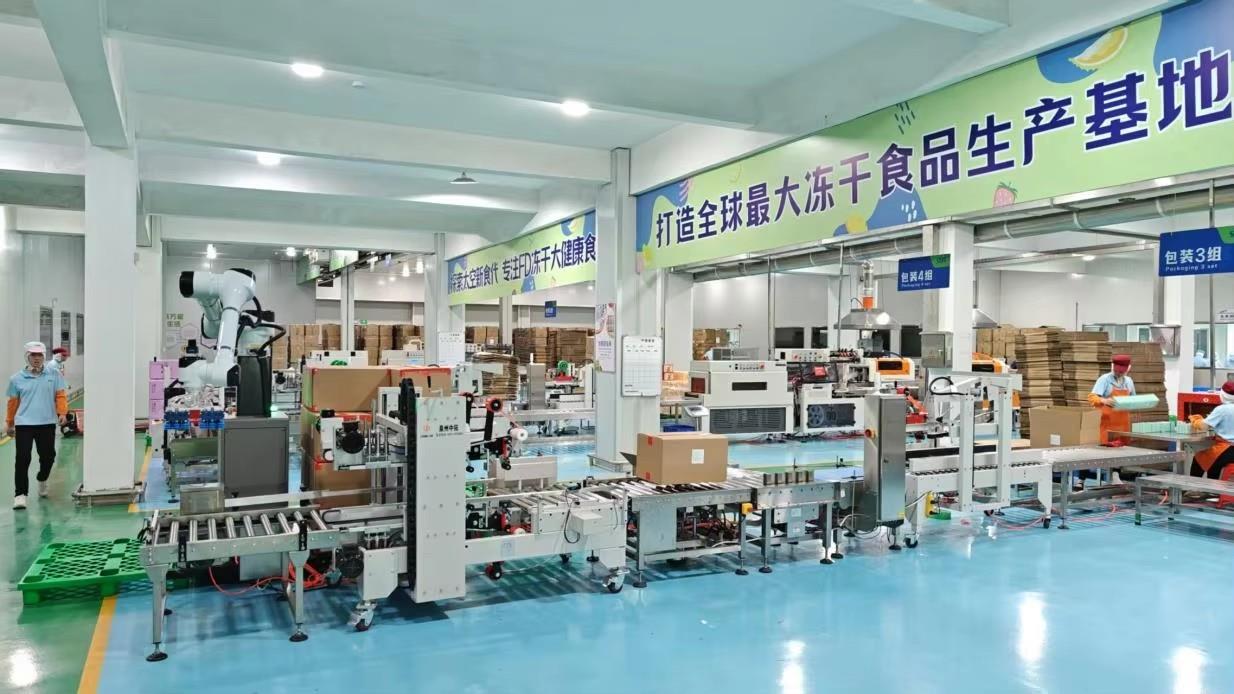
4. Automated Packaging
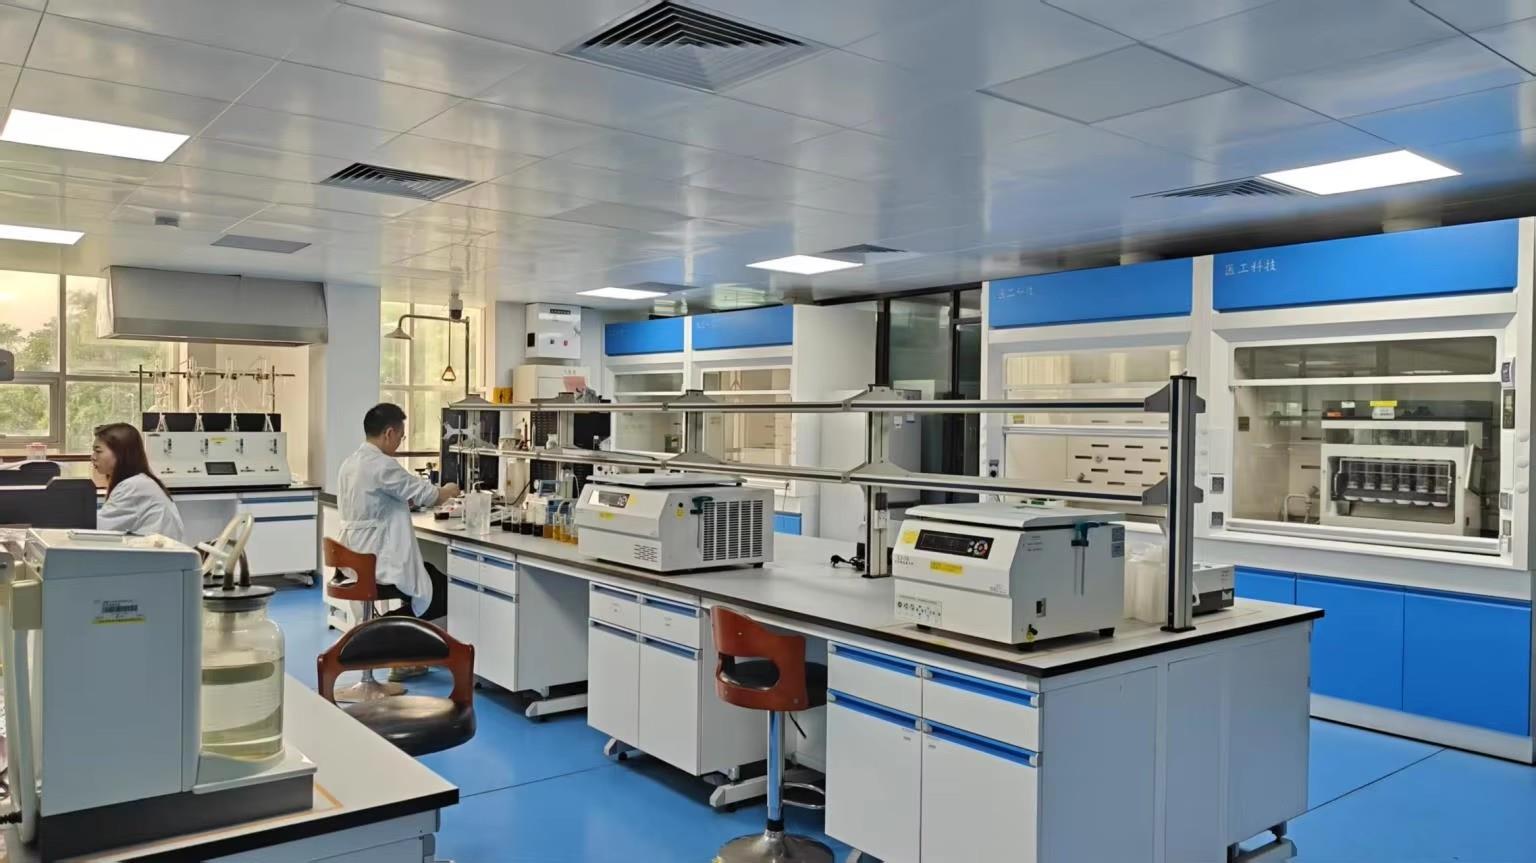
5. Analytical Testing Suite
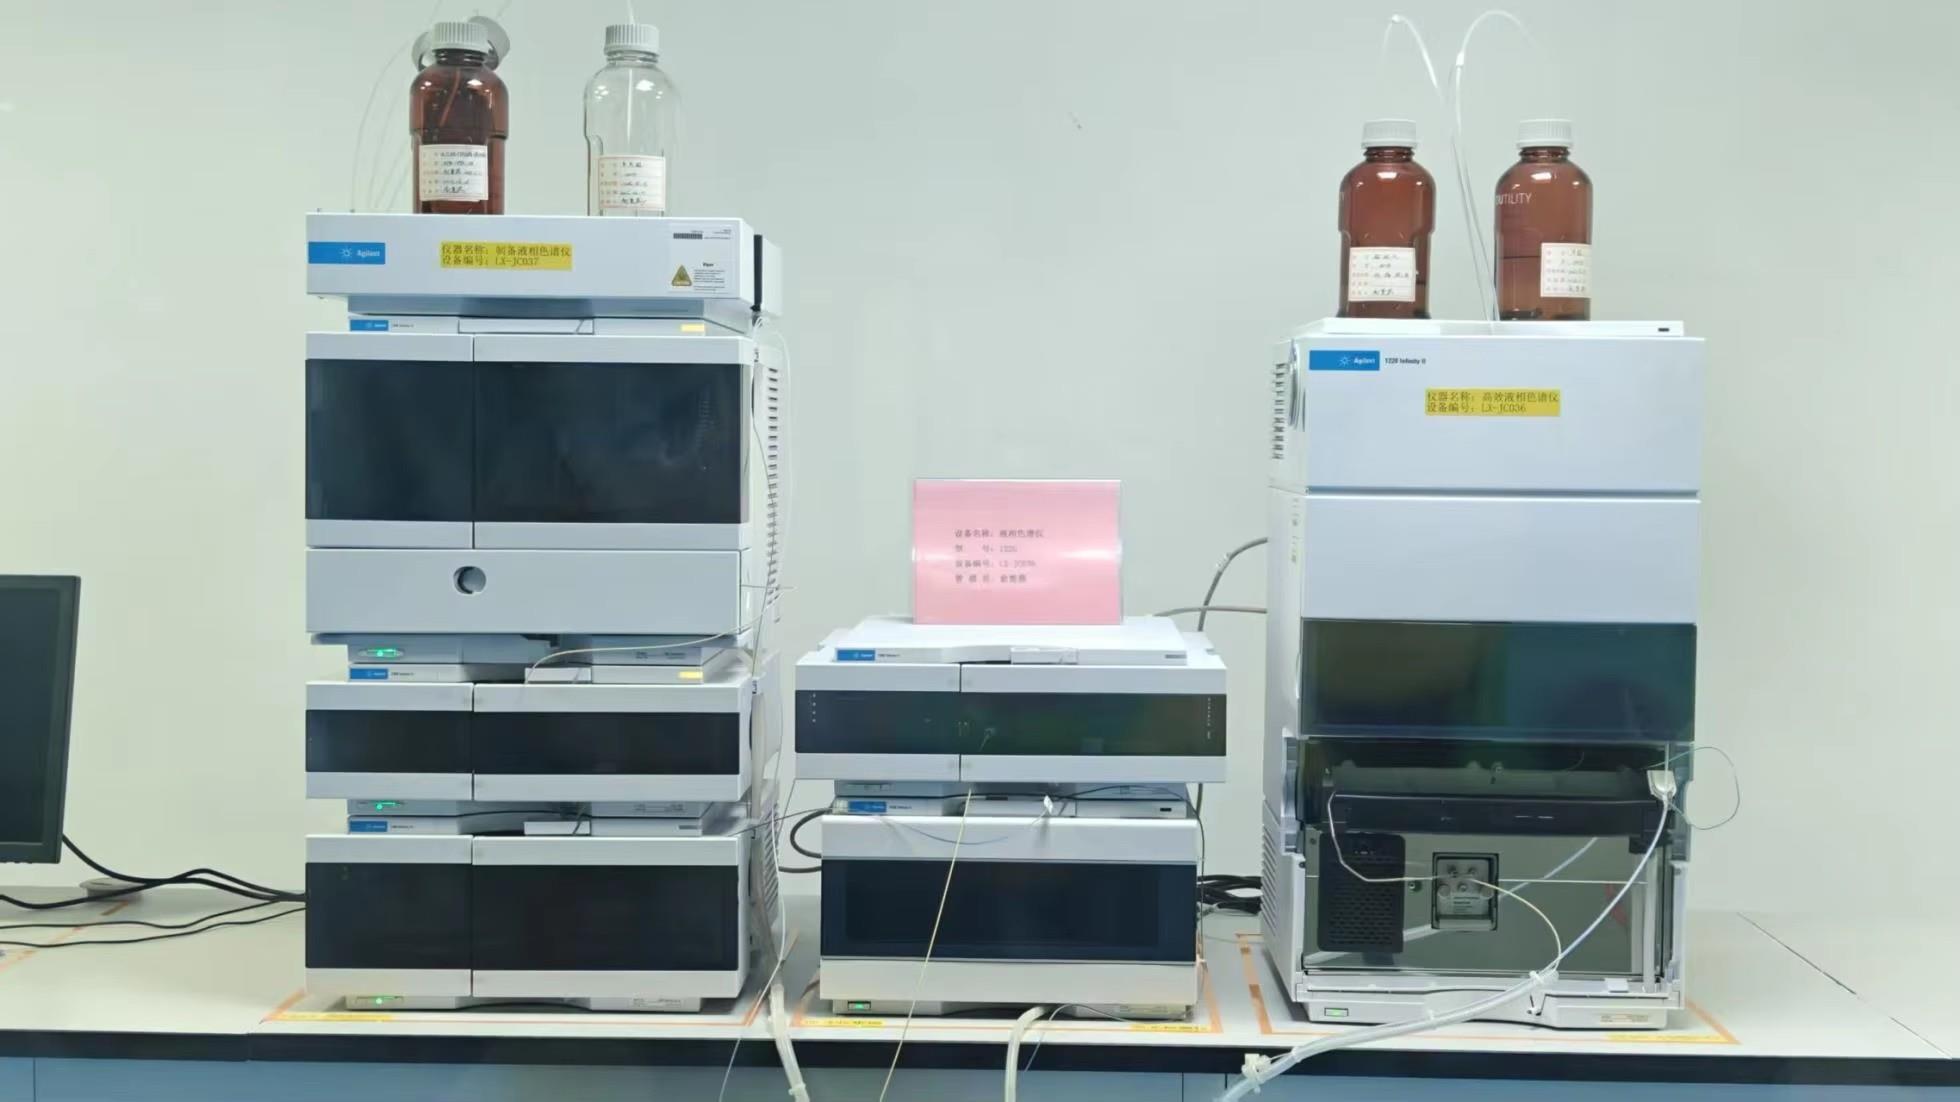
6. HPLC Chromatography
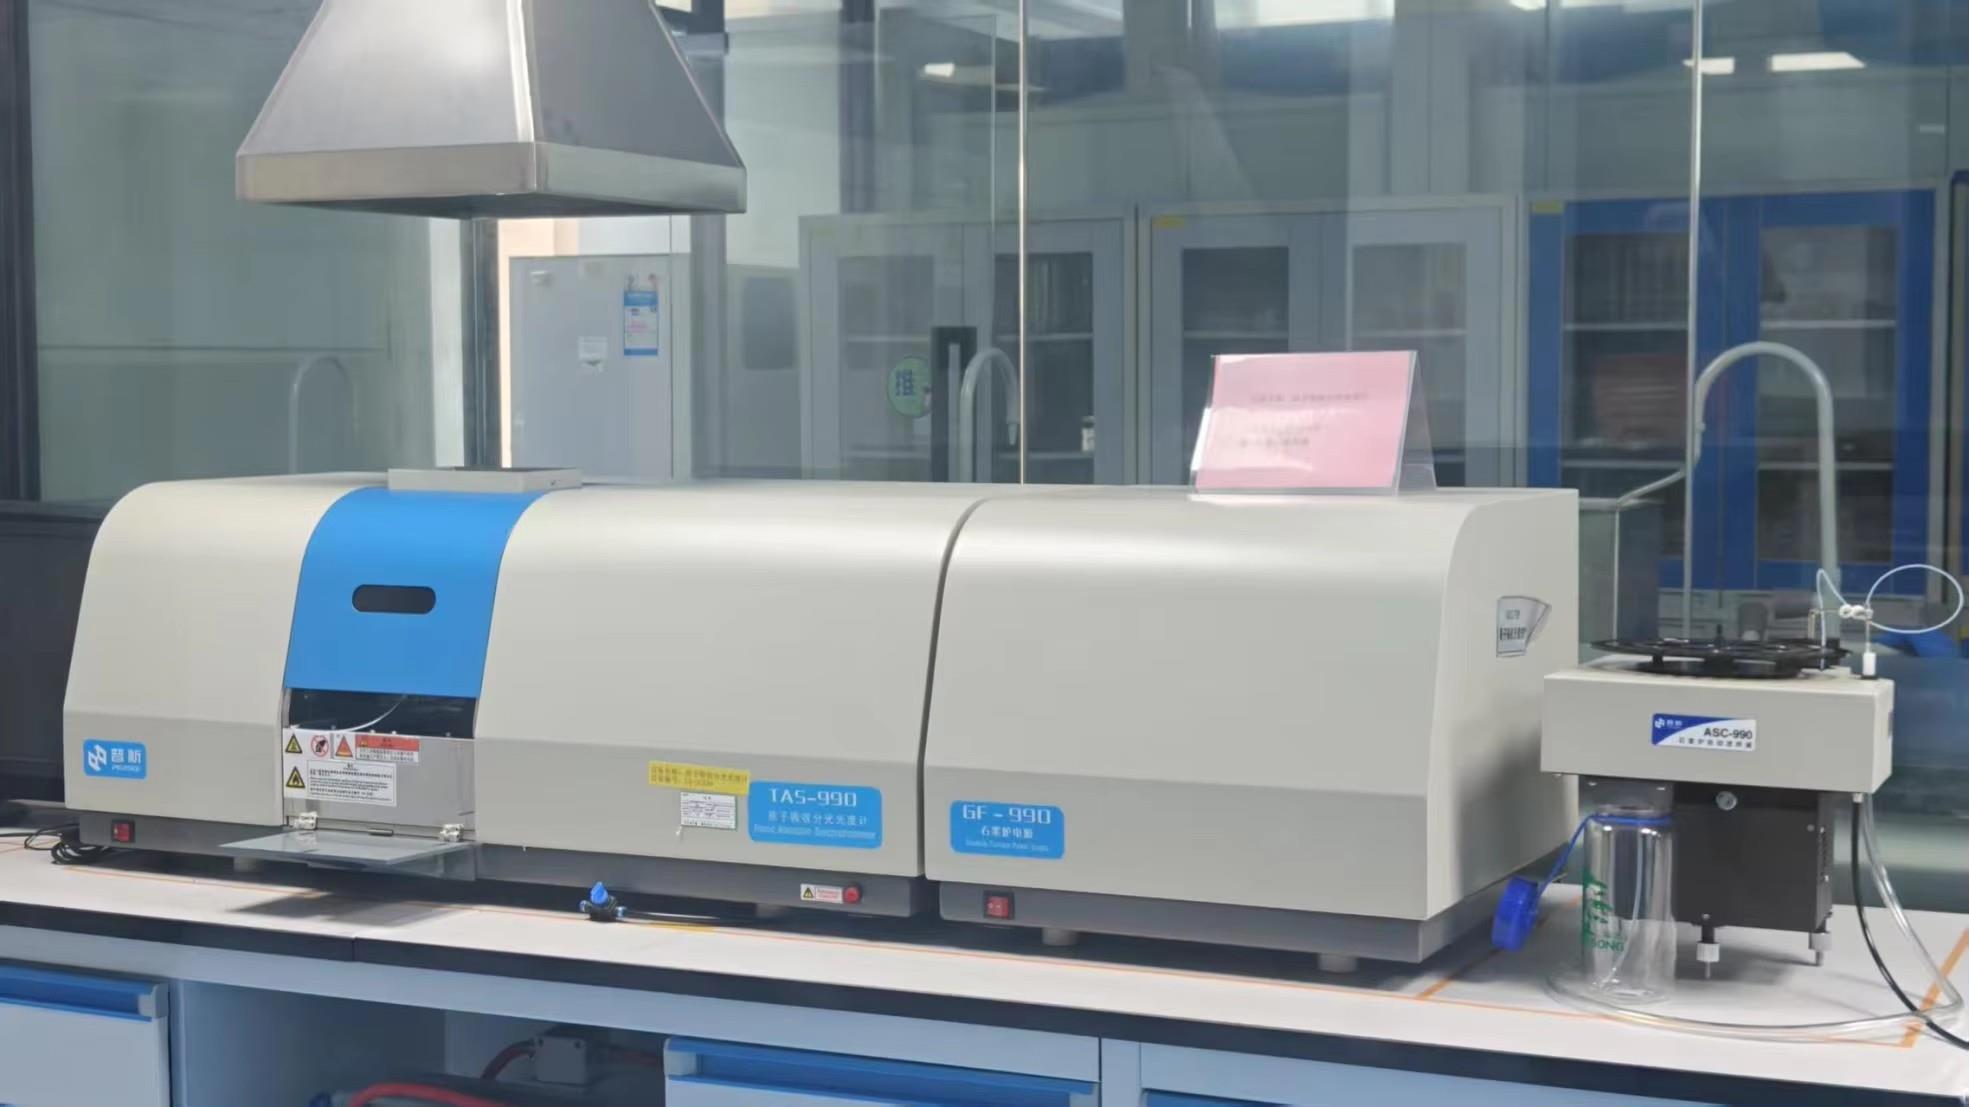
7. Heavy Metal Analysis
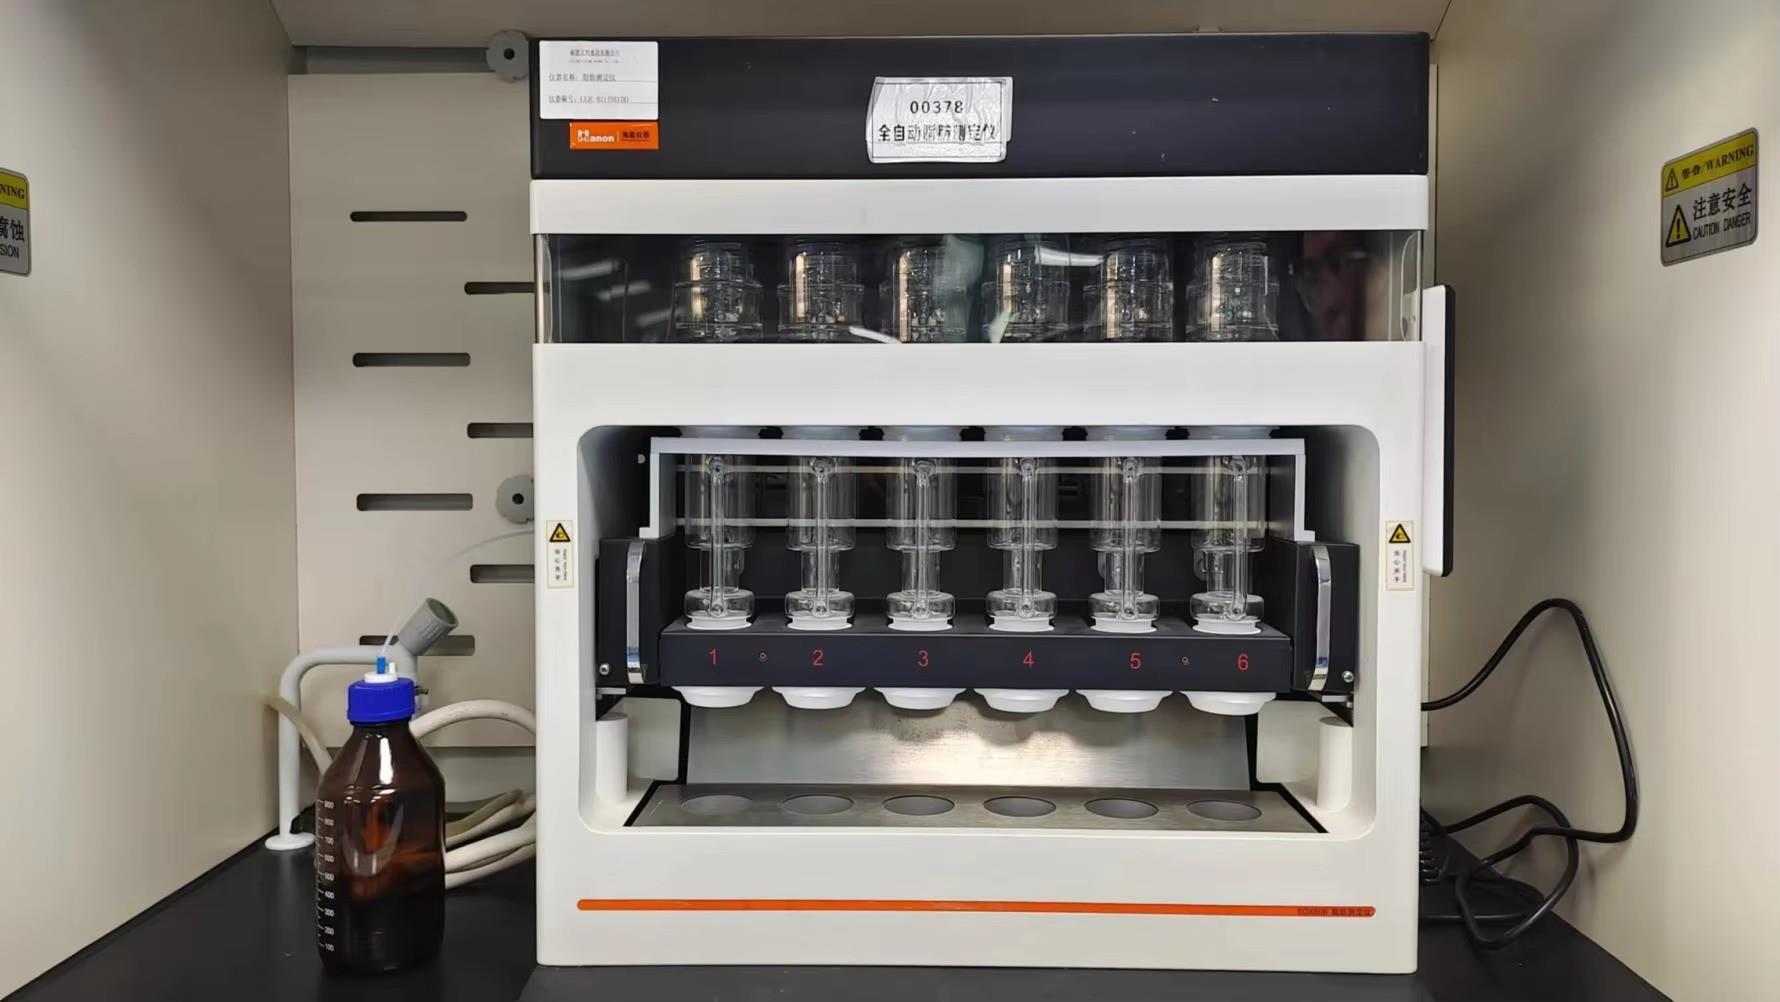
8. Nutritional Testing Lab
Frequently Asked Questions by Louisville Food Importers
Addressing compliance, freight lead times, storage, and private labeling for commercial buyers.
What is the minimum order quantity (MOQ) for bulk freeze-dried durian chips shipped to Louisville?
Standard export MOQs for bulk freeze-dried durian chips in poly-lined master export cartons typically start at 100 kg to 500 kg. For retail-ready private-label packaging (custom printed zip-pouches or nitrogen-purged composite canisters), production runs usually begin between 3,000 and 10,000 units. For new market product testing across the Louisville-Jefferson County territory, trial starter volumes can be coordinated through our sales engineering desk.
How does freeze-dried durian perform in Louisville's seasonal Ohio Valley humidity?
Because vacuum freeze-dried foods possess open microscopic cellular pores and low moisture content (≤3-5%), they are naturally hygroscopic. While high summer humidity along the Ohio River Valley would rapidly cause unpackaged product to absorb atmospheric moisture and lose crispness, our factory utilizes high-barrier packaging materials, such as multi-layer aluminum-foil lamination (PET/AL/PE) with inert nitrogen flushing (residual O₂ <1.5%). Under proper storage in a cool, dry warehouse environment, products maintain peak crunch and aromatic qualities for 18 to 24 months.
Are your production facilities fully audited and compliant with US-FDA Food Safety Standards?
Yes. Fujian Fynergy Foods holds internationally recognized third-party food safety certifications including BRCGS (Grade AA), HACCP, and ISO 22000, with facility verifications conducted by TÜV Rheinland. Our factory is fully registered with the US-FDA under FSMA regulations. Every batch shipped across US maritime entry ports (such as Savannah, Norfolk, or Newark) for onward rail to Louisville is backed by full analytical Certificates of Analysis (COA), microbiological clearances, and phytosanitary certificates.
What raw durian varieties are utilized in your freeze-drying process?
We primarily utilize premier Monthong (Golden Pillow) and selected Musang King varieties harvested at peak ripeness (Brix 28°+). Monthong is especially prized by commercial brands and Western consumers for its rich, custardy sweetness, golden color, and balanced, accessible aroma, which avoids the harsh sulfurous notes sometimes found in wilder varieties.
Can we obtain custom particle sizes such as granules or ultra-fine durian powder for baking or brewing?
Absolutely. Beyond standard intact fruit chips and natural thick slices, our factory operates cleanroom cryogenic pulverization and screening lines. We regularly supply 20–60 mesh granules for trail mixes and cereal toppings, as well as 80–200 mesh ultra-fine powders specifically engineered for instant dissolvability in ice creams, beverage bases, bakery fillings, and distilling washes.
What is the typical shipping lead time from your factory to the Louisville distribution corridor?
Standard production lead times for containerized orders average 15 to 25 days following formulation and packaging design sign-off. Ocean freight transit to primary US East Coast or Gulf gateways (Savannah, Charleston, or Houston) followed by direct intermodal rail or freight into Louisville logistics hubs typically takes 22 to 32 days. Expedited air-cargo routes directly to Louisville Muhammad Ali International Airport (SDF) are also available for urgent evaluation batches or high-priority ingredient deliveries.
Request Specifications & Commercial Wholesale Pricing
Connect with our technical export engineers to request free laboratory sample kits, comprehensive product COAs, or complete OEM private label quotation sheets for the Louisville market.