
37
Industrial FD Lines
8,000 m²
Vacuum Chamber Area
62,718 m²
GMP Standard Campus
41
Authorized Patents
Industrial Product Portfolio
Specialty Freeze-Dried & Extracted Ingredients for Trondheim
From whole wild gourmet mushrooms to nutrient-dense plant and tea matrices, our cold sublimation lines preserve molecular integrity, culinary aroma, and active beta-glucans.







Technical Whitepaper: Sublimation Criteria for Trondheim's AgTech & Gastronomic Markets
As the technological capital of Norway and the heart of Trøndelag’s renowned European Region of Gastronomy, Trondheim demands raw food ingredients with uncompromising analytical rigor. Whether serving the pioneering food-science clusters connected to NTNU (Norwegian University of Science and Technology) and SINTEF, or the exacting requirements of Michelin-starred culinary institutions like Speilsalen and Fagn, industrial food ingredients cannot merely be dried; they must retain absolute structural and aromatic fidelity.
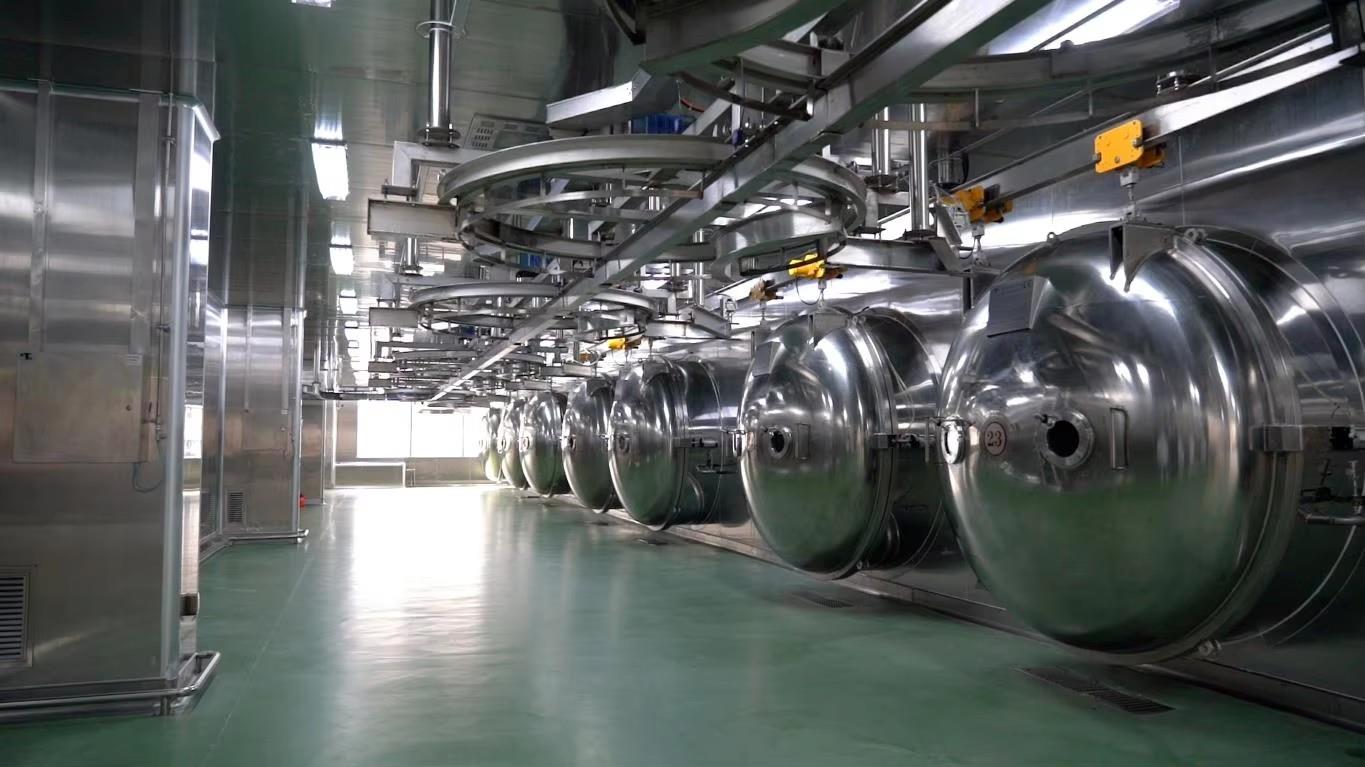
Traditional thermal dehydration degrades up to 60% of volatile terpene profiles and denatures delicate beta-glucans in edible fungi such as Boletus edulis (Porcini), Cantharellus cibarius (Chanterelle), and Lentinula edodes (Shiitake). Fujian Fynergy Foods solves this through cryogenic triple-stage vacuum lyophilization. Operating across 37 automated production lines and 8,000 m² of vacuum chamber surfaces, our factory executes deep pre-freezing at -40°C, followed by primary sublimation under strict vacuum conditions (≤50 Pa). The sublimation trajectory avoids the triple point of water, entirely bypassing the liquid phase. The outcome is a residual moisture spec consistently ≤4.0%, leaving cell wall structures completely uncollapsed and maintaining cellular integrity for instantaneous reconstitution in cold maritime kitchens.
Furthermore, cold-chain transport to maritime ports like Trondheim Havn requires absolute packaging barrier guarantees. Our modified atmosphere packaging (MAP) with nitrogen flushing prevents lipid oxidation in high-protein fungi and lipid-rich plant matrices, ensuring a 24-month ambient shelf life that resists the coastal humidity shifts of the Trondheimsfjord.
Application Scenarios
Localized Integration across Trøndelag's Food Ecosystem
How institutional food manufacturers, catering specialists, and research laboratories in Trondheim deploy our freeze-dried fungal products.
Nordic Gastronomy & Culinary Innovation
Fine-dining restaurants, craft charcuteries, and culinary academies across Trondheim utilize our whole freeze-dried wild chanterelles and porcini slices. Instant rehydration restores pristine spongy textures, allowing chefs to capture autumn woodland forest profiles all winter without soggy degradation.
Arctic Expedition Rations & Emergency Preparedness
Trondheim acts as a key departure nexus for Arctic research, maritime shipping, and offshore energy projects. Our ultra-lightweight, high-density freeze-dried mushroom cubes and instant vegetable soups serve emergency rations and outdoor trekking brands requiring zero refrigeration and effortless field reconstitution.
NTNU AgTech & Functional Food Formulation
Biotech pioneers in Trondheim incorporate our micro-milled medicinal mushroom powders (Lion’s Mane, Reishi, Chaga) into nootropic coffees, sports nutrition matrices, and immune supplements. Cleanroom micronization guarantees consistent particle distribution and uncompromised bioactive yields.
Market Trends
Trondheim & Central Norway Procurement Trajectories
Emerging shifts shaping how B2B buyers and contract manufacturers source clean-label, shelf-stable ingredients.
The "Clean Umami" Sodium Reduction Trend
In accordance with Norwegian Directorate of Health directives, Trondheim food processors are actively replacing synthetic MSG and excess sodium. Freeze-dried mushroom granules serve as 100% natural, glutamate-rich seasoning bases that enhance flavor complexity while keeping sodium counts low.
Traceable ESG & Audited Global Sourcing
Central Norwegian distributors have raised the bar on international supply chains. Buyers demand full chain-of-custody documentation, TÜV Rheinland verified manufacturing infrastructure, and stringent limit testing for pesticides, heavy metals, and polycyclic aromatic hydrocarbons.
Expanding Private Label Functional Beverages
Consumer demand for adaptogenic drinks has surged across Trondheim's universities and tech parks. Brand owners require turn-key OEM/ODM partners capable of delivering instant, dispersible mushroom extracts formulated alongside freeze-dried coffee and tea matrices.
Factory Capabilities
Fynergy Enterprise Advantages Backed by Hard Evidence
Global manufacturing competence delivering scale, precision, and compliance to Norwegian importers.
Class-100,000 Cleanroom Processing
Our 62,718 m² manufacturing facility operates high-standard air-filtered cleanrooms. This prevents spore cross-contamination, ensuring biological safety for export to strict EFTA and EU regulatory zones.
Comprehensive Testing Laboratory
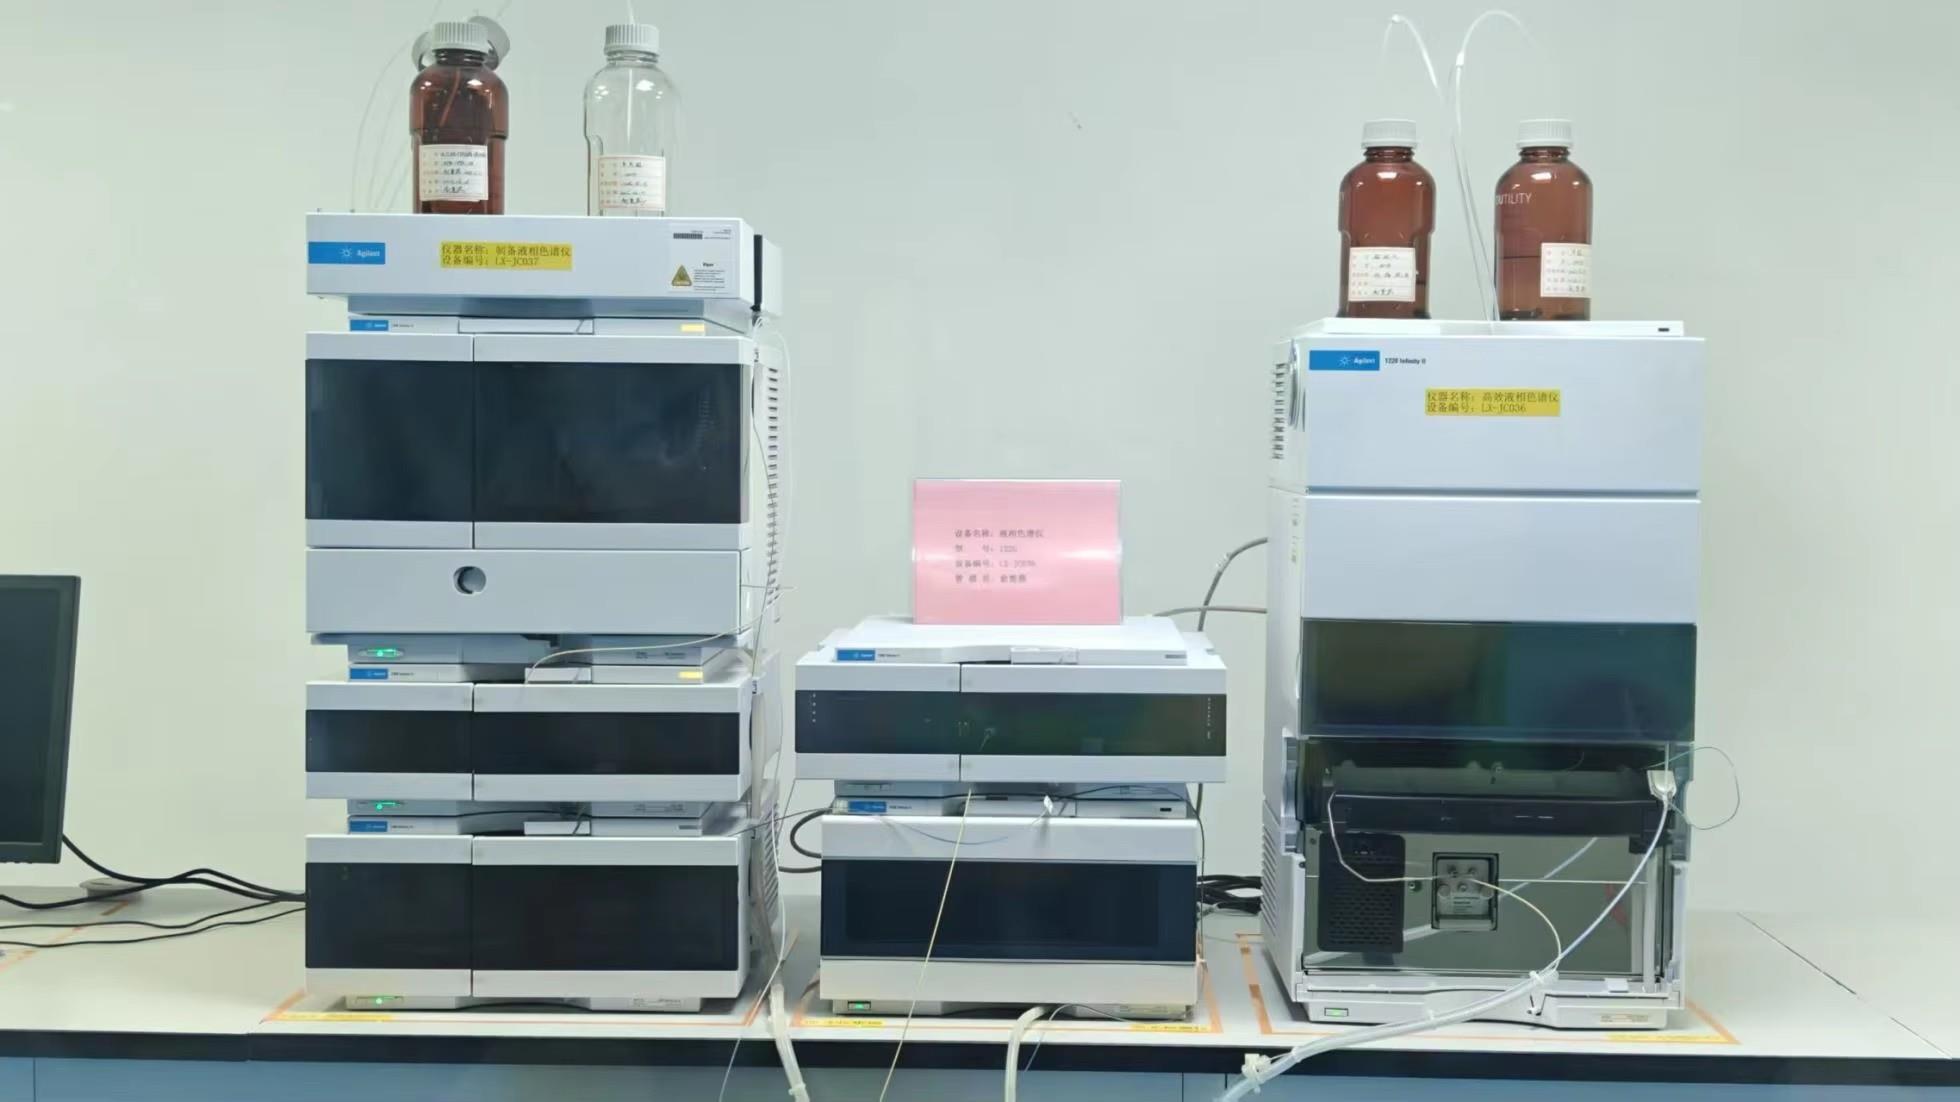
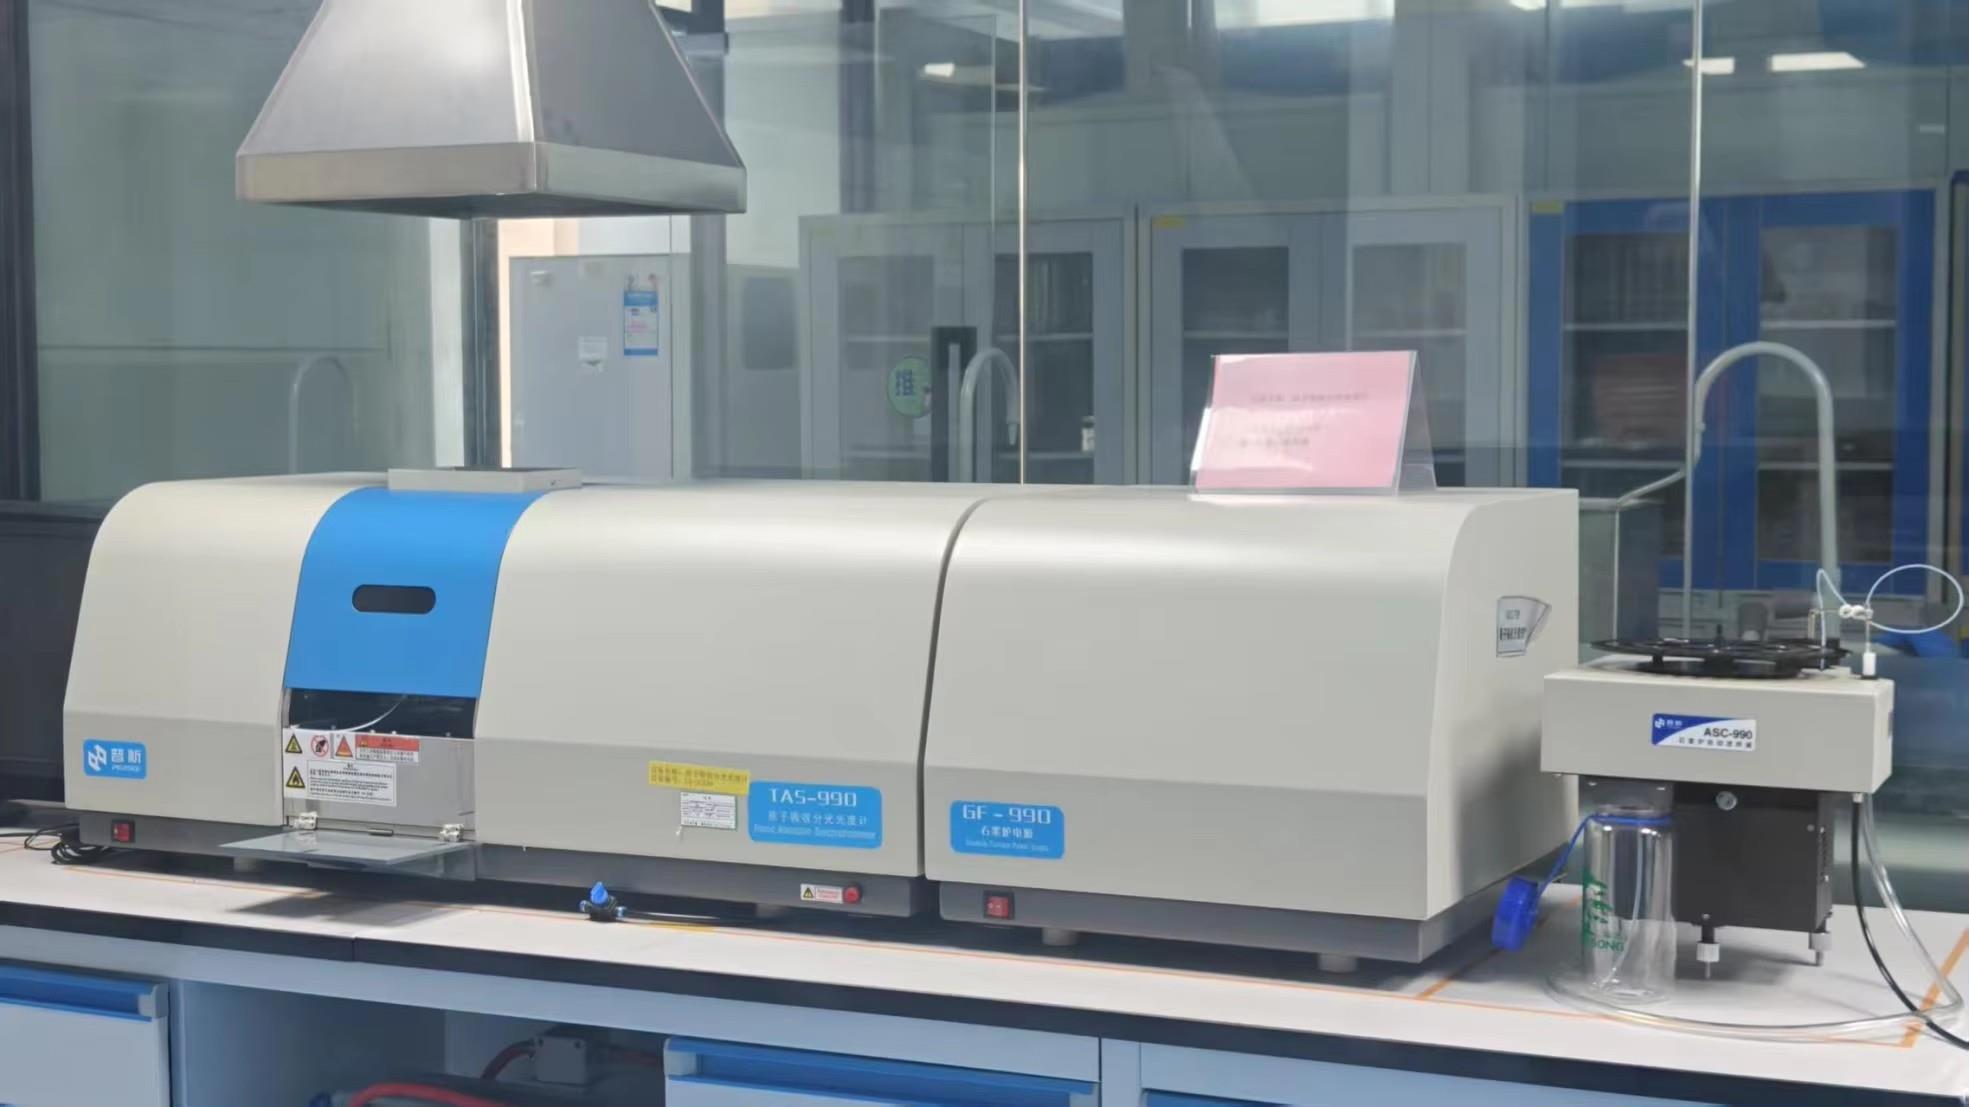
Every shipment is verified through Liquid Chromatography (HPLC), Atomic Absorption Spectrophotometry, and Kjeldahl apparatus, guaranteeing strict limits on heavy metals, moisture, and microbiological counts.
Turnkey OEM / ODM & Custom Slicing
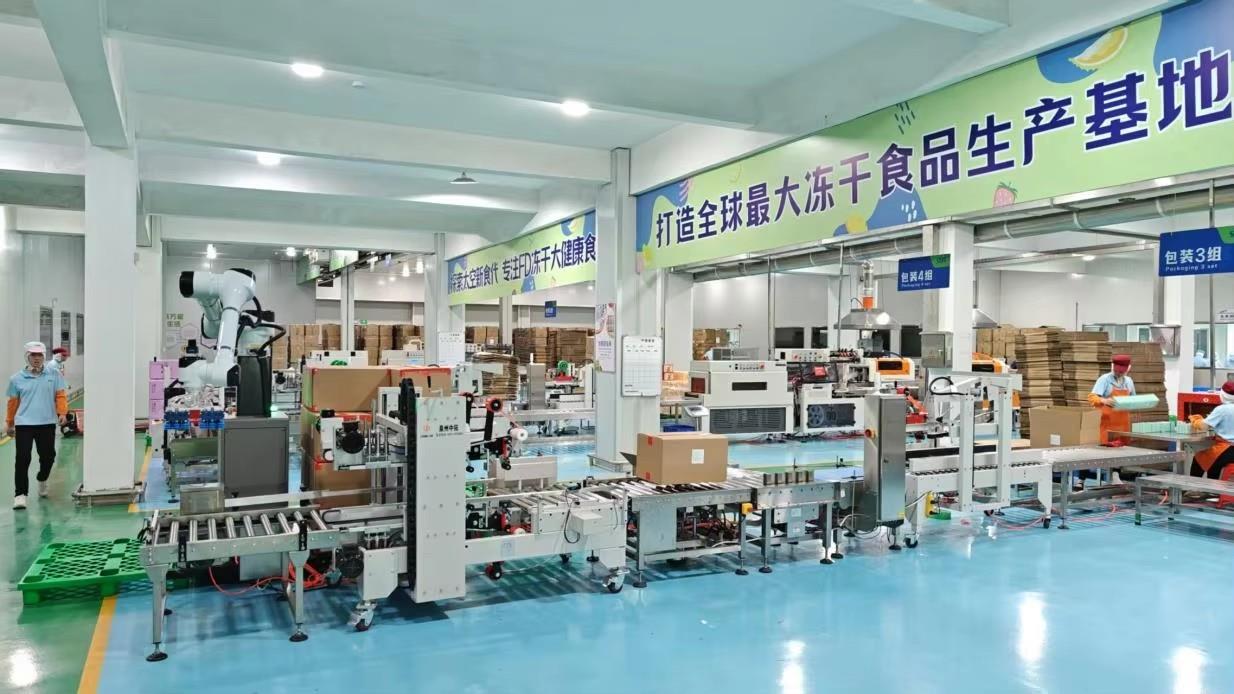
From whole mushroom buttons and custom dice sizes (2-6mm) to ultrafine powders, we offer comprehensive private label packaging options ranging from industrial drums to nitrogen-purged retail standing pouches.
Factory Tour & Testing
Real-World Testing & Manufacturing Verification
Glimpse our on-site laboratory testing stations and production machinery certified by BRCGS, ISO 22000, and TÜV Rheinland.
Procurement Knowledge Base
Frequently Asked Questions for Trondheim Importers
Direct technical answers addressing Norwegian customs, food safety compliance, shipping logistics, and custom formulation.
Does your manufacturing comply with Norwegian Mattilsynet and EU food safety standards?
Yes. Our manufacturing facilities are fully certified under BRCGS (Global Standard for Food Safety), HACCP, and ISO 22000. Our in-house analytical lab tests every batch for microbiological counts, pesticide residues, and heavy metals (lead, cadmium, arsenic, mercury) in strict alignment with European Commission regulations and the Norwegian Food Safety Authority (Mattilsynet). Full Certificate of Analysis (COA) documents accompany each shipment.
What are the typical sea freight transit options and lead times to Trondheim Port?
Bulk shipments depart from Xiamen Port with sea freight routing directly into Trondheim Havn or via transshipment hubs in Rotterdam or Hamburg. Typical sea freight transit runs 35 to 45 days. Production lead times for standard OEM specifications usually range from 15 to 25 working days following sample approval and deposit confirmation.
What is the Minimum Order Quantity (MOQ) for custom cut sizes or private labeling?
For bulk industrial orders (whole mushrooms, tailored slices, or micro-milled powders packed in double-layer poly-lined cartons), our standard MOQ starts at 100 kg to 500 kg per SKU. For custom-printed retail packaging (doypack pouches, jars, or branded tins), MOQs generally start at 5,000 units. Trial batch sizes are negotiable for pilot launches in the Norwegian market.
How does freeze-drying compare with air-drying for high-end culinary applications?
Air-drying utilizes sustained heat, which causes shrinkage, dark oxidation, and structural collapse while turning fungi chewy upon rehydration. Our vacuum freeze-drying sublimes water vapor directly from the solid ice state at sub-zero temperatures, maintaining pore structures, rich natural colors, and authentic aroma profiles. Rehydration takes less than 3 to 5 minutes in room-temperature water.
Can you supply certified organic mushroom and vegetable powders?
Yes. We manage verified organic raw material sourcing channels that meet EU organic equivalents. Furthermore, we maintain dedicated production windows with cleanroom sanitization protocols to prevent contact with conventional materials. Complete traceability dossiers from raw harvest to final seal are delivered with your shipment.
How can we obtain bench samples for sensory and laboratory evaluation?
We routinely ship sample evaluation kits directly to R&D facilities and procurement offices in Trondheim via DHL or FedEx. Each kit includes complete product specification sheets, typical batch microbiological analyses, and suggested moisture barrier guidelines. Simply click our inquiry button to initiate sample dispatch.
Partner with an Audited Freeze-Drying Leader
Elevate your ingredient line with reliable sublimation capacity, verified quality systems, and turnkey private labeling tailored specifically for the Norwegian food industry.
Get Catalog