
Factory Inventory & Custom Portfolio
Engineered Lyophilized Ingredients & Novelty Formats
Explore our industrial freeze-dried solutions serving Tampere's commercial bakeries, retail distributors, specialty roasters, and ready-to-eat brand owners.







20+
Years Lyophilization Expertise
37
Dedicated FD Production Lines
8,000 m²
Vacuum Chamber Area
41
Authorized Proprietary Patents
Nordic Technical Application
Precision Cryogenics Meets the Tampere Confectionery & Outdoor Sector
Solving extreme logistical cold-chain challenges while elevating sensory performance for the Finnish market.
As the industrial and technology heartland of inland Finland, Tampere and the wider Pirkanmaa region present a uniquely sophisticated ecosystem for high-value food technologies. While traditionally reliant on energy-intensive continuous sub-zero refrigeration for standard dairy novelties, Finnish procurement directors, contract packagers, and FMCG brand managers are increasingly confronting volatile electricity tariffs, freight overheads across Fennoscandia, and strict ESG compliance mandates. The introduction of ambient-stable, vacuum freeze-dried ice cream sandwiches manufactured by an enterprise equipped with 37 continuous industrial lyophilization lines provides a game-changing commercial solution.
Operating under ultra-low vacuum sublimative parameters (typically below 0.05 mbar at condenser temperatures plummeting to -50°C), our manufacturing process ensures that the complex multi-phase cellular matrix of premium dairy cream—composed of air cells, emulsified milk fat globules, and concentrated serum proteins—remains structurally rigid. Ice crystal sublimation occurs without capillary collapse, retaining over 97% of native volatile aromatic terpenes and original honeycomb aeration. For food brands distributing from Tampere logistically westward to Pori, south toward Helsinki, or north into Lapland, ambient shelf stability eliminates seasonal chill-chain dependency entirely.
High-Calorie Nordic Trekking Rations
Finland's entrenched hiking, bushcraft, and military training sectors demand non-perishable, nutrient-dense nutrition. Freeze-dried ice cream sandwiches offer an ultralightweight, zero-melt fat-to-carb ratio that withstands sub-arctic excursions and summer lakeside camps alike.
Impulse Ambient Retail (S-Market & K-Citymarket)
By bypassing the freezer aisle entirely, Finnish retail partners place these novelty items directly into ambient checkout queues, seasonal displays, and specialty novelty snack aisles, drastically improving margin yields and eliminating thaw shrinkage.
Gourmet Bakery Inclusions & Café Toppings
Tampere's artisan bakery hubs and third-wave café chains utilize wafer-sandwiched freeze-dried dairy solids as moisture-resistant, crunch-retaining culinary garnishes for signature soft serves, pastries, hot cocoa beverages, and winter desserts.
Scientific Parameter Comparison: Lyophilization vs. Conventional Food Stabilization
Benchmarking thermodynamic sublimation against legacy industrial thermal reduction protocols.
| Critical Parameter | Fynergy Industrial Vacuum Freeze-Drying | High-Temperature Air Evaporation | Deep Freezing Storage (Cold Chain) |
|---|---|---|---|
| Thermodynamic Phase | Solid-to-gas direct ice sublimation (< 0.05 mbar) | Liquid-to-gas evaporation via sensible heat | Continuous latent heat management (-18°C) |
| Cellular Integrity | Unchanged; micro-porous matrix retained | Severe cellular shrinkage, vitrification & collapse | Intact; vulnerable to freeze-thaw crystal migration |
| Residual Moisture (aw) | ≤ 3.0% (Water activity < 0.25) | 8.0% - 15.0% (Enzymatic risk remains) | Saturated (High water content immobilized) |
| Aroma & Lipid Stability | Zero thermal degradation; protected from oxidation | Oxidative rancidity & caramelization loss | Stable until surface freezer-burn occurs |
| Logistics Overhead to Finland | Ambient standard palletized sea/rail freight | Ambient freight; poor sensory quality | High-cost reefer containers & chilled distribution |
Factory Heritage & Infrastructure
Engineering Superiority Backed by Independent Verification
Over two decades of precision production spanning our 62,718 m² manufacturing base in Zhangzhou, Fujian.
Tier-1 Global Compliance (BRCGS, HACCP, ISO 22000)
Verified on-site by TÜV Rheinland, our manufacturing facilities adhere to strict European hygiene norms, providing Finnish importers complete audit transparency, lot traceability, and full EU customs clearance documentation.
Class-100,000 Cleanroom Packaging
Moisture reabsorption is the critical hazard of freeze-dried dairy. We execute secondary handling and automated nitrogen flushing within Class-100,000 pharmaceutical-grade cleanrooms, ensuring prolonged shelf stability without humectants.
Advanced Analytical In-House Laboratory
Equipped with Liquid Chromatography (HPLC), Atomic Absorption & Fluorescence Spectrophotometry, and automated Kjeldahl protein units, we conduct exhaustive screen testing for heavy metals, pesticides, and microbial pathogens per batch.
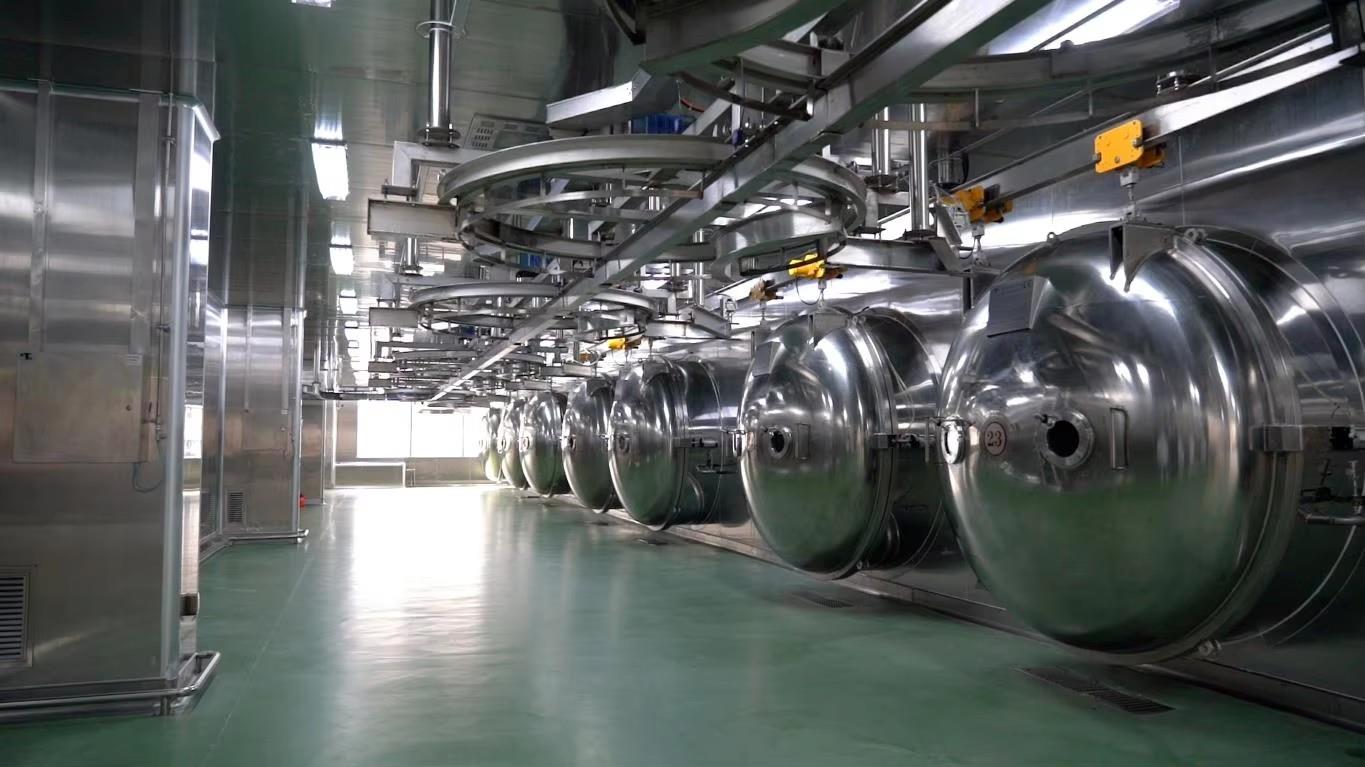
Continuous Sublimation Chambers
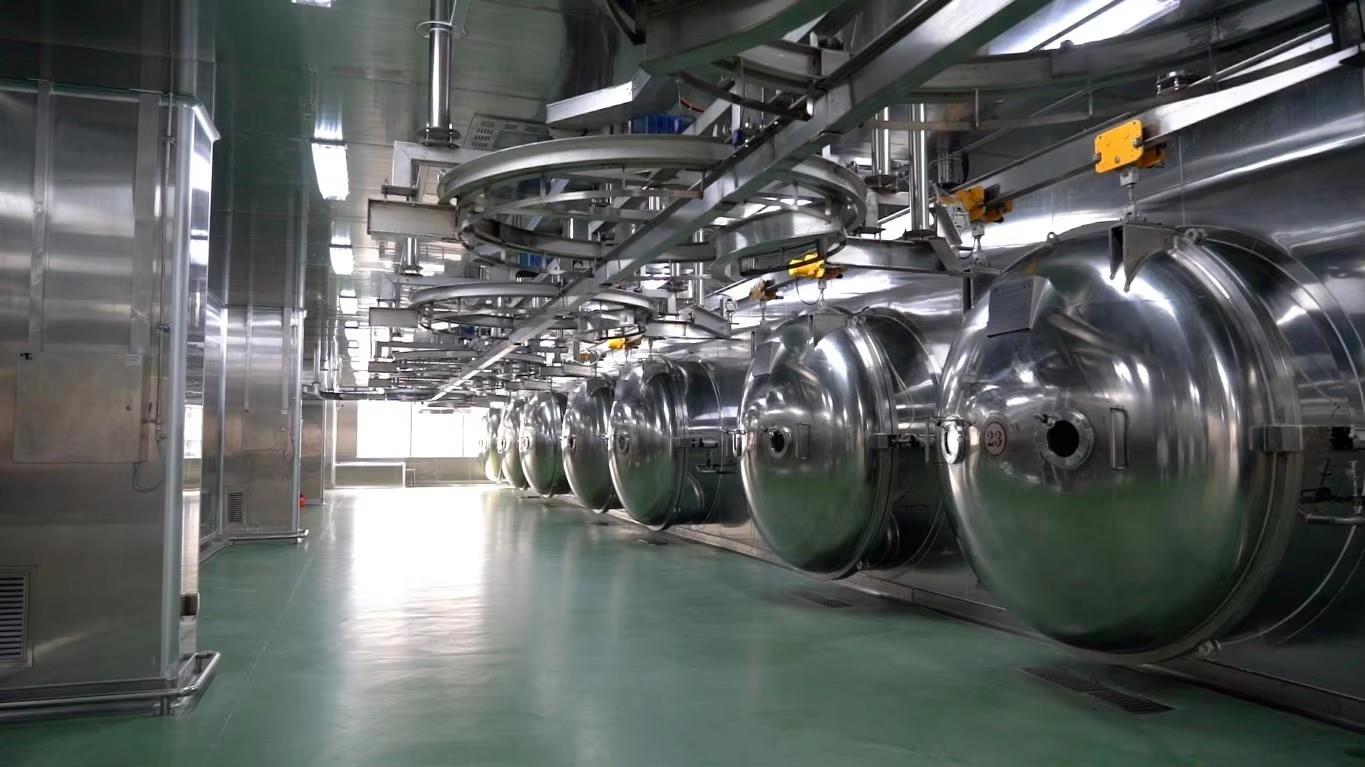
37 Industrial Lyophilization Lines
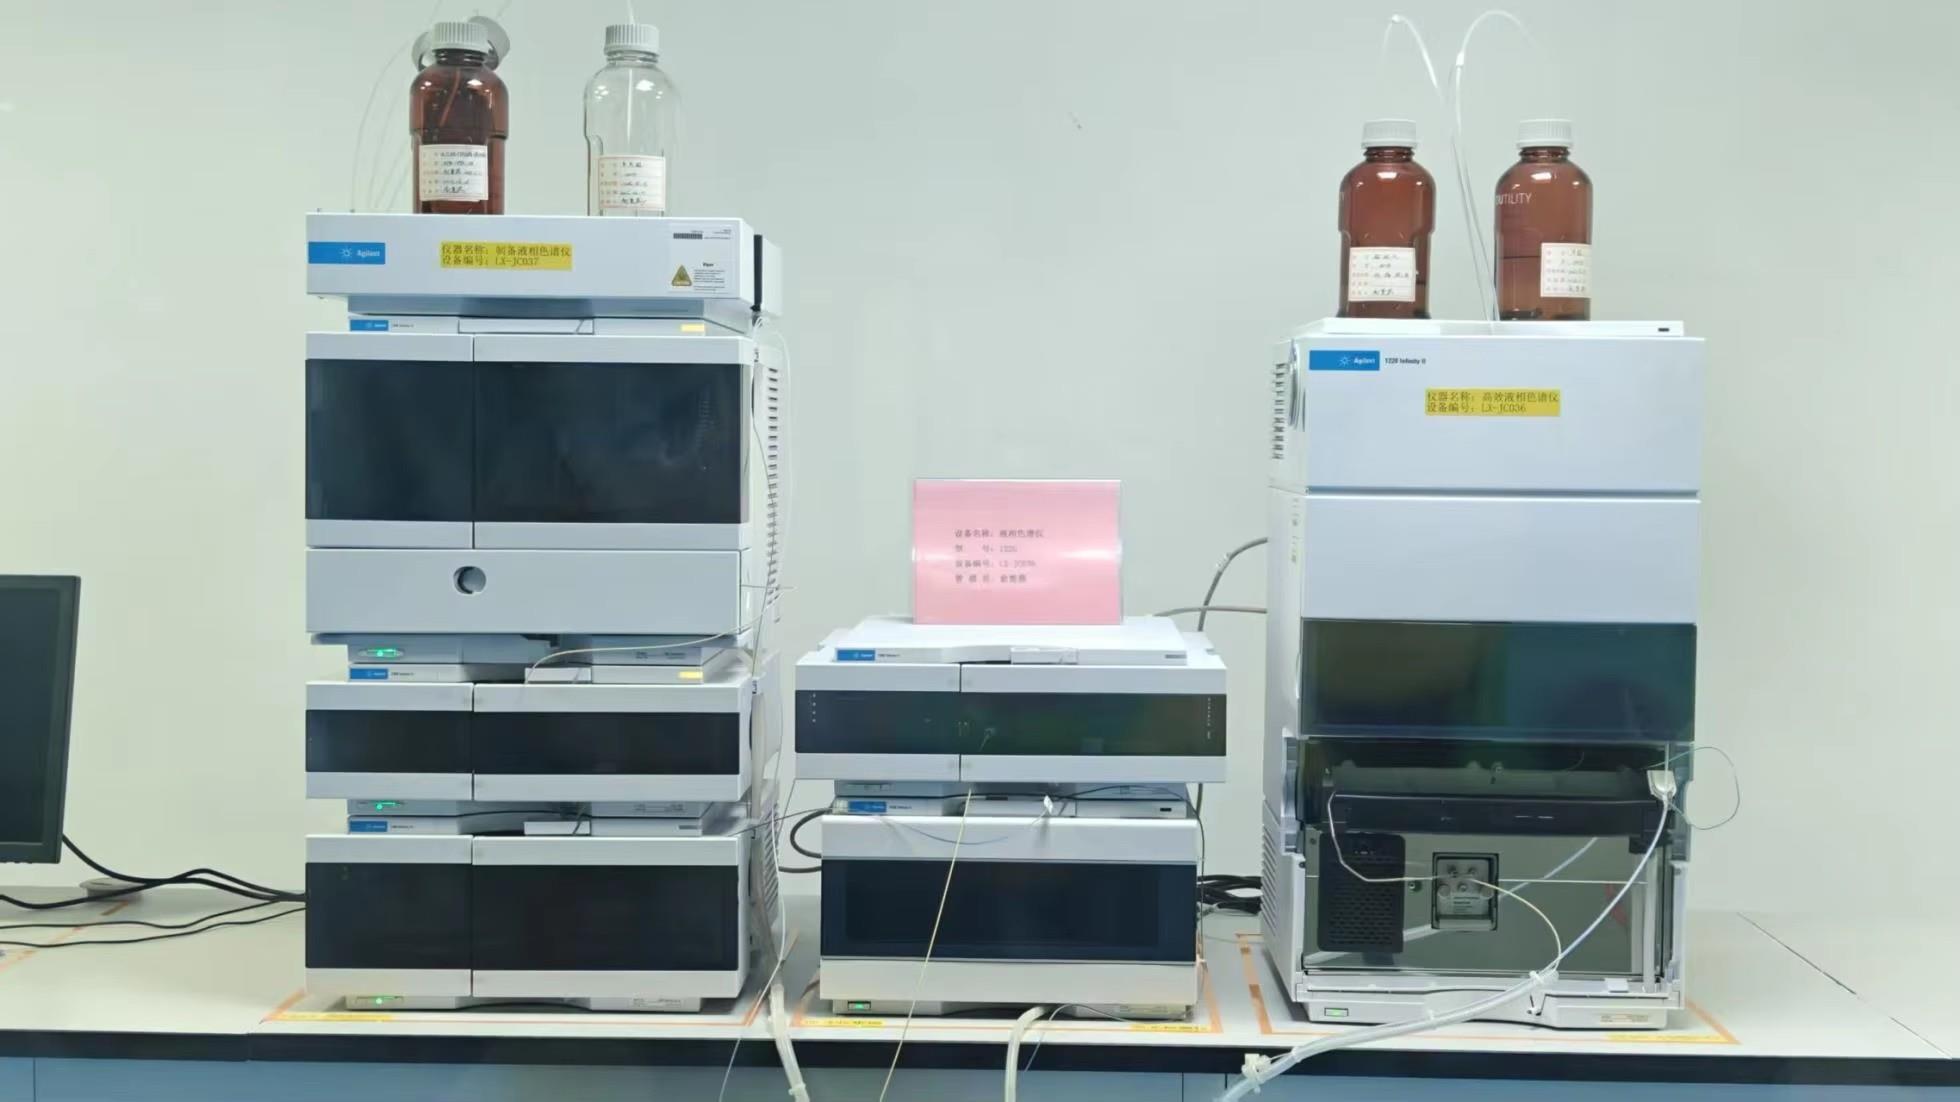
Analytical HPLC Lab Verification
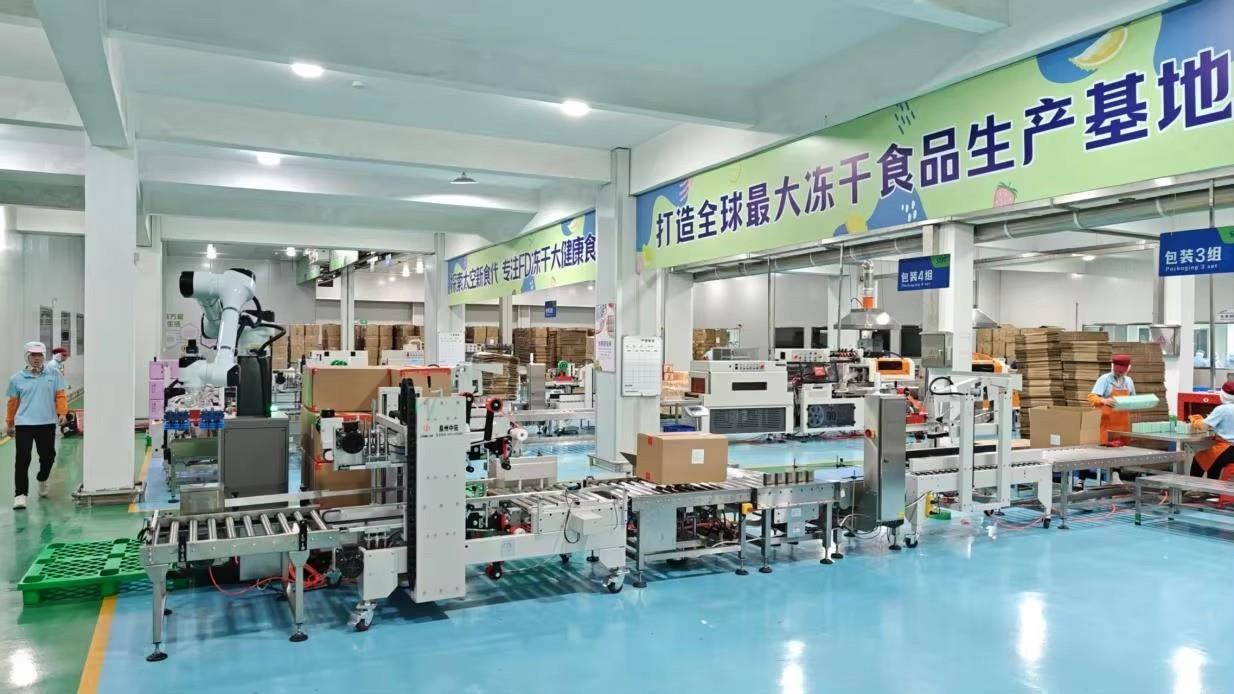
Cleanroom Precision Packaging
Procurement Directives
Frequently Asked Inquiries by Finnish & Nordic Importers
Technical, logistical, and certification clarity for prospective wholesale and private-label partners in Tampere.
How does freeze-dried ice cream retain structural stability during transit to Pirkanmaa without cold storage?
Freeze drying removes water through vacuum sublimation rather than thermal melting, locking the dairy proteins, natural sugars, and fats into an airy, rigid microscopic sponge. With a moisture content under 3%, microbial proliferation is suspended, and the product cannot melt even at ambient room temperatures up to 35°C. For Tampere distributors, this eliminates temperature-controlled logistics entirely, allowing transport via standard dry container freight through Port of Vuosaari or Port of Turku directly inland.
What are the minimum order quantities (MOQ) and lead times for OEM private-label production?
Our standard starting MOQ for bulk freeze-dried ice cream sandwiches is 100 kg, while customized printed retail nitrogen-flushed foil packaging typically commences at 20,000 to 30,000 retail pouches. Initial formulation matching, sensory profiling, and wafer moisture-barrier testing require 7 to 10 working days, with mass chamber batch processing taking 20 to 25 days following artwork sign-off.
Does the facility comply with European Union Food Hygiene Regulations (EC No 852/2004)?
Yes. Fujian Fynergy Foods holds comprehensive BRCGS, HACCP, and ISO 22000 certifications verified annually by TÜV Rheinland. Every export batch is accompanied by comprehensive COAs (Certificates of Analysis), allergen disclosures, heavy metal and microbiology lab panels, and veterinary/dairy origin health declarations necessary for Finnish Customs (Tulli) clearance.
Can custom Finnish flavor profiles (such as Salmiakki, Bilberry, or Rye Wafer) be engineered?
Absolutely. Operating our own R&D center with 41 authorized patents, we regularly formulate customized flavorings and structural biscuit layers. We can integrate Nordic wild berry purees (such as Arctic lingonberry or bilberry), Finnish licorice/salmiakki swirls, or gluten-free rye crisps, calibrating the specific sugar-to-fat crystallization threshold to guarantee uniform crispness after sublimation.
What packaging barrier properties are deployed to withstand Nordic winter humidity fluctuations?
Because lyophilized products are intensely hygroscopic, we exclusively engineer multi-layer metallized barriers (PET/AL/PE or high-barrier OPP/VMCPP) featuring moisture vapor transmission rates (MVTR) below 0.5 g/m²/24hr. Packages are nitrogen-purged during automated sealing to reduce residual headspace oxygen below 1.5%, guaranteeing a 12 to 24-month crispness shelf-life under diverse storage conditions.
Architect Your Freeze-Dried Line for the Nordic Market
Initiate a direct consultation with our export engineering and food formulation team. Receive comprehensive specification sheets, technical dossiers, and expedited product samples dispatched directly to your Tampere testing facility.