
Ingredient Portfolio
Curated Freeze-Dried Products for Latin American Formulators
Direct supply from Fujian Fynergy Foods Co., Ltd. Every product is produced under vacuum sublimation parameters at our 62,718 m² manufacturing base, preserving molecular cell matrix integrity and natural aroma profiles.







62,718 m²
Industrial Footprint
37 Lines
Freeze-Drying Chambers
8,000 m²
Total Sublimation Area
41 Patents
Proprietary Technologies
Industrial Whitepaper: The Strategic Role of Lyophilized Banana Ingredients in El Salvador
While El Salvador is historically situated in a tropical bio-corridor celebrated for fresh Cavendish, Gros Michel, and criollo plantain crops, local industrial processors face pronounced vulnerabilities: tropical climatic fluctuations, post-harvest spoilage exceeding 28% in unchilled logistics lines, and intense enzymatic browning triggered by polyphenol oxidase (PPO) in warm ambient humidity. For industrial food operations centered around San Salvador, Santa Ana, San Miguel, and Puerto Acajutla, sourcing high-grade lyophilized (freeze-dried) banana ingredients transforms volatile agricultural inventory into an analytically uniform, room-temperature raw material.
At Fujian Fynergy Foods Co., Ltd., we bridge this operational divide. With more than two decades of cryogenic engineering, our facility operates 37 dedicated vacuum freeze-drying lines across 8,000 square meters of sublimation surface area. We process fully ripened bananas at the exact peak of Brix sweetness, utilizing rapid IQF flash freezing (-38°C) followed by secondary desorption under deep vacuum (<20 Pa). This process preserves over 96% of thermolabile micro-nutrients (potassium, vitamin B6, natural pectin) while maintaining pristine natural color without sulfites or artificial preservatives.
Integration & Processing
Localized Application Scenarios in El Salvador's Industrial Food Sector
How our freeze-dried banana slices, dices, and micronized powders solve technical formulation barriers across key Salvadoran production verticals.
Industrial Coffee & Banana Synergies
El Salvador's distinguished coffee sector (Bourbon and Pacamara varieties) is expanding rapidly into value-added RTD (Ready-To-Drink) cold brew beverages, instant functional lattes, and specialty coffee concentrates. Fresh banana purées present major problems with rapid sedimentation and phase separation when paired with acidic coffee extracts.
Our 80-120 mesh freeze-dried banana powder acts as an instant, 100% natural dispersible base. It imparts creamy mouthfeel, natural fruit sweetness, and authentic aromatics without triggering dairy-protein denaturation or creating gritty throat feel.
Cold Brew Premixes
Specialty Latte Formulations
Stable Emulsification
Export Bakery, Semita & Pastry Inclusions
Salvadoran commercial bakeries catering to both national supermarket chains (such as Super Selectos) and diaspora export lines throughout the United States face shelf-life limitations with traditional pastries like Semita de Piña o Plátano. Hot-air dehydrated banana gets tough, leathery, and darkens rapidly.
Fynergy's freeze-dried banana dices (5x5mm to 10x10mm) offer a light, porous cellular structure that absorbs butterfat and residual moisture evenly during baking. They remain tender yet structurally intact without caramelizing or burning under deck-oven temperatures.
Pan Dulce Inclusions
No Browning Under Bake Heat
Clean Label Decoration
Nutraceutical Premixes & Sports Nutrition
The growing fitness and wellness culture across urban Salvadoran hubs has catalyzed demand for high-potency sports electrolytes, vegan protein shakes, and recovery superfood blends. Potassium bioavailability and rapid rehydration are paramount for local athletes training in humid, high-heat environments.
Because our lyophilization is conducted at cryogenic sub-zero levels, the native potassium (approx. 1,400 mg/100g dry weight) and soluble dietary fiber remain unaltered. Our powder disperses smoothly in cold water, plant-based milks, or whey protein isolates without clump formation.
High Bioavailable Potassium
Meal Replacements
Clean Rehydration
Industrial Dairy, Yogurts & Frozen Confectionery
Salvadoran dairy brands face microbiological issues when introducing wet banana purée into yogurt, artisan ice cream, and chilled dairy desserts. High water activity ($a_w > 0.95$) encourages wild yeast bloom and molds, shortening supermarket shelf life.
Supplying freeze-dried banana flakes and powders with water activity below 0.25 ensures absolute microbiological safety. When blended into stirred yogurts or frozen dairy creams, it rehydrates smoothly without creating icicle crystals.
Zero Ice Crystallization
Low Water Activity (aw ≤ 0.25)
Extended Refrigerated Life
Technical Evaluation
Lyophilization (FD) vs. Conventional Hot-Air Drying (AD)
A side-by-side engineering comparison designed for Quality Assurance (QA) managers, procurement directors, and food scientists in Central America.
| Analytical Parameter | Fynergy Vacuum Freeze-Drying (FD) | Hot-Air Dehydration / Drum Drying (AD) | Formulator Impact in El Salvador |
|---|---|---|---|
| Drying Mechanism | Sublimation of frozen ice crystals directly to vapor (<20 Pa vacuum) | Thermal evaporation using heated forced air (65°C - 90°C) | Zero heat damage; cellular honeycomb remains uncollapsed |
| Residual Moisture Content | ≤ 3.0% - 5.0% (Controlled via moisture analyzers) | 8.0% - 15.0% (Substantial residual water) | Extended 18-24 month shelf stability even in high tropical humidity |
| Nutrient & Vitamin Retention | > 95% (Potassium, Vitamin C, Vitamin B6 preserved) | 30% - 50% (Extensive oxidation & thermal loss) | Allows functional front-of-pack health claims on clean labels |
| Aroma & Brix Flavor Profile | Intense, true-to-fruit aromatic esters, natural sweetness | Caramelized, scorched notes with oxidized flavor profile | Eliminates need for synthetic flavor enhancement agents |
| Rehydration Rate | Instant (15 - 45 seconds in ambient or cold fluids) | Slow and incomplete (10 - 20 minutes in hot water) | Perfect for instant beverage pouches and quick-dissolve shakes |
| Physical Matrix & Color | Crisp, airy texture; natural pale cream color without sulfites | Leathery, dense, rubbery; prone to enzymatic browning | Superior mouthfeel in RTE cereals, snack bags, and pastry toppings |
Market Dynamics
Market Trends Driving Freeze-Dried Demand in El Salvador
Strategic developments shaping the Salvadoran and wider Central American commercial food and beverage environment through 2026.
Surging Clean-Label & Anti-Sugar Consumer Demands
Salvadoran consumers are paying closer attention to nutritional panels. With rising regulatory attention to front-of-pack warning labels across Latin America, large manufacturers are seeking natural ways to reduce refined cane sugar.
Freeze-dried banana powder contains naturally concentrated fructose and glucose accompanied by whole dietary fiber, enabling R&D teams to replace artificial sweeteners and high-fructose corn syrups with recognizable "100% Real Fruit" ingredients.
Modern Retail Expansion & Private-Label Snacking
The expansion of modern grocery retailers, including Walmart Central America, Super Selectos, and convenience chains like Pronto, has created rapid growth in healthy grab-and-go convenience snacks.
Freeze-dried banana slices in moisture-barrier stand-up pouches (Doypack) represent a high-margin, shelf-stable SKU. They do not melt or degrade in warm coastal climates, outperforming chocolate-coated and fragile confectionery snacks.
Strengthened Logistics Links via Puerto de Acajutla
With modern trans-Pacific container freight corridors connecting Xiamen and Shanghai directly to the Port of Acajutla, Salvadoran importers now benefit from dependable maritime lead times.
Standardizing on lyophilized banana avoids the high reefer freight costs and temperature-breakage risks of frozen purées. Shipped in desiccated, nitrogen-flushed multi-wall barrier cartons, these ingredients arrive ready for immediate factory storage without specialized refrigeration.
Procurement Dossier
Frequently Asked Questions by Salvadoran Importers & QA Teams
Direct, practical guidance covering tariffs, moisture control, import documentation, and sample evaluation.
What are the import procedures, customs clearance documentation, and tariff classifications for El Salvador?
Freeze-dried banana products are imported into El Salvador under Central American Tariff System (SAC / Sistema Arancelario Centroamericano) classifications, typically falling under HS Code 0803.90.11 or 0811.90 for fruit preparations, or 1106.30 for banana flour/powder. Fujian Fynergy Foods Co., Ltd. provides all essential commercial export documentation required by the Ministry of Health (MINSAL) and customs authority (Dirección General de Aduanas - DGA):
- Certificate of Analysis (COA) with complete microbiological and heavy metal assay per production lot.
- Official Phytosanitary Certificate issued by entry-exit inspection authorities.
- Certificate of Origin for smooth customs processing.
- Detailed Commercial Invoice, Packing List, and Clean On-Board Bill of Lading (B/L).
- Third-party BRCGS, HACCP, and ISO 22000 certificate copies to accelerate sanitary registration.
How does your factory protect freeze-dried banana from El Salvador's high tropical humidity?
Lyophilized banana is inherently hygroscopic: exposure to ambient humidity ($> 65\%$) can cause moisture reabsorption, resulting in structural collapse and loss of crunch within minutes. To prevent this, all sorting, dicing, milling, and packing operations at Fynergy take place inside Class-100,000 cleanrooms equipped with industrial dehumidification systems maintaining relative humidity strictly below 35%.
For bulk deliveries to El Salvador, products are packed inside heavy-gauge, heat-sealed aluminum-laminated bags or virgin dual-layer polyethylene liners with food-grade desiccant packets, encased within double-wall corrugated export master cartons. For private-label retail projects, we use high-barrier multi-layer metallized films (PET/AL/PE or PET/VMPET/PE) with hermetic zipper seals.
What are the Minimum Order Quantities (MOQ) and lead times for shipping to Puerto de Acajutla?
For bulk freeze-dried banana ingredients (slices, dices, powder), our standard production MOQ begins at 500 kg to 1,000 kg per SKU. For custom private-label pre-packaged retail pouches, the MOQ starts at 10,000 to 30,000 units depending on pouch format and print cylinder parameters.
Production lead times for standardized bulk orders run between 15 to 25 business days following formula and spec sign-off. Maritime transit from our primary dispatch ports (Xiamen or Shenzhen) to Puerto de Acajutla generally ranges between 26 and 34 days, depending on shipping line routing.
Can Salvadoran buyers request custom particle cuts, sugar-free profiles, or proprietary blends?
Yes. Fynergy is a certified custom OEM/ODM contract manufacturer. We tailor our processing lines to match your specific production requirements:
- Cut Formats: Whole fruit, 3mm/5mm/7mm transverse slices, 6x6mm and 10x10mm dices, granules, and fine powders from 40 to 120 mesh.
- Formulation Control: 100% pure single-ingredient banana with zero carriers, or co-milled functional formulations integrated with oat fiber, whey protein, or plant extract powders.
- Clean-Label Positioning: Non-GMO, zero added sugars, non-irradiated, and completely free from artificial stabilizers.
What laboratory validation and safety checks are performed before dispatch?
Every production lot undergoes rigorous multi-point analysis in our in-house quality testing facility prior to export release. We employ liquid chromatography, atomic absorption spectrophotometers, microplate readers, and automated Kjeldahl apparatus to verify:
- Microbiology: Aerobic Plate Count (≤ 10,000 CFU/g), Coliforms (≤ 10 CFU/g), Yeast & Mold (≤ 50 CFU/g), Salmonella (Negative/25g), E. Coli (Negative/10g).
- Heavy Metals: Strict verification for Lead (Pb), Arsenic (As), Cadmium (Cd), and Mercury (Hg) compliant with CODEX Alimentarius and US FDA thresholds.
- Physical Parameters: Moisture content via Karl Fischer titration and water activity ($a_w$) analysis.
Manufacturing Benchmark
Why Fynergy is the Preferred Global Freeze-Drying Partner
High-volume processing capacity, audited food safety frameworks, and dedicated R&D engineering support global enterprises, multinational brands, and Fortune 500 supply chains.
Class-100,000 Cleanroom Processing
Our manufacturing workshops are built to medical cleanroom standards. Air filtering, differential positive pressure controls, and rigorous personnel disinfection prevent cross-contamination, ensuring that delicate, low-moisture freeze-dried products remain hygienically clean.
37 Automated Industrial Freeze-Drying Lines
With 8,000 square meters of sublimation chamber area supported by automated pre-cooling tunnels, robotic tray systems, and computerized vacuum controls, we provide batch-to-batch consistency and scale for multi-container contracts.
Audited Food Safety & Onsite Verification
Certified under BRCGS (Grade A), HACCP, and ISO 22000, with onsite facility audits verified by TÜV Rheinland. We also provide Halal and Kosher certified production lines for international distribution.
Comprehensive R&D & In-House Lab Testing
Equipped with 41 authorized patents, our technology center works with universities and industry standard committees. Our on-site lab handles atomic absorption, HPLC chromatography, and allergen screens directly, eliminating testing delays.
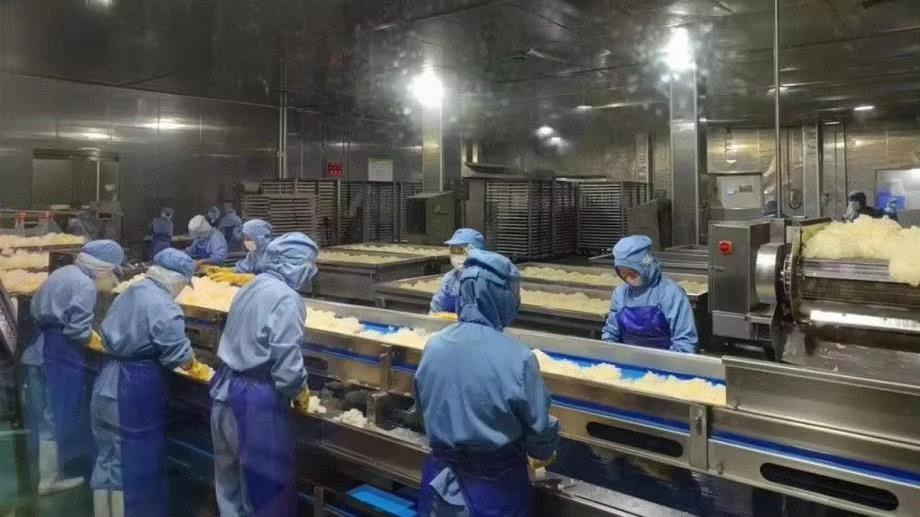 1. Automated Cleaning Line
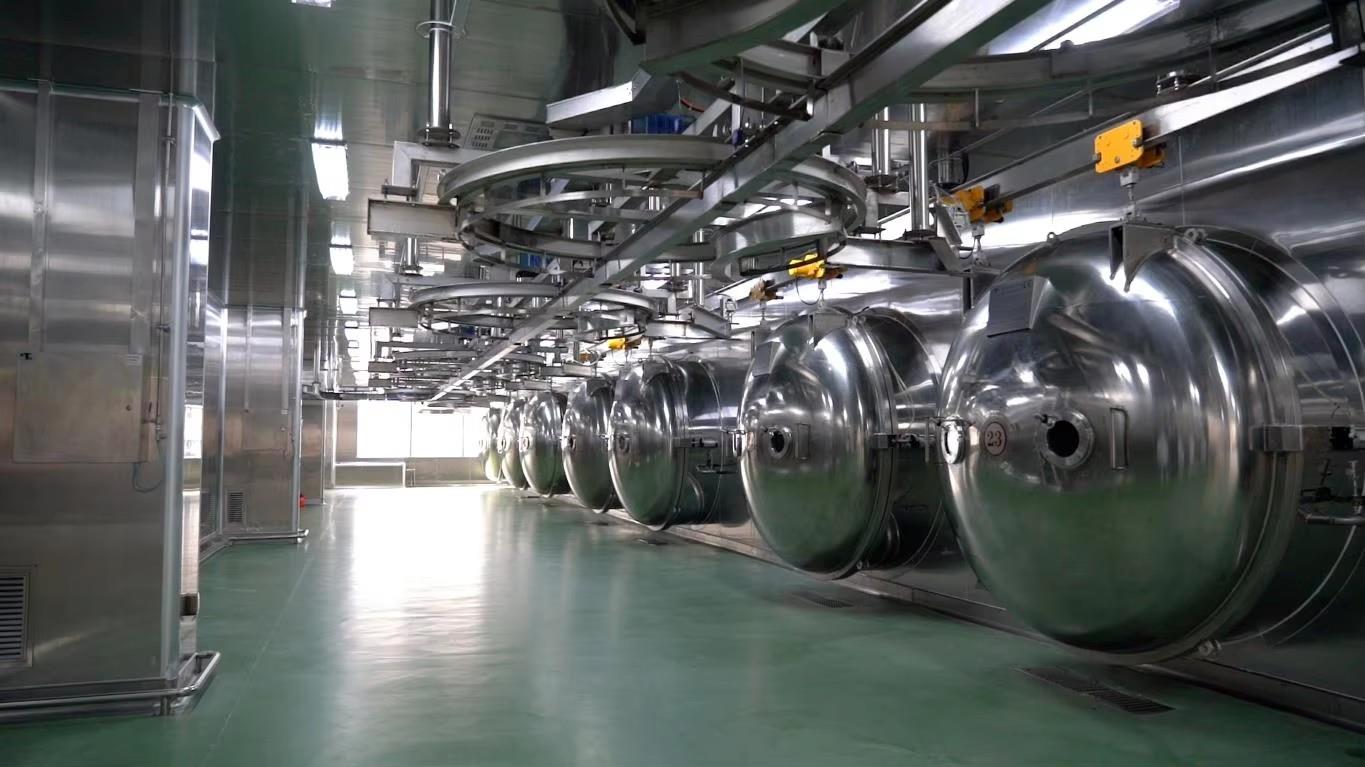 2. Cryogenic Freeze Chambers
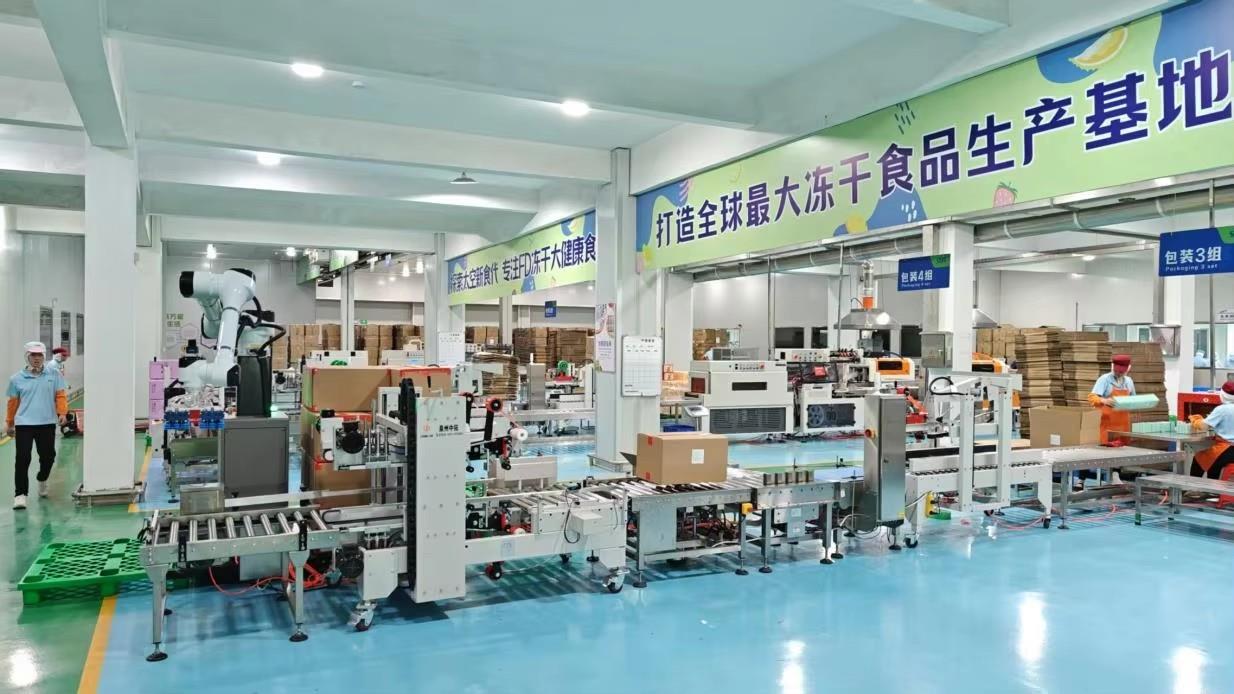 3. Cleanroom Packaging Systems
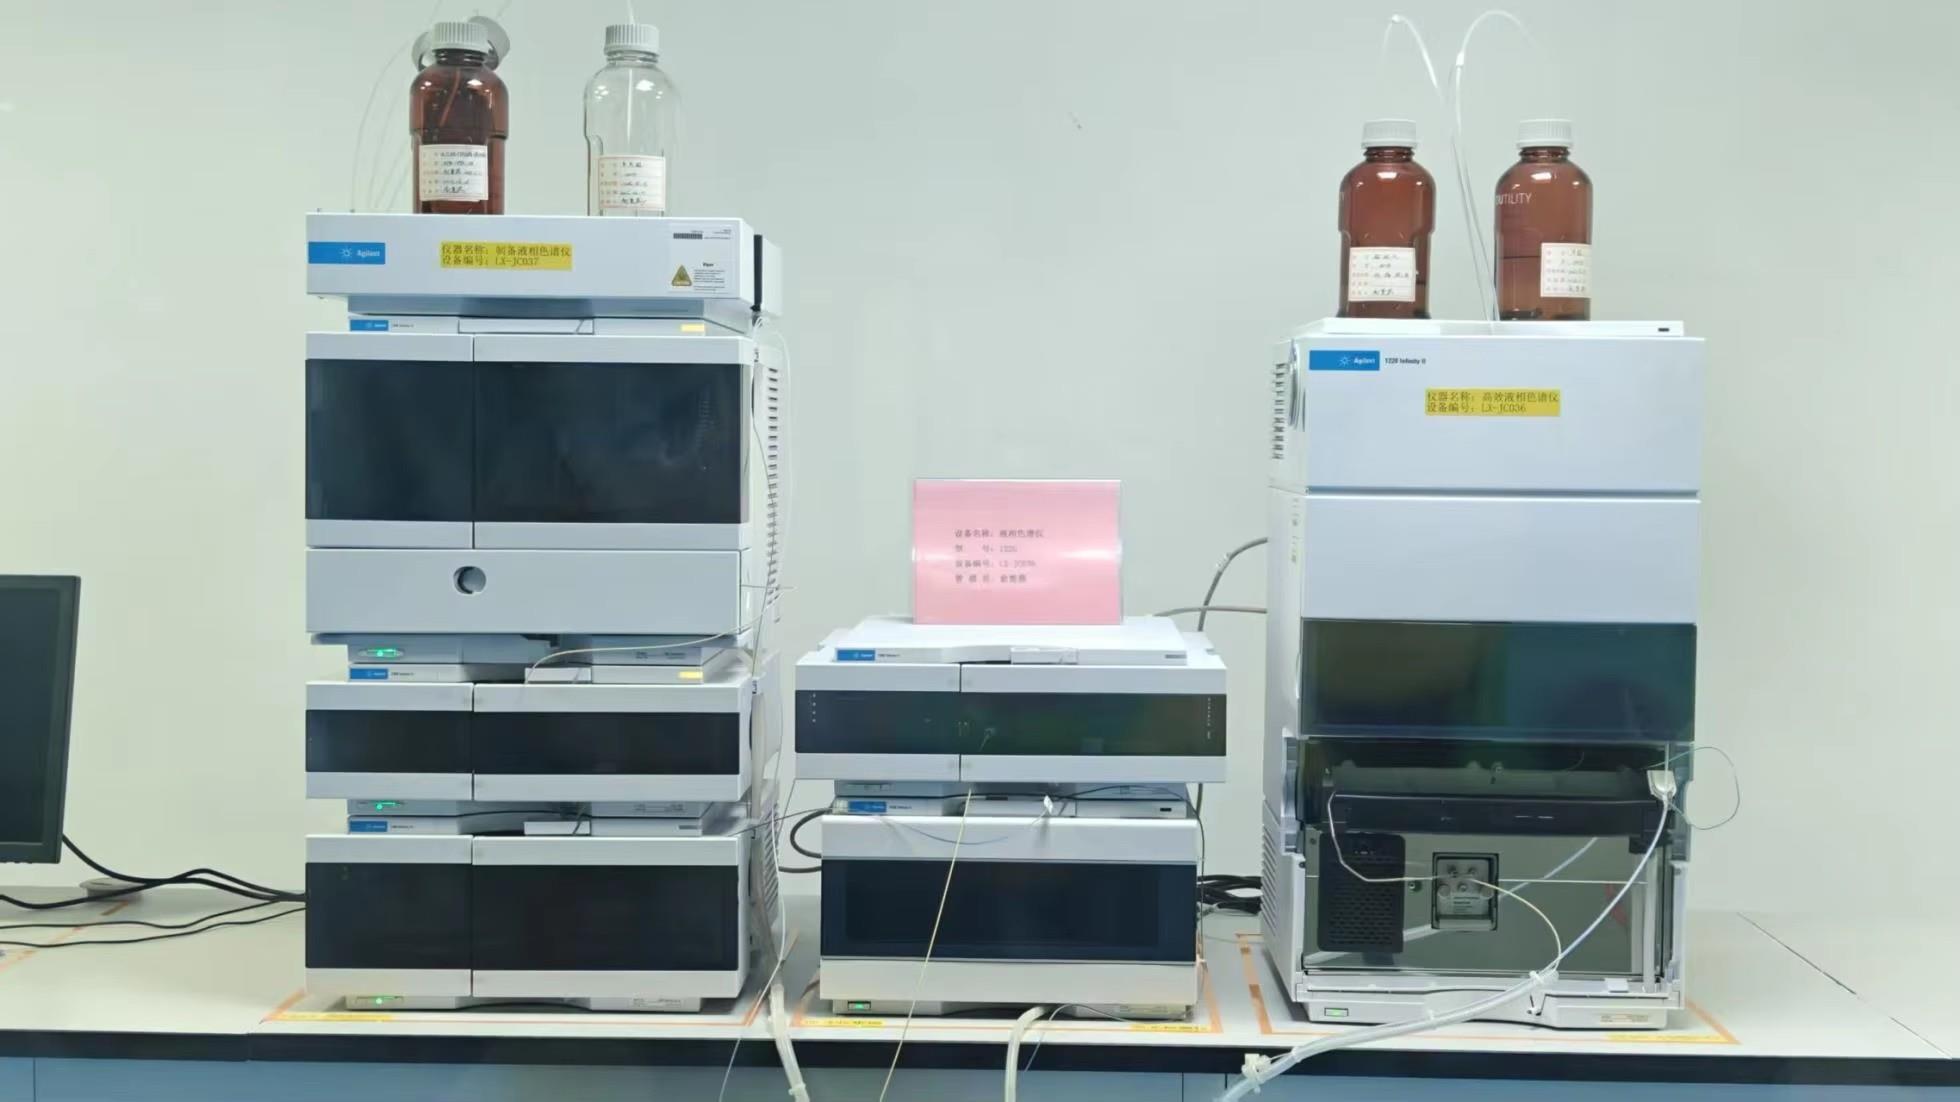 4. HPLC Chromatography Testing
Initiate Your Freeze-Dried Banana Supply Line for El Salvador
Connect directly with our export engineering and food formulation team. Receive detailed technical spec sheets, full microbiological dossiers, custom cut sizing options, and express air courier sample kits for your laboratory testing.
Contact Us
Free Sample Kits with Official Lot COA
Direct Acajutla Port CIF Pricing Models
Complete BRCGS / ISO 22000 Technical Dossiers
Custom Slicing, Milling & OEM Packaging