Organic Bulk

Explore our core dehydrated lines, manufactured in Class-100,000 cleanrooms under strict vacuum sublimation parameters for rapid rehydration and volatile retention.







Commercial allium dehydration demands acute thermal-vacuum equilibrium. Conventional hot-air drying invariably destroys the volatile organosulfur enzymes—principally alliinase and isoalliin—collapsing cellular walls into dense, leathery sheets with degraded lachrymatory potency and caramelized, scorched discoloration.
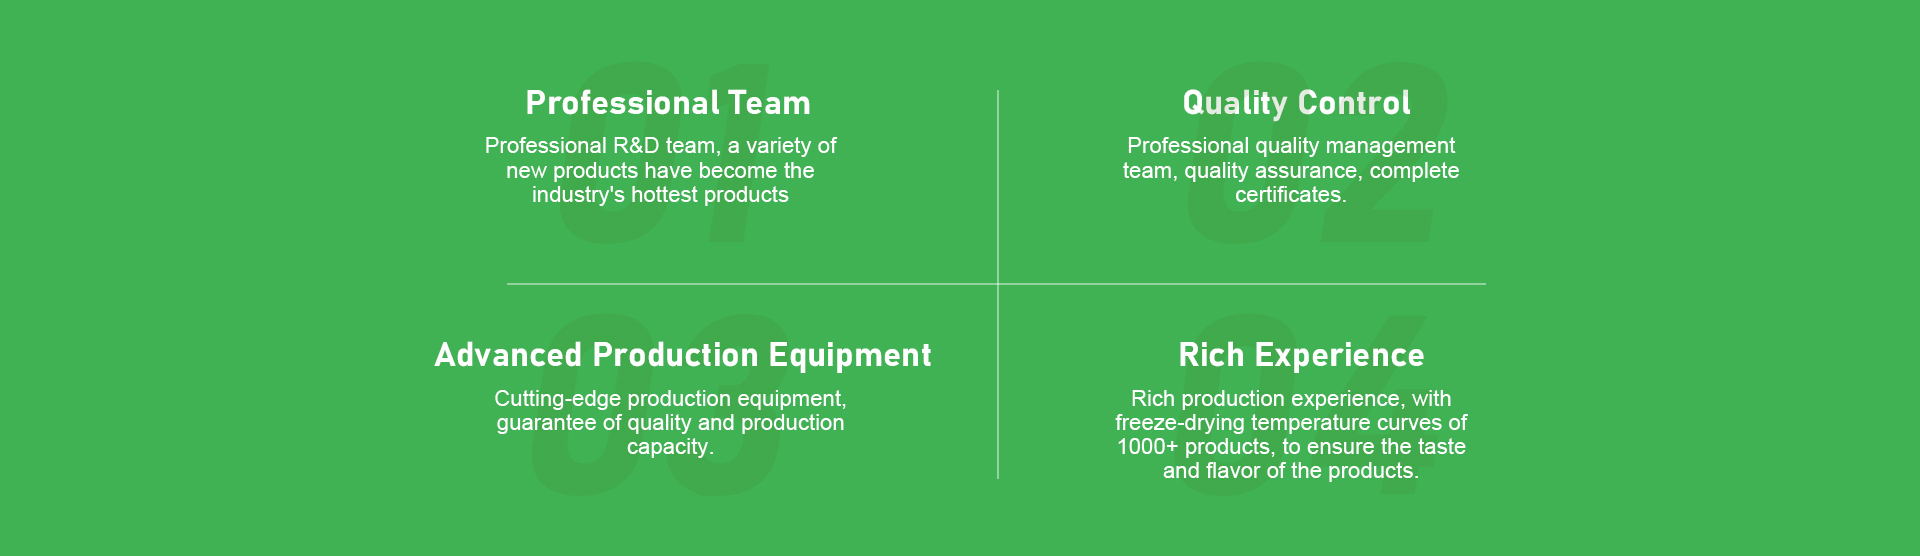
Our Zhangzhou installation deploys rapid hyper-cryogenic blast freezing (-40°C) followed by sublimation under high vacuum (≤ 20 Pa). This locks the moisture crystals in a static ice matrix, allowing direct solid-to-gas transition. The biological cell membranes of the Allium cepa remain intact, creating an ultra-porous, cellular honeycomb that guarantees instant rehydration within 30 to 45 seconds in warm aqueous formulations.
| Quality Parameter | Vacuum Freeze-Drying (FD) | Standard Hot Air Drying (AD) |
|---|---|---|
| Allicin & Flavor Integrity | 92% – 97% Retained | 20% – 35% (Severe Thermal Loss) |
| Rehydration Speed | 30 – 45 Seconds Complete | 12 – 20 Minutes (Incomplete Core) |
| Residual Moisture Spec | ≤ 3.0% – 5.0% Critical | 8.0% – 14.0% (Risk of Caking) |
| Bulk Density Uniformity | 0.12 – 0.22 g/cm³ (Fluffy/Crisp) | 0.35 – 0.55 g/cm³ (Dense/Hard) |
From seed cultivation surveillance to international regulatory customs clearance, we eliminate supply vulnerability for supermarket supply chains, spice processors, and FMCG conglomerates.
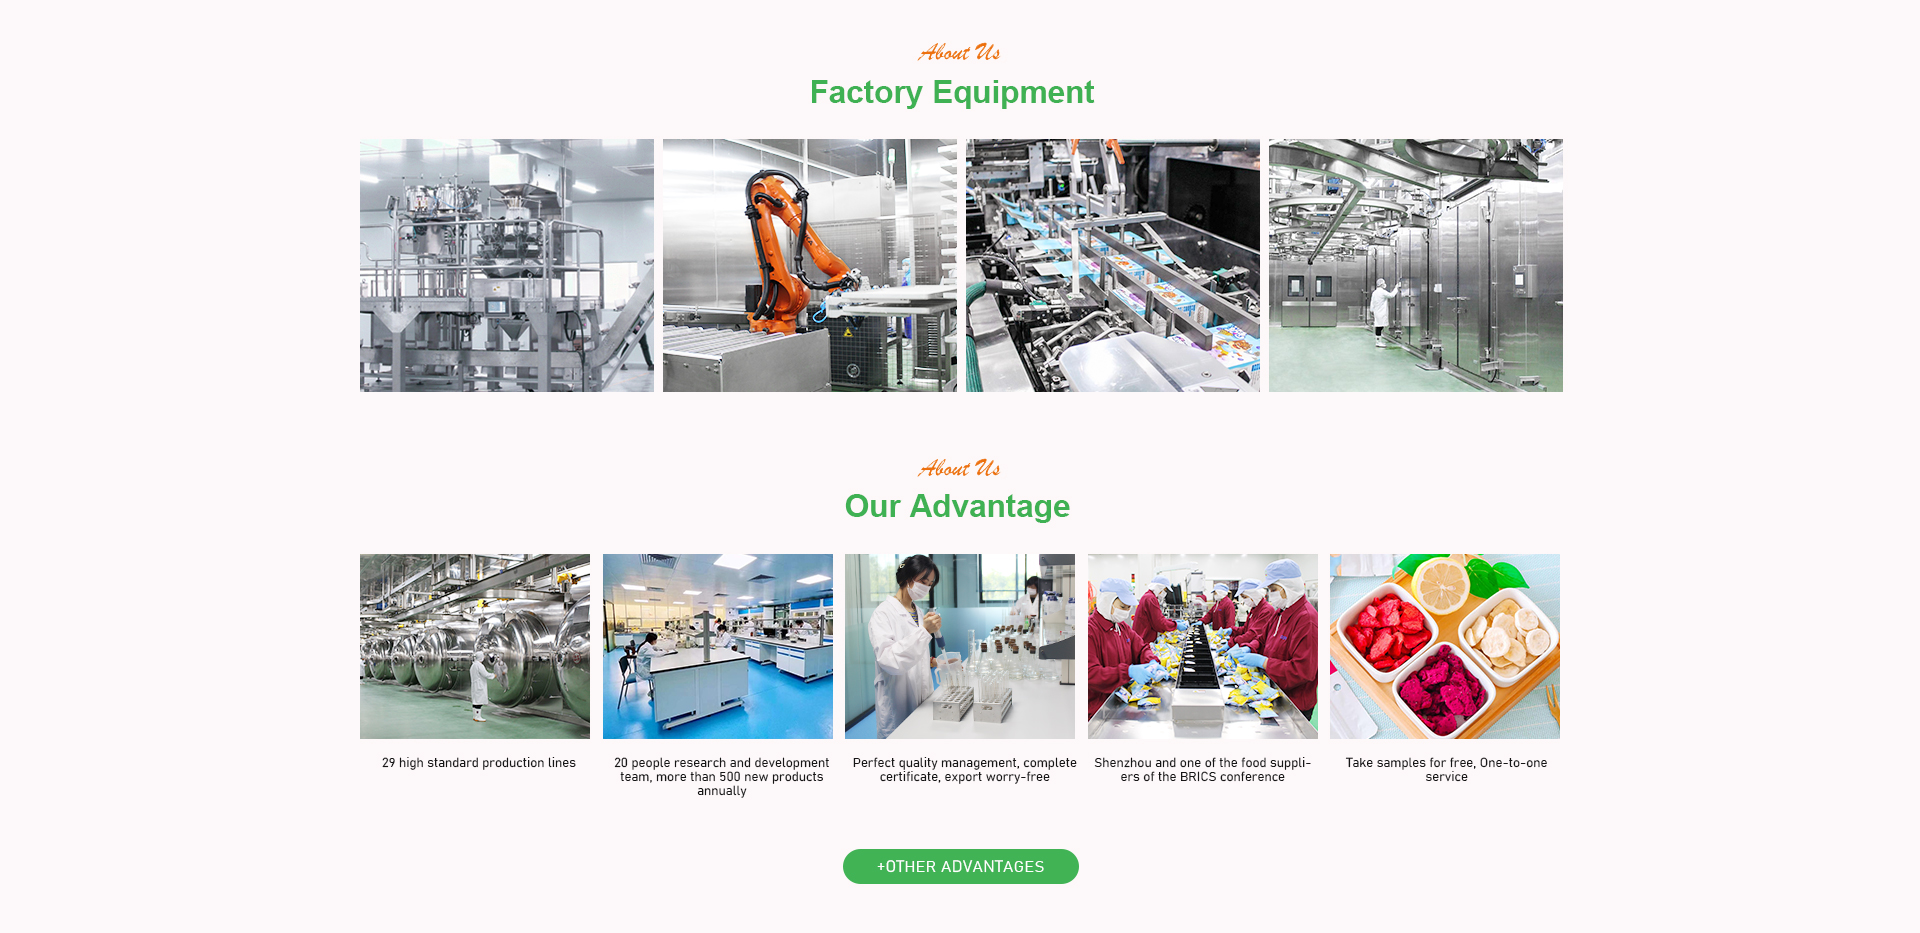
Operating across a dedicated 62,718 m² footprint equipped with 37 continuous freeze-drying lines and approximately 8,000 m² of internal vacuum chamber volume. We provide uninterrupted capacity for multi-container enterprise contracts without seasonal disruption.
Fully compliant with global consumer benchmarks: verified onsite by TÜV Rheinland, certified under BRCGS Global Food Safety Standard (Issue 9), HACCP Hazard Control, and ISO 22000, complemented by certified Kosher and Halal production circuits.
Our internal analytical laboratory utilizes advanced high-performance Liquid Chromatography (HPLC), Atomic Absorption Spectrophotometry, Atomic Fluorescence, and automated Kjeldahl apparatus for meticulous screening of pesticide residue, mycotoxins, and heavy metals.
Engineering customized onion profiles to exact technical dossiers: whole onion bulbs, cut slices (3mm/5mm), precision cross-cut dices (4x4mm, 6x6mm, 10x10mm), granules, and superfine 80-120 mesh powders formulated for slurry blending and spice applications.
Ultra-low dew point packing operations with in-line metal detection, X-ray scanning, and nitrogen flush sealing. Packaged in multilayer aluminum foil barrier pouches or heavy-duty food-grade poly-lined cartons designed to conquer trans-oceanic humidities.
Critical market shifts reshaping freeze-dried onion and botanical vegetable procurement across Europe, North America, and the Asia-Pacific through 2030.
Global regulatory bodies are accelerating mandatory sodium restrictions in processed foods. Food formulators are leveraging freeze-dried onion powder as an active clean-label flavor modulator. Due to non-thermal sublimation, the naturally occurring glutamic acid precursors and pungent thiosulfinates remain intact, creating an intense savory profile that allows developers to reduce NaCl concentrations by up to 25% without sacrificing customer flavor perception.
The explosive consumer adoption of premium instant noodles, freeze-dried camping rations, meal kits, and institutional soups demands rehydration parity. Standard dehydrated onion requires up to 15 minutes of boiling to reconstitute, often remaining rubbery. High-porosity freeze-dried onion flakes rehydrate seamlessly within 30 to 45 seconds upon hot broth contact, matching modern short-cycle noodles perfectly.
Supply chain auditors have banned artificial radiation and ethylene oxide (EtO) sterilization due to persistent carcinogenic residues. The procurement trend strongly favors manufacturers with closed-loop sanitary cleanrooms, integrated ozonated wash systems, and validated steam microbial reduction steps that satisfy strict EU MRL (Maximum Residue Limit) protocols without degradation.
Volatile oceanic freight rates and erratic geopolitical tariffs are driving procurement directors away from multi-tiered merchant brokers. Sourcing teams are locking long-term master contracts directly with primary manufacturers possessing in-house raw agro-intake, processing chambers, and certified testing facilities to ensure absolute traceability back to farming cooperatives.
Future-forward ESG mandates demand radical reductions in commercial post-harvest loss. By transforming graded, farm-fresh onion surpluses directly into shelf-stable (24-month) freeze-dried formats at origin, Fynergy mitigates massive organic spoilage typical of raw vegetable transit.
Furthermore, freeze-dried onion eliminates over 88% of transport cargo mass without requiring energy-intensive refrigerated reefer containers during shipping, drastically shrinking the overall carbon footprint per metric ton of delivered flavor solids.
Everything QA executives, food formulators, and supply chain managers require prior to contract finalization and PO issuance.
We supply freeze-dried onion in diverse granulometries tailored to specific industrial uses: Whole Ring/Slices (3mm & 5mm), Precision Minced Dices (3x3mm, 6x6mm, 10x10mm), Chopped Flakes, and Fine Particle Powders (40 mesh, 80 mesh, and ultra-fine 100 mesh). Custom sieving parameters and bulk density adjustments are engineered upon request for continuous automatic dosing systems.
For standard bulk cartons of freeze-dried vegetables and onions, our baseline MOQ starts at 500 kg to 1,000 kg depending on specific cut geometry. For customized retail pouches, canisters, or private label programs, standard runs typically begin at 5,000 to 10,000 units. We provide fully qualified 100g to 500g analytical evaluation samples complete with Comprehensive Certificates of Analysis (COA) to verified R&D teams prior to production.
Because freeze-dried allium products exhibit critical moisture sorption isotherms (≤ 4% moisture content), they are naturally hygroscopic. All post-sublimation crushing, sieving, and packing are conducted in relative humidity (RH ≤ 30%) and temperature-controlled cleanroom facilities. The finished product is sealed within heavy-gauge aluminum foil-laminated barrier pouches with nitrogen (N2) flushing, preventing clumping and oxidative flavor degradation over a guaranteed 24-month shelf life.
Fujian Fynergy Foods maintains transparent supply chain verification. We welcome third-party technical factory audits and are certified under BRCGS (Global Standard for Food Safety Issue 9), HACCP systems, and ISO 22000:2018. We provide full multi-residue pesticide test panels, microbial safety data (Salmonella negative, E. coli < 10 CFU/g, total plate counts under strict limits), heavy metal screening, non-GMO declarations, and allergen control validations.
Yes. As a recognized full-category freeze-dried manufacturer operating 37 continuous lines, we maintain specialized ribbon blending and micro-dosing systems. We formulate custom culinary seasonings, soup bases, and dip mixes blending freeze-dried onion with our own freeze-dried garlic, green peas, sweet corn, spinach, mushrooms, and spray-dried tea or culinary extracts.
Direct communication with our technical sales engineers in Zhangzhou, Fujian. Receive tailored product cut specifications, laboratory COA documentation, and volume-tiered price quotations.
Send an Inquiry