
37
FD Processing Lines
62,718 m²
Total Processing Base
≤ 5.0%
Target Moisture Spec
BRCGS / HACCP
Dual Certified Safety
Featured Industrial Freeze-Dried & Extracted Portfolio
Manufactured across Class-100,000 cleanroom vacuum drying suites. Optimized for moisture barrier packaging, immediate solubility, and natural color preservation.







Industrial Freeze-Dried Blueberry Manufacturing White Paper
Engineering structural porosity, retaining anthocyanin biomarkers, and establishing clean-label compliance for enterprise B2B procurement pipelines.
Sublimation Physics
Unlike thermal air-drying, which induces cellular collapse and structural case-hardening, our industrial lyophilization transitions berry moisture directly from ice to vapor at pressures below 6.11 mbar. This maintains cell wall integrity and eliminates chemical cross-linking of surface sugars.
Anthocyanin Biomarkers
Cyanidin-3-glucoside and delphinidin compounds degrade rapidly above 55°C. By limiting sublimation plate temperatures within an audited window (-35°C to +40°C), our blueberries achieve an independently verified polyphenol retention rate exceeding 93.8% across production batches.
Controlled Porosity & Water Activity
Our computerized condenser staging ensures final water activity ($a_w$) remains strictly beneath 0.28, stopping non-enzymatic browning and bacterial proliferation. Highly porous microstructures guarantee instant rehydration kinetics for instant dairy and beverage applications.
Critical Quality Control Specifications (Freeze Dried Blueberry)
Standard analytical parameters verified batch-by-batch via in-house liquid chromatography and atomic absorption instrumentation.
| Analytical Parameter | Whole Berries (Grade A) | Crushed Dices (1–3mm / 2–5mm) | Micronized Powder (>100 Mesh) | Testing Protocol |
|---|---|---|---|---|
| Moisture Content | ≤ 4.0% | ≤ 3.5% | ≤ 3.0% | Karl Fischer / Vacuum Oven 70°C |
| Water Activity ($a_w$) | 0.20 – 0.26 | 0.20 – 0.25 | 0.18 – 0.24 | Chilled Mirror Dew Point Method |
| Anthocyanin Content | ≥ 480 mg / 100g | ≥ 450 mg / 100g | ≥ 420 mg / 100g | HPLC-UV/VIS Detection |
| Rehydration Speed | 35 – 50 seconds | 15 – 25 seconds | Instant Dissolution | Standard Water Immersion (25°C) |
| Aerobic Colony Count | < 5,000 CFU/g | < 5,000 CFU/g | < 3,000 CFU/g | ISO 4833-1 Microbial Enumeration |
| Heavy Metals (Pb, As, Cd) | Conforms to EU/FDA | Conforms to EU/FDA | Conforms to EU/FDA | Atomic Absorption Spectrophotometry |
Automated Manufacturing & Testing Facility
37 lyophilization tunnels, cleanrooms, and testing infrastructure located in Zhangzhou, Fujian.
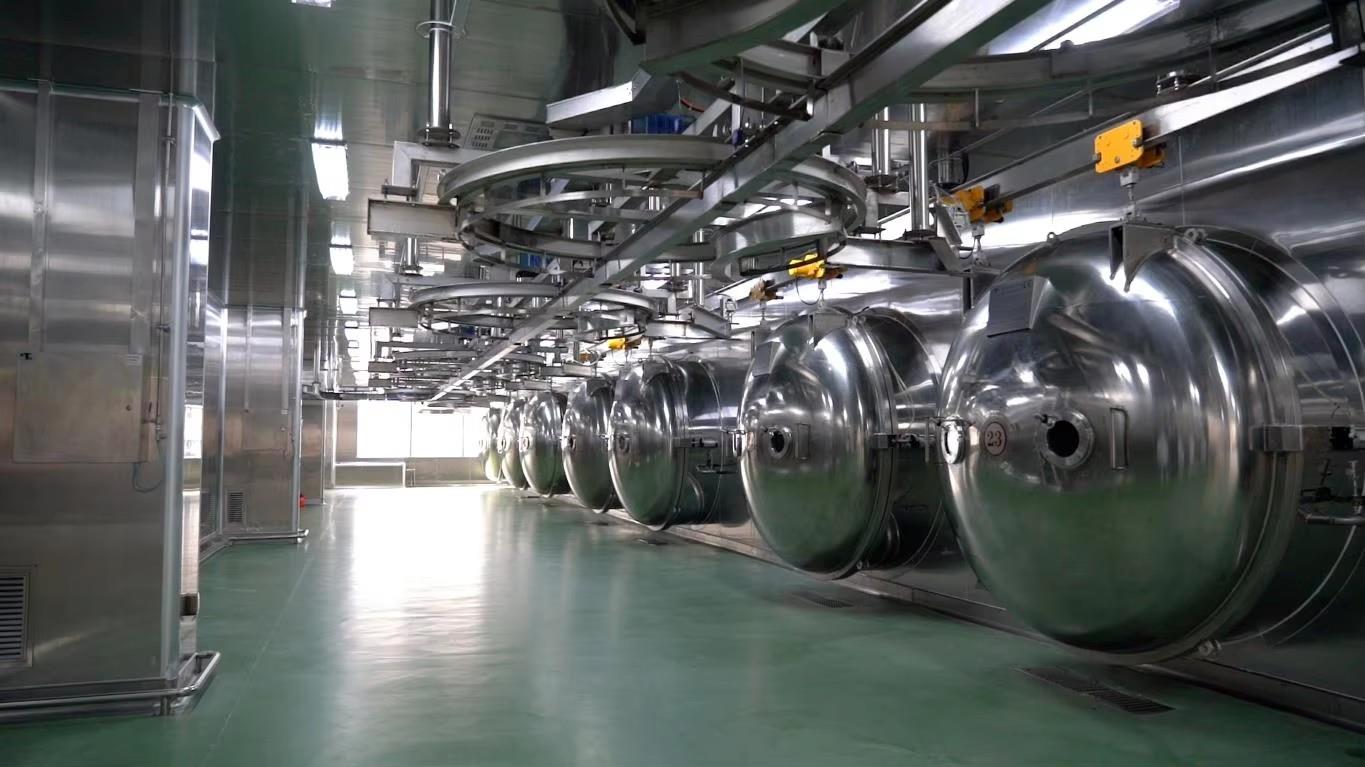
Vacuum Freeze Drying Chambers
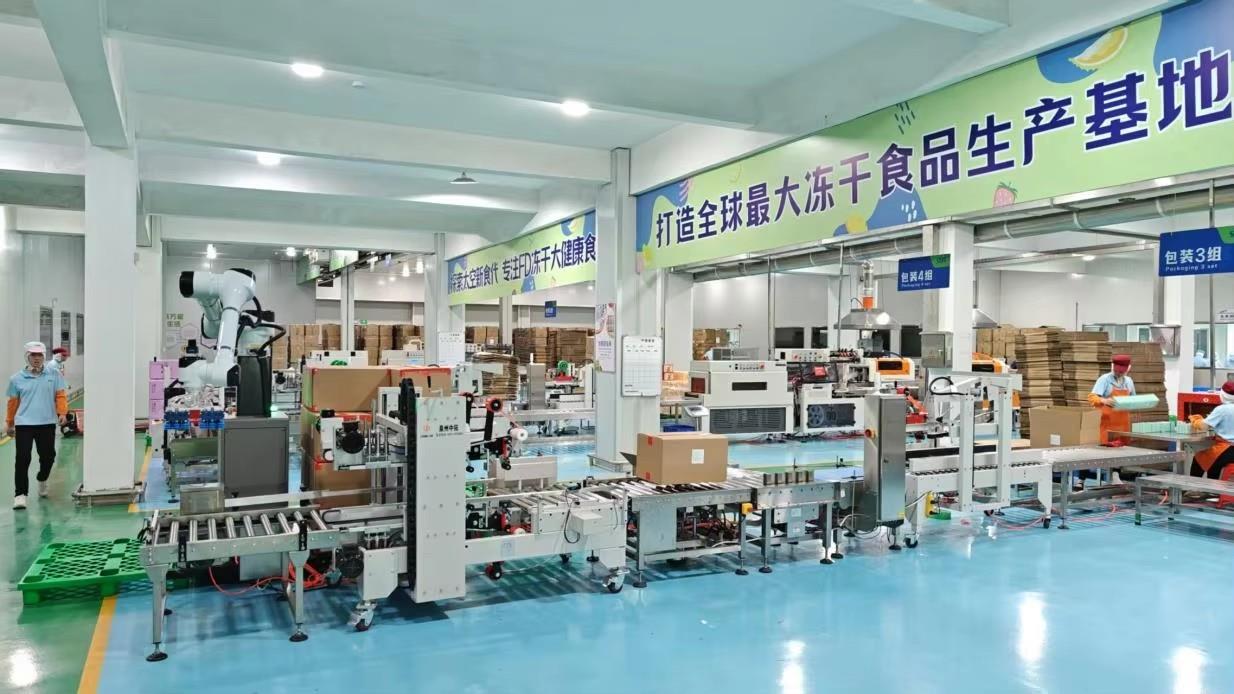
Cleanroom Automatic Packaging Line
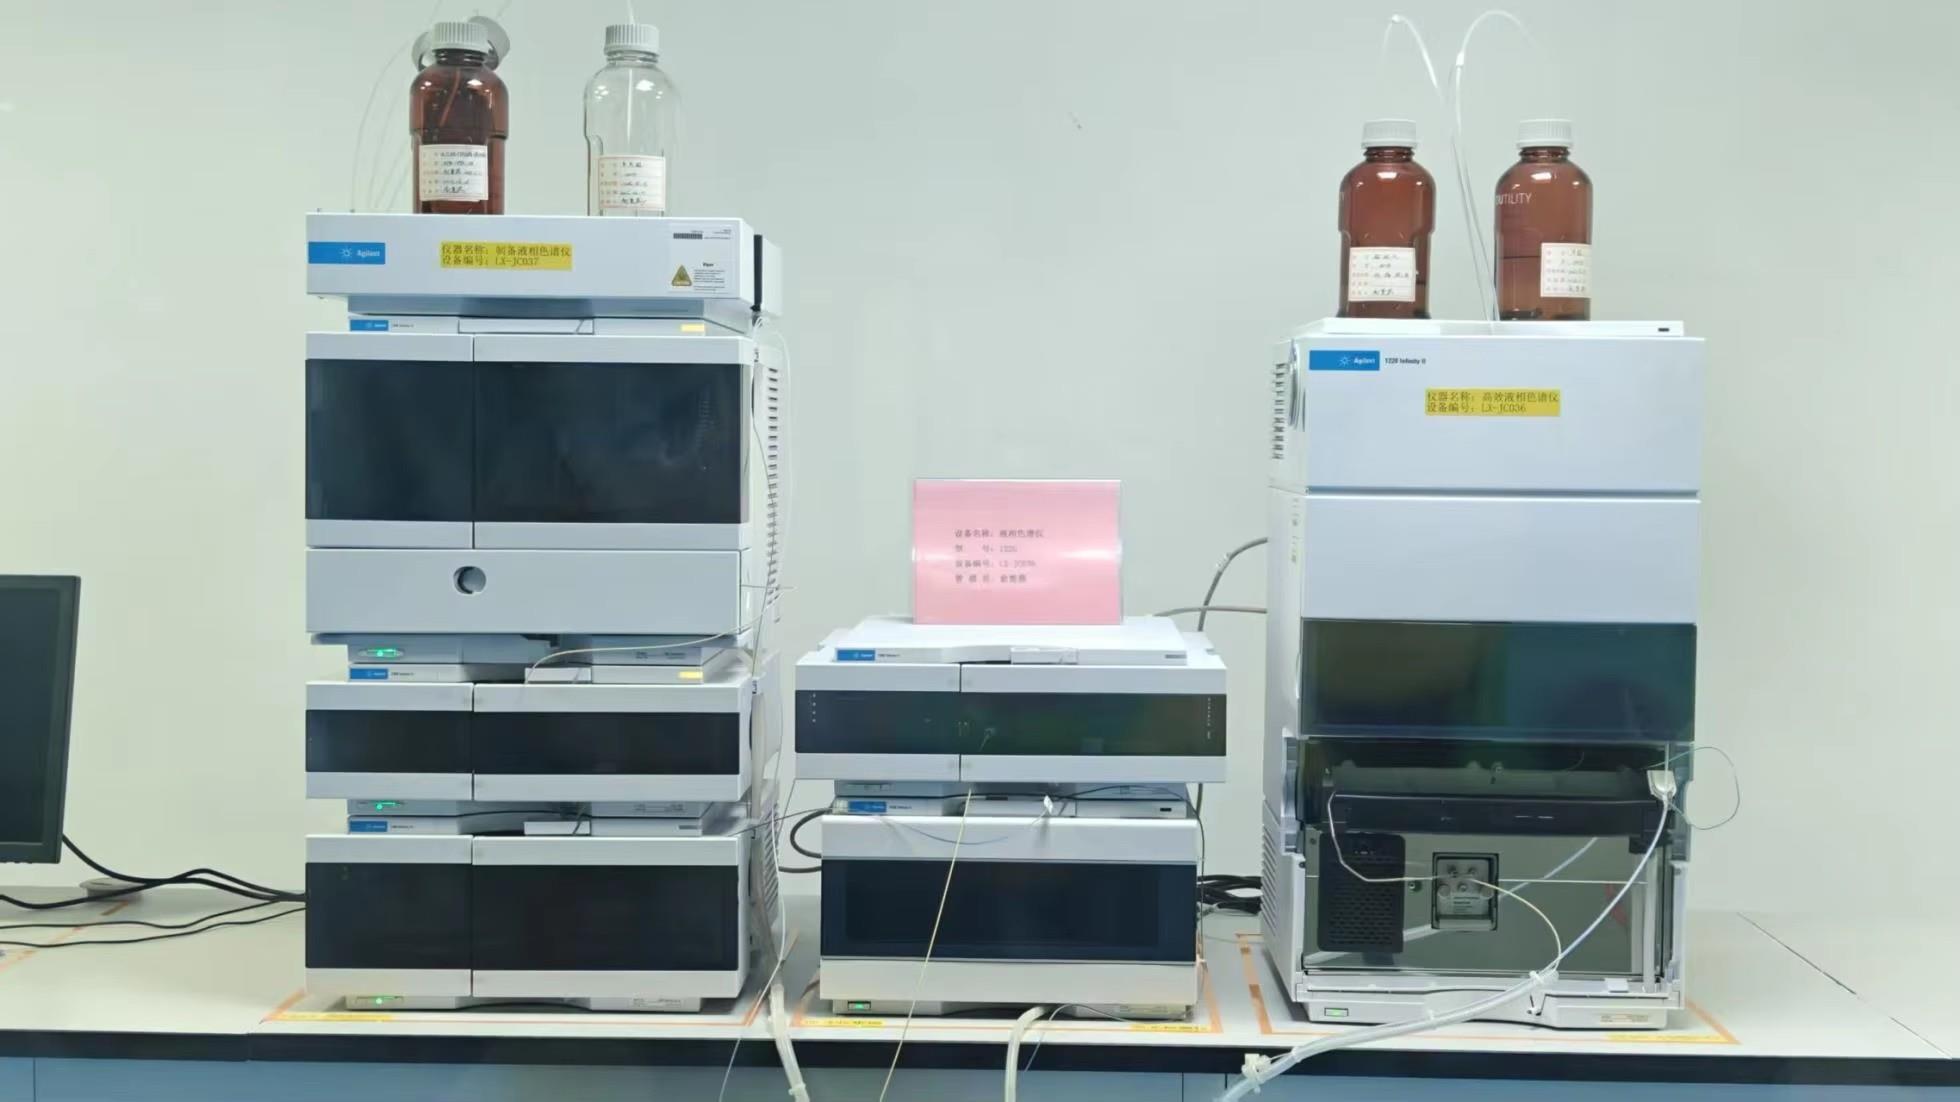
Liquid Chromatography Lab Station
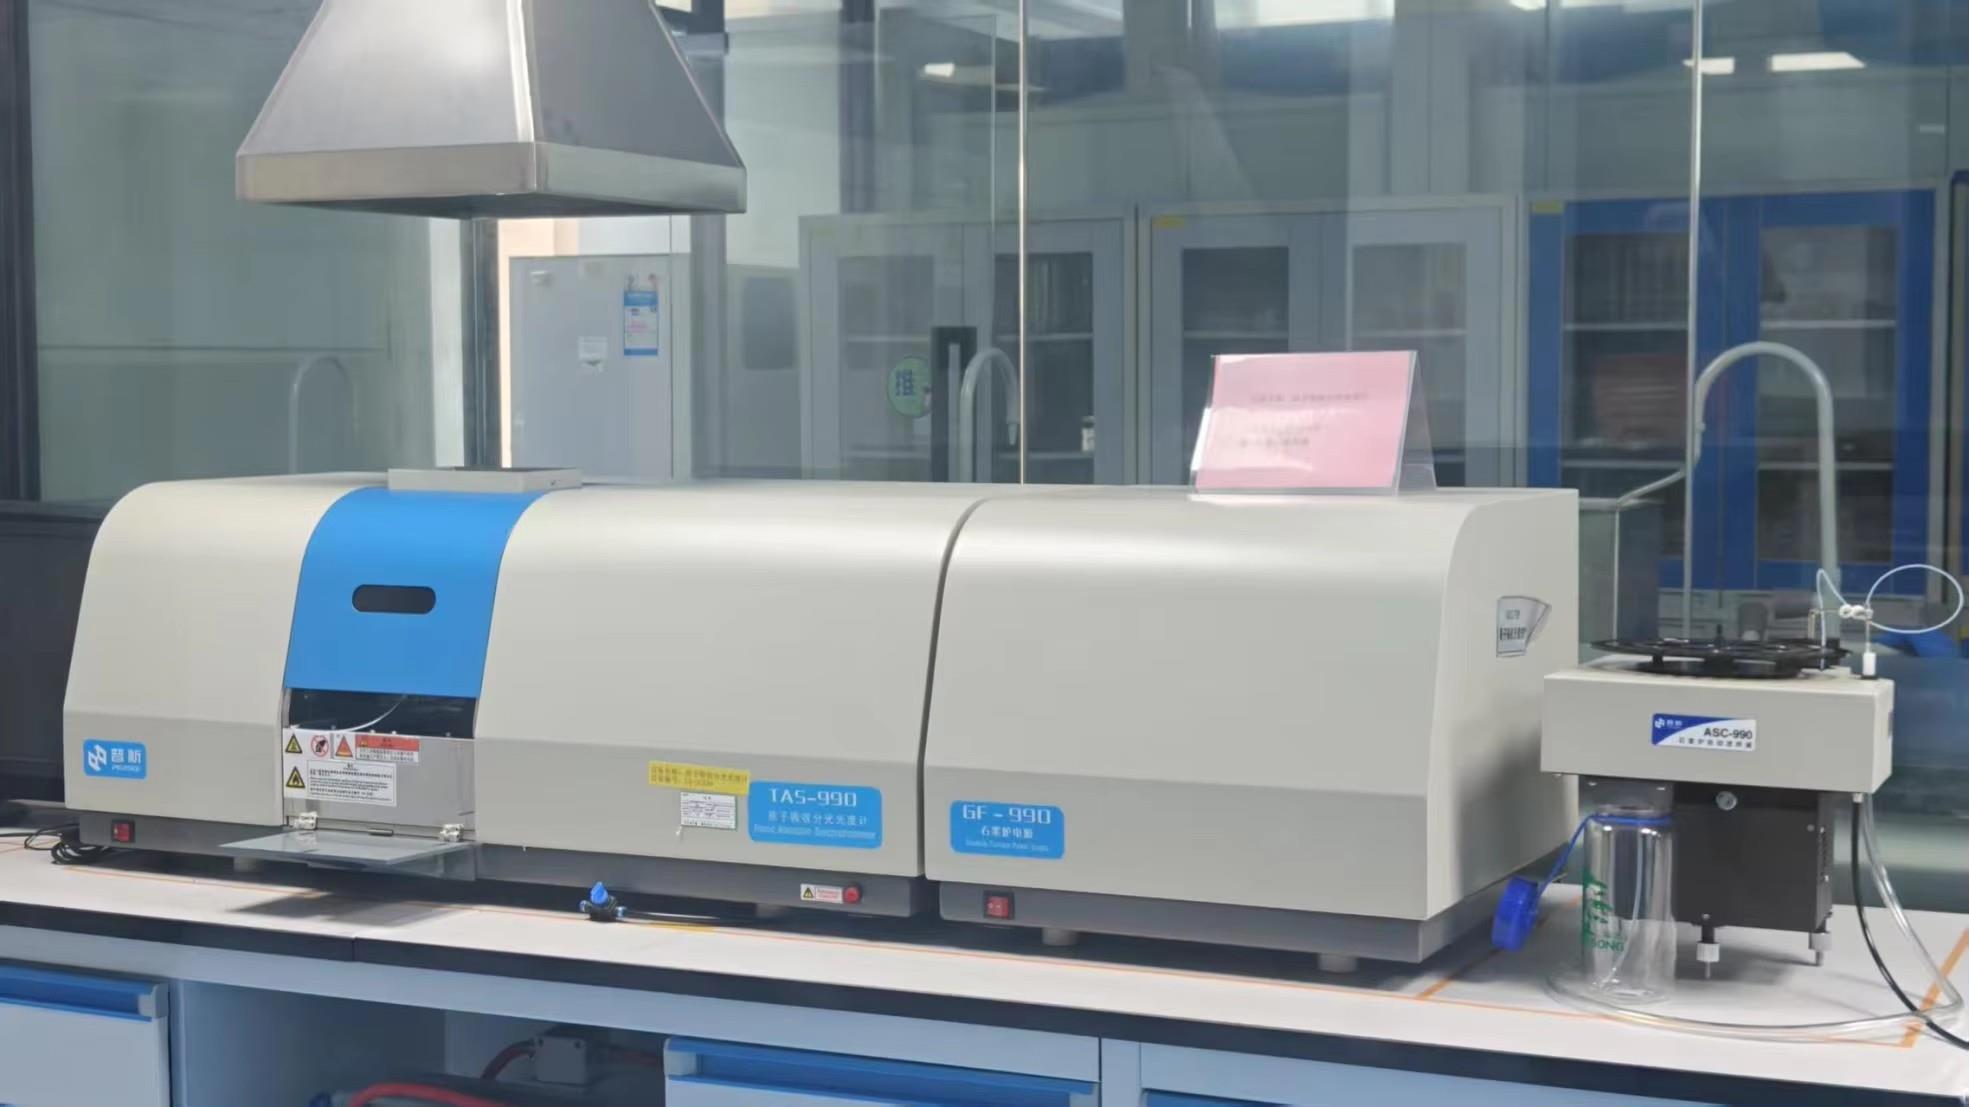
Atomic Absorption Trace Metal Analysis
Future Procurement Forecast & Sourcing Vectors (2025–2030)
Strategic shifts reshaping bulk contract negotiations, supplier audits, and clean-label ingredient portfolios.
Upgraded Clean-Label Mandates
Global brands are phasing out artificial purple lake dyes and sugar-infused dried blueberries. The demand vector is moving toward 100% pure freeze-dried blueberry powders acting simultaneously as active functional nutrients and natural colorants in clean-label RTDs, protein shakes, and toddler nutrition.
Cold-Water Instant Dispersibility
Standard fruit powders often clump in cold milk, tea, or water without anti-caking additives. Enterprise buyers are contracting for fluid-bed agglomerated and custom-micronized blueberry powders that guarantee complete suspension without synthetic dispersion agents.
Supply Chain ESG Compliance
Procurement departments require documented carbon footprints and pesticide trace transparency. Suppliers offering complete pesticide screening (GC-MS/MS), automated heat-recovery lyophilizers, and verified zero-additive chain-of-custody protocols are commanding preferred-vendor allocations.
Enterprise Manufacturing Strength & QA Verification
Operating out of Fujian Fynergy Foods' facility, our freeze-drying operations provide supply chain resilience for Fortune 500 food companies.
Industrial Scale (37 Lines)
Our footprint includes 37 dedicated lyophilization lines covering approximately 8,000 m² of vacuum chamber area. This guarantees batch consistency across multi-metric-ton supply contracts without seasonal production bottlenecks.
Certified Quality Infrastructure
Audited and verified onsite by TÜV Rheinland. We maintain BRCGS, HACCP, and ISO 22000 quality systems, with full documentation available for Kosher and Halal export markets.
In-House Analytical Chemistry
Every lot undergoes pre-shipment screening in our laboratory equipped with Liquid Chromatography, Atomic Absorption, Atomic Fluorescence Spectrophotometers, and Automated Kjeldahl nitrogen analyzers.
B2B Procurement & Technical FAQ
Common inquiries from importers, private labels, and formulation chemists regarding freeze-dried blueberry sourcing.
How do freeze-dried blueberries compare to infused dried blueberries in industrial baking?
Infused dried blueberries are processed with high-fructose corn syrup or sucrose, resulting in high moisture (12–18%), high density, and dark visual characteristics. They tend to sink in cake batters and bleed color excessively. In contrast, freeze-dried whole blueberries maintain their cellular structure, contain 0% added sugar, possess residual moisture below 4.0%, and disperse evenly without structural crushing during mechanical batter mixing.
What are your standard packaging options to prevent hygroscopic moisture absorption?
Freeze-dried blueberries are extremely hygroscopic. For bulk industrial shipments, we pack in double-layer food-grade poly bags vacuum-sealed inside corrugated master cartons (typically 10 kg or 15 kg net). Nitrogen flushing and specialized aluminum foil barrier laminates (water vapor transmission rate < 0.05 g/m²/24h) are standard for retail pouches and private label contracts.
What are the Minimum Order Quantities (MOQ) for custom cuts and private labels?
Standard industrial bulk cartons start from an MOQ of 100 kg to 500 kg depending on raw material stock and seasonal picking cycles. For custom cut dimensions (e.g., custom dice sizing of 1–3mm, fine micron powders) or printed consumer-ready stand-up pouches, the MOQ typically ranges between 3,000 and 10,000 units. Trial validation samples with full analytical Certificates of Analysis (COA) are provided prior to commercial production.
How does the lyophilization curve prevent berry skin toughening?
Skin toughness occurs when secondary desorption drying runs at excessively high shelf temperatures, denaturing natural pectin. We employ multi-stage controlled desorption cycles with gradual vacuum decay, maintaining cell wall elasticity and crisp friability across whole berry formats.
Can you provide full documentation for pesticide residues and heavy metals?
Yes. Every production run is matched to a batch-specific COA containing full trace testing results from our internal laboratory, including GC-MS/MS pesticide screening, heavy metal content (Lead, Cadmium, Arsenic, Mercury), and full microbiological enumeration (APC, Yeast & Mold, Coliforms, Salmonella, E. Coli).
Partner with a Certified Freeze-Dried Blueberry Manufacturer
Request technical specification sheets, custom mesh sizing, or sample validation lots for your upcoming formulation cycles.
Inquire Now