Customized Or Bulk Spray Dried Puer Tea Powder
- Form: Superfine Powder (80-120 Mesh)
- Rehydration: Instant Cold/Hot Water Soluble
- MOQ: 100 kg / Flexible Trial Batch
- Application: Beverages, Nutraceuticals, RTD
Engineered for maximum cellular integrity, vibrant bio-color retention, instant reconstitution kinetics, and extended room-temperature shelf stability without additives or artificial binders.
As the international food processing, functional beverage, and retail confectionery markets mature, institutional buyers must navigate tectonic shifts in clean-label regulation, moisture management, and functional formulation.
Global supermarket aggregators and multinational CPG enterprises are phasing out artificial preservatives, sulfur agents, and chemical texturizers. Freeze-drying technology addresses this paradigm by deploying physical sublimation under vacuum. Residual moisture levels consistently sit below 5%, eliminating bacterial activity while retaining native cellular morphology, authentic aroma, and biological nutrients completely naturally.
High international cold-chain freight rates and stringent temperature monitoring are driving enterprise procurement heads toward ambient-stable raw commodities. Dehydrated via precision lyophilization, our freeze-dried foods achieve a weight reduction of up to 88% to 92% compared to raw biomass, slashing ocean and air freight carbon footprints and warehousing storage costs while delivering a 24-month sealed ambient shelf life.
Procurement teams no longer source generic wholesale commodities. The contemporary purchasing landscape demands precise technical cut sizes: whole berries, standardized diced cubes (3x3mm, 6x6mm, 10x10mm), crunchy wafer slices (4-6mm), and micronized powders (80 to 200 mesh) with controlled flowability, instant cold-water solubility kinetics, and strict bulk density specifications for high-speed automated packaging machines.
Understanding the thermodynamics of vacuum sublimation versus thermal evaporation allows quality assurance leaders and procurement directors to substantiate commercial ROI and consumer loyalty.
| Evaluation Parameter | Industrial Vacuum Freeze-Drying (FD) | Hot-Air Oven Dehydration (AD) | Vacuum Frying (VF / Chip Style) |
|---|---|---|---|
| Operating Thermodynamics | Sublimation under high vacuum (<60 Pa) at -35°C to +40°C | Thermal evaporation with continuous convective heat (60°C to 95°C) | Rapid moisture vaporization immersed in low-pressure oil bath (80°C to 110°C) |
| Nutritional Retention Matrix | >94% Retention of Vitamin C, Polyphenols & Enzymes | Severe degradation (35% - 60% loss of thermolabile micro-nutrients) | Moderate loss; lipid penetration introduces thermal oxidative degradation |
| Cellular Microstructure | Rigid porous lattice preserved; 0% shrinkage or collapse | Porous matrix collapses; dense, hardened, shrink-deformed body | Crisp lipid-infiltrated crust; cellular walls altered by oil absorption |
| Rehydration Speed & Capacity | Instant rehydration (15-60 seconds) restoring native organoleptic state | Sluggish, incomplete rehydration requiring 15-45 minutes of soaking | Non-rehydratable snack food format; saturated internal structure |
| Total Oil & Fat Content | 0.0% Added Oil (Pure Native Fruit/Veg Lipids Only) | 0.0% Added Oil (Native Matrix Only) | 15% to 30% absorbed fat content from high-temperature oils |
| Storage Life & Water Activity | Aw < 0.25; 18-24 Months ambient stability in moisture-barrier film | Aw 0.45 - 0.65; Susceptible to moisture pickup, hardening & mold | Aw 0.30 - 0.40; Limited by rancidity and lipid peroxidation profiles |
The freeze-drying sector has expanded far beyond traditional single-ingredient fruits. We are pioneering high-value composite categories including freeze-dried yogurt bites enriched with active probiotics (Lactobacillus and Bifidobacterium strains verified viable post-lyophilization), melt-resistant astronaut ice cream sandwiches, cold-brew fruit tea fusion blocks, and crunchy freeze-dried candies that deliver unprecedented sensory soundscapes and intense sweetness without melting in tropical transit.
Our OEM lyophilized outputs serve as primary ingredients across multiple industrial segments. In commercial bakery and chocolate panning, freeze-dried raspberry and strawberry fragments provide natural moisture-free decoration that prevents fat bloom and moisture migration. In dry soup manufacturing, our freeze-dried vegetable dices and instant chicken broth cubes reconstitute within seconds when exposed to hot water, retaining original shape, color, and culinary savoriness.
Combining 20+ years of lyophilization engineering with institutional capital assets, we operate as a tier-1 supplier to global retail giants, Fortune 500 food conglomerates, and specialized private label brands.
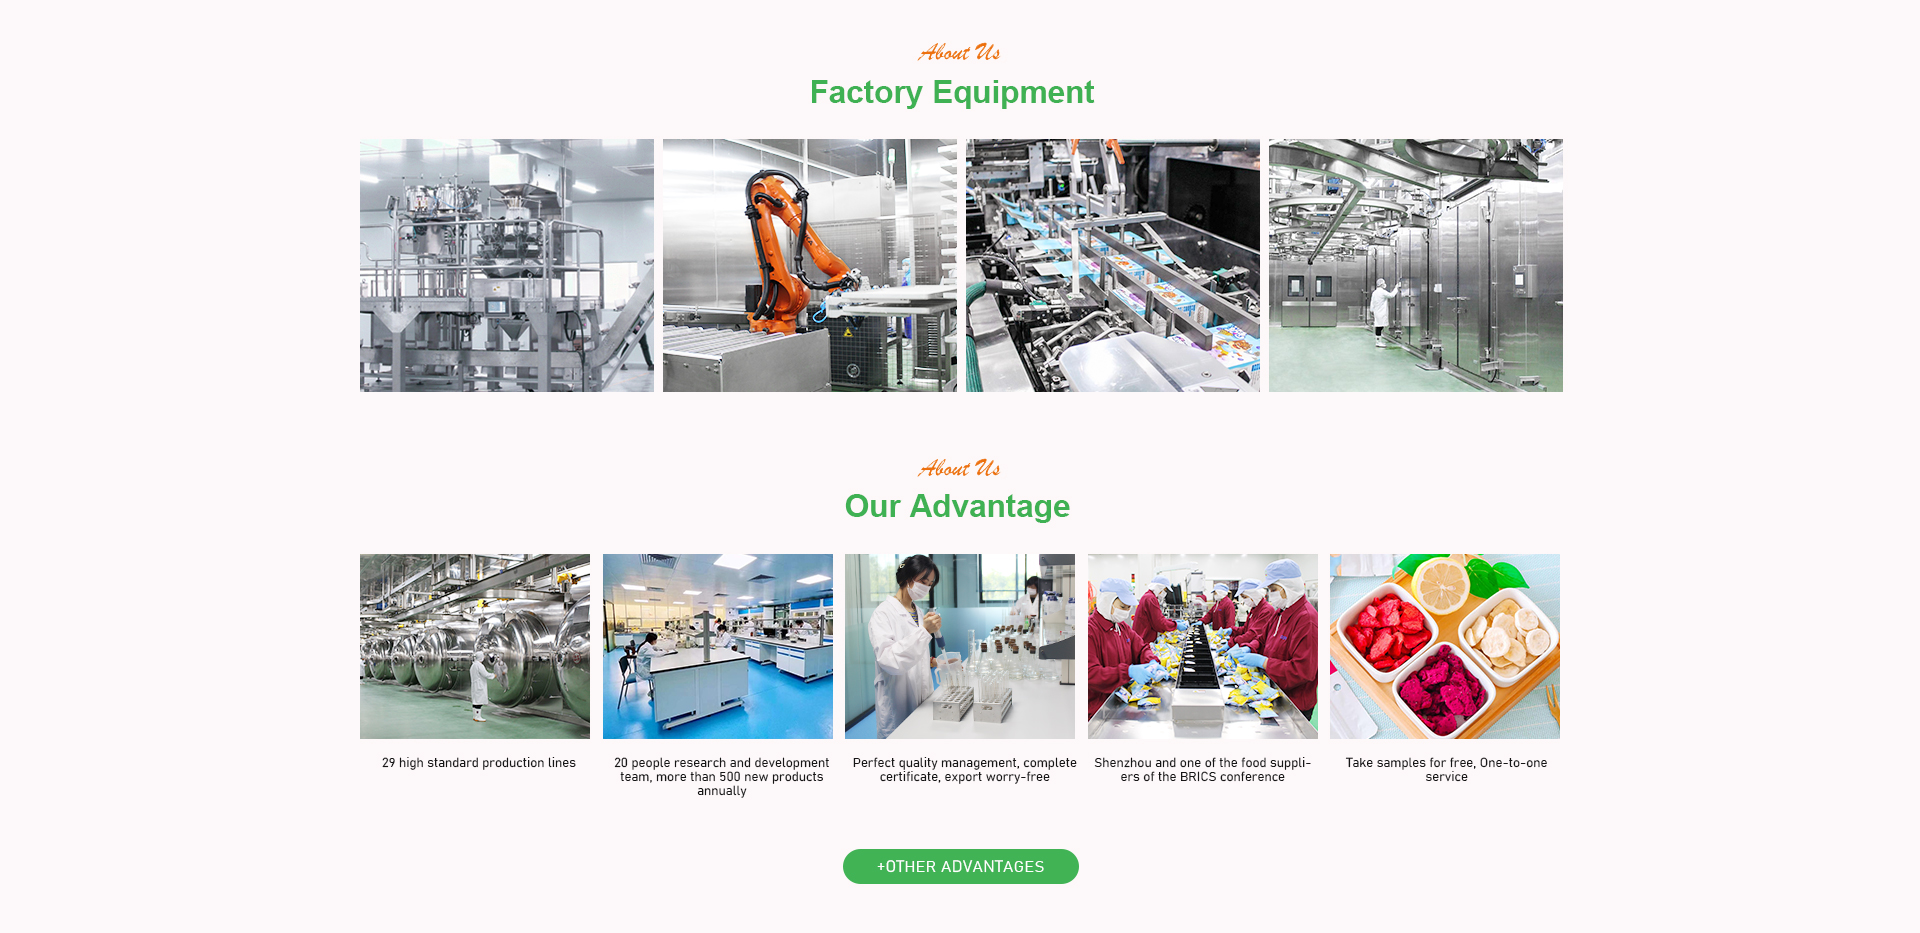
Our Zhangzhou, Fujian campus spans 62,718 m² of specialized production space. We operate strictly regulated Class-100,000 cleanroom environments for all slicing, tray loading, unloading, and packaging stages. Constant temperature and low relative humidity air handling prevent hygroscopic freeze-dried structures from absorbing atmospheric humidity during high-speed sealing.
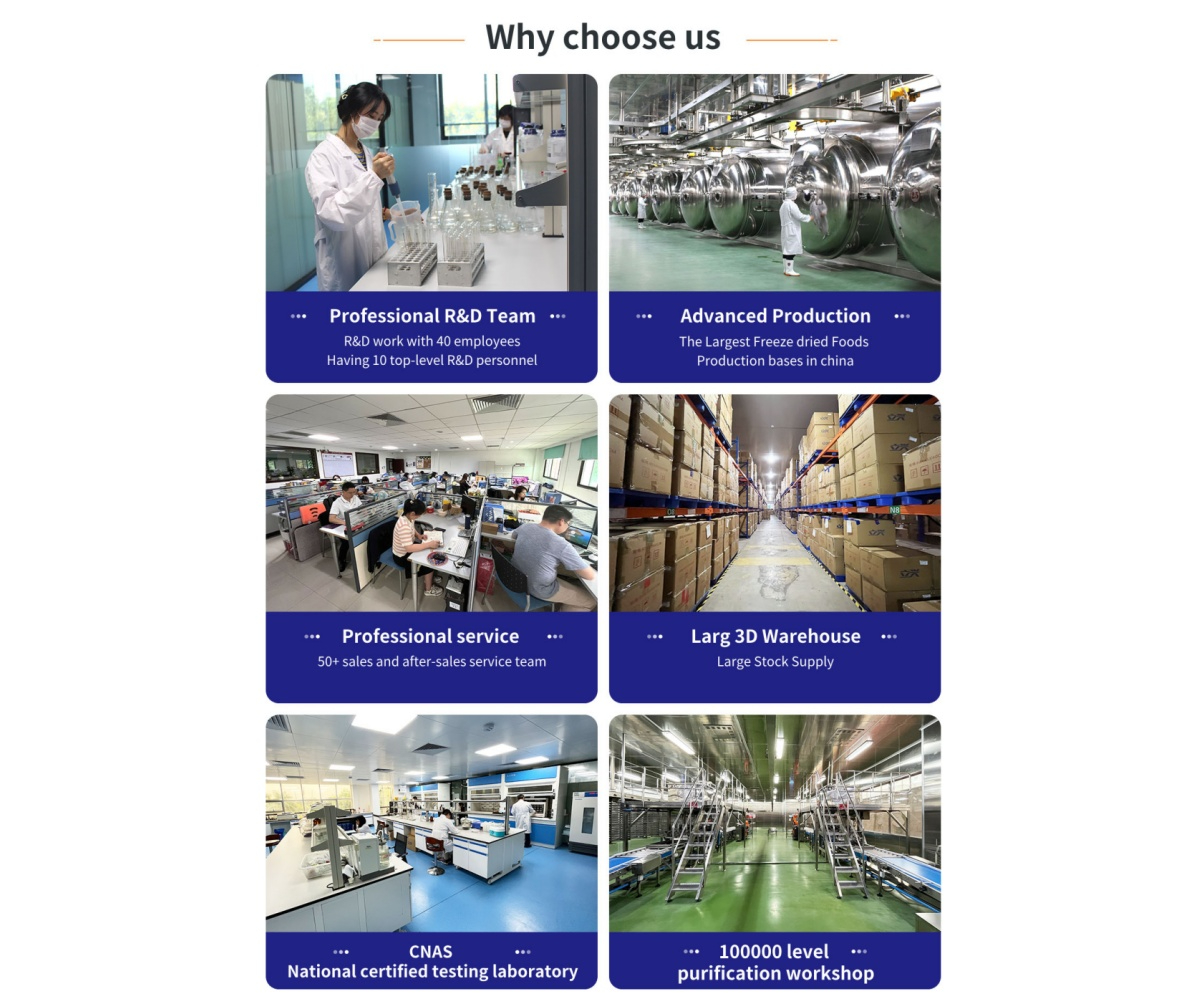
With 37 dedicated lyophilization lines and approximately 8,000 m² of vacuum chamber area, Fynergy boasts one of the largest single-site sublimation processing capacities in the Asia-Pacific region. Our automated PLC heating shelf profiles ensure homogeneous heat flux transfer across thousands of simultaneous trays, guaranteeing complete batch-to-batch uniformity and zero cold-spot residues.
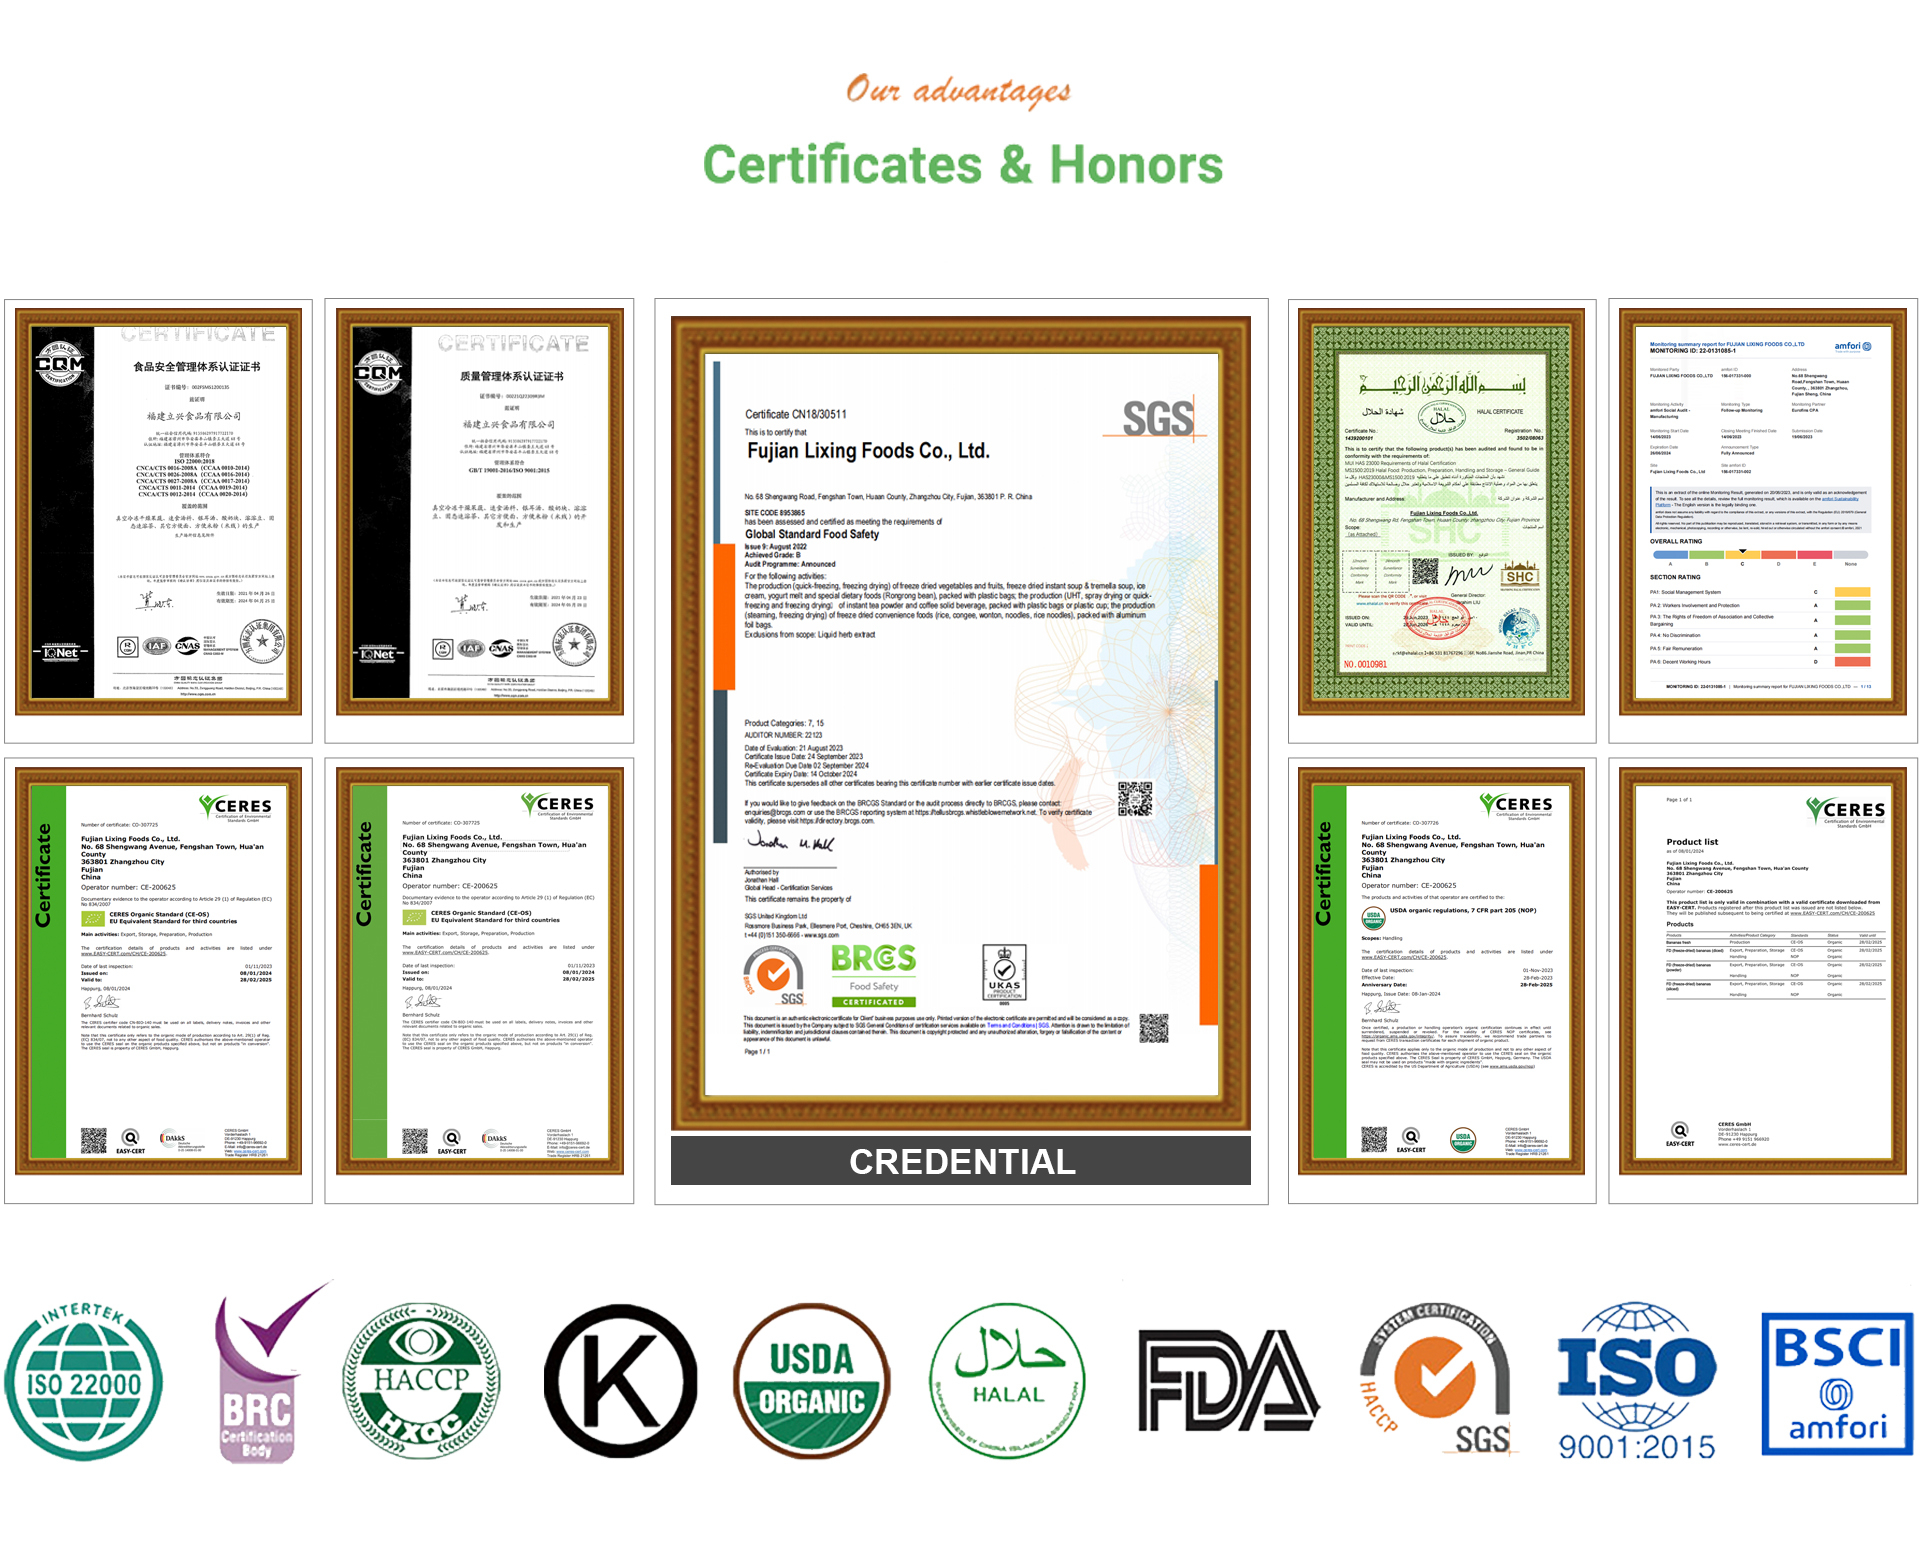
Our quality management is audited and certified under BRCGS (A Grade), HACCP, and ISO 22000 regimes, complemented by Halal and Kosher approvals for eligible item families. Furthermore, our site undergoes annual on-premise verification audits conducted by TÜV Rheinland, providing complete supply chain transparency and regulatory confidence for export compliance.
We do not rely on slow external testing contractors. Our on-site analytical laboratory is equipped with High-Performance Liquid Chromatography (HPLC), Atomic Absorption Spectrophotometers (AAS), Atomic Fluorescence Spectrophotometers, and Automated Kjeldahl nitrogen digestion systems. Every commercial production batch is tested on-premise for moisture content, microbiological counts, heavy metals, pesticide residues, and nutritional density.
We actively innovate rather than simply copy formulas. In sustained institutional partnership with prominent national food research academies, Fynergy holds 41 authorized processing patents. Our innovations span low-temperature structural preservation, natural color shielding algorithms, and proprietary freeze-dried instant matrix binders that dissolve instantly in ice water without clumping.
From high-barrier bulk carton packaging (heat-sealed aluminum composite bags with food-grade inner liners and nitrogen purging) to automated retail packaging, we offer full OEM/ODM flexibility. Our secondary packaging equipment handles doypacks, stand-up zipper pouches, transparent PET cans with easy-open aluminum ends, composite jars, single-serve sachets, and retail counter display master boxes.
Direct technical and logistical insights curated by our international export engineering and quality assurance departments.
Our minimum order quantities reflect our industrial production infrastructure while accommodating phased market trials. For standard bulk freeze-dried fruit pieces, powders, and vegetable dices packed in double-sealed polyethylene or aluminum-lined master cartons, MOQ ranges from 100 kg to 500 kg per SKU. For custom printed retail consumer packaging (stand-up zipper pouches, customized cans, and private label boxes), MOQs typically start at 10,000 to 30,000 units, dependent upon the physical dimensions and structural barrier film specifications of the requested packaging format.
Freeze-dried food matrices are naturally hygroscopic and eagerly absorb airborne moisture if exposed to normal humidity. To guarantee that our products remain below ≤4.0% - 5.0% moisture content from chamber exit to the consumer's pantry, our Zhangzhou plant operates Class-100,000 cleanrooms with dynamic dehumidification (maintaining relative humidity <35%) across all packaging zones. In addition, we utilize high-barrier multilayer foil materials (such as PET/AL/PE or metallized structures), deploy food-grade desiccants where appropriate, and offer optional automated nitrogen gas purging during final sealing.
Yes. As a verified OEM/ODM manufacturer, we can formulate and fabricate custom specifications tailored to your target application. We engineer precision cuts including whole berries, longitudinal slices (3-5mm or 5-7mm), standardized cubes (3x3x3mm, 6x6x6mm, 10x10x10mm), crushed crumbles (1-3mm, 2-6mm for yogurt toppings), and micronized powders ranging from 60 mesh to ultra-fine 200 mesh. We also develop proprietary composite recipes, such as freeze-dried fruit tea cubes with honey, fortified yogurt buttons with defined probiotic counts, and multi-ingredient instant soup blocks.
Every commercial container shipment is supported by a comprehensive technical compliance dossier. This package includes a verified Certificate of Analysis (COA) issued by our in-house testing lab detailing physicochemical parameters, residual moisture, and microbiological testing (Total Plate Count, Yeast & Mold, Coliforms, Salmonella, and E. coli). We also provide official Phytosanitary Certificates issued by China Customs (GACC), Certificates of Origin (CO, Form A, Form E, RCEP), complete allergen declarations, Non-GMO verification statements, and third-party inspection certifications from BRCGS, HACCP, ISO 22000, and TÜV Rheinland.

Spray drying relies on high-temperature atomization (where liquid extract is forced into an inlet air drying stream between 150°C and 200°C), which can denature delicate proteins, caramelize natural sugars, and evaporate volatile aromatic terpenes. In contrast, vacuum freeze-drying (lyophilization) freezes the botanical product solid to -35°C to -45°C before initiating sublimation under high vacuum. Because water transitions directly from solid ice crystals to vapor without ever passing through a liquid phase, the cellular framework remains intact and bio-active antioxidants, native polyphenols, and delicate fragrance compounds are preserved at rates exceeding 90% to 95%.
For standard catalog ingredients with spot raw materials on inventory (such as standard freeze-dried strawberry, banana, instant tea powder, or instant coffee), custom production lead times are typically 15 to 25 calendar days from deposit confirmation and technical specification sign-off. For custom-printed retail packaging involving new cylinder engraving and composite film lamination, initial production cycles run approximately 30 to 35 calendar days. Evaluation sample packages along with technical specification data sheets are typically prepared and dispatched via DHL, FedEx, or UPS within 3 to 5 business days.